
When Mercury Touches Metal, Something Invisible Happens
Mercury embrittlement is one of those failure mechanisms that shows up without warning and costs companies millions in unexpected downtime. I learned this the hard way in 2019 when a stainless steel valve in our refining unit cracked open during routine maintenance. The weld looked perfect from the outside. Inside, the grain boundaries had been completely compromised by trace mercury exposure from the process stream. It took us three months to trace the root cause. The phenomenon is straightforward in principle but treacherous in practice. When liquid mercury comes into contact with certain metals — particularly steels, aluminum alloys, and copper-based materials — it penetrates along grain boundaries through a mechanism called liquid metal embrittlement (LME). The result is a dramatic loss of ductility. A material that could previously bend and absorb energy becomes brittle at room temperature. Cracks initiate and propagate with minimal applied stress. The chemistry behind this is not well understood by most engineers. It involves adsorption of mercury atoms at crack tips, reduction of surface energy, and stress-assisted diffusion. The key point is that this happens at ambient temperatures. You do not need elevated heat or pressure. This distinguishes mercury embrittlement from other forms of liquid metal cracking like those caused by gallium or sodium.
How to Detect It Before It Fails
Visual inspection alone will not catch mercury embrittlement. The damage is internal. Here is what actually works in practice. Ultrasonic testing is your first line of defense. Use a phased array probe at 5 MHz minimum frequency. Look for subtle changes in sound velocity and attenuation patterns. Normal steel shows consistent readings. Embrittled zones display scattered signals even when the material looks intact externally. I typically scan at 10-millimeter spacing on critical welds. A full scan of a single valve assembly takes about 45 minutes on a well-tuned system. Acoustic emission monitoring catches early-stage cracking during pressurization. Attach piezoelectric sensors near suspected zones and monitor for micro-fracture events. Signal thresholds below 40 dB usually indicate stable conditions. Anything above 60 dB in the 100 kHz to 1 MHz range suggests active crack propagation. This method requires baseline measurements from known-good specimens. Without a reference, you cannot distinguish noise from real events.
Scanning electron microscopy with EDS confirms contamination after failure. Cross-section the fracture surface, polish it, and look for mercury peaks in the energy-dispersive spectrum. Mercury shows up at 2.3 keV and 9.97 keV. These peaks are unmistakable when present. However, mercury can migrate during sample preparation, so seal specimens immediately after cutting. Delay of more than two hours compromises results. Hardness mapping around affected zones reveals embrittlement indirectly. Measure Vickers hardness at 0.5-millimeter intervals from the surface inward. Embrittled regions often show 15 to 30 percent hardness reduction compared to unaffected base metal. This is not diagnostic alone but provides supporting evidence when combined with other methods.
Get the Full Details

Prevention Strategies That Actually Work
Eliminating mercury exposure is ideal but often impossible in existing facilities. Here are practical mitigation approaches. Material selection matters enormously. Austenitic stainless steels like 316L show better resistance than ferritic grades, but no steel is immune to prolonged mercury exposure. In high-risk environments, consider nickel-based alloys like Inconel 625 or Monel 400. These cost three to five times more per kilogram but last ten to twenty times longer under mercury service conditions. The economics work when you factor in unplanned shutdown costs. Surface coating provides temporary protection. Apply thermal-sprayed aluminum or nickel aluminide layers at least 150 micrometers thick. These coatings create a barrier between mercury and the substrate. Maintenance intervals depend on coating quality and flow conditions. Typical service life ranges from eighteen months to three years before reapplication becomes necessary. I found that plasma-sprayed coatings outperform pack cementation in turbulent flow service.
Mercury removal systems upstream of sensitive equipment reduce exposure risk. Activated carbon beds, gold-coated sorbents, and chemical scrubbers can remove mercury to sub-ppb levels. Design contact time of at least thirty seconds for carbon beds at typical gas velocities. Pressure drop across a properly sized bed stays below 5 kPa. When breakthrough occurs, replace media immediately rather than attempting regeneration. Spent mercury sorbents require hazardous waste disposal procedures. Operational controls complement engineering solutions. Monitor mercury concentrations continuously with gold film sensors or cold vapor analyzers. Set alarm thresholds at 10 ppb and trip actions at 50 ppb in gas streams contacting susceptible materials. Logging intervals of one minute provide sufficient resolution for trend analysis without overwhelming data storage.
Edge Cases and Failure Modes You Should Know About
Not all mercury embrittlement behaves the same way. Some scenarios catch engineers off guard. Cold working increases susceptibility dramatically. Strained stainless steel subjected to mercury exposure can fail at stresses as low as 20 percent of yield strength. This is far below design allowances. I once reviewed a case where a bent tube in a heat exchanger cracked at operating pressure because the forming operation had not been followed by stress relief annealing. The fix was complete replacement with annealed tubing. Local repair was not viable. Transient mercury pulses cause delayed failure. Brief exposure events followed by dry periods still produce embrittlement. The mercury remains trapped at grain boundaries and continues to degrade properties over weeks or months. This time-dependent aspect makes hazard assessment difficult. Assume worst-case accumulation unless proven otherwise through sampling and analysis.
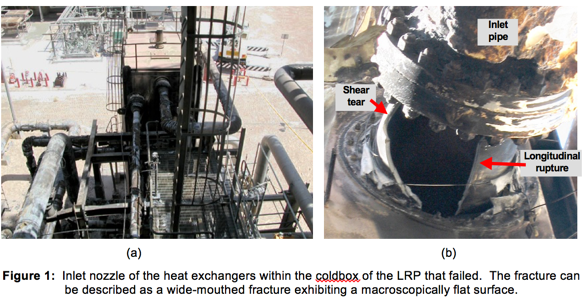
Galvanic couples complicate remediation. When mercury-containing components interface with dissimilar metals, electrochemical effects can accelerate degradation. I encountered a situation where copper alloy fittings adjacent to mercury-exposed steel showed accelerated cracking due to formation of mercury-copper amalgams at the interface. Isolation with non-conductive gaskets and fittings eliminated the problem. This workaround added two days to the shutdown schedule but prevented recurrence over the next five years. Inspection gaps hide damage. Standard hydrostatic pressure tests do not detect incipient embrittlement. A vessel can pass a 1.5-times-design-pressure hold test and still fail under normal service conditions due to subcritical crack growth. Incorporate NDE into periodic inspection regimes. Ultrasonic volumetric inspection every twelve months catches progression before it reaches critical size.
What to Do When You Suspect Mercury Exposure
Take systematic action rather than guessing. Here is a practical sequence. First, review process history for any mercury sources. Feedstock specifications, catalyst regeneration streams, and environmental control equipment discharge are common origins. Request analytical data going back at least five years. Trends matter more than single measurements. Second, identify all susceptible materials in contact with potentially contaminated streams. Make a complete inventory including welds, heat-affected zones, and cold-worked regions. Mark each item with its fabrication date and any post-weld heat treatment records. This documentation becomes critical for root cause analysis if failures occur.
Third, prioritize inspection based on risk ranking. Assign scores for exposure duration, stress level, material susceptibility, and consequence of failure. Rank items from highest to lowest priority. Begin with the top twenty percent of the list. These receive full NDE coverage including UT, AE monitoring where feasible, and hardness surveys. Fourth, establish a monitoring program for continuing operations. Install mercury detectors at strategic locations. Train operators to recognize warning signs such as unusual vibration, pressure fluctuations, or coating deterioration. Report any anomalies immediately. Do not wait for scheduled inspections. Fifth, budget for remediation before problems escalate. Replacing susceptible components proactively costs ten to twenty percent of emergency repair expenses. Factor coating maintenance, media replacement, and inspection labor into annual operating budgets. Unexpected failures disrupt production schedules and attract regulatory scrutiny.

When Mercury Embrittlement Cannot Be Managed
Sometimes the only viable solution is complete redesign. If mercury concentrations exceed 100 ppb in gas streams and operate continuously above 60°C, even nickel alloys show accelerated degradation. In these conditions, consider ceramic-lined vessels, fluoropolymer-coated internals, or alternative process pathways that eliminate mercury contact entirely. The capital expenditure is substantial but cheaper than repeated failure cycles. Mercury embrittlement demands respect, not fear. Understand the mechanisms, inspect regularly, and act on evidence rather than assumptions. The engineers who manage this risk successfully are the ones who plan ahead and maintain disciplined inspection programs.


