Coil design isn't glamorous, but it's where most projects either scale or fail quietly
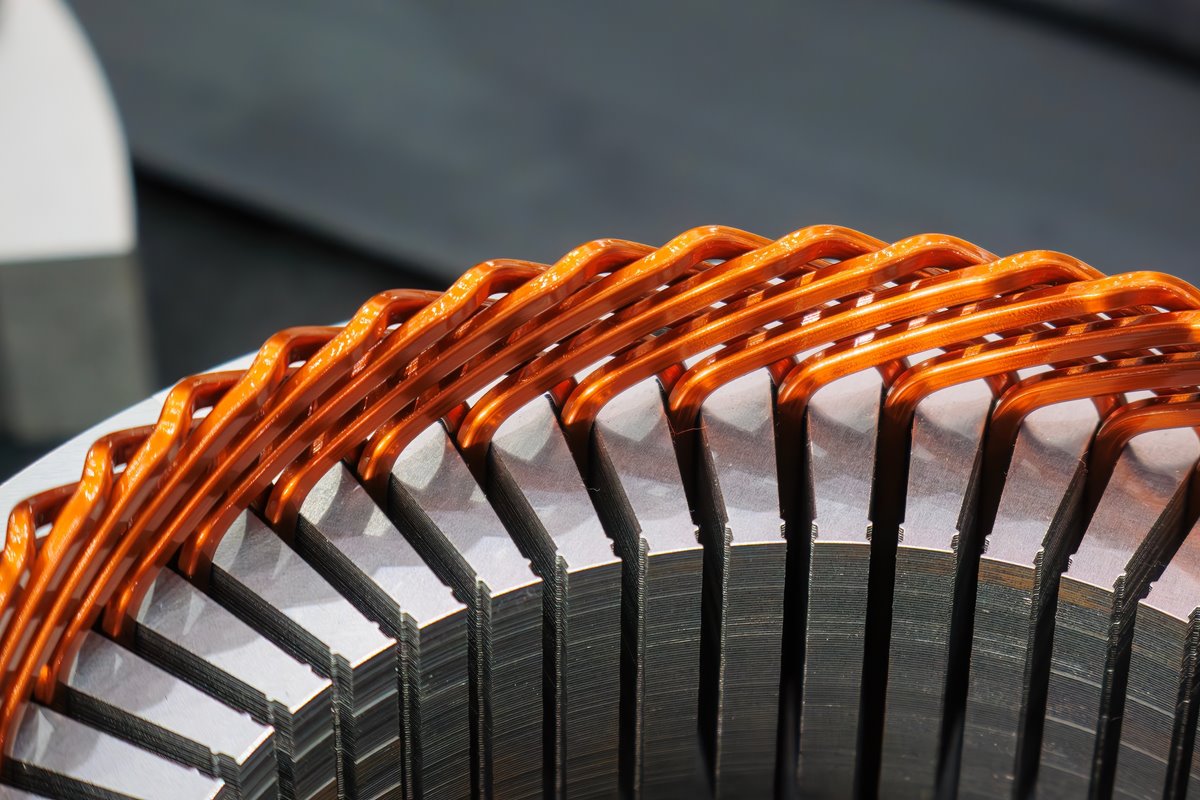
I spent three years working on electromagnetic system optimization before I started taking this seriously. Most engineers treat coils as black boxes — you pick a gauge, wind it, slap a core on it, and pray the simulation matches reality. It rarely does. The gap between theoretical and actual performance comes down to how you think about the winding process itself. Not just the geometry, but the physical constraints that show up when you move from a spreadsheet to a workbench. Let me walk through what actually matters when you're designing a coil for a real application. The parameters most people start with are wire gauge, number of turns, and core material. Those are correct starting points, but they're incomplete. You need to account for fill factor — the ratio of copper volume to total winding volume. A well-designed hand-wound coil might achieve 55-65% fill factor. Machine-wound with proper tensioning and layering, you can push toward 70-75%. That difference isn't academic. It directly affects your resistance, your thermal profile, and your magnetic field uniformity. Here's where people make mistakes. They calculate the wire length based on mean turn diameter and multiply by turn count, then select a spool size. What they forget is that each successive layer adds approximately one wire diameter to the mean turn circumference. After five layers, you could be off by several percent on your resistance calculation. I learned this the hard way on a custom solenoid project for a medical device prototype. The datasheet resistance was 12 ohms. The actual coil measured 14.7 ohms. Took me two days to realize I'd been calculating from the inner layer diameter rather than accounting for the build-up across all seven layers. The fix was simple — use the outer diameter of the wound package, not the bobbin diameter, and recalculate mean turn length as the average of inner and outer circumference across all layers.
Thermal management is where strategic coil design actually separates itself from basic coil making. Power dissipation in a coil follows I-squared-R, so higher current demands exponential heat management, not linear. The surface area available for heat transfer depends on your winding geometry. A compact solenoid with dense layering traps heat in the inner layers while the outer layers stay relatively cool. That temperature gradient creates thermal stress on the insulation — enamel on magnet wire degrades faster than the datasheet suggests when you have sustained hot spots. For high-current applications, I typically specify hollow-core windings or use insulated spacer tubing between layers to create cooling channels. It costs more and takes longer to wind, but it prevents the kind of premature insulation failure that shows up six months into a field deployment. There's a counter-intuitive thing about laminated cores that beginners miss. More lamination layers don't always mean lower eddy current losses if your winding strategy doesn't account for flux fringing at the core interfaces. When you have a gapped core or a non-uniform magnetic path, the flux density redistributes at the boundaries, and your inner winding layers see different inductance characteristics than your outer layers. This becomes a real problem in transformer design where you're trying to maintain tight coupling between primary and secondary. I once spent a week troubleshooting why a dual-winding transformer kept overheating under load. The simulation looked fine. The issue was that the primary and secondary weren't interleaved — they were wound sequentially, which meant the leakage inductance was three times higher than my model predicted. Switching to an interleaved wind pattern dropped the effective leakage inductance and reduced the copper loss enough to solve the problem without changing any other parameters. Wire selection deserves more attention than it gets. The default choice is usually enameled copper because it's cheap and readily available. But for high-frequency applications above 10 kilohertz, skin effect starts eating into your effective conductor cross-section. At 100 kilohertz, a 20 AWG wire is effectively using only about 40% of its copper cross-section for conduction. Litz wire solves this by using multiple individually insulated strands woven in a specific pattern, but it's expensive and harder to terminate. For medium-frequency applications, solid silver-plated copper wire is a reasonable middle ground — the plating reduces surface oxidation and improves high-frequency performance slightly without the cost of full Litz construction.
Another practical consideration that nobody mentions in the textbooks is mechanical stability during operation. A coil that's properly wound on the bench will still loosen over time if you're subjecting it to vibration or thermal cycling. I've seen coils where the winding pack moved enough to change the inductance by 3-4% after a few hundred thermal cycles. The standard workaround is varnish impregnation — dipping the completed coil in epoxy or polyurethane varnish and curing it. This locks the windings in place and improves thermal conductivity from the copper to the external surface. The trade-off is that you can't modify or repair the coil afterward without destroying it. When you're designing for mass production, the winding process itself becomes a design parameter. Consistent tension during winding affects the final dimensions and electrical characteristics. Automatic winding machines can maintain tension within a few percent, but each machine has its own quirks. I've found that the best approach is to wind sample batches on the actual production equipment and measure the results rather than relying on theoretical calculations. Even small variations in bobbin tolerance or wire diameter tolerance accumulate across hundreds of turns and shift your final parameters measurably. The biggest bottleneck I see in modern coil design isn't the physics — it's the disconnect between the design team and the winding operation. Engineers will optimize a winding pattern on paper that's mechanically impossible to reproduce consistently. Overlap windings with tight tolerance, for example, require specialized tooling and skilled operators. If you're designing for a production run of fifty thousand units, the winding process needs to be robust enough that a technician changing shifts doesn't produce a coil that's ten percent out of spec. That means designing with manufacturing constraints in mind from the start, not retrofitting after the prototype phase.
Get the Full Details
For those looking to get better at this, there's no substitute for actually building coils and measuring them. Start with simple solenoids on ferrite rod cores and map out the relationship between your calculated and measured inductance across different frequencies. Then move to transformers and pay attention to leakage inductance and inter-winding capacitance. The numbers on your LCR meter will tell you things your simulations missed. That gap between prediction and measurement is where the actual learning happens.