What You Actually Need To Know About Precision Gunsmithing
Most people think gunsmithing is about making things look pretty or chasing the lowest possible group size at the range. It isn't. It's about understanding that a rifle is a machine where every component interacts with every other component under extreme conditions, and your job is to make those interactions predictable. Murphy's approach to this work has always been rooted in the idea that precision isn't something you add to a gun. It's something you reveal by removing the variables that cause inconsistency. I've spent years working on action-jobbed rifles, rebarreling hand-guns, and fixing weapons that people brought in after they'd already tried everything else. The common thread I see in every botched build is the same thing: someone rushed a fit or ignored a measurement that looked close enough. Close enough doesn't hold true downrange. Here's how the actual work breaks down when you do it right.
Starting With The Stock And Bedding
A gun only shoots as well as its interface with the stock allows it to. The most common mistake I see is people bedding a gun and then torquing the action screws immediately, wondering why their zero shifts between 40 and 80 degrees. The correct sequence is to bed the gun cold, let the epoxy cure fully, then check the fit across a temperature range if you're building for serious work. I once had a guy bring me a Weatherby that was shooting one-inch groups at 100 yards in July and three-inch groups the same week in January. We stripped it down, found that the stock had a hairline crack running along the bottom of the forearm that was opening and closing with temperature changes. The bedding was perfect. The stock was the problem. We replaced the stock and the rifle went back to consistent sub-MOA at any temperature I tested it in. When bedding a rifle action, use a thick epoxy like J-B Weld or a purpose-made bedding compound. Thin epoxy will shrink more and introduce stress points. Apply it sparingly. You want the action to seat into the bedding without creating a vacuum seal that prevents it from sitting fully. If the action won't seat all the way because the bedding is blocking the way, you've applied too much material or your action channels aren't cut wide enough.
The Barrel: Fit Matters More Than Brand
People spend a fortune on barrels and then don't think about how the barrel actually fits into the receiver. Chamber length, headspace, and throat dimensions are where most accuracy dies before the bullet even leaves the muzzle. I had a customer who wanted a custom match barrel for a Remington 700 action. He picked a heavy contour barrel from a well-known manufacturer and we got it fitted. Freebore measurement came back fine, but when I ran a field gauge, it showed the chamber throat was inconsistent by about .020 inches from one side to the other. That might not sound like much. At 300 yards with match ammo, it meant the bullet was jumping to the lands at different points depending on which side of the chamber the case sat against during firing. We swapped the barrel and found one from a different manufacturer that had tighter chamber tolerances. The difference at the range was immediate and measurable without changing anything else about the build. When fitting a barrel, always check headspace with both a close and a field gauge. If the barrel won't go on properly because the headspace is off, you need to either retime the barrel or send it back to the gunsmith who chambered it. Don't try to force a barrel onto an action that doesn't match. You'll strip the threads and create a problem that costs three times as much to fix.
Get the Full Details
Action Work And Trigger Jobs
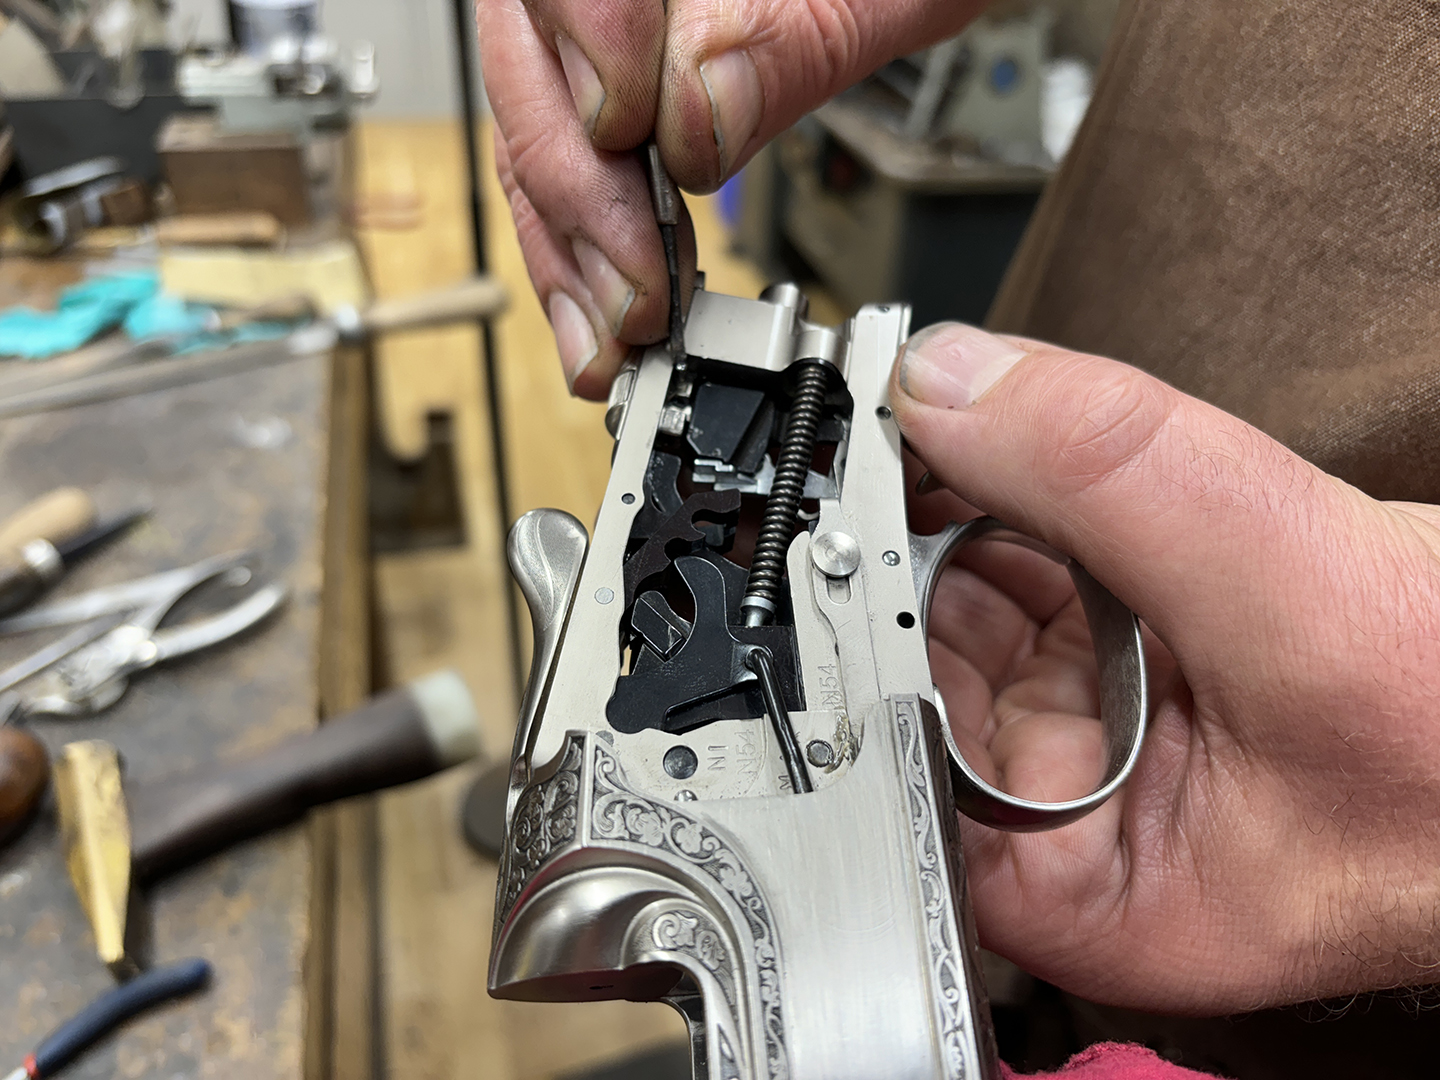
The action is the heart of the rifle, and action work is where most DIY builds fall apart. Fitting an action to a stock requires precision in a way that most people don't expect. The screw holes in the stock have to align perfectly with the action's threaded inserts. If they don't, you're either going to have to drill and tap new holes, which weakens the stock, or you're going to have a loose action that moves under recoil. Trigger jobs are another area where people go too far. A trigger should break cleanly and consistently. Pull weight is secondary. I've seen triggers pulled down to two pounds on hunting rifles that ended up being unsafe in the field. A four-to-five pound trigger on a bolt-action rifle is more than adequate. What matters more is the creep and the wall. If you can feel the trigger moving before it breaks, that's creep, and that's what affects your shot placement, not the pull weight. I worked on a Sako rifle once where the previous owner had taken it to a shop that filed the sear surfaces to reduce pull weight. They removed so much material that the trigger was hanging and the safety was unreliable. We had to fit a new sear set from the manufacturer. The total repair cost more than the trigger job would have cost if done correctly the first time. Shops that advertise trigger jobs starting at fifty dollars are almost always doing cosmetic work. Real trigger work takes hours and requires the right tools and jigs.
Scope Mounts And Optics Alignment
This is where I see the most wasted money. People buy expensive scopes and then mount them poorly. A scope ring that isn't aligned with the bore axis will introduce error that no amount of turret adjustment can fix. The proper way to mount a scope is to use alignment bars or a laser boresighter to ensure the rings are concentric with the bore before you torque anything down. I once took apart a build where someone had used a self-centering scope mount system. The mounting bases were drilled and tapped into the receiver with what they thought was Loctite. They weren't. Over time, the vibration of firing worked the bases loose, and the scope was shifting approximately .5 MOA per session. The scope itself was fine. The mount was the problem. We re-drilled, re-tapped with proper thread-locking compound, and torqued the bases to spec. The rifle went from shooting inconsistent groups to consistently sub-MOA. Same scope, same rifle, same ammunition. Just a proper install.
Final Checkout And Validation
A finished rifle needs to be test-fired and records need to be kept. I shoot every build I do through at least fifty rounds before I consider it done. I group the ammunition I know the shooter will use, because different loads can behave differently in the same rifle. I also record the ambient temperature, humidity, and wind conditions. These numbers matter later when you're troubleshooting why a rifle that shot well last month is suddenly not grouping like it used to. If you're building a precision rifle and don't have access to a range, you're cutting corners. There's no substitute for seeing how the gun actually performs. A bench rest rifle that hasn't been shot after build is just an expensive paperweight until it goes through a real target. The real secret to this kind of work isn't any single technique or tool. It's the habit of measuring twice and not assuming anything is close enough. Murphy's philosophy on this was straightforward: if something can go wrong, it will, so you measure it, check it, and verify it before you move to the next step. Most people skip the verification part. That's the difference between a rifle that shoots and one that doesn't.