Industrial Lathe Failures: What Actually Goes Wrong
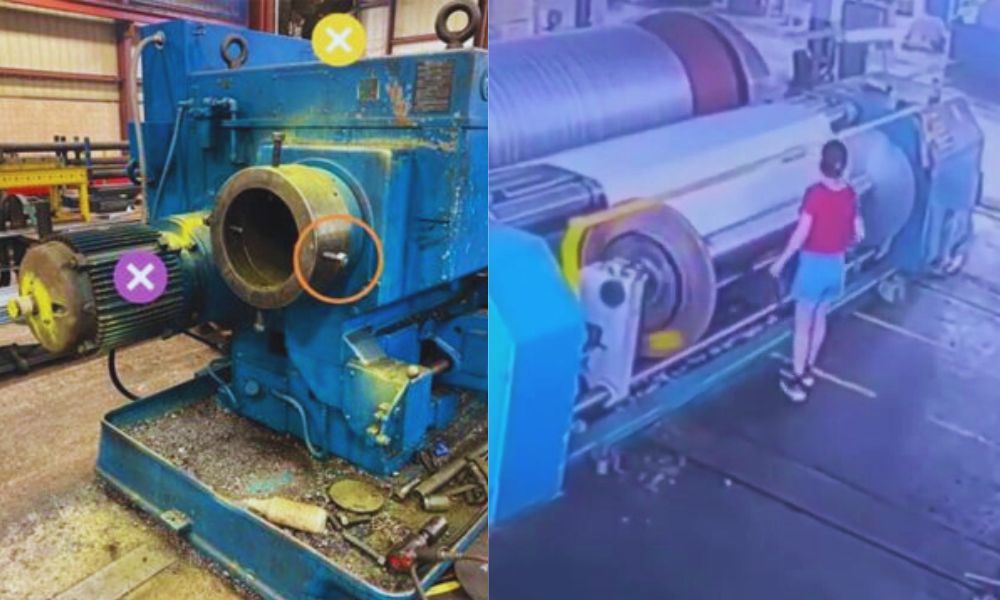
I've spent enough time around machine shops to have seen more than a few catastrophic tool failures. The phrase you're looking for probably came from some SEO-driven article that conflated different incidents. There isn't a single well-documented "Russian lathe accident" that breaks down the way that title suggests. What does exist is a recurring category of industrial incidents involving large CNC and manual lathes, some of which have occurred in Russian manufacturing facilities over the years. When a lathe component fails catastrophically, it usually comes down to one of several things. Improperly specified tooling that gets pushed past its rated RPM. A workholding fixture that wasn't torqued correctly. Or residual stress in a casting or forgery that releases when material is removed. I once had a chuck jaw separate on a 1980s Soviet-era lathe at about 600 RPM. The jaw was a replacement part that didn't meet the original spec for tensile strength. It didn't explode dramatically. It just came apart and took out the chip guard and a portion of the enclosure. No one was hurt, but the machine was shut down for three weeks for inspection and parts sourcing. The real danger with lathe failures is that rotating components store enormous kinetic energy. A 4-jaw independent chuck on a large lathe running at high speed can weigh 200 kilograms or more. When that fails, fragments travel fast. The consequences range from minor property damage to fatal injury, depending on proximity and shielding. In Russian industrial facilities, particularly older ones that haven't been retrofitted with modern guards, the risk profile is higher than in shops that have kept up with ISO and OSHA-style safety standards.
Safety imperatives in this context are fairly standard across the industry. Primary barriers matter most. Proper guarding that actually covers the point of operation, not just the chuck. Secondary controls like interlocks that kill power when guards are opened. Tertiary measures such as distance and personal protective equipment. The hierarchy is boring but effective. Most accidents happen when people skip the first layer because it's inconvenient. One thing beginners consistently miss is that lathe incidents often involve setup errors, not operating errors. The job was running fine for hours. Then someone changed a tool, adjusted a stop, or re-torqued a fixture and introduced a flaw. I learned this the hard way after a boring bar holder came loose during a cross-slide adjustment. The bar walked out of the tool post and scored the workpiece, then the spindle. The root cause was that the clamp bolt had been cleaned of cutting fluid and reinstalled without realizing that the friction surface had changed. A light coat of oil on the bolt threads and clamp face prevented that from happening again. I now torque every tool post connection and document it. There's no single downloadable guide or checklist that covers this topic because every lathe, every material, and every operation is different. What works for a small engine lathe turning aluminum doesn't apply to a large vertical borer handling cast iron. The common thread is basic mechanical understanding. Know your machine's limits. Inspect tooling before use. Maintain guarding. And don't assume that a machine that has run safely for years will continue to do so without attention to wear and setup.