NDT in Seattle Is Not What You Think It Is
Seattle Ndc Unlocking The World Of Nondestructive Testing For The Modern Era
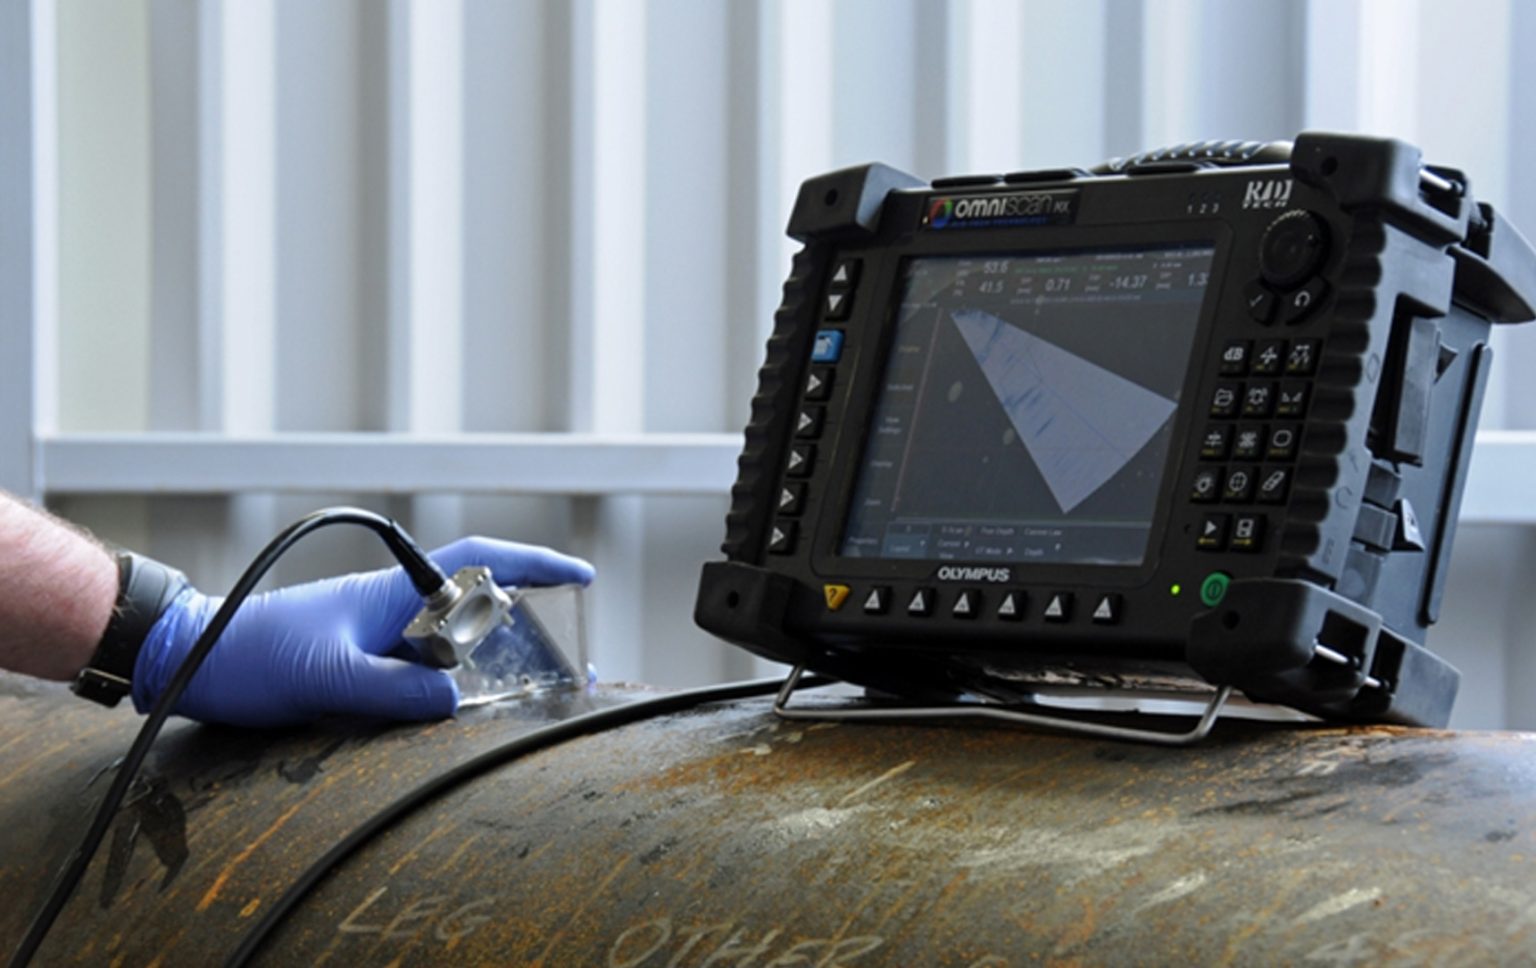
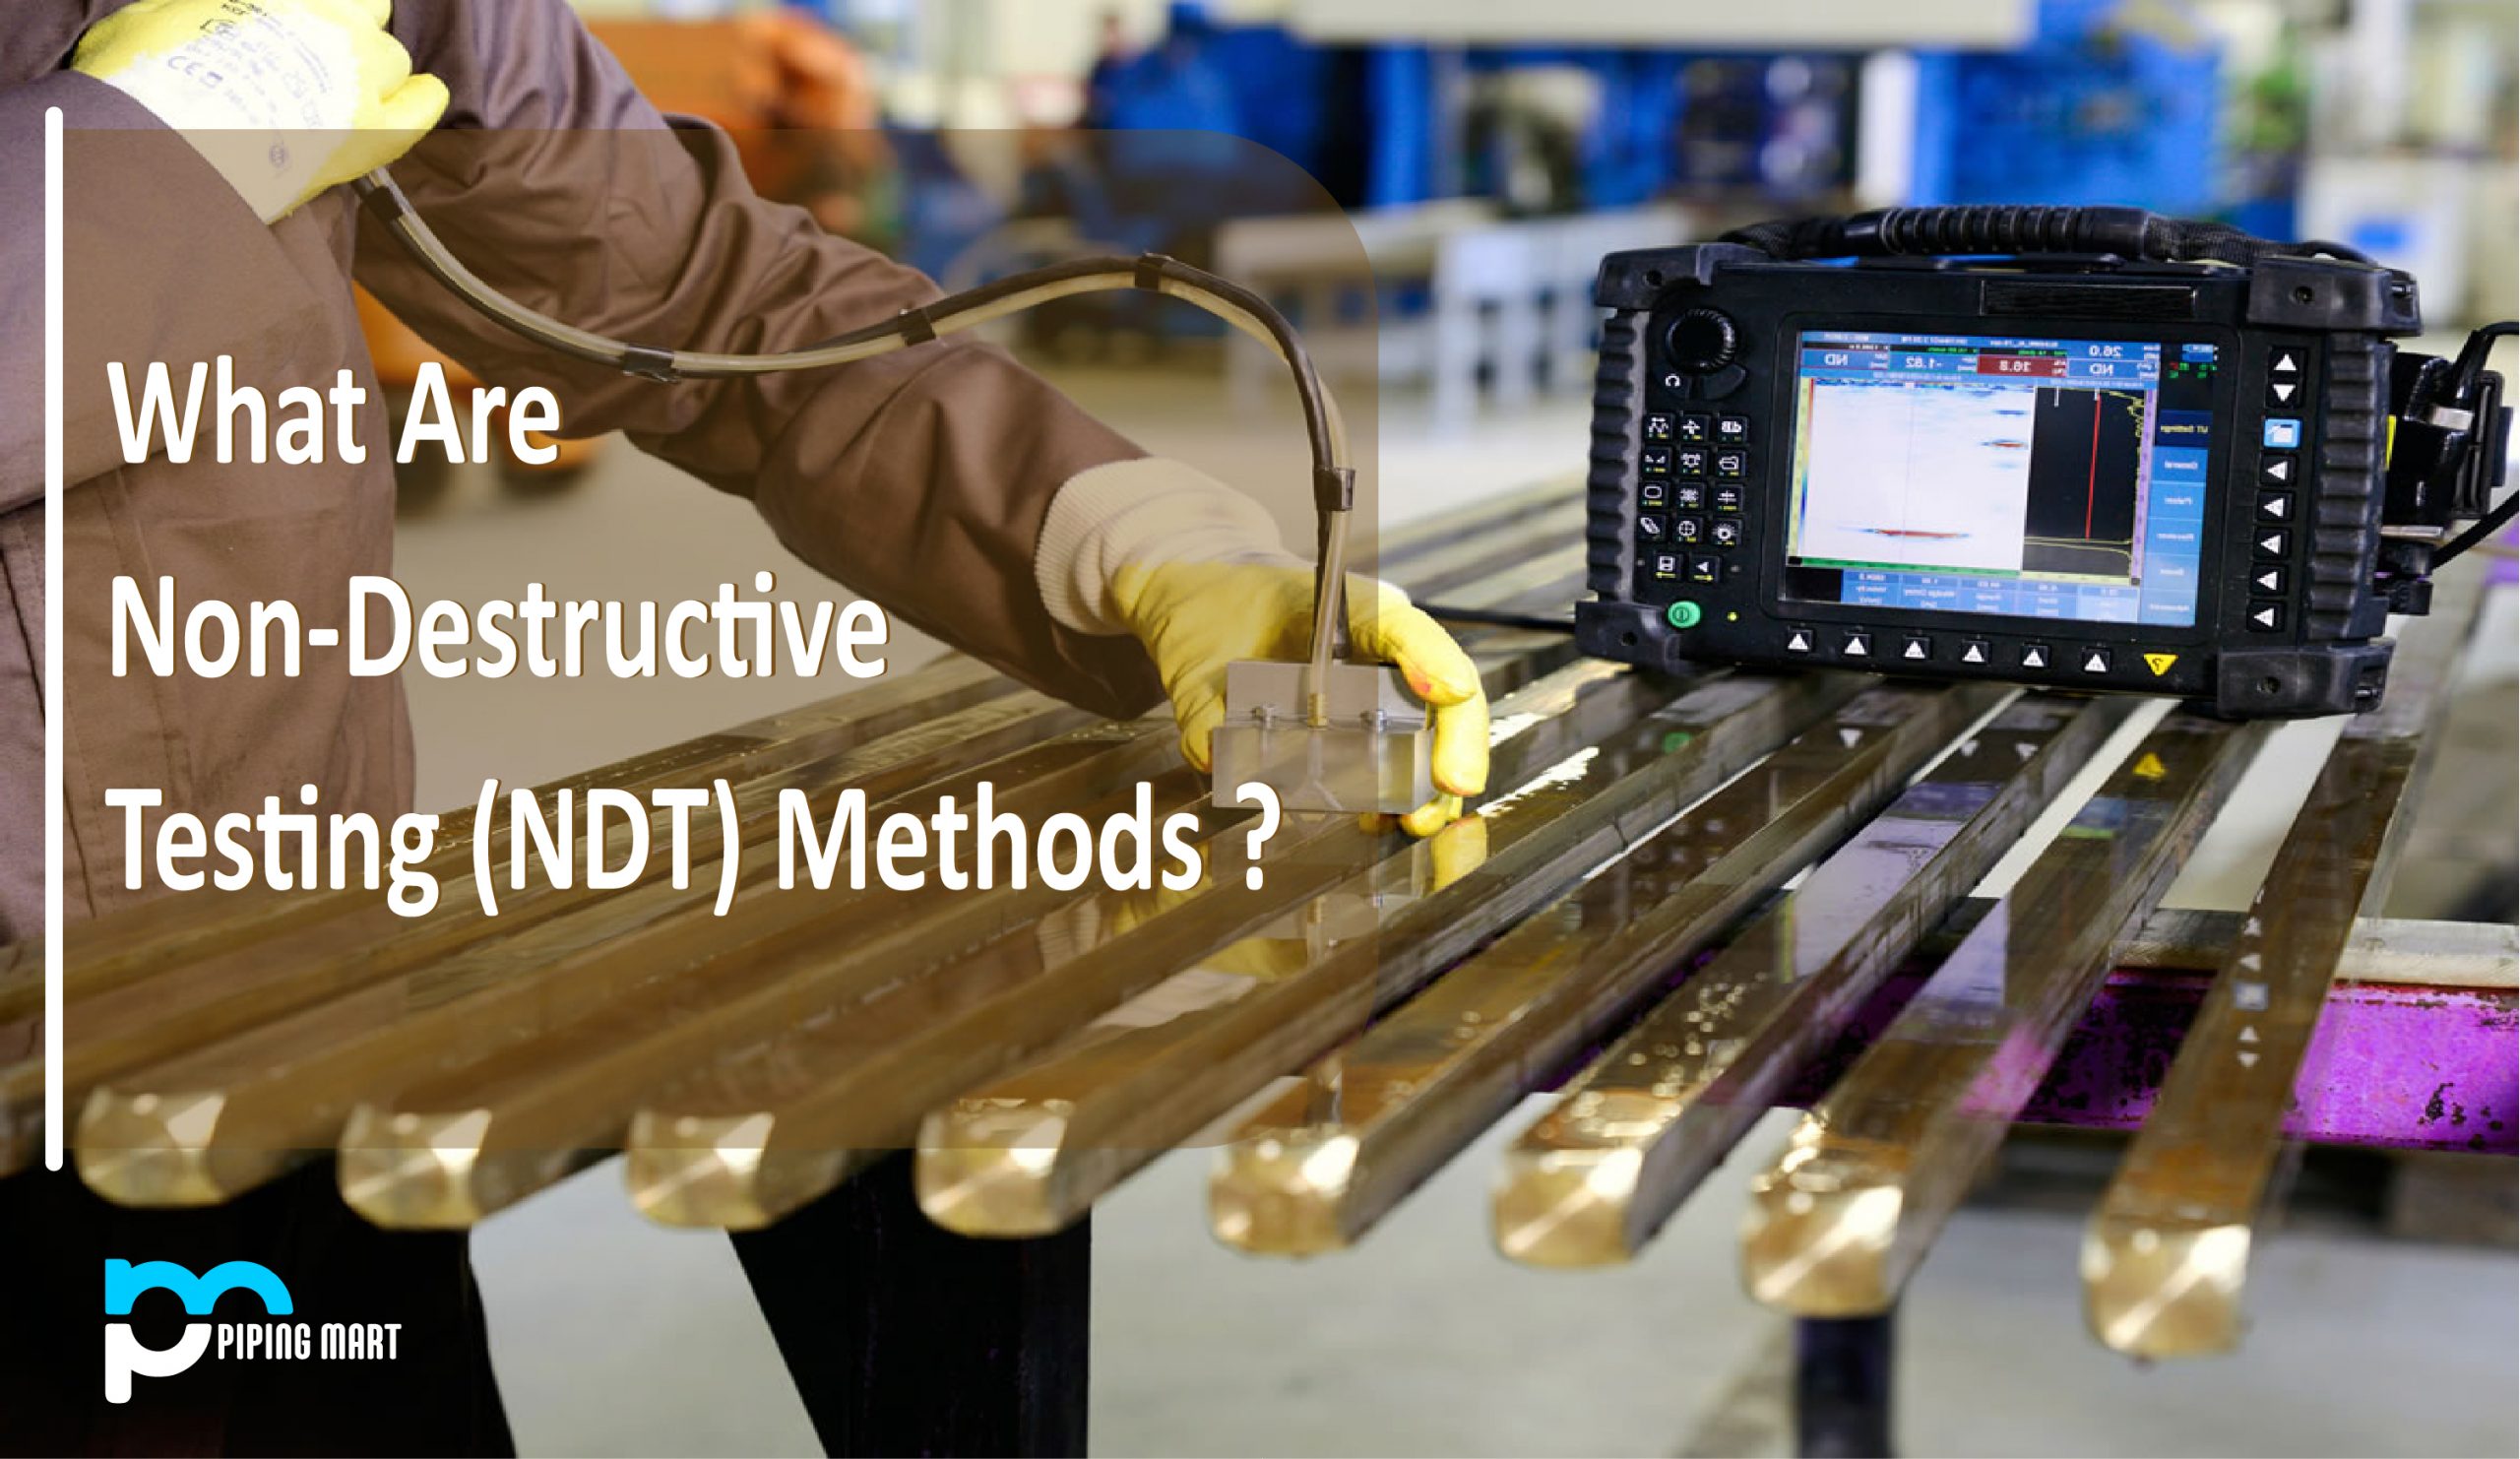
If you are new to nondestructive testing in the Seattle area, the first thing you need to understand is that this city runs on aerospace and maritime work. Boeing. Lockheed Martin. The shipyards. Every NDT professional here answers to AS9100 quality standards, and the paperwork can be just as punishing as the actual inspection. I spent seven years doing phased array ultrasonic testing on Boeing 737 fuselage panels, and let me tell you — the method itself is straightforward. The documentation, the calibration blocks, the traceability requirements, that is where most people choke. Nondestructive testing covers a range of methods. Ultrasonic testing uses high-frequency sound waves to detect internal flaws. Magnetic particle inspection catches surface cracks in ferromagnetic materials. Dye penetrant does the same for non-porous surfaces. Radiography uses X-rays or gamma rays. Eddy current testing finds cracks in conductive materials. Each has its place. Each also has scenarios where it simply will not work, and beginners often waste weeks trying to force the wrong method onto a job. In Seattle, the dominant method is phased array ultrasonics. Traditional ultrasonic testing sends one beam at a time. Phased array uses multiple elements fired in sequence to steer and focus the beam electronically. This means you can scan a weld in a single pass and get a cross-sectional image rather than a series of amplitude readings. The equipment costs more upfront, but the throughput gain is real. We typically cut inspection time on a standard butt weld from about forty-five minutes down to ten or twelve minutes per joint, assuming the access is reasonable and the surface preparation is clean.
Here is something most guides do not mention. Phased array is not a magic bullet for every geometry. I worked on a project inspecting rivet holes in a corrosion-alloy stringer where the curved surface and the tight clearance between adjacent rivets made proper couplant contact nearly impossible. The instrument would give false calls on every third hole because of backwall noise from the curve. I solved it by fabricating a custom polymer wedge with a radius that matched the airframe curvature, and I switched to a dual-element transducer set at an angle that kept the near-surface dead zone outside the region of interest. Cost me about two days of setup time, but after that the inspection ran clean. If you skip the setup phase and just start firing, you will spend the rest of your shift chasing ghosts. Radiography remains relevant in Seattle, though it is declining in production environments. Digital radiography has replaced film almost entirely. The shift happened around 2018 when flat-panel detectors became affordable enough for shop floor use. Image quality is consistent, there is no chemical processing variability, and exposure times dropped significantly. But digital radiography has its own trap. The dynamic range of a flat panel is different from film. You can capture more detail in thick sections, but the system will also show you every benign indication — grain boundaries, inclusions that are well within acceptance criteria — that a trained inspector would normally filter out. Newer technicians tend to over-call defects on digital radiography because they have not yet developed the visual discrimination that comes from years of reading film. I always tell people to go back and look at known-good reference images before making a rejection call on anything borderline. Magnetic particle and dye penetrant are still widely used, mostly for final surface inspection after machining or repair. The limitation nobody likes to admit is that both methods are entirely surface-sensitive. If a crack extends subsurface even by a millimeter, neither method will find it unless the open tip reaches the surface. I once inspected a turbine blade for a contract that had failed in service. The original supplier had passed it with MPI. We found a cluster of sub-surface laminations using ultrasonic testing that MPI had completely missed. The blade was scrapped. That is the kind of story that makes procurement teams take UT seriously.
For anyone looking to get started in Seattle NDT, the practical path is ASNT Level II certification in your chosen method. The theory exam is straightforward. The hands-on practical is where people struggle, especially if you are studying from generic material and have never touched the equipment. Take every hands-on lab seriously. Calibrate your equipment correctly. Learn to read the difference between a legitimate signal and a geometric artifact. In phased array, a change in amplitude at a specific depth could mean a crack, a lack of fusion, or it could mean the sound wave just passed through a region of different acoustic impedance due to a weld microstructure variation. Context matters more than the raw signal. The current trend in the Seattle market is toward automated inspection systems and data analytics integration. Some shops are now feeding phased array and radiography data into machine learning models that flag potential defects automatically. The results are promising but far from ready for standalone certification decisions. Right now, an automated system can serve as a screening tool, reducing the volume of inspections a certified Level III needs to review. It cannot replace the engineer who has to sign off on the result. I have seen three separate projects where the AI flagged a benign geometric indication as a rejection, and each time the Level III inspector overrode it after examining the raw data. The technology is improving, but it is not at the point where you should trust it unconditionally. If you want hands-on training resources, the Aviation Supply Center in Seattle maintains publicly available NDT procedure documents for commercial aerospace applications. The FAA also publishes advisory circulars on NDT acceptance criteria that are freely downloadable. For hands-on practice, the NDT Technician Training Center near Tacoma offers Level I and II courses in UT, MT, PT, and RT. Tuition runs roughly four to six thousand dollars per level depending on the method. The certification exam through ASNT costs around two hundred dollars.
Get the Full Details

One more practical note about working in this area. The weather here affects field inspections. Ultrasound requires couplant, and at five degrees Fahrenheit with wind chill, the couplant freezes on the part before you can complete a scan. I learned to keep a heated enclosure around the inspection area and to use low-temperature couplant formulations when working outdoors in winter. Radiography is less affected by temperature but wind can be an issue if you are using gamma sources in an open yard. Seal the area. Secure the source. Check your dosimeters. These are the things that matter when you are actually on site, not the ones that make it into the training manuals.