Ammonia Basics
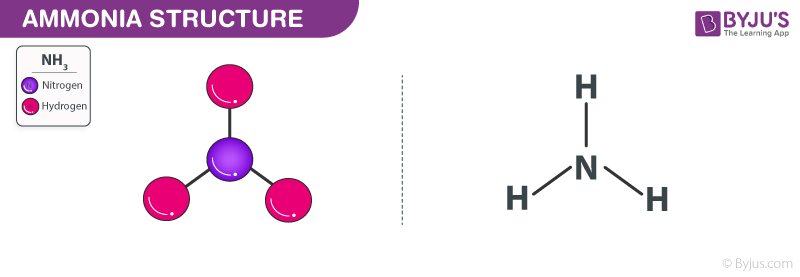
NH3 is a simple molecule with a triangular pyramidal shape. One nitrogen atom bonded to three hydrogen atoms, one lone pair sitting on top. The H-N-H bond angle is about 107 degrees. It's a gas at room temperature and pressure, but it liquefies at roughly -33 degrees Celsius or under moderate pressure. That property is exactly why it moved around so easily in industrial settings before modern refrigeration existed. The chemical identity part is straightforward. It's a weak base. It accepts a proton to become ammonium, NH4+. That acidity behavior matters in every application, from fertilizer to scrubbing systems. The industrial footprint is where things get complicated. Global ammonia production runs about 180 million metric tons per year, and nearly all of it uses the Haber-Bosch process. Hydrogen comes from steam methane reforming, usually. Nitrogen comes from the air. High pressure, iron-based catalyst, temperatures around 400 to 500 degrees Celsius. The process consumes roughly 28 to 35 gigajoules per ton of ammonia produced, depending on plant efficiency and whether you're using older or newer technology. I worked on a retrofit at a mid-sized fertilizer plant back in 2019. We were trying to trim CO2 emissions from the reformer furnace without touching the downstream shift converters. The problem was that the existing waste heat recovery train was already optimized for the old feedstock composition. When we switched to a slightly higher natural gas quality stream to reduce sulfur poisoning on the catalyst, the furnace outlet temperature climbed about 40 degrees Celsius faster than the heat exchangers could handle. Standard procedure would have been to add another air preheater stage, which meant a three-month shutdown. Instead, we rerouted the high-pressure feedwater through the existing economizer loop in parallel with a bypass, effectively creating a temporary two-stage preheat. It wasn't pretty. The control valves had to be manually tweaked during transitions, and operators complained about the instability. But it kept the plant running at 85 percent capacity for fourteen months while we ordered and installed the proper heat exchange section. That workaround saved us roughly 2.1 million dollars in lost production.
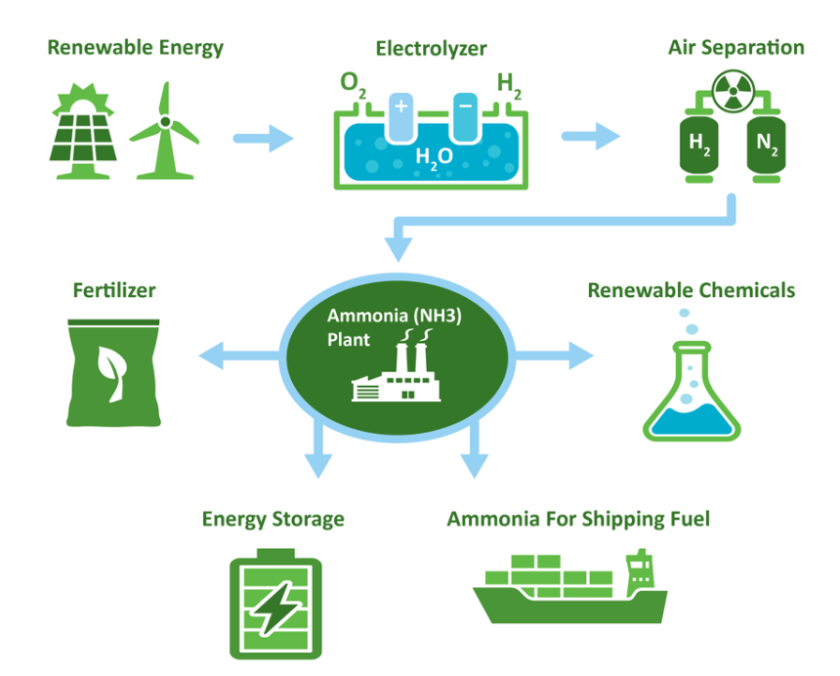
The environmental side isn't simple either. Ammonia production accounts for about 1.8 percent of global energy-related CO2 emissions. That's not a small number. The hydrogen in ammonia has to come from somewhere, and currently that somewhere is almost always fossil fuel. There are methods to make green ammonia using electrolysis and air separation, but the electricity cost alone pushes the production price above 800 dollars per ton compared to roughly 300 to 400 dollars per ton for conventional production. The economics haven't worked except in places with severely constrained natural gas access or subsidized renewable energy. Here's something most people don't consider. The real environmental damage from ammonia isn't always the production phase. It's the application and runoff. When you spread urea-ammonium nitrate solutions on fields, a portion converts to ammonia gas and volatilizes into the atmosphere. That's a direct loss of nitrogen and a source of particulate formation. In some corn Belt operations, volatilization losses run 10 to 20 percent of applied nitrogen unless you use nitrification inhibitors or incorporate the product into the soil within six hours. That's a practical detail that matters more than the production emissions if you're doing a full lifecycle assessment. There's also the issue of ammonia as a refrigerant. It's excellent. High latent heat of vaporization, cheap, zero ozone depletion, zero global warming potential. But it's toxic at concentrations above 300 parts per million and flammable between 15 and 28 percent in air. I've seen facilities treat ammonia leakage as a secondary concern because the old compression units rarely exceeded 50 kilograms of charge. Modern large-scale cold storage warehouses routinely carry over 2,000 kilograms. When a gasket fails at 3,000 pounds per square inch in a confined space, the evacuation radius is measured in hundreds of meters, not feet. Several plants in the Great Lakes region have been required to install ammonia detection grids linked to automatic nitrogen purging after incidents in the mid-2020s. The detection systems cost between 150,000 and 400,000 dollars depending on facility size, and they reduce allowable charge sizes by about 30 percent in many jurisdictions.
The scrubbing technology for removing excess ammonia from industrial off-gases is fairly mature. Wet scrubbers using sulfuric acid produce ammonium sulfate, which can be sold as a fertilizer. Dry scrubbers with acidic media are cheaper upfront but require more frequent media replacement. The tradeoff is usually water consumption. A wet scrubber handling a typical 50,000 cubic meter per hour gas stream at 500 ppm ammonia will consume roughly 12 to 15 cubic meters of water per hour. In drought-prone areas, that's a real operational constraint. Some facilities have switched to closed-loop scrubbing with crystallization, but those systems add complexity and maintenance costs that aren't justified unless you're dealing with high ammonia concentrations above 1,000 ppm. Ammonia's role as a potential hydrogen carrier is getting a lot of attention. You can crack it back to nitrogen and hydrogen at about 500 to 600 degrees Celsius with a catalyst. The conversion rate is decent, roughly 95 to 98 percent per pass. But the energy penalty for cracking is significant. You're burning fuel or using electric resistance heating just to break the N-H bonds that you spent energy creating in the first place. The round-trip efficiency from electricity to ammonia to hydrogen lands around 40 to 45 percent. That's worse than compressed hydrogen storage at equivalent scales and much worse than liquid organic hydrogen carriers for long-duration storage. The advantage of ammonia is purely in shipping density and existing infrastructure compatibility. It can move through modified natural gas pipelines at up to 20 percent blend ratios without material compatibility issues. At higher concentrations, you need new pipeline material because ammonia accelerates stress corrosion cracking in standard steel grades. If you're evaluating ammonia for any application, the first question should be whether you actually need it. A lot of processes that specify ammonia are just following tradition. Sodium hydroxide handles pH adjustment cheaper in many cases. Urea is safer to transport and store. CO2 injection into irrigation water achieves similar bicarbonate buffering without the ammonia risk. The chemistry is clear. The decision is usually economic and institutional, not technical.
Get the Full Details

The environmental balancing act comes down to this. Ammonia enables food production at civilization scale. Without it, global crop yields would drop by an estimated 40 to 50 percent. That's the industrial footprint you can't replace yet. But the production method is locked into fossil carbon unless you accept price increases that current markets won't absorb. The practical path forward involves incremental efficiency improvements in existing plants, wider adoption of nitrification inhibitors to cut agricultural emissions, and targeted investment in green ammonia for applications where the hydrogen purity requirements justify the cost. There's no single solution. The technology exists. The economics are the bottleneck.