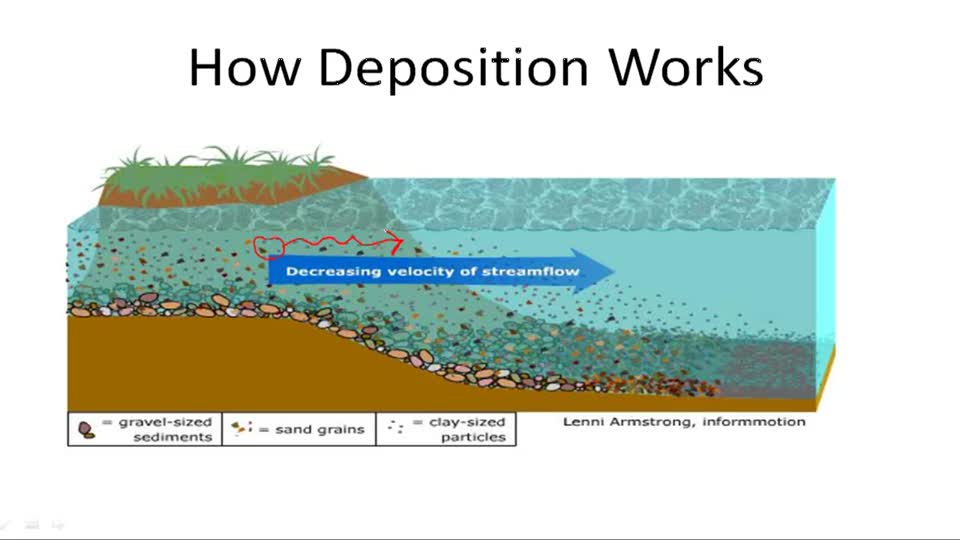
How Deposition Actually Works When You're Staring at a Failed Coating Run
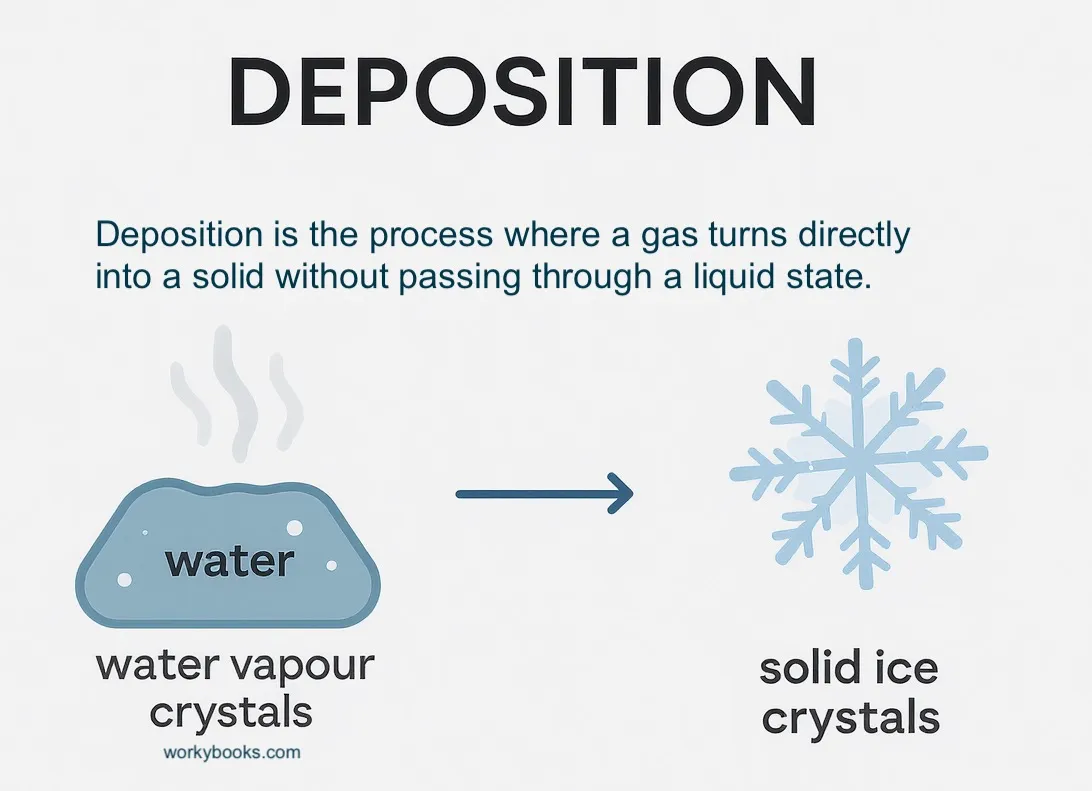
I spent about three hours last November troubleshooting why a batch of sputtered aluminum films kept delaminating from silicon wafers. The deposition parameters looked right on paper. Temperature was stable, chamber pressure sat at 3 milliTorr, and the power settings matched our recipe. Turns out the real issue was a 40-second pump-down delay that let the chamber reabsorb trace moisture from the walls. The fix was a simple bake-out cycle and a tighter process window for rough-in time before ignition. That's the kind of thing nobody tells you about deposition until it breaks something expensive. Deposition in science refers to the process where a substance transitions from a gaseous phase directly into a solid phase, bypassing the liquid state entirely. This is the same mechanism behind frost forming on a cold windowpane in winter. The water vapor in the air deposits straight onto the glass as ice crystals without ever becoming liquid water first. In laboratory and industrial settings, scientists and engineers manipulate this phase transition deliberately to build thin films, coat materials, and fabricate everything from solar cells to microchip components.
What Is Deposition In Science The Silent Process Shaping Our World
There are two fundamentally different mechanisms at play here, and confusing them will get you wrong results every time. Physical vapor deposition, or PVD, involves taking a solid material and turning it into vapor through physical means like heating or bombarding it with ions, then letting that vapor condense back onto a substrate. Chemical vapor deposition, or CVD, is entirely different. You introduce precursor gases into a chamber where they undergo chemical reactions on a heated substrate surface, and the solid product deposits while the gaseous byproducts get pumped away. The choice between PVD and CVD depends on what you need the film to do. PVD coatings like titanium nitride on cutting tools are hard and wear-resistant but relatively thin, usually under 5 micrometers. CVD processes can deposit thicker layers and cover more complex geometries because the reactive gases flow into crevices and react everywhere simultaneously. The trade-off is that CVD typically requires much higher temperatures, sometimes exceeding 1000 degrees Celsius, which rules out temperature-sensitive substrates like certain polymers or already-fabricated semiconductor devices. I once tried running an atomic layer deposition process, which is a subset of CVD, on textured silicon structures meant for solar cell passivation. The concept sounded perfect because ALD gives you Angstrom-level control over film thickness. What I didn't account for was the aspect ratio of the features I was coating. The precursor gases couldn't diffuse deep enough into the narrow trenches before reacting at the entrance, so the films were thick on top and practically nonexistent at the bottom. The workaround was lowering the precursor pulse pressure and extending the exposure time by a factor of five, which let the molecules seep in gradually rather than reacting immediately at the surface. It made the process slower but finally gave uniform coverage throughout the structure.
One counter-intuitive fact about deposition that trips people up is that higher temperatures don't always produce better films. In PVD sputtering especially, raising the substrate temperature can increase adatom mobility on the surface, which does improve crystallinity up to a point. But push it too far and you start getting island growth again, known as Volmer-Weber mode, where atoms cluster into three-dimensional mounds instead of spreading into flat layers. This creates a rough, porous film that flakes off under thermal cycling. The sweet spot is usually somewhere between 0.3 and 0.5 of the material's melting point in Kelvin, measured as a fraction of the absolute melting temperature of the depositing substance. Another thing beginners miss is the importance of substrate preparation. I have seen good deposition runs ruined by fingerprints left on wafers during handling. A single fingerprint introduces carbon contamination and creates nucleation sites that disrupt film growth, leading to pinholes and uneven thickness. The standard procedure is ultrasonic cleaning in acetone, then isopropanol, then a nitrogen blow-dry, followed by immediate placement into the deposition chamber. If you cannot load into the chamber right away, storing cleaned substrates in a desiccator prevents ambient moisture from recontaminating the surface. The real limitation of most deposition techniques is step coverage on patterned surfaces. Line-of-sight methods like thermal evaporation and standard sputtering cannot coat the sides of tall features uniformly because the vapor or sputtered atoms travel in straight lines from the source. You get a shadowing effect where the tops of structures receive heavy deposition while the undersides and trenches get very little. For advanced semiconductor manufacturing, this is solved by using rotational substrate holders, multi-angle deposition, or transitioning to plasma-enhanced CVD where ion-assisted deposition helps drive material into recessed areas.
Get the Full Details

Deposition rates also vary wildly depending on the method and equipment. Thermal evaporation can run anywhere from 0.1 to 10 nanometers per second. Reactive sputtering typically sits in the 0.01 to 1 nanometer per second range. Atomic layer deposition is deliberately slow, often just 0.001 to 0.01 nanometers per cycle, because each cycle deposits only a single molecular layer before the process has to flush and repeat. If you need a 100-nanometer ALD film at 0.005 nanometers per cycle, you are looking at 20,000 cycles, which at roughly 10 seconds per cycle means about 55 minutes of pure deposition time not counting pump-down and venting. For anyone setting up a basic deposition system, the most common mistake is assuming that base pressure equals process pressure. Your vacuum gauge might read 10^-6 Torr during pumping, which looks excellent, but once you introduce argon for sputtering or start heating the substrate, the partial pressures of residual gases shift dramatically. Water vapor, hydrogen, and hydrocarbons desorb from chamber walls when heated, spiking the total pressure and contaminating your film. Running the system with the substrate heater on for at least 30 minutes before starting any deposition, a process called bake-out, reduces this outgassing significantly. I usually verify success by watching the pressure stabilize for 10 minutes after ignition before trusting my readings. There are scenarios where deposition simply cannot deliver what you need. If you require thick bulk materials rather than thin films, PVD and CVD are the wrong tools and you should be looking at casting, sintering, or additive manufacturing instead. Deposition excels at films ranging from a few Angstroms to maybe 50 micrometers under special conditions, but beyond that the stress in the film becomes a serious problem and adhesion deteriorates. Internal stress in deposited films is another persistent issue. Compressive stress can cause buckling and delamination, while tensile stress leads to cracking. Managing this requires tuning background gas pressure, substrate temperature, and deposition rate in concert, and there is no universal setting that works across all material combinations.
Environmental deposition outside the lab, like the accumulation of particulate matter on solar panels or the formation of scale inside industrial pipes, follows the same fundamental phase-change principles but operates on completely different timescales and scales. Understanding the laboratory mechanisms gives you a baseline for predicting how these natural and industrial processes behave, even when the conditions are far less controlled.