
What orifices actually do
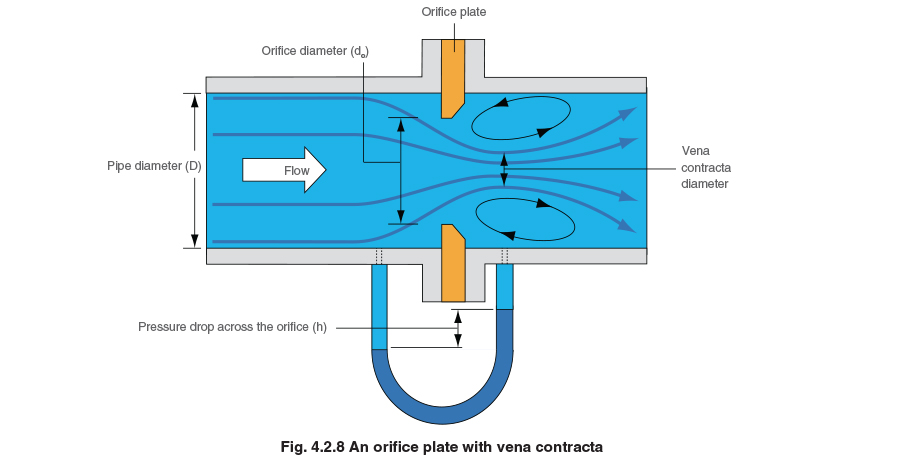
An orifice is simply a hole in a plate, pipe, or wall that constrains fluid passage. It is not a component you typically design from scratch. More often, you pick one that fits your Reynolds number range, your allowable pressure drop, and the tolerance of your downstream equipment. The physics is straightforward—Bernoulli plus a discharge coefficient—but getting the details right is where people make mistakes. In practice, the orifice acts as a flow restriction that creates a measurable pressure differential. That differential becomes the signal you use to infer flow rate. The governing equation is the standard orifice flow equation, but the real work happens in the assumptions you make before you even plug numbers into it. Start with the maximum and minimum flow rates you expect. I usually work from a baseline of 10 to 100 percent of design capacity. Anything outside that window makes the orifice a poor meter. Next, pick your beta ratio—the ratio of orifice diameter to pipe inner diameter. A beta between 0.3 and 0.7 keeps most of the standards happy. Going below 0.3 gives you enormous pressure loss for little gain. Going above 0.7 and your differential pressure becomes so small that any sensor noise swamps the reading.
Calculate the expected differential pressure at maximum flow. Most installations aim for a differential in the range of 25 to 80 percent of the transmitter's full scale at max flow. If your calculated differential is 5 percent of range, go back and reduce the beta. If it is 120 percent, go the other direction. This step alone prevents about half the field problems I see. Then check the Reynolds number at your minimum expected flow. Below a certain Re threshold, the discharge coefficient becomes unstable and the meter loses accuracy. For standard orifice plates per ISO 5167, you generally want a Reynolds number above 10,000 in the pipe. If your application runs at low flow or with a viscous fluid, an orifice plate may not be the right choice at all.
The part nobody talks about: installation effects
An orifice plate is only as good as the piping upstream of it. The standards specify straight-run requirements—typically 10 to 30 diameters depending on what fittings exist upstream. A double elbow in the same plane can throw off your reading by 3 to 5 percent even if everything else is perfect. I learned this the hard way on a glycol circulation loop where the manufacturer's calibration was off by nearly 7 percent because someone installed a reduced-size adapter plate upstream that acted like a partial orifice itself. The workaround was not to replace the orifice. It was to add a flow conditioner—a honeycomb or plate-type straightener—about 5 diameters upstream and then recalibrate the beta calculation to account for the modified velocity profile. The corrected readings matched a portable ultrasonic clamp-on within 1.2 percent. Without the conditioner, we were flying blind.
Get the Full Details

Discharge coefficient nuances
The discharge coefficient Cd is not a constant. It varies with Reynolds number, beta ratio, tap location, and even pipe roughness. The classic Equation 3 from ISO 5167-2 gives you a starting point, but the Folsom and Reader-Hunt correlations handle different tap configurations more accurately at low Reynolds numbers. If you are working with compressed gas or steam, you also need the expansibility factor epsilon. For liquids, epsilon is essentially 1. For gases, ignoring it can introduce errors of 4 to 8 percent depending on the pressure ratio across the orifice. A common pitfall is using a generic Cd of 0.61 for everything. That value is reasonable for water at moderate Reynolds numbers with flange taps, but it drifts significantly outside that window. At Re below 5,000, Cd can drop toward 0.58. At very high Reynolds numbers with corner taps, it may climb toward 0.62. The difference matters when you are billing for custody transfer.
Pitfalls that show up in the field
Erosion is the quiet killer. If your fluid carries solids—sand in a production line, catalyst fines in a reactor feed, particulate in a slurry—the orifice edge will wear. A sharp-edged orifice is part of the calibration assumption. Once that edge rounds, the discharge coefficient shifts and your flow reading slowly creeps high. I have seen plates in service for 18 months with erosion that reduced the effective beta by 0.02 and went entirely unnoticed because nobody re-checked the pressure drop against the expected curve. Condensation in gas service is another one. If you are measuring wet natural gas and the orifice plate temperature drops below dew point, liquid forms on the downstream face. That changes the effective flow area and introduces slug-like behavior in the differential pressure signal. The fix is usually trace heating on the tap lines and making sure the transmitter is vented properly. A clogged impulse line reads as a stuck differential, which looks like a flat-line flow problem until someone checks the bleeding valves.
When an orifice is the wrong call
Orifice plates have real limitations. They produce permanent pressure loss equal to roughly 40 to 70 percent of the differential pressure you measure. In high-pressure gas systems where every kilopascal of loss translates to compression cost, that adds up fast. A Venturi tube or an aerodynamic flow nozzle will give you similar accuracy with a fraction of the permanent loss—maybe 10 to 20 percent recovery instead. If your operating margin is thin, the orifice is cheap upfront but expensive over time. They are also sensitive to upstream disturbance and not ideal for dirty fluids. A V-cone meter or a magnetic flowmeter handles slurry and two-phase flow far better. For low-flow applications below 10,000 Reynolds, a Pitot tube array or a thermal mass meter may serve you better. The orifice is not a bad choice, but it is a narrow one. Use it where it fits, not where it is convenient.
A quick practical checklist
Before ordering an orifice plate, verify these things. Know your fluid properties at operating temperature and pressure. Confirm your pipe inner diameter has been measured, not assumed from nominal size—Schedule 40 steel is not a precise dimension. Check your straight-run lengths against the manufacturer's requirements. Select your tap type and locate it correctly. Decide on your transmitter range and make sure the expected differential covers at least 20 percent of the span at minimum flow. Finally, document the beta ratio, the Reynolds number at design flow, and the calculated Cd. When something goes wrong two years later, that documentation is the only thing that will save you from guessing. I keep a spreadsheet for every orifice installation that tracks the as-installed beta, the original Reynolds number, the expected differential at five flow points, and the actual readings from the first commissioning run. It sounds excessive. It saves hours when you are troubleshooting a drift problem in year three and nobody remembers what the original calibration looked like.


