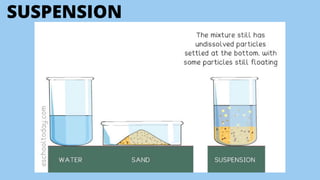
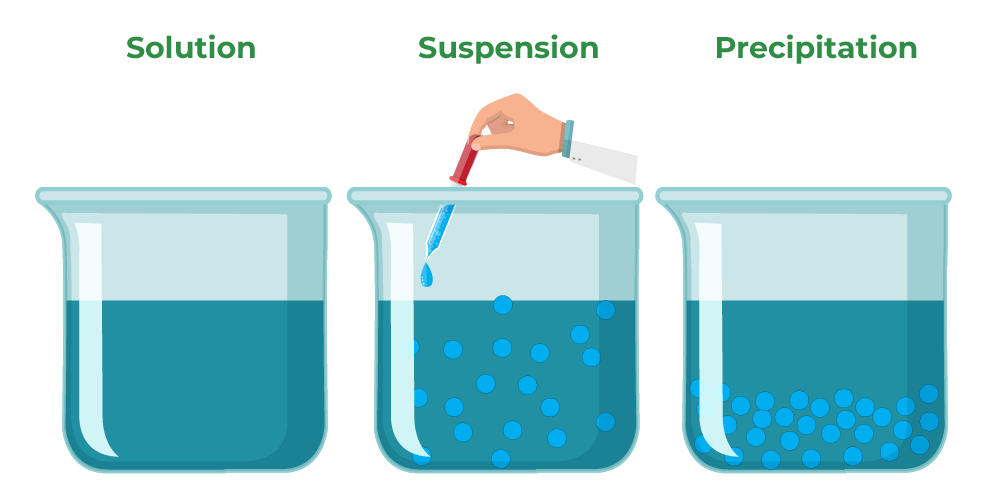
What Actually Makes A Suspension A Suspension
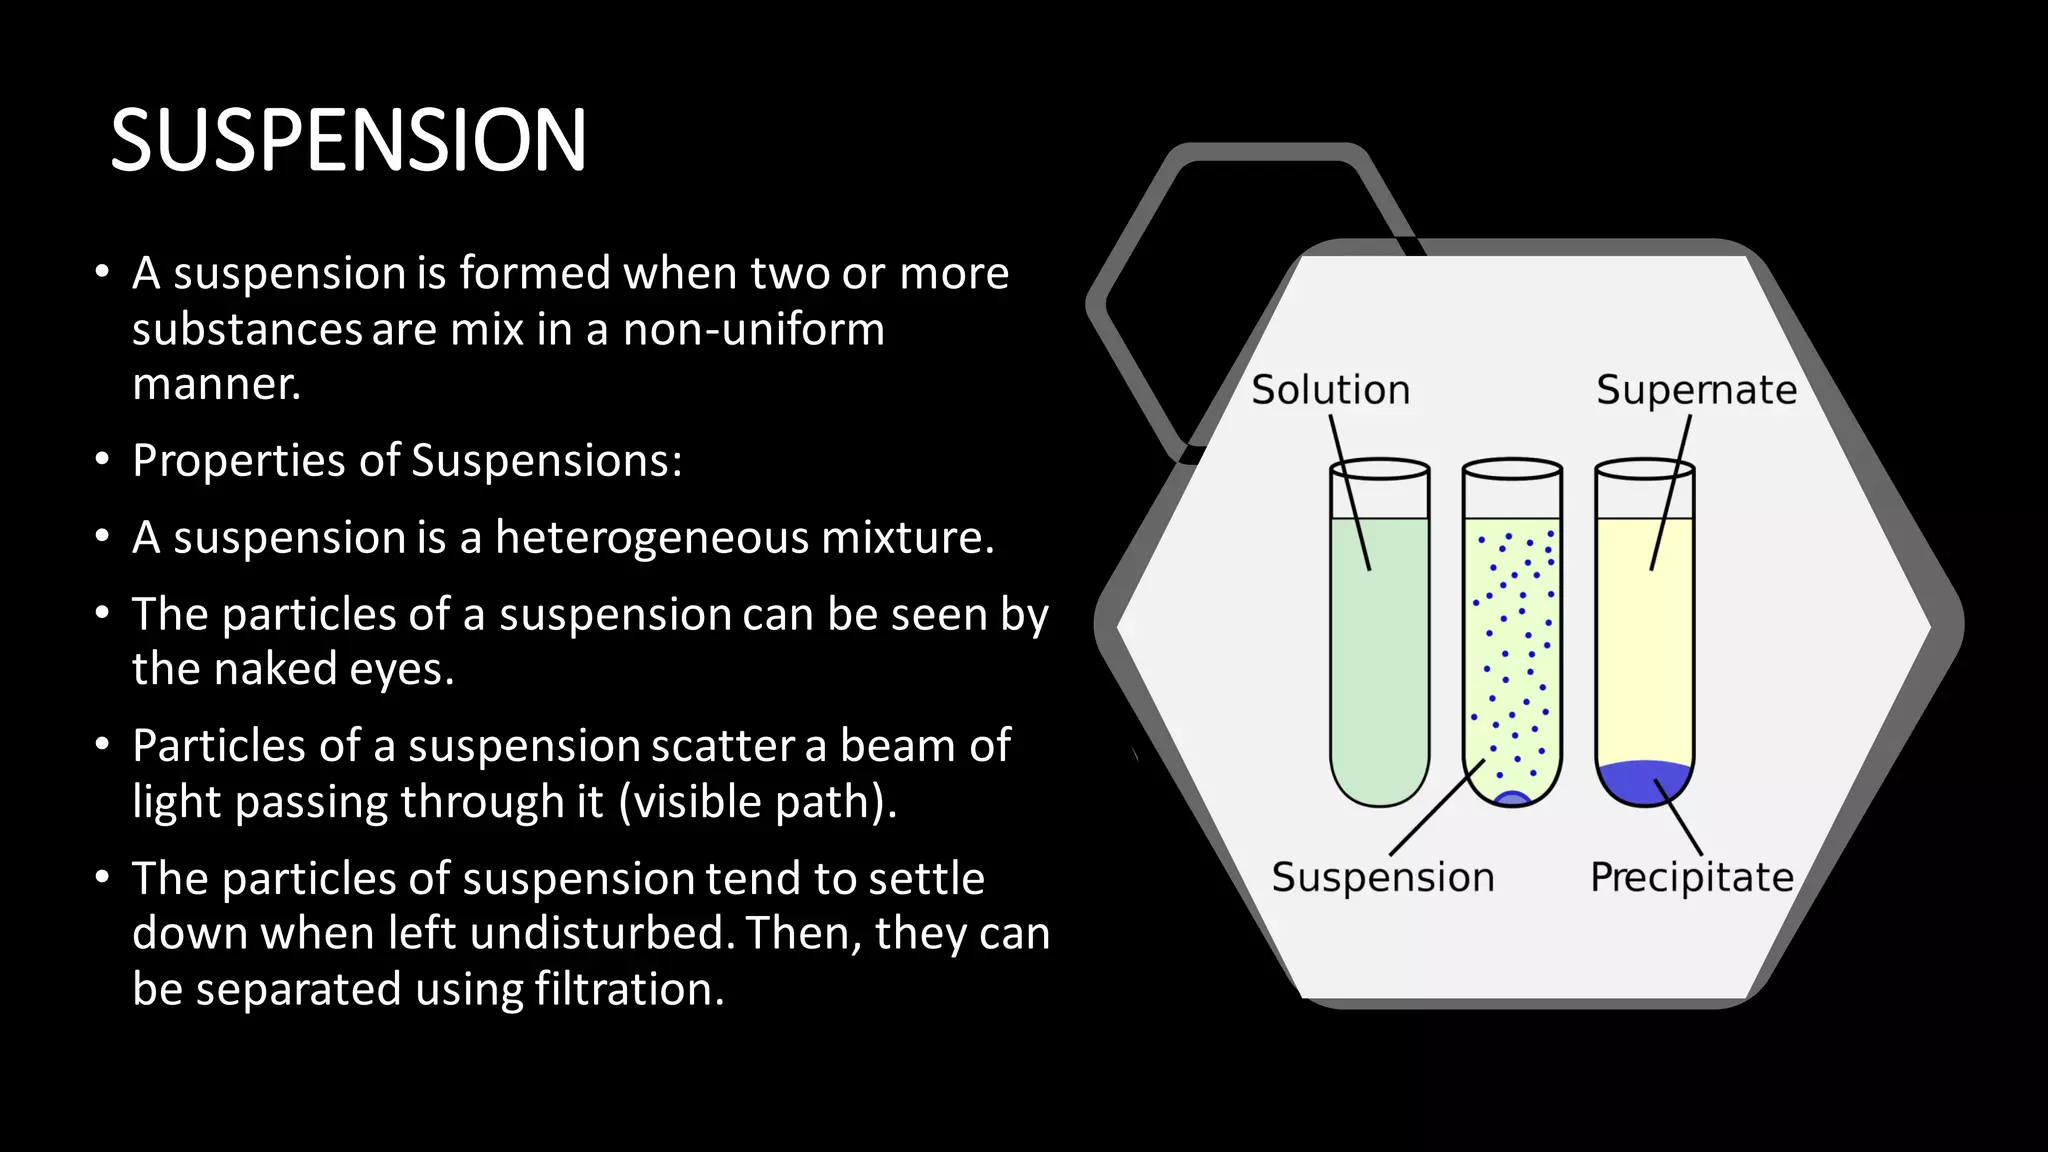
A chemical suspension is a heterogeneous mixture where solid particles are dispersed throughout a liquid medium but do not dissolve. The particles are large enough—typically over 500 nanometers—that they will eventually settle under gravity if left undisturbed. This distinguishes them from solutions, where the solute integrates at the molecular level, and from colloids, where particles remain suspended much longer due to Brownian motion and smaller size. I used to confuse the boundary between colloidal dispersions and true suspensions when I was still running routine preparations in a university lab. The practical difference comes down to settling behavior and light scattering. A suspension will throw a visible precipitate within minutes to hours depending on particle density and viscosity. A colloid like milk or gold sol stays distributed for months without separation.
What Is A Chemical Suspension Unpacking The Science Behind These Common Mixtures
The science behind suspensions revolves around three forces fighting each other constantly. Gravity pulls particles downward. Brownian motion from the solvent molecules pushes them back upward. Interparticle forces—van der Waals attraction, electrostatic repulsion, steric hindrance—determine whether particles clump together or stay separate. The Stokes equation describes settling velocity: v equals 2r squared times the difference in density between particle and fluid, divided by 9 times the fluid viscosity. This means doubling the particle radius quadruples how fast it falls. Doubling viscosity halves it. The practical takeaway is that particle size control matters far more than people expect when formulating stable suspensions. I ran into a specific problem once preparing a zinc oxide suspension in an aqueous formulation. The batch settled into a rock-hard cake at the bottom of the vessel within forty minutes, and no amount of shaking brought it back into a uniform dispersion. The root cause was that the ZnO particles had a narrow size distribution centered around 2 micrometers, which happens to be the worst possible range for stability. Particles in that window settle quickly enough to compact densely but are small enough that Brownian motion cannot effectively resuspend them.
The workaround was straightforward once I identified the issue. I milled a portion of the batch down to below 200 nanometers and blended it back with the coarser fraction. The bimodal size distribution prevented tight packing during settling, and the finer particles stayed in suspension long enough to keep the whole mixture usable for several hours. It is a standard trick in pigment dispersion and pharmaceutical formulation, but it is not obvious unless you have watched a hundred batches fail the same way.
Get the Full Details

How To Make A Stable Suspension In Practice
Stability in suspensions is always relative. Nothing stays suspended forever. The goal is extending the usable window to whatever your application requires. The first lever is particle size reduction. Ball milling, jet milling, or high-shear homogenization can bring particle diameters into ranges where settling is slow and resuspension is easier. Grind them fine enough and you transition into the colloidal regime, where the behavior changes fundamentally. The second lever is viscosity modification. Adding thickeners like xanthan gum, cellulose derivatives, or synthetic thickeners increases the continuous phase resistance to particle movement. A formulation at 500 centipoise will settle roughly four times slower than one at 125 centipoise, all else being equal.
The third lever is surface chemistry. Wetting agents and dispersants adsorb onto particle surfaces and create either electrostatic repulsion through charged groups or steric repulsion through long polymer chains. Without proper dispersion, even nanometer-scale particles will flocculate and settle rapidly. I spent two days troubleshooting a titanium dioxide suspension where the problem was not settling speed but flocculation. The primary particles were fine, but they were aggregating into loose clusters that behaved like coarse particles and sank fast. Switching from a nonionic surfactant to a phosphate-based dispersant at 2 percent by weight of pigment fixed it. The difference in shelf stability went from hours to weeks.
Common Pitfalls And Where Suspensions Fail Completely
Suspensions fail in predictable ways, and most failures come from ignoring one variable while optimizing another. Ostwald ripening is a silent failure mode. Smaller particles dissolve while larger ones grow, shifting the size distribution over time even in a sealed container. This is especially problematic with poorly soluble compounds in the sub-micron range. If you see your suspension gradually getting coarser and more sediment-prone after weeks, this is likely what happened. Temperature control and selecting an appropriate solvent system are the main mitigations. Caking is the other major problem. When particles settle into a dense, consolidated layer that does not redisperse by shaking, the formulation is essentially dead. This happens when interparticle attractive forces overcome repulsive forces during compaction. Flocculated suspensions are far less prone to caking than deflocculated ones, which is counterintuitive. Loose flocs trap liquid within the network and remain pourable. Tight deflocculated packs compress into a hard mass. Pharmaceutical manufacturers sometimes intentionally flocculate suspensions to avoid caking, accepting a slightly grainier texture in exchange for reispersibility.
There are also cases where suspensions simply cannot work. If your active compound has a density very close to the carrier fluid, settling becomes negligibly slow but resuspension becomes equally difficult because there is no gravitational driving force to help particles separate from the surface they rest on. In those situations you are better off pursuing an emulsion, a solid dispersion in a polymer matrix, or a true solution if the chemistry allows it.
Real-World Applications
Suspensions are everywhere in industry despite their inherent instability. Paint and coatings rely on pigment suspensions. The pigments must stay dispersed during storage, flow properly during application, and then form a coherent film. Antibiotic suspensions for pediatric oral use are another classic example. The drug is practically insoluble in water, so it is suspended in a flavored vehicle with controlled viscosity and proper dispersants. The dose must be uniform throughout the bottle, which means the suspension has to remain stable enough that a patient can shake it, measure it, and get the correct amount every time. Agrochemical formulations like wettable powders and suspension concentrates work on the same principle. The active ingredient is milled to a specific size range, suspended in water with surfactants and thickeners, and packaged for dilution at point of use. Particle size here directly affects both efficacy and phytotoxicity. Too coarse and coverage is poor. Too fine and you risk leaf burn or rapid sedimentation during storage. Understanding what makes a suspension stable enough for its intended use case is more useful than chasing perfect stability, which does not exist. The tradeoffs between particle size, viscosity, dispersant type, and shelf life are the actual work of formulation.