Manufactured goods are just things that someone transformed from raw materials into something else. Here is what nobody tells you about the process.
Most people think manufacturing is a linear thing. You get raw materials, you put them in a machine, and you get a finished product. That is the textbook version. The real version involves a lot more moving parts than most people realize. I have spent years working around supply chains and production floors, and honestly, it is more about managing friction than it is about any elegant process. At its core, manufacturing converts raw inputs into finished outputs through some combination of mechanical, chemical, or manual processes. That sounds almost too simple. The inputs can be things like steel, plastic pellets, textiles, or even food ingredients. The output is whatever you were trying to make in the first place. But the gap between input and output is where everything falls apart if you do not pay attention. There are different types of manufacturing depending on what you are building. Discrete manufacturing covers things like cars, appliances, and electronics where each unit is individually identifiable. Process manufacturing covers things like chemicals, food, and pharmaceuticals where you deal with batches and formulas rather than individual items. The distinction matters more than you would think when you are actually running a production line.
I remember dealing with a supplier who had switched from discrete to process manufacturing without really understanding the implications. They were ordering raw materials the same way they used to, which meant their inventory tracking was completely wrong. Their yield calculations were off by about eighteen percent because they were applying discrete logic to a batch process. The fix was straightforward once we caught it, but it cost them nearly three weeks of disrupted production before we figured out what was going on. They had to reconfigure their bill of materials and update their ERP settings to account for the batch-based nature of their new process. That kind of mistake is expensive in ways that are not always immediately obvious.
The actual process is messier than diagrams suggest
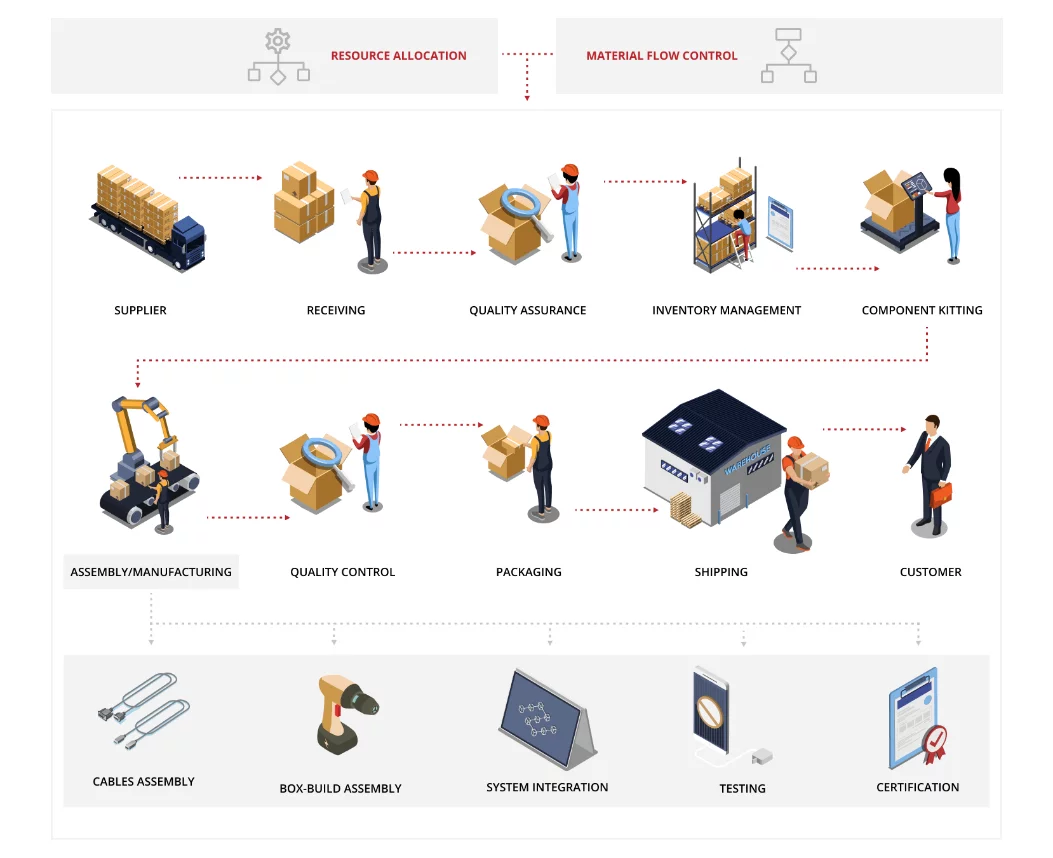
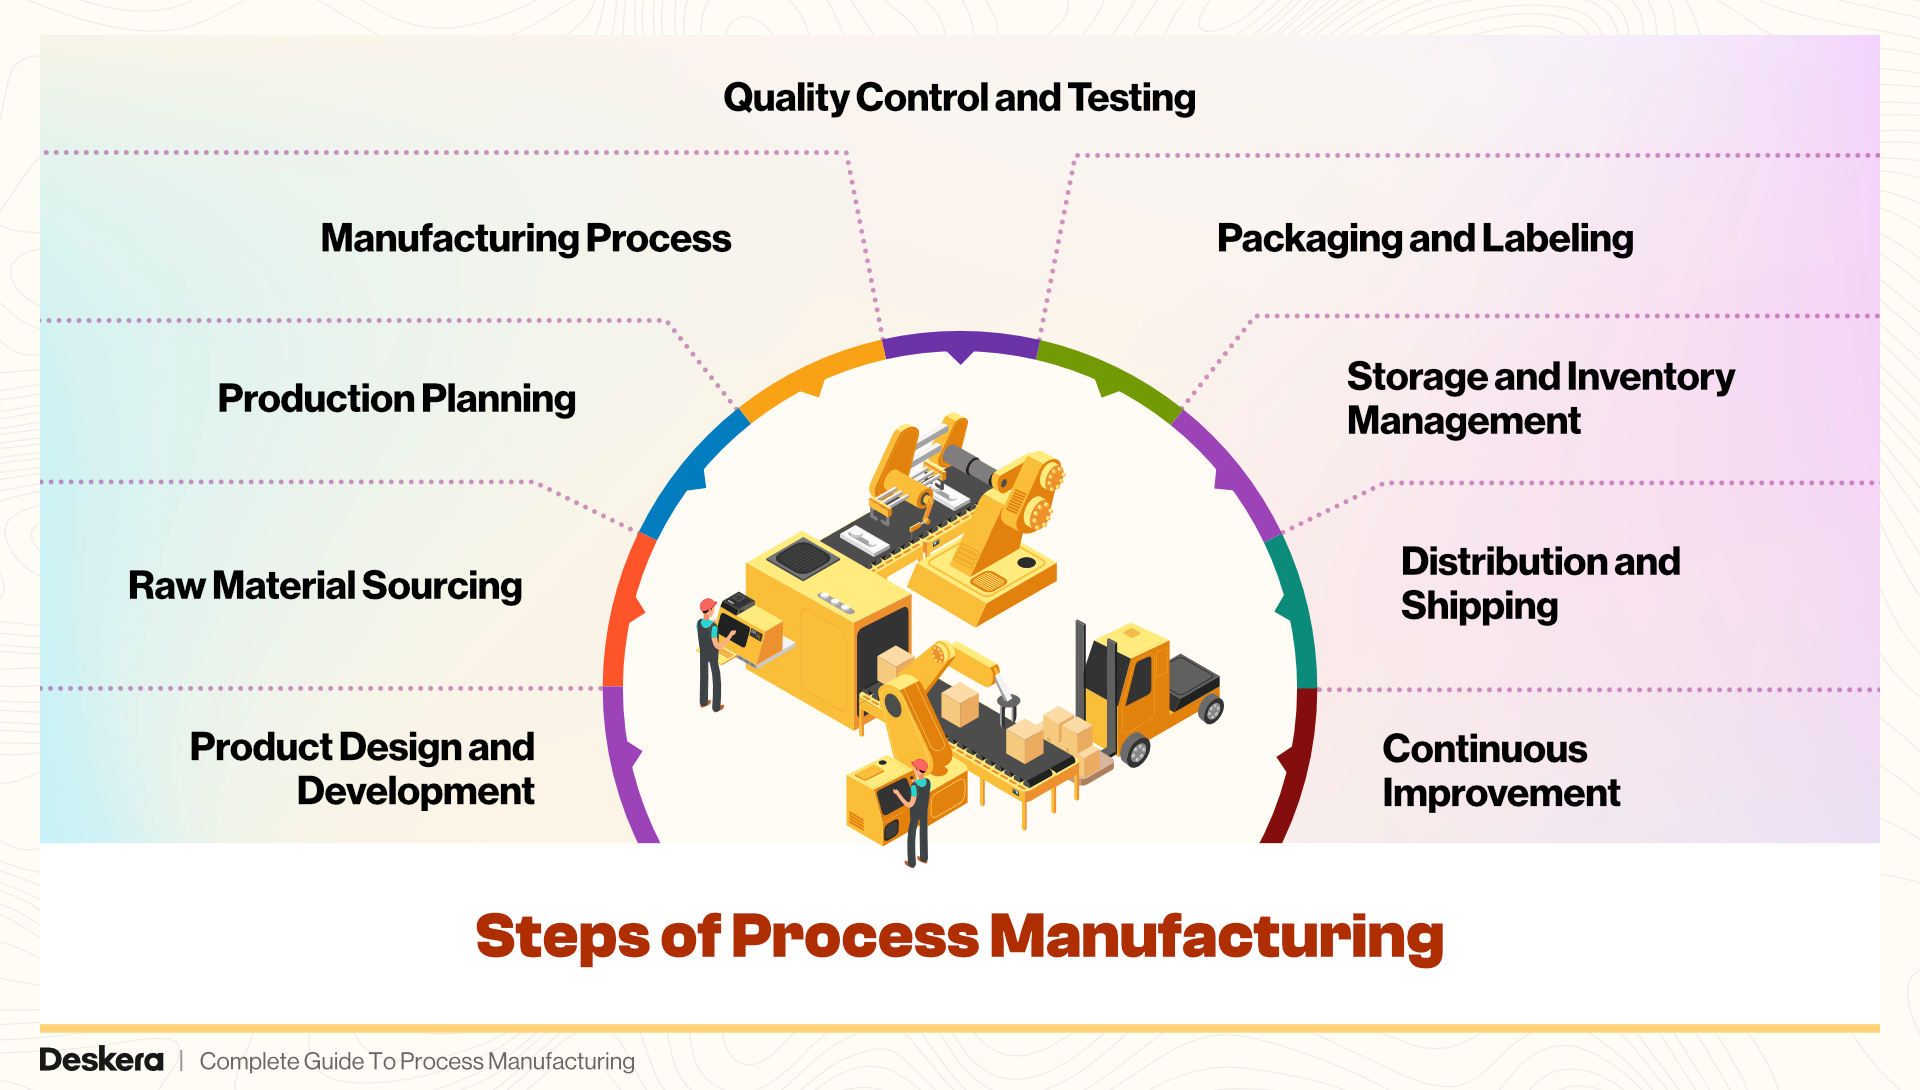
A typical manufacturing workflow starts with design and engineering, moves through procurement, then production, quality control, and finally distribution. Each step has its own failure modes. The design phase might produce something that looks great on paper but is impossible to manufacture at scale. Procurement can derail everything if a key material is delayed. Production itself has variability built into it. Quality control either catches problems early or admits it is too late. One thing that trips up a lot of people is the assumption that quality control comes at the end. It does not have to. In fact, integrating quality checks throughout the process rather than leaving everything for final inspection tends to save a lot of trouble. I have seen operations cut their defect rate roughly in half just by adding in-process checks instead of relying on final inspection alone. The tradeoff is that you need more personnel or better automation at intermediate stages, but the math usually works out in your favor. Supply chain management is another area where people underestimate the complexity. You are not just ordering parts from a supplier. You are dealing with lead times, minimum order quantities, currency fluctuations, and the occasional situation where a factory in another continent shuts down for a week because of a weather event or a labor dispute. Having a single source for any critical component is a real vulnerability. I learned that the hard way when a sole supplier for a specialty valve went offline for two months due to a fire. We lost about forty thousand dollars in missed shipments before we could qualify a backup vendor. The whole incident took roughly six months to fully resolve, even though production eventually resumed.
Get the Full Details

The impact extends well beyond the factory floor
Manufacturing has economic impact that is easy to gloss over. It creates jobs, yes, but it also drives demand for raw materials, transportation, packaging, and a whole ecosystem of supporting industries. When a manufacturing plant opens in a region, you tend to see ripple effects in local services, housing, and infrastructure. When it closes, the opposite happens. This is not theoretical. I watched a small town lose about fifteen percent of its population after a major manufacturing facility shut down in the early twenty-twenties. The decline was gradual but steady, and it affected every business in that area. Environmental impact is another consideration that gets talked about but rarely understood in practical terms. Manufacturing consumes energy, water, and raw materials, and it generates waste. Some of that waste is recyclable. Some of it is not. The push toward sustainable manufacturing is real, but it is also uneven. Some companies have genuinely reduced their environmental footprint through better processes and materials. Others use sustainability as a marketing angle without meaningful changes underneath. The economic impact of manufacturing also ties into trade policy. Tariffs, quotas, and trade agreements directly affect the cost of imported raw materials and exported finished goods. A tariff change can shift the entire economics of a product line overnight. I have seen companies that appeared profitable one quarter become unprofitable the next purely because of a regulatory shift in a key import market. Planning for that kind of volatility requires a level of strategic thinking that most small manufacturers do not have the bandwidth for.
Practical realities that most guides skip
If you are dealing with manufacturing, whether as a business owner or just someone trying to understand how things get made, there are a few hard truths worth knowing. First, lead times are almost always longer than anyone estimates. If a supplier tells you four weeks, plan for six. If they tell you six, plan for eight. This is not pessimism. It is experience. Second, the cheapest option is rarely the best option. A low-cost supplier might save you money on unit price, but if they have inconsistent quality or unreliable delivery, those savings get eaten up quickly. I once saved maybe two hundred dollars per unit by switching to a cheaper supplier, but the return rate on defective products cost us roughly fourteen hundred dollars per unit in rework and customer complaints. The math did not work out the way it looked on paper. Third, communication between design and production teams is where most problems originate. Engineers design things that look good but are difficult or expensive to manufacture. Production teams build things that meet the spec but miss the intent. Getting these groups to talk to each other early in the process prevents a lot of downstream headaches. It also tends to reduce prototype iterations, which saves both time and money.
Scaling is another area where expectations collide with reality. What works at a small production run often breaks when you try to multiply it. Tools wear out faster. Quality control becomes harder to maintain consistently. Supplier capacity becomes a constraint. I have seen companies double their output on paper and then spend six months actually hitting that number because they had not accounted for the operational drag that comes with scale. The impact of manufacturing also touches consumers in ways that are easy to overlook. The price you pay for a product includes not just the cost of materials and labor, but also the cost of quality management, logistics, and the overhead of keeping a production line running. When you see a product priced lower than expected, it is worth asking what tradeoffs were made to achieve that price. Sometimes the tradeoff is nothing significant. Sometimes it is a compromise on materials or process that will show up later.