Pressure gauges, calibration labs, and the noise that comes from ignoring one number
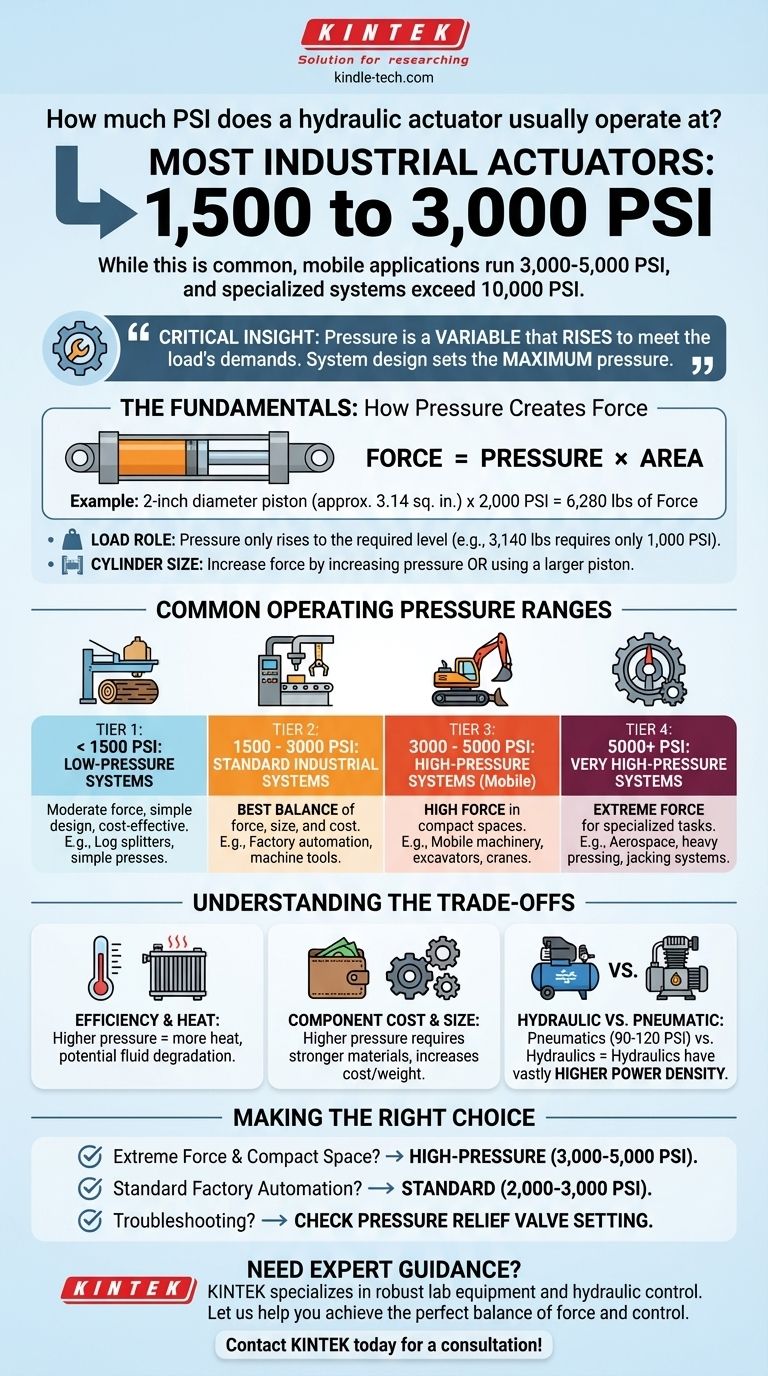
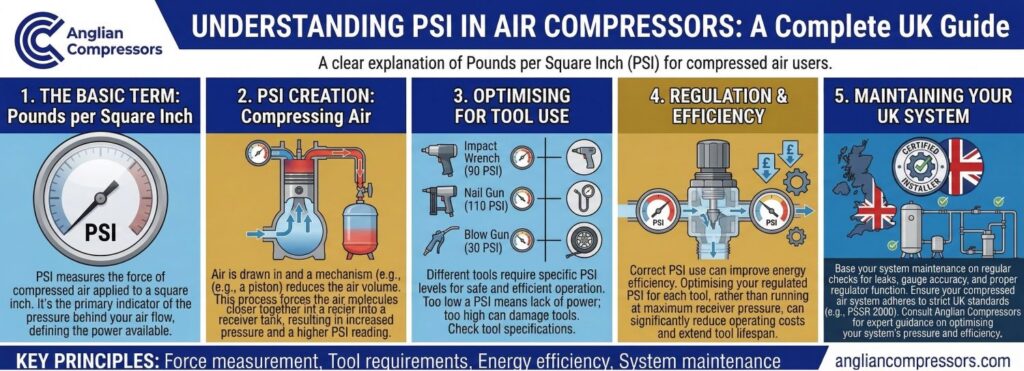
I spent three days in a manufacturing plant in Ohio trying to figure out why a hydraulic press kept failing intermittent pressure tests at exactly 3,200 PSI. The schematic said the system was rated for 5,000 PSI, the gauge read fine, the pump sounded normal, and the maintenance log showed no leaks. The problem turned out to be a $14 gauge from a discount supplier that had drifted 8 percent off scale at the high end, combined with a relief valve that was set 120 PSI too high because someone had backed it out during a previous overhaul and never torqued it back down. When I finally got a NIST-traceable reference gauge on the line, the real system pressure was 3,640 PSI, not 3,200. The press wasn't under-pressurized. It was over-pressurized and the bad gauge was lying about it. PSI stands for pounds per square inch. It is a unit of pressure in the US customary system, defined as one pound-force applied to an area of one square inch. In SI terms that is approximately 6,894.76 pascals. The reason PSI remains the dominant unit in North American pressure system documentation is historical lock-in, not technical superiority. Hydraulic systems, pneumatic instrumentation, boiler codes, and pipeline specs all reference PSI or multiples thereof (ksi, msi) because the ASME Boiler and Pressure Vessel Code, ISO 5198, and API standards were written around it. The industry standard that actually holds pressure systems together is not a single document. It is a layered set of codes and test methods that overlap, contradict, and sometimes leave gaps. ASME Section VIII Division 1 covers unfired pressure vessels up to 3,000 PSIG in the US. ASME B31.3 covers process piping. ISO 4126 covers safety valves. API 520 and 521 cover pressure-relieving systems. SAE J1926 covers hydraulic fittings. Each one defines its own test pressures, acceptance criteria, and material allowances. A system designer has to reconcile all of them, and when they conflict, the project typically defaults to the most conservative clause unless someone explicitly decides otherwise.
I learned this the hard way on a compressed air system upgrade where the engineering spec called for ASME B31.3 compliance, the safety valve was sized per API 521, and the manifold piping was fabricated to ASTM A106 Grade B. The pressure test procedure followed ASME Section VIII, which requires a hydrostatic test at 1.3 times the design pressure. The valve manufacturer required a pneumatic test per ISO 4126 at 1.1 times the set pressure. We ended up performing both tests sequentially, which added four days to the schedule and cost roughly $18,000 in lost production time. The system worked fine afterward, but the coordination overhead was unnecessary if someone had decided upfront which code governed the test.
How pressure ratings actually work in practice
A pressure rating is not a single number. It is a temperature-dependent allowance that degrades as temperature rises. ASME Section II Part D provides the allowable stress values for materials at various temperatures. For carbon steel like ASTM A106 Grade B, the allowable stress at ambient temperature is about 20 ksi, but at 400 degrees F it drops to roughly 17.4 ksi, and at 600 degrees F it is about 13.8 ksi. A pipe rated for 500 PSI at ambient might only be rated for 398 PSI at 600 degrees F. Most operators miss this because they look at the nameplate rating and assume it applies across the entire temperature range. Gauge accuracy is another area where people routinely make mistakes. A Class 1.0 gauge has a tolerance of plus or minus 1 percent of full scale. If the gauge has a 0 to 500 PSI range, the error band is plus or minus 5 PSI across the entire scale. A Class 0.5 gauge improves that to plus or minus 2.5 PSI. For precision work like hydraulic test benches or calibration labs, you typically need Class 0.25 or better, which costs two to three times as much. I once saw a plant use a $22 hardware-store gauge to verify a 3,000 PSI hydraulic system. The gauge read 2,950 PSI when the NIST-traceable reference showed 3,040 PSI. The difference was 90 PSI, or about 3 percent, which exceeded the gauge accuracy by a factor of three.
Get the Full Details

Common failure modes and what to check first
Pressure system failures typically fall into three categories: overpressure events, leakage, and instrumentation error. Overpressure events are the most dangerous because they can cause catastrophic rupture. The primary defense is a properly sized and tested relief valve. API 521 provides the calculation method for determining required relief capacity. The formula accounts for flow rate, fluid properties, back pressure, and discharge conditions. If the relief valve is undersized, the system pressure can exceed the design limit during a block valve closure or heat exchanger tube rupture. I once investigated a steam trap failure where the upstream block valve was closed for maintenance, the trap continued to receive steam from a cross-connected line, and the relief valve was set 200 PSI above the pipe rating. The pipe ruptured at a weld seam. The root cause was a design review that missed the cross-connection. Leakage is the most common failure mode but also the least dangerous if caught early. Gasket failures, fitting creep, and seal degradation typically show up as a gradual pressure drop over hours or days. A well-maintained system should hold pressure within 1 to 2 percent over a 24-hour hydrostatic test. If the drop exceeds 5 percent, you should isolate sections and perform a bubble test with soapy water or a helium leak detector for small leaks. I once found a 0.002-inch pinhole leak in a 2-inch Schedule 80 pipe using a helium mass spectrometer. The leak was at a brazed joint where the braze had cracked during thermal cycling. The system lost 15 PSI per day, which seemed minor until someone calculated the total annual loss of compressed air at the local utility rate. Instrumentation error is the most insidious failure mode because it mimics normal operation while quietly degrading performance. Bad gauges, drifted transmitters, and miscalibrated controllers can cause operators to make decisions based on wrong data. I once replaced a pressure transmitter on a nitrogen service line where the reading had been stable at 150 PSI for six months. When we removed it, the diaphragm was corroded and stuck, holding a constant output regardless of actual pressure. The real pressure was 120 PSI, which meant the downstream process was running at 20 percent less pressure than specified. The quality defects that followed took two weeks to trace back to the transmitter.
Test procedures that actually matter
Hydrostatic testing is the standard method for verifying pressure vessel and piping integrity. ASME Section VIII requires a test pressure of 1.3 times the design pressure for most vessels. The test should be held for a minimum of one hour at steady temperature. The acceptance criterion is no visible leakage and no pressure drop exceeding the temperature-corrected allowance. Pneumatic testing is used when the system cannot be wetted, such as oxygen service or nitrogen systems. The test pressure is 1.1 times the design pressure, which is lower than hydrostatic because compressed gas stores significant energy and presents a higher rupture risk. I once saw a plant perform a pneumatic test on a 500 PSI nitrogen system at 650 PSI without adequate shielding. The test manifold fitting failed and the coupling flew across the room, injuring a worker. The fix was simple: use hydrostatic testing whenever possible, and when pneumatic testing is required, provide blast shields and maintain a safe distance. Relief valve testing is often neglected because it requires system shutdown. ASME Section VIII and API 520 recommend periodic testing per the manufacturer's instructions, typically every one to five years depending on service severity. The test method varies: pop test for spring-loaded valves, vacuum test for bellows valves, and calibration bench test for high-precision applications. A relief valve that is set 5 percent above the design pressure provides minimal protection. A valve that is set 10 percent below may nuisance-pop during normal transient conditions. I once found a relief valve on a hydraulic accumulator system that was set 180 PSI above the design pressure because the setter had misread the nameplate. The valve never opened during a test event, and the accumulator ruptured at 3,200 PSI. The repair cost was approximately $42,000, including the accumulator, piping replacement, and three days of downtime.
When PSI is the wrong unit
PSI works well for systems up to about 10,000 PSI. Beyond that, ksi (kilo PSI) or bar becomes more practical. Bar is the standard unit in most of the world outside the US, and 1 bar equals approximately 14.5038 PSI. Many international projects require conversion between PSI and bar, and errors in this conversion have caused real incidents. I once saw a European-spec pump ordered for a US plant with a relief valve set at 100 bar, which the installer read as 100 PSI. The valve opened at 1,450 PSI instead of 100 PSI. The system exceeded the pipe rating by a factor of three before the second relief device opened. The root cause was a purchase order that listed the set pressure without units, and the installer assumed PSI because that was the local convention. Temperature compensation is another area where PSI ratings can mislead. A pressure vessel rated for 500 PSI at 100 degrees F may only be rated for 350 PSI at 500 degrees F due to material strength reduction. The ASME material tables provide the correction factors, but they are not always included on the nameplate. Operators should consult the original design calculation or the manufacturer's pressure-temperature rating chart before raising the operating temperature. I once saw a heat exchanger operated at 450 degrees F when it was rated for 350 degrees F at full pressure. The shell thickness was adequate for the higher temperature, but the tube sheet joints were not. The exchanger leaked after 40 hours of operation at the elevated temperature. The repair required a full tube sheet replacement, which cost approximately $68,000.

Documentation that prevents problems
A complete pressure system file should include the design basis, material specifications, welding procedure qualifications, NDT reports, hydrostatic test records, relief valve certification, and operating procedures. When a system fails, the first question is whether the original design documents are available and accurate. I once spent two weeks trying to reconstruct the design pressure for a vintage boiler because the original calculation sheet was lost during a facility relocation. The pressure gauge nameplate said 150 PSI, but the safety valve certification said 175 PSI, and the pipe rating varied by section. We eventually determined the original design pressure was 150 PSI based on the thinnest section, and we derated the entire system accordingly. The process cost approximately $28,000 in engineering time and six weeks of delayed operation. Instrument calibration records are equally important. A calibration certificate should show the as-found and as-left data, the traceability chain to NIST or an equivalent national metrology institute, and the uncertainty budget. If a gauge or transmitter was calibrated against a reference with an uncertainty of 0.5 percent of reading, and the gauge itself has a tolerance of 1 percent, the total uncertainty is approximately 1.12 percent. For high-precision applications, the reference uncertainty should be no more than one-third of the gauge tolerance, which means using a reference with 0.33 percent uncertainty or better. I once replaced a calibration program where the reference gauge had an uncertainty of 2 percent, which meant the entire calibration was essentially meaningless. The fix was to invest in a NIST-traceable reference with 0.1 percent uncertainty, which cost approximately $4,500 but reduced calibration error by a factor of twenty.
Bottom line on what PSI means for your system
PSI is a unit, not a standard. The standards that govern pressure systems are codes, calculation methods, and test procedures that vary by jurisdiction, fluid service, and equipment type. Understanding the difference between the unit and the code is essential for safe system design, operation, and maintenance. A well-documented system with proper testing and calibration can operate reliably for decades. A system that ignores the layered standard structure typically encounters problems that are expensive to trace and even more expensive to fix. The investment in proper documentation, qualified materials, and correct test procedures is almost always less than the cost of a single failure event.