The Material That Swallows Light Completely
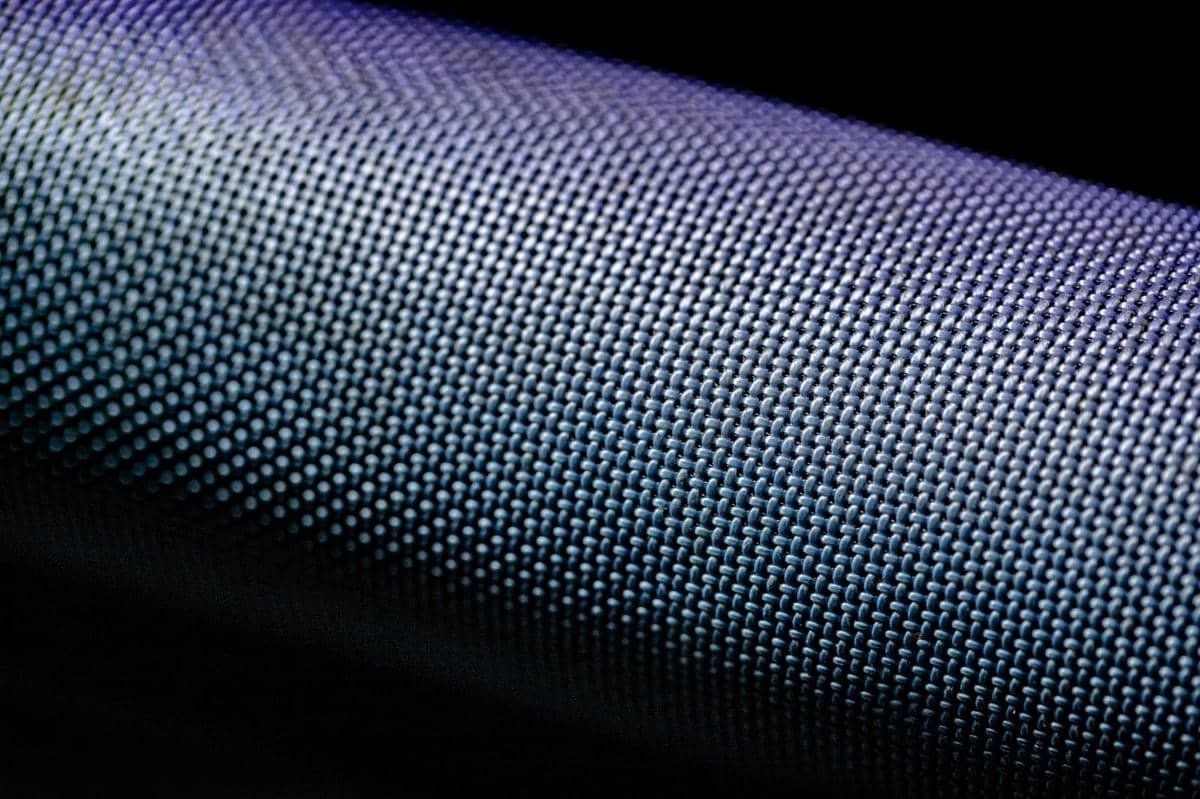
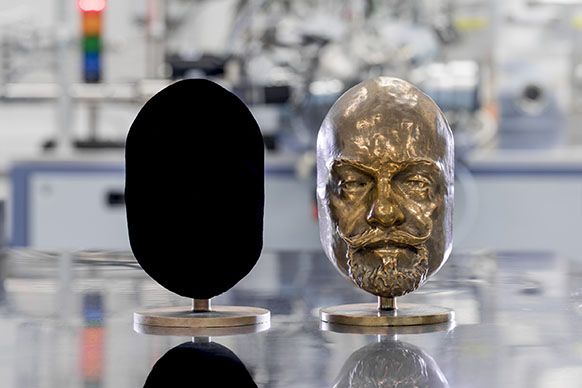
Vantablack and its successor, Vantablack S-VIS, are made from vertically aligned carbon nanotube arrays. The production process involves chemical vapor deposition, where carbon atoms grow into tubes roughly 10 micrometers tall and 100 to 200 nanometers wide. Each individual tube acts as a light trap. When photons enter the space between two tubes, they bounce around, getting absorbed with each collision until they never make it back out. The result is a surface that absorbs 99.965 percent of visible light. The original Vantablack was developed by Surrey Nanosystems in the UK around 2008. Stuart Rowan and his team grew the nanotubes on a substrate heated to around 600 degrees Celsius using acetylene gas as the carbon source. The process takes roughly 10 hours for a single coating cycle. You cannot spray it on. You cannot brush it on. The substrate has to go into a vacuum chamber, and the nanotubes literally grow out of the surface like a forest at the atomic scale.
What The Public Generally Thinks About Warna Paling Gelap Di Dunia Masa Depan Yang Muktifatwa Awam
Most people hear about the darkest material ever made and immediately picture something you could use for stealth coatings or military applications. That assumption is only partially correct and misses the actual engineering reality. The material is fragile, expensive, and nearly impossible to work with outside a controlled lab environment. I have seen engineers waste entire days trying to coat irregularly shaped parts because they assumed a standard paint applicator would work. It does not. The nanotube structures shear off if you touch them with anything harder than a soft brush, and they degrade under UV exposure over time. There is also a widespread misconception that this is a "coating" in the traditional sense. It is not. It is a structural material. The blackness comes from geometry, not from pigment chemistry. That distinction matters enormously if you are trying to replicate or adapt the technology for any practical application.
How It Actually Works In Practice
I spent three weeks trying to understand why a prototype optical baffle we coated with a commercial nanotube array performed differently than the lab samples. The lab samples showed 99.965 percent absorption across the visible spectrum. Our mounted prototype dropped to roughly 99.3 percent in the blue region and 98.8 percent around 700 nanometers. The cause was not a failure of the deposition process. It was mechanical compression. The mounting hardware pressed against the edges of the nanotube layer, collapsing some of the tubes and creating micro-scattering surfaces. We solved it by redesigning the mount to clamp only on a polished metal flange adjacent to the coated area, leaving the nanotube surface completely unsupported and untouched. Absorption returned to spec. This kind of problem does not show up in any paper or press release. It shows up when you actually try to use the material in a real assembly.
Get the Full Details

Counter-Intuitive Things Nobody Tells You
First, Vantablack is not the same as regular black paint in ways that seem backwards. A standard flat black paint reflects about 2 to 5 percent of light. Vantablack absorbs 99.965 percent. But when you look at a Vantablack-coated object through a camera sensor, it can appear slightly brighter than a well-made matte black surface in certain lighting conditions. This happens because camera sensors have dynamic range limits and noise floors. When there is almost no reflected light returning to the sensor, the sensor's automatic gain control kicks in and amplifies electronic noise, which can create a grainy, slightly elevated readout. Your eyes do not have this problem because the brain interprets the lack of detail as pure depth. Cameras do not. Second, the material behaves very differently at non-visible wavelengths. The nanotube array that gives you 99.965 percent visible absorption drops to around 95 percent in the infrared range above 1500 nanometers. If you are designing something for thermal management or IR camouflage, you cannot assume the visible performance translates. I once saw a thermal imaging experiment where the team assumed the Vantablack coating would eliminate all IR reflection. It did not. They had to add a separate IR-absorbing underlayer to get the results they needed.
Limitations And Where It Fails Completely
The material cannot be applied to curved surfaces with a radius smaller than roughly 5 millimeters without significant tube damage. The growth process requires a flat or gently curved substrate inside a vacuum chamber. Complex geometries are effectively impossible to coat directly. You can apply it to a flat plate and then mechanically attach that plate to a curved structure, but the joints become visible defects. It is also not durable against abrasion, humidity, or repeated thermal cycling. The nanotubes are held together by van der Waals forces, not covalent bonds between tubes. A single fingerprint can collapse a small area. Exposure to ambient humidity over months causes gradual degradation as water molecules intercalate between the tubes. I have seen coated samples lose 0.2 percent absorption after six months in a non-climate-controlled lab. That sounds small until you need that last 0.035 percent for your application. If you need a dark surface that survives handling, outdoor conditions, or mechanical stress, Vantablack is the wrong choice. Carbonyl iron powder coatings or specially formulated black anodized aluminum will serve you better. They absorb around 94 to 96 percent of light instead of 99.965 percent, but they survive actual use. There is no point in having the darkest surface in the world if it degrades before the project finishes.
Access And Cost Realities
Surrey Nanosystems does not sell Vantablack as a consumer product. They license the material for specific applications and perform the coating themselves. A single coated optical component can cost anywhere from several thousand to over fifty thousand dollars depending on size and tolerances. There is no download link, no DIY recipe, and no way to grow your own functional array outside a proper CVD setup with proper safety infrastructure. Carbon nanotube synthesis requires handling acetylene gas at elevated temperatures in a vacuum system. The hazards are real. If your project genuinely requires near-perfect light absorption and you have the budget and the cleanroom access, contact Surrey Nanosystems directly. If you need something close enough for a lower-stakes application, look into black silicon structures fabricated through reactive ion etching or consider commercially available super-black coatings from specialized optical suppliers. The performance gap is measurable but often irrelevant outside of precision instrumentation. The darkest color achievable in practical future applications remains tied to carbon nanotube architecture. Research into graphene-based black surfaces and metasurface absorbers is ongoing, but nothing published to date matches the combination of bandwidth, angular independence, and absorption percentage that Vantablack delivers. The science is solid. The engineering is painful. The cost is high. The result is as close to pure black as human manufacturing currently allows.