What Microencapsulation Actually Is
Microencapsulation is just a way of wrapping tiny particles or droplets of a core material inside a protective shell. The core can be liquid, solid, or gas. The shell is usually a polymer, lipid, or protein-based barrier. The particle sizes range from about one micrometer to a few hundred micrometers. This isn't some revolutionary breakthrough from last week. People have been doing variations of this since the 1950s, with commercial applications scaling up in the late 1990s. The basic goal is always the same: control the release of something, protect it from degradation, or mask a taste. The industries that care most about this are pharmaceuticals, food, agriculture, and cosmetics. Each one has wildly different requirements. A drug has to survive stomach acid and release at the right time. A fragrance has to slowly bleed out over hours instead of vanishing instantly. A pesticide has to stay active in sunlight and rain. The technique you pick depends entirely on what you're trying to encapsulate and where it needs to go.
How The Main Methods Work In Practice
Unveiling The Power Of Microencapsulation Techniques A Comprehensive Guide To Revolutionizing Industries
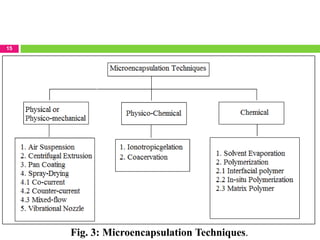
There are several production methods, and they fall into roughly three buckets: physical, chemical, and physicochemical. The most common ones you will actually encounter in a lab or production setting are coacervation, spray drying, fluid bed coating, and emulsion techniques. Complex coacervation involves mixing two oppositely charged polymers, usually gelatin and gum arabic, in an aqueous solution. When you adjust the pH and salt concentration, the polymers phase-separate into a dense, syrupy liquid called coacervate. That coacervate wraps around your core material. Then you cool the mixture or add a crosslinker like glutaraldehyde to harden the shell. This method gives you smooth, uniform shells. It works well forfragile cores like probiotics or enzymes that can't handle high heat. The problem is that coacervation is slow. A typical batch takes four to six hours from start to finish. It also requires careful control of pH, temperature, and stirring speed. If you get the shear rate wrong, the coacervate won't coat properly and you end up with clumped particles or bare cores. I spent three weeks wrestling with a gelatin-gum arabic system where the particles kept aggregating into rice-ball-sized clusters. The fix turned out to be lowering the polymer concentration from 15 percent to 8 percent and switching from a overhead stirrer to a homogenizer set at 8,000 rpm during the coating phase. Once I did that, particle size dropped from an average of 200 micrometers down to about 50 micrometers with much better uniformity.
Spray Drying
This is the workhorse of industrial microencapsulation. You dissolve or suspend your core material in an emulsion or solution with your wall material, then force it through a nozzle into a hot air chamber. The droplets dry almost instantly as they fall through the heated zone. The result is free-flowing powder. Spray drying can process liters per hour and is relatively straightforward to scale from bench to production. The catch is heat sensitivity. Even though the residence time inside the chamber is only seconds, the inlet air temperature typically runs between 150 and 220 degrees Celsius. If your core is a volatile essential oil, a heat-sensitive vitamin, or a live culture, you will lose a significant portion of it. The exit air temperature matters more than you might think. Keeping it below 80 degrees Celsius helps preserve thermolabile compounds, but that means longer drying times and potentially higher moisture content in the final powder. For heat-sensitive materials, spray chilling or spray congealing is a better alternative, using a molten lipid carrier instead of hot air.
Get the Full Details
Fluid Bed Coating
In fluid bed processing, pre-formed core particles are suspended in an upward stream of air, fluidizing them like a boiling liquid. Then a binder or wall material solution is sprayed onto the moving particles. The air dries the coating as it is applied, and you build up layers with repeated passes. This is how you get controlled-release tablets and coated pellets in pharma. It gives you excellent control over shell thickness because you can literally build it layer by layer. What people don't tell you is that fluid bed coating is finicky with particle size distribution. If your starting cores vary too much in size, the smaller ones will fluidize differently and you will get uneven coating. You need a narrow size range, ideally within plus or minus 20 percent of the mean diameter. I worked on a project where the core excipients had a broad distribution, and the final product had a bimodal size curve that caused caking in the packaging. Sieving the cores before coating solved the issue, but it added a whole extra step to the process and reduced yield by about twelve percent.
Emulsion-Based Methods
Oil-in-water emulsions are the basis for many microencapsulation processes. You disperse your core material, which is usually hydrophobic, into an aqueous phase containing a wall material, using high-shear mixing or ultrasonication. Then you stabilize the emulsion through cooling, pH adjustment, or addition of a crosslinker. Emulsion techniques are versatile and can produce very small particles if you use high-pressure homogenization. The main drawback is the potential for o/W interface issues. If your core is a liquid oil and your wall material is not sufficiently surface-active, the droplets will coalesce during processing. You need the right emulsifier at the right concentration. Lecithin, Tween 80, and sodium caseinate are common choices, but they each have limitations. Lecithin can introduce oxidative stability problems. Tween 80 has been flagged in some regulatory environments for purity concerns. Caseinate requires precise pH control to stay soluble.
Choosing The Right Wall Material
The wall material is just as important as the encapsulation method. It determines everything: release profile, stability, biocompatibility, and cost. The most widely used materials are modified food starches, sodium caseinate, gum arabic, chitosan, alginate, whey protein isolate, and various synthetic polymers like Eudragit or PLGA. Starches are cheap and generally recognized as safe, but they form relatively permeable shells unless chemically modified. Cross-linked starches give better barrier properties but cost more. Alginate is interesting because it gels at room temperature through ionotropic crosslinking with calcium chloride. That makes it excellent for thermolabile materials, but the resulting beads are fragile and can leak if the calcium concentration is too low or the ionic environment changes after ingestion. I once encapsulated a probiotic strain in alginate beads and stored them at room temperature for six months. The viability dropped from 10 to the power of 9 CFU per gram down to 10 to the power of 6 in about eight weeks. Switching to a composite wall of alginate and chitosan, with a brief calcium chloride dip followed by a chitosan coating, extended shelf stability significantly. The double layer acted as a moisture barrier and the chitosan has intrinsic antimicrobial properties that helped. PLGA is the standard for pharmaceutical controlled release. It degrades through hydrolysis of its ester bonds into lactic and glycolic acid, both of which are metabolized naturally. The degradation rate is tunable by changing the lactide-to-glycolide ratio. Higher glycolide content means faster degradation. But PLGA is expensive, and the acidic degradation products can destabilize certain proteins and peptides. I have seen formulations where the encapsulated protein denatured inside the microcapsules during storage because the local pH dropped. The workaround was adding a buffering agent like calcium carbonate directly into the wall matrix, which neutralized the acid as it formed and kept the protein stable for over a year at refrigerator temperatures.
Common Pitfalls And What To Watch For
Encapsulation efficiency is rarely 100 percent, and that matters more than you might think. In spray drying, for example, fine particles can carry unencapsulated core material that ends up stuck to the chamber walls or collected separately. I measured encapsulation efficiency at about 78 percent on a pilot-scale spray dryer for an essential oil formulation. The missing 22 percent was mostly recoverable by cleaning the cyclone separator and extracting the adhered powder, but that added labor and time. On a larger scale, you need to account for this yield loss in your cost calculations. Another issue is residual solvent. If you use organic solvents in your encapsulation process, especially in methods like solvent evaporation, you need to ensure complete removal. Residual dichloromethane or ethanol above certain thresholds is a regulatory concern. I worked with a contract manufacturer who was using dichloromethane and their final product consistently failed residual solvent testing. The issue was insufficient vacuum drying time. Extending the secondary drying step from four hours to twelve hours under reduced pressure brought the levels well below the permitted limits. They could not afford to switch to a different method at that stage, so they just ran longer cycles and accepted the throughput hit. Packaging matters more than most people realize. Microencapsulated powders are hygroscopic. If you store them in a non-barrier package in a humid environment, the shells will absorb moisture, swell, and eventually rupture. The core will oxidize or degrade. Aluminum-lined pouches or moisture-barrier containers are almost always necessary. I learned this the hard way with a flavor encapsulation project. We used standard polypropylene bags for storage and the product caked and lost volatile content within three weeks at 60 percent relative humidity. Switching to aluminum foil laminated pouches with a desiccant packet eliminated the problem entirely.
When Microencapsulation Is The Wrong Choice
It is worth noting that microencapsulation is not a universal solution. If your core material is already stable and you do not need controlled release or taste masking, the added cost and complexity is unnecessary. Encapsulation typically adds 15 to 40 percent to the per-unit cost of a formulation, depending on the method and scale. For a high-volume food ingredient where the active compound is shelf-stable, simple direct mixing is cheaper and simpler. If you need very large particles, above 500 micrometers, or very small ones, below 100 nanometers, other techniques may be more appropriate. Liposomes and nanoparticles are fundamentally different systems with different manufacturing equipment and regulatory pathways. Microencapsulation occupies a middle ground that is well-suited for particles in the 1 to 500 micrometer range. Trying to force it outside that range usually leads to poor reproducibility and disappointing results. Scale-up is another area where things commonly fall apart. A process that works perfectly in a 500-milliliter batch can behave completely differently at 500 liters. Heat transfer, mixing dynamics, and fluid dynamics all change non-linearly with scale. The safest approach is to validate your process at intermediate scales before jumping to full production. Data from a 50-liter run will tell you far more than extrapolating from a 2-liter lab experiment.


