Polylactic Acid Is Just A Bioplastic, But That Label Oversells It
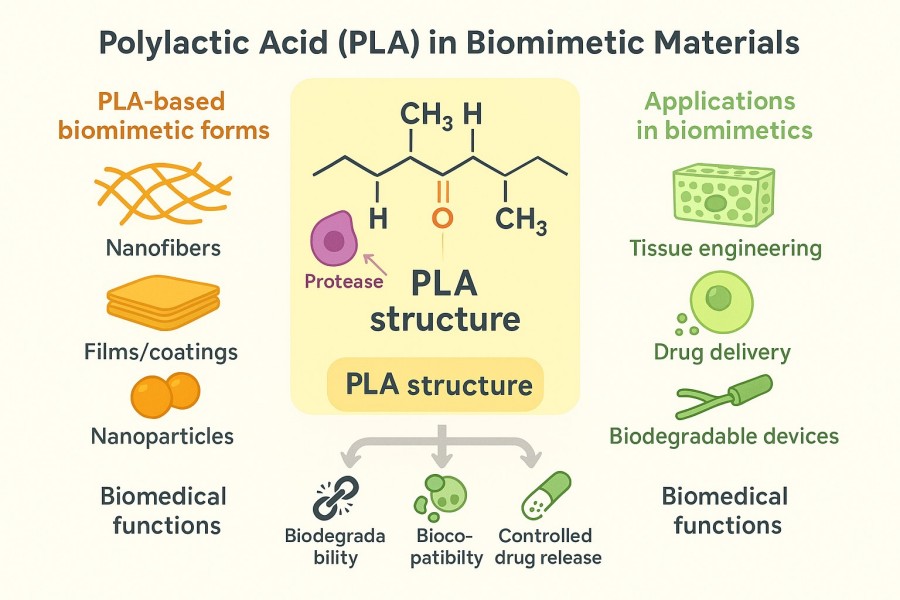
Most people encounter PLA through 3D printing filament or disposable cutlery, and they walk away thinking it is some kind of miracle material. It is not. It is a thermoplastic polyester derived from renewable feedstocks like corn starch or sugarcane, and it has a fairly straightforward structure: repeating lactic acid units linked by ester bonds, with a methyl side group hanging off every other carbon. The polymer chain can arrange itself into different crystalline forms depending on how it is processed, which is where things start to get interesting and frustrating at the same time. The basic repeat unit comes from lactic acid, which exists as two enantiomers — L-lactic acid and D-lactic acid. When you polymerize mostly L-lactic acid, you get PLLA, which is semi-crystalline and relatively stiff. Mix in some D-lactic acid and you get PDLLA, which is amorphous and more ductile. That single structural choice determines whether your printed part will warp like crazy or sit there quietly, so it matters more than most beginners realize. The glass transition temperature for typical PLA sits around 60 to 65 degrees Celsius. Below that, it is rigid and brittle. Above that, it softens dramatically and loses structural integrity fast. This is why a PLA coffee cup placed in hot liquid deforms within minutes, and why a PLA 3D printed bracket left on a dashboard in summer becomes a sad puddle of plastic. The melting range is roughly 150 to 160 degrees Celsius for the crystalline regions, but you will commonly see extrusion temperatures pushed to 190 through 230 depending on the manufacturer and any additives present.
I once spent three days troubleshooting warping and poor layer adhesion on a series of PLA prototypes before I realized the spool had absorbed enough moisture from the warehouse to shift its processing window. The filament had absorbed roughly 0.8 percent water by weight after sitting unpackaged for two weeks in a non-climate-controlled room. Drying it at 55 degrees for six hours brought the moisture down below 0.02 percent and the parts came out clean immediately. You do not need to post-process PLA for moisture nearly as aggressively as you do with PETG or nylon, but skipping drying entirely when the filament has been exposed is a reliable way to get bubbly, weak prints.
How PLA Actually Gets Made
The industrial route usually starts with fermentation. Microorganisms convert sugars from plant material into L-lactic acid, which is then purified and oligomerized into low-molecular-weight lactide rings. These rings undergo ring-opening polymerization using a tin-based catalyst, typically stannous octoate, to produce the high-molecular-weight PLA resin. The lactide intermediate step is critical because it allows you to control stereochemistry far more precisely than direct condensation polymerization would. Direct condensation of lactic acid produces lower molecular weight polymer with significant coloration due to thermal degradation. The ring-opening route gives you the molecular weights needed for extrusion and molding, usually in the 80,000 to 150,000 dalton range for standard grades. If you need higher strength, you can push toward chain extenders that increase the molecular weight further, but that adds cost and process complexity. The byproduct of the condensation step is water, which is trivial to manage. The ring-opening route does not produce water at all, which is one reason it dominates commercial production. The tin catalyst residue is the real environmental talking point here. Food-contact applications require the catalyst to be removed or reduced to parts-per-million levels, which adds a purification step that smaller producers sometimes skip, leading to yellowing and inconsistent mechanical properties in the final resin.
Get the Full Details

Mechanical Behavior And What The Data Actually Means
Tensile strength for neat PLA typically falls between 50 and 70 megapascals, which puts it in the same ballpark as polystyrene and above ABS in raw numbers. Young's modulus runs around 3 to 4 gigapascals, making it noticeably stiffer than many commodity plastics. Elongation at break is the weak point, usually 2 to 6 percent for standard grades, meaning it fractures rather than stretches under load. That brittleness is the single biggest limitation for structural applications. Adding impact modifiers or plasticizers changes the picture, but each modification introduces trade-offs. A common toughened PLA blend might push elongation to 20 or 30 percent while dropping tensile strength into the 40 megapascal range and reducing heat deflection temperature by 10 to 15 degrees Celsius. You are always balancing at least three properties against each other, and there is no free lunch. PLA is also sensitive to hydrolysis over time, especially at elevated temperatures and in humid environments. The ester bonds in the backbone can cleave when water molecules attack them, which means the material slowly degrades even without microbial action. This is why PLA packaging designed for compostability will break down in an industrial composting facility at 58 degrees Celsius and high humidity within weeks, but a PLA product sitting on a shelf at room temperature and normal indoor humidity can retain its properties for years. The degradation rate is highly dependent on environment, not just material composition.
Processing Considerations That People Ignore
PLA shrinks less than most thermoplastics — roughly 0.2 to 0.8 percent linear shrinkage — which is why it is popular for 3D printing and why it can still warp badly if the part cools unevenly. The shrinkage is low but anisotropic, meaning it contracts more in one direction than another depending on flow orientation during molding or extrusion. This creates internal stresses that are not visible until the part is demolded or loaded. For injection molding, the melt temperature window is narrow. Run too cool and you get short shots and poor surface finish. Run too hot and the polymer degrades, producing acrolein — a sharp, irritating odor — and the part turns yellow while losing mechanical properties. The sweet spot is usually 180 to 210 degrees Celsius for standard grades, with mold temperatures between 30 and 80 degrees. Higher mold temperatures promote crystallinity, which improves heat resistance but increases cycle time because the part needs more time to solidify enough to eject cleanly. Blistering in injection molded PLA parts almost always traces back to moisture or degraded polymer breaking down inside the barrel. I learned this the hard way on a run of thin-walled containers where the first 200 pieces looked fine and then every piece after that came out cloudy with visible gas pockets. The screw had been sitting at 220 degrees for four hours with no material flowing through it during a lunch break, and the resident polymer had degraded enough to start decomposing on subsequent shots. Flushing the barrel with a stable polymer like HDPE and dropping the idle temperature to 185 eliminated the problem entirely.
Applications Beyond The Usual Suspects
Surgical sutures are one of the older and more reliable uses of PLA. The material degrades into lactic acid, which enters the Krebs cycle and is metabolized naturally by the body. Absorbable orthopedic fixation devices — pins, screws, plates — rely on the same mechanism, with degradation timelines ranging from several months to two years depending on the device geometry and crystallinity. The key advantage is that the implant loses strength gradually as new tissue forms, rather than failing catastrophically. Packaging applications span food containers, film wraps, and injection-molded trays. PLA film has good clarity and a pleasant sheen, which is why it is common for produce packaging and retail display bags. The barrier properties are mediocre compared to PET or EVOH, so multilayer structures are often used when oxygen or moisture barriers are required. A single-layer PLA container will let oxygen pass through at rates that compromise shelf life for many products, which is why the industry typically co-extrudes with barrier layers. Agricultural mulch films made from PLA are gaining traction in Europe and parts of Asia. Instead of collecting and disposing of traditional PE mulch films after harvest, farmers till the PLA film into the soil where it degrades over the growing season. The degradation rate needs to match the crop cycle closely — too fast and the film disintegrates before the crop is ready, too slow and you have residue problems. Formulations are tuned with starch blends and additive packages to hit that window, usually 90 to 180 days of field exposure.
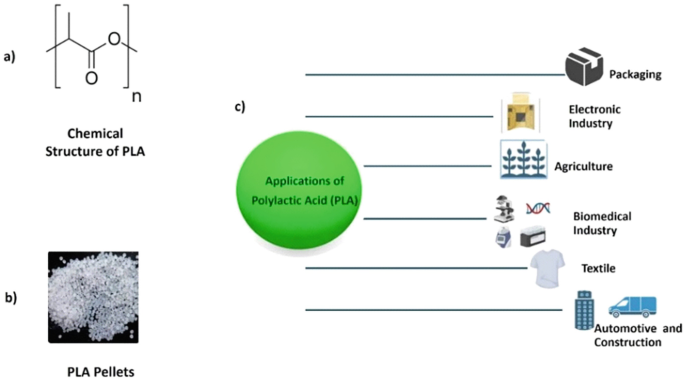
In 3D printing, PLA remains the default choice for prototyping and hobbyist use because it extrudes reliably, sticks well to build surfaces, and requires no heated chamber. The limitation is temperature resistance. Any application where the part will exceed 55 degrees Celsius consistently is a poor candidate for standard PLA. For those cases, PETG, ASA, or polycarbonate blends are better options, though they demand more careful printing conditions and sometimes enclosure temperature control.
What The Composting Claim Actually Covers
PLA is marketed as biodegradable and compostable, and that is technically true under specific conditions. Industrial composting standards like EN 13432 and ASTM D6400 require the material to disintegrate into fragments smaller than 2 millimeters within 12 weeks, achieve a certain percentage of biodegradation measured by CO2 evolution, and not contain heavy metals at harmful levels. PLA meets all of these requirements in an industrial composting environment maintained at 58 to 60 degrees Celsius with active microbial activity and high moisture. Home composting bins rarely reach those temperatures, and ambient outdoor conditions are even less favorable. A PLA cup buried in a garden pile at 25 degrees will degrade very slowly, possibly taking a year or more depending on moisture and microbial populations. Throwing PLA into a home compost and expecting it to vanish in a month is unrealistic. Marine degradation is even slower, and PLA does not meaningfully break down in ocean conditions on any useful timescale. The recycling stream is another complication. PLA contaminates PET recycling if it enters the same stream, because the two materials have different melting points and degradation behaviors. Even small percentages of PLA in a PET recycle batch can cause haze, weak spots, and processing defects. Many recycling facilities do not have the sortation capability to separate PLA from other clear plastics, which means PLA packaging often ends up landfilled or incinerated regardless of what the label says. Mechanical recycling of pure PLA is possible but economically marginal due to the volumes involved and the quality degradation that occurs through repeated reprocessing.
When PLA Is The Wrong Choice
High-temperature environments, outdoor structural applications exposed to UV for extended periods, and parts that need to absorb impact without fracturing are all scenarios where PLA underperforms. UV exposure causes yellowing and surface embrittlement within weeks to months depending on the grade and any stabilizers added. Standard PLA has essentially no UV resistance unless modified with stabilizers, which adds cost and may affect food-contact compliance. If you are selecting a material and the part will see sustained temperatures above 55 degrees, flexural loading with sharp impact, or long-term outdoor exposure, PLA is not the default answer. PETG handles moderate temperatures better with more toughness. ASA resists UV degradation and maintains properties outdoors. Polycarbonate handles higher heat and offers superior impact strength, though it requires drying and higher processing temperatures. Each alternative has its own processing trade-offs, but they address the specific failure modes that PLA cannot. The material itself is not flawed. It is just narrowly optimized for a specific set of conditions — moderate temperature, moderate load, short-to-medium service life, and end-of-life scenarios where industrial composting or controlled degradation is available. Understanding where that optimization breaks down is what separates someone who picks materials randomly from someone who picks them intentionally.