What Actually Happens Inside an Extruder
Plastic extrusion is continuous. You melt polymer pellets, force them through a die, and you get a consistent profile out the other end. That sounds simple enough until you've been running a line for six hours and the dimensions start drifting. The machine is fine. The material isn't. I ran into this with a custom PVC conduit profile back in 2019. We were pulling 45 mm outer diameter pipe at roughly 12 meters per minute. Everything looked stable on the HMI. Then the quality tech flagged that the wall thickness was oscillating by plus or minus 0.3 millimeters over a twenty-minute window. The die nuts weren't backing off. The screw RPM was locked. We checked the barrel thermocouples — all within spec. The problem turned out to be the raw compound. The resin supplier had shifted to a slightly different bulk density batch without telling us. Same MFI rating on the data sheet, different flow behavior once it hit the metering zone. The feed zone started surging because the pellets were packing differently. Fixed it by adjusting the feeder rate down 8 percent and adding a short dwell time in the conversion section. It was a pain to dial in, but once we knew what we were looking for, it became routine.
Unlocking The Secrets Of Plastic Extrusion A Comprehensive Guide
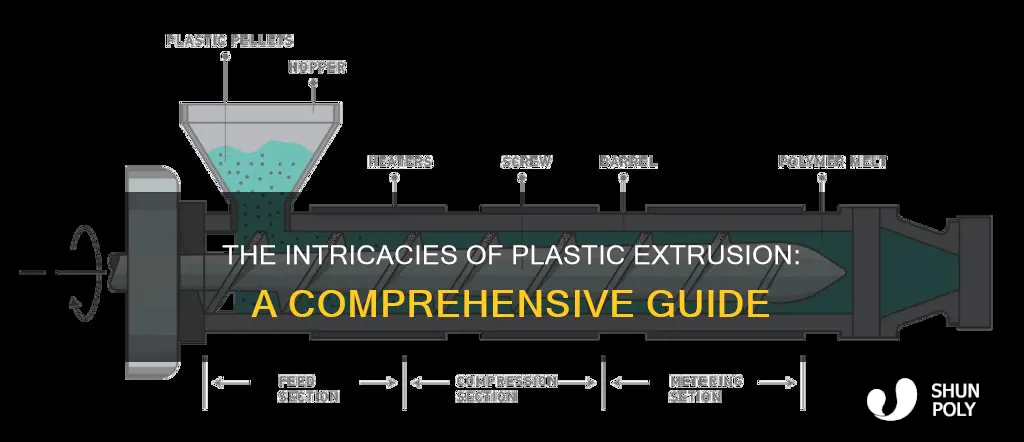
This guide isn't about theory you can pull from a textbook. It's about the things that actually matter when you're standing in front of a running line trying to hit tolerances. Let's talk about the screw, the die, and the cooling section, because those three sections are where 90 percent of your problems live. The screw design dictates everything before the melt even reaches the die. A standard 25:1 L/D screw with a compression ratio of 2.5 to 3.0 will handle most commodity thermoplastics — PP, PE, PS — without issue. But if you're running PVC or PC, you need a different geometry. PVC degrades fast above 200°C in the barrel, so you want a lower compression ratio around 2.0 to 2.2 and a longer transition zone to keep shear heat down. Polycarbonate is the opposite problem — it needs high shear to viscous flow properly, so a higher compression ratio and a shorter feed section work better. Beginners usually buy one screw and try to run every material through it. That works for prototypes. It doesn't work for production. Here's something most guides skip: the barrier screw isn't always better. A mixed screw with a standard design actually melts HDPE more consistently than a barrier type because HDPE has a wide melting range. The barrier flights create localized hot spots that degrade the polymer in that narrow gap. I learned that the hard way running 63 mm irrigation tubing. Swapped to a mixed screw, output went up 15 percent and the part clarity improved noticeably. The die manufacturer had recommended the barrier screw on paper. Paper doesn't account for polyethylene's crystalline structure.
Die design is where dimensional control lives or dies. The die head distributes melt evenly across the profile cross-section. If the flow isn't balanced, some sections will pack denser than others and shrink differently during cooling. A proper die uses manifold design with individually adjustable die lips. You open or close each lip with a shim system — usually 0.05 mm increments — to fine-tune wall thickness across the profile. Counter-intuitive point: thinner sections don't always need more material flow through the die. Sometimes they need less. When a profile has thick and thin walls, the thick sections cool slower and continue drawing material from the die after the thin sections have solidified. That's why you calibrate by pulling vacuum on the thinner sections first, then let the thicker sections breathe. Running the vacuum too aggressive on thick areas causes sink marks that no amount of die adjustment will fix. I spent three days fighting sink on a 40 mm channel profile before someone pointed out that the downstream vacuum was set 10 kPa higher than the upstream stations. Lowered it, sink disappeared. Profile went from reject to acceptable in about twenty minutes. Calibration is the step people rush and regret. Calibrators — either vacuum tanks or sleeve calibrators — hold the extrudate to final dimensions while it cools. Vacuum calibration is standard for hollow profiles like pipes and conduits. The part enters the calibrator, vacuum pulls it against the stainless steel bore, and a spray of water or a mist keeps it cooling. Sleeve calibrators are used for solid profiles where the shape is complex enough that vacuum alone can't maintain geometry.
Get the Full Details

The mistake I see most often: people set the calibrator length equal to the die length and call it done. A calibrator should be at least 3 to 5 times the profile's largest dimension in length. Anything shorter and the part hasn't developed enough skin strength to hold its shape when it exits. The result is warpage that shows up downstream, not at the line. Warpage is expensive because it's invisible during the extrusion run and only apparent when the part gets cut or assembled. A 6-meter run of warped conduit looks straight when it's coiled. It looks wrong the second you lay it flat on a bench. Cooling throughput matters more than anyone admits. You can run the line faster by increasing screw speed, but if your cooling section can't keep up, you're just producing poorly formed product at a higher rate. Every meter per minute you gain on the line needs corresponding cooling capacity. A general rule of thumb: you need roughly 2 to 3 kW of cooling per kilogram of output for amorphous plastics like PVC and PC, and 1.5 to 2 kW per kilogram for semi-crystalline materials like PP and PE. Crystalline plastics release more latent heat during solidification, which seems backwards but it's because the phase change from melt to crystal structure is highly exothermic. Amorphous materials cool gradually without that sharp thermal event, so paradoxically they can sometimes be easier to manage in marginal cooling setups. I had a situation where we tried to pull a PP profile at 18 m/min through a cooling bank rated for 12 m/min maximum. The part came out dimensionally okay but internal stresses were through the roof. Two weeks later, the parts were warping in storage. The material hadn't fully relaxed. We dropped the line speed to 10 m/min, added a stress-relief oven section after cooling, and the warpage stopped. The throughput hit dropped by 44 percent but the scrap rate went from about 8 percent to under 1 percent. Net gain.
Troubleshooting common defects without guessing. Sharkskin — that rough, orange-peel surface on extrudate — happens when the melt stress at the die exit exceeds the polymer's critical strain. It's most common with high MFI materials and high output rates. The fix isn't always "lower the temperature." Sometimes raising the die temperature actually makes it worse because the melt strength drops further. The real solutions are using a die with a longer land length, adding a breaker plate with higher mesh count upstream, or switching to a process aid like a fluoropolymer additive that migrates to the surface and reduces friction. Most compounders already include these additives. If you're running a base resin and wondering why sharkskin appears at 20 m/min but not at 15, that's your clue. Melt fracture is the worse version of sharkskin. The surface becomes gross and irregular, not just textured. This is a rheology limit, not a process tweak problem. If you're hitting melt fracture, you need to either reduce the shear rate by increasing the die gap, switch to a higher molecular weight grade, or add a processing aid. There's no amount of temperature adjustment that will fix fundamental melt fracture. I've seen operators crank barrel temperatures up 20°C trying to smooth out a surface defect that was purely a shear problem. It made the fracture worse because lower viscosity at higher temperature means higher shear rate at the same output.
Bubbles or voids in the profile usually mean moisture or volatiles. Dry your material. PVC needs drying at 60 to 70°C for 2 to 3 hours. PC needs 120°C for 3 to 4 hours. If you're running a dried-but-still-bubbling profile, check for degraded material in the barrel. Old material sitting in the screw flight gaps for hours will and release gas. A purging compound run at maximum screw speed for 15 minutes usually clears it, but prevention is better — don't let the barrel sit hot and empty between runs. Dimensional stability testing is where production meets reality. You can measure diameter at the calibrator exit and it looks perfect. Measure it three meters downstream and it's different. Thermal contraction varies by material. PP shrinks about 1.5 to 2.5 percent. PVC shrinks 0.1 to 0.5 percent. PE can shrink 1.5 to 4 percent depending on the grade. You need to oversize the die opening to compensate, not chase dimensions with the calibrator. The calibrator sets the final size, but the die determines the melt distribution. If you're adjusting die lips constantly to hit diameter, your die is undersized or your melt distribution is off. That's a die design problem, not a process problem. When extrusion isn't the right answer.

Extrusion is great for constant cross-section profiles produced in long continuous lengths. It's terrible for short runs with frequent material changes because purging between colors or resin types costs time and material. Switching from white PVC to black PVC can take 30 to 45 minutes of purging on a standard line, sometimes longer with dark colors going to light. If your order book is mostly small batches under 500 meters, injection molding or even thermoforming might be more economical despite higher per-unit cost. The setup time on an extrusion line is measured in hours, not minutes. Break-even for a typical 65 mm line producing rectangular conduit comes out around 800 to 1200 meters depending on profile complexity and material. Below that, you're eating setup cost into your margin. High-fill composite materials — say, wood-plastic composites with 60 to 70 percent wood flour — are another case where extrusion struggles. The abrasiveness wears screw and barrel rapidly. The viscosity is unpredictable because filler loading affects flow differently than pure resin. Output rates drop significantly, and die wear becomes a recurring expense. If you're considering WPC extrusion, budget for a twin-screw micro-feed system and hardened screw/barrel elements. A single-screw line will be out of tolerance within weeks of running high-fill compounds. Process documentation saves more jobs than any single optimization trick. The best lines I've worked with keep a running log for every profile: screw speed, take-up speed, barrel temperature zones, die lip settings, calibrator vacuum levels, and cooling water temperature. When a new batch of material arrives and dimensions drift, that log is the first place you look. Without it, you're guessing. With it, you can compare current conditions against the last successful run and adjust from a known baseline instead of starting from zero.
A final note on automation. Modern lines have closed-loop control on diameter using laser micrometers feeding back to the haul-off speed or screw RPM. These systems work well within their design envelope. They don't handle material variability well. If your compound batch changes MFI by 20 percent — and that happens more often than you'd think — the feedback loop will chase the correction and oscillate. The operator needs to be ready to intervene manually when the automatic adjustments become erratic. Automation handles steady-state. It doesn't replace judgment during transients.