What ID Card Sample Formats Actually Look Like in Practice
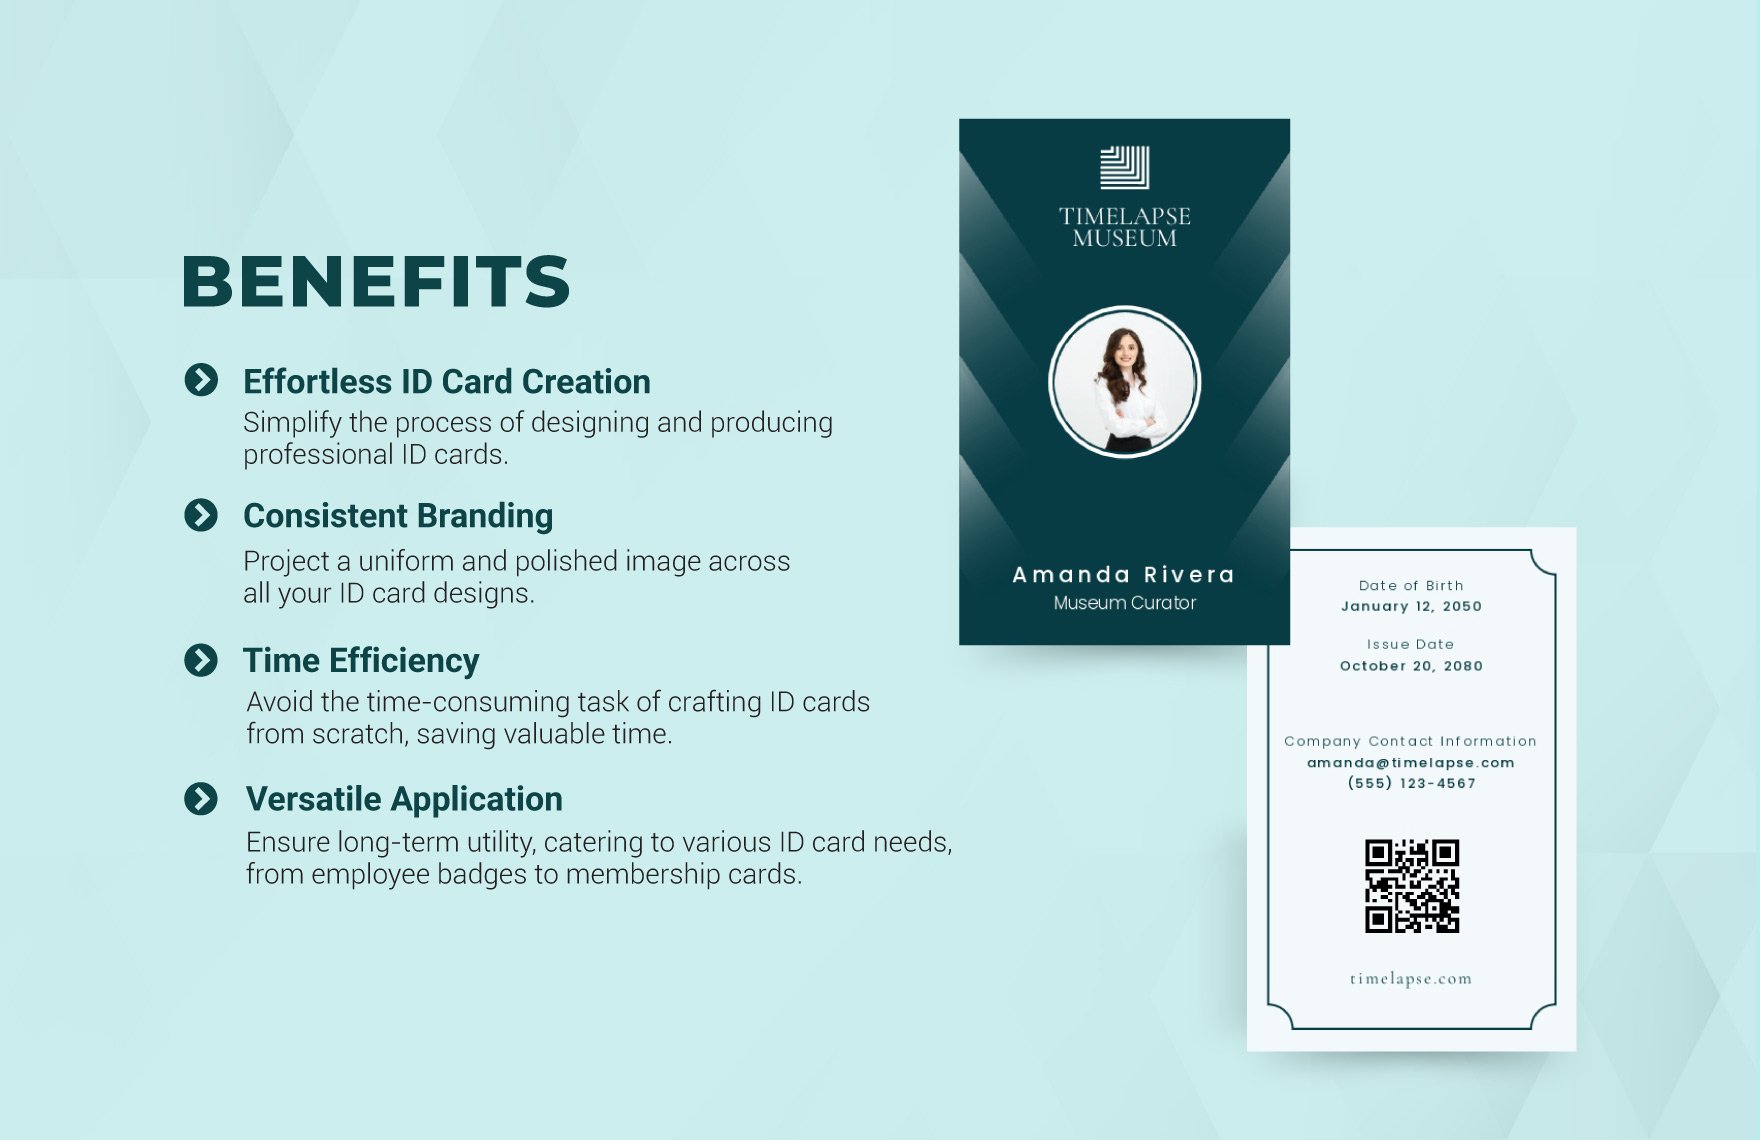
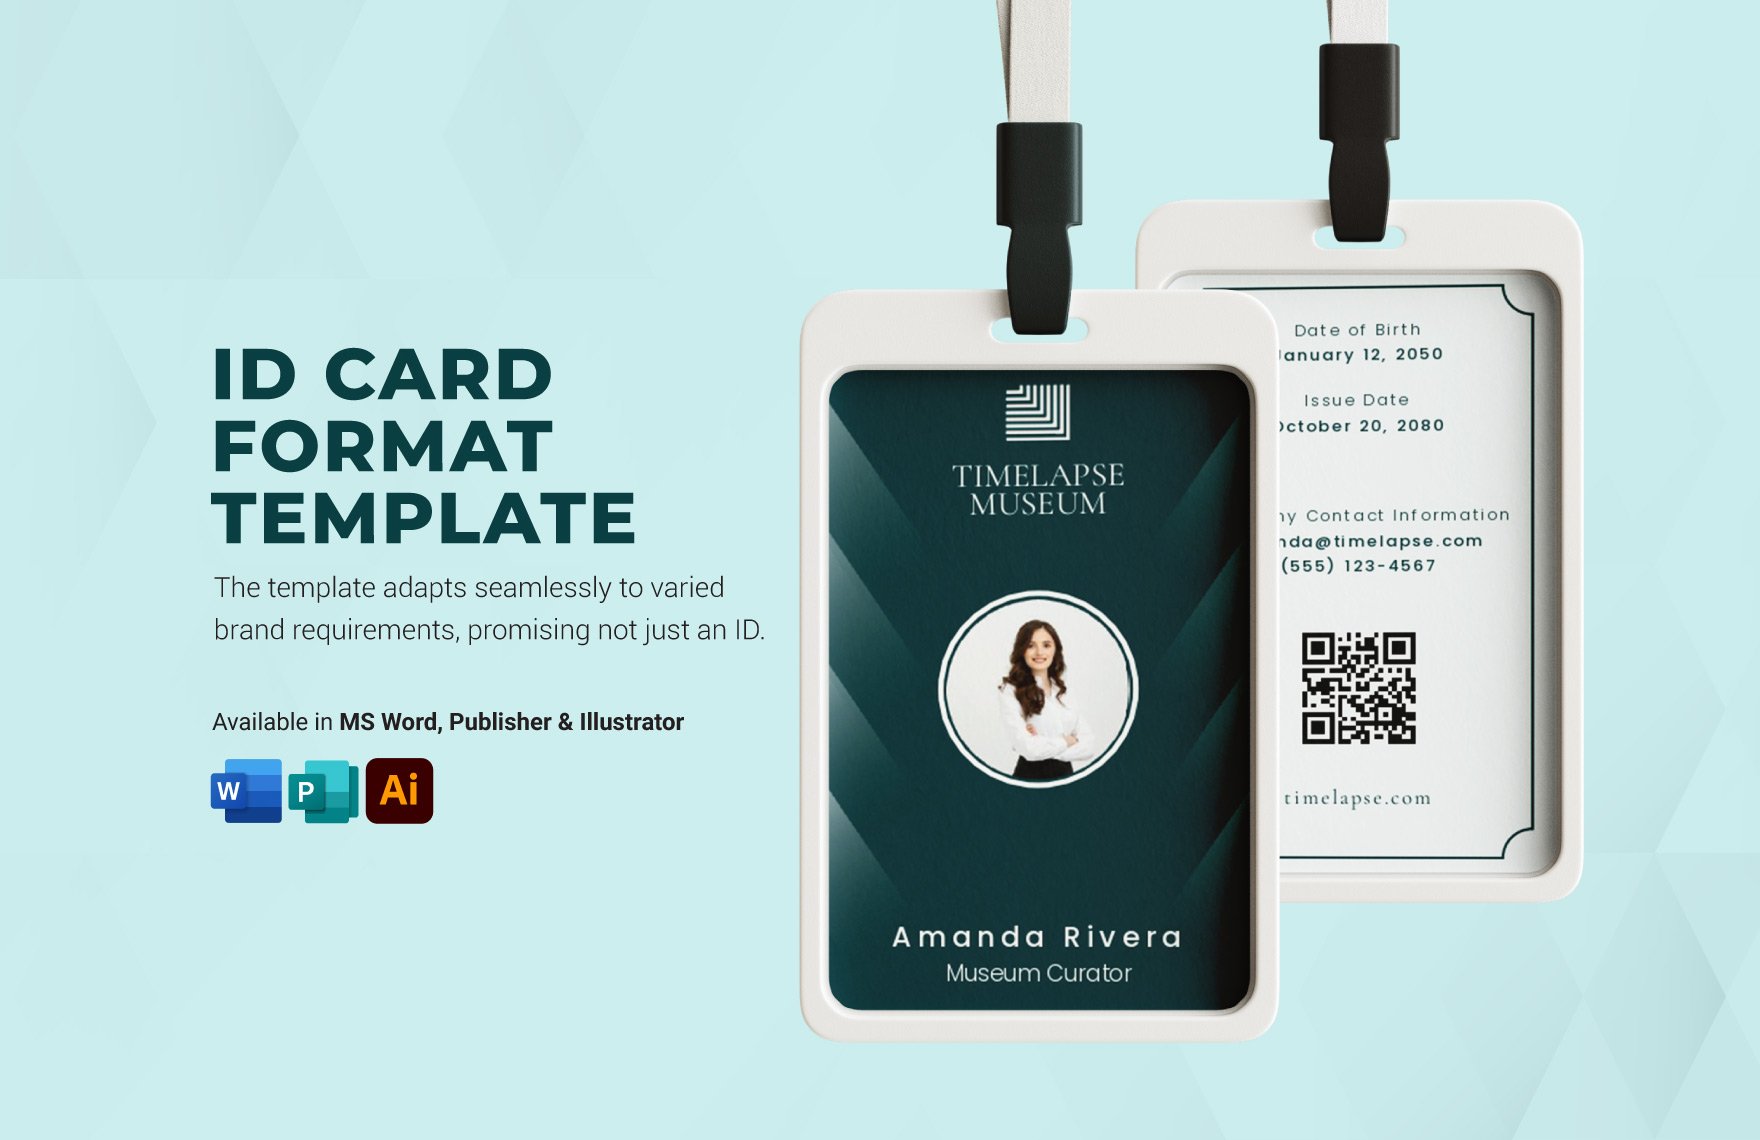
The standard ID card layout usually runs 85.6mm by 54mm — that's the ISO/IEC 7810 ID-1 size, the same dimensions as a credit card. Most people design these in tools like Adobe Illustrator, Canva, or sometimes even PowerPoint if they're just doing something basic. The card is typically split into a front side and a back side. Front side has your photo, name, ID number, maybe a barcode or QR code. Back side has the magnetic stripe, signature panel, and sometimes a secondary barcode or hologram. I've spent years working with identity document production for municipal offices and corporate HR departments. Here's the thing nobody tells you: the most common failure point isn't the design. It's the printing substrate and the lamination process. I once had a client who spent three weeks perfecting a design in full CMYK, sending it to a printer, and getting back cards that looked washed out and slightly warped. The problem was they'd chosen a PVC substrate with a glossy finish but were using a dye-sublimation printer calibrated for matte polyester. The colors shifted about 15-20% across the spectrum. We fixed it by matching the ICC profile to the exact printer-ribbon-substrate combination and recalibrating the color separation. That cost us about four hours and probably saved them twenty grand in reprinting.
Unlocking The Power Of Id Card Sample Format Your Ultimate Guide
To build a proper ID card from a sample format, you need to understand a few key layers. First, there's the base card stock. Polycarbonate cards are the gold standard for government and high-security use. They're welded together, not printed on, which makes them nearly impossible to alter. PVC cards are cheaper and good for temporary access badges or internal use. PET-G sits somewhere in between. If you're doing something that needs to survive a few years of daily carry, PVC will start to yellow and warp after about eighteen to twenty-four months in normal conditions. Second layer is the print method. Dye-sublimation is the most common for full-color cards. The ribbon transfers ink into the card surface under heat. It's decent quality but limited to about 300 DPI effective resolution. If you're printing fine text or small QR codes, this can get fuzzy. Thermal transfer works better for text and barcodes but doesn't handle photographs well. Inkjet card printers exist but they're mostly for prototyping, not production runs. Laser printers are out entirely for card stock unless you're feeding blank media through a modified machine, which is a whole other headache. Here's a counter-intuitive point that will save you a lot of trouble: design for bleed from the start. Most sample templates you'll find online don't account for the fact that the laminating overlay needs to extend past the edge of the printed layer. If your design goes right to the edge without a bleed margin, the lamination film will show a thin white line around the perimeter after curing. Standard bleed is 3mm beyond the card edge on all sides. I've seen at least five separate projects where the entire print run was rejected because someone used a template without bleed allowances. Adding the bleed after the fact is possible but it eats into your safe zone and can crop important elements.
The back of the card deserves more attention than it gets. Magnetic stripes — specifically HiCo stripes — are the workhorse for data encoding. They hold about 2,400 to 4,200 bits per inch depending on the format. Track 1 carries the primary account number and name, Track 2 is mostly the number and some discretionary data, and Track 3 exists in theory but rarely gets used in practice. If you're encoding data, make sure your reader hardware supports the format you're writing. I ran into a situation where we encoded Track 1 in a proprietary format and the existing readers at two facility entrances couldn't parse it. We ended up having to re-encode every card twice because the readers only handled standard ANSI MCRA format on Track 1. For QR codes and barcodes, the error correction level matters more than most people realize. If you're embedding a QR code that links to a verification page or database record, use at least Q-level error correction. Lower levels mean the code is fragile — a small scratch or scuff on the card can make it unreadable. Industrial QR scanners tolerate damage better than phone cameras, but your card needs to work with whatever reader is actually being used. I tested a batch of cards with 256-byte QR codes at L-level error correction and about 18 percent of them failed when read through standard smartphone cameras after just a week of handling. Bumping to Q-level dropped the failure rate to under 2 percent. Photographs on ID cards have their own set of problems. The lighting needs to be flat and even — no harsh shadows or blown-out highlights. A ring light or softbox setup works. The background should be a consistent light color, usually white or light blue depending on the jurisdiction's requirements. Face recognition software, if you're integrating that, needs the subject centered with both ears visible and a neutral expression. Cards that get rejected for photo issues are usually rejected because of uneven lighting creating shadows under the chin or nose bridge, which throws off the facial geometry that the algorithm uses for matching.
Get the Full Details

One more thing that catches people off guard: font selection and sizing. Don't use decorative or script fonts for any field that needs to be readable at a glance. ID card text is typically scanned by both humans and machines. Stick to sans-serif typefaces like Helvetica, Arial, or Univers. Name should be at least 11pt. ID numbers should be at least 9pt and ideally monospaced so each digit aligns cleanly. If you're including a barcode, the human-readable number beneath it needs to match the encoded data exactly — character for character. I've caught three separate instances where a font rendering issue caused the number 1 to look like the letter l, and the scanner read it wrong because the KERNING wasn't set properly. Security features aren't optional if this card is going to function as a legitimate credential. Overt features include holographic overlays, microprinting that's visible under magnification, UV-reactive ink, and color-shifting inks. Covert features are embedded in the substrate during manufacturing and require specific readers to verify. If you're producing cards for an organization that needs tamper resistance, polycarbonate cards with laser engraving are the baseline. The data gets etched directly into the card layers, which means anything printed on top can be removed but the underlying data remains visible. This is standard for passports and national ID cards. If you're looking for sample formats to start from, most card printer manufacturers offer downloadable templates. Magicard, Evolis, and Fargo all have design portals with pre-sized PSD and AI files. Some municipalities publish their ID card specifications publicly. The tricky part is adapting those templates to your specific needs without breaking the alignment of pre-printed elements like borders and security zones. I usually import the manufacturer's template into Illustrator, duplicate the lock layer, and build my design on top while keeping the original template hidden underneath as a reference. This way if something goes out of alignment, I can check it against the original spec.
Testing is where most people cut corners. Before you commit to a full print run, produce a test batch of at least ten cards covering every variation in your design — different photos, different text lengths, different barcode content. Run them through the actual readers, scanners, and lamination equipment you'll be using in production. Check that the magnetic stripe encodes correctly on your specific writer. Verify that QR codes scan cleanly from multiple angles. Inspect the lamination for air bubbles or misalignment. This testing phase usually adds one to two days to your timeline but prevents the kind of costly recalls that happen when you discover a flaw after printing five thousand cards.
Where This Approach Falls Short
ID card production using sample formats isn't a perfect solution. The biggest limitation is that template-based design restricts you to the dimensions and zones that the template author anticipated. If you need a non-standard layout — say, a larger photo area or an additional data field — you'll be working against the template rather than with it. In those cases, starting from a blank canvas with the ISO dimensions and building your own layout from scratch is often faster in the long run, even though it requires more upfront work. Another issue is the cost of quality. A decent dye-sublimation card printer runs anywhere from two thousand to eight thousand dollars depending on the model and throughput. The ribbons and blank cards add up quickly — expect to spend about fifty to one hundred cents per card in consumables for mid-range quality, or two to four dollars per card for polycarbonate and high-security options. If you're only producing fifty or sixty cards per year, the equipment cost alone may not justify the investment and you'd be better off outsourcing to a professional card production service. The learning curve for color calibration alone can take a full day of trial and error. ICC profiles vary by printer, ribbon batch, and card substrate, and even slight changes in ambient temperature can shift the output. If you're doing this as a one-off project, the time spent getting the colors right might outweigh the benefit of in-house production compared to sending the job out to a shop that already has their profiles dialed in.
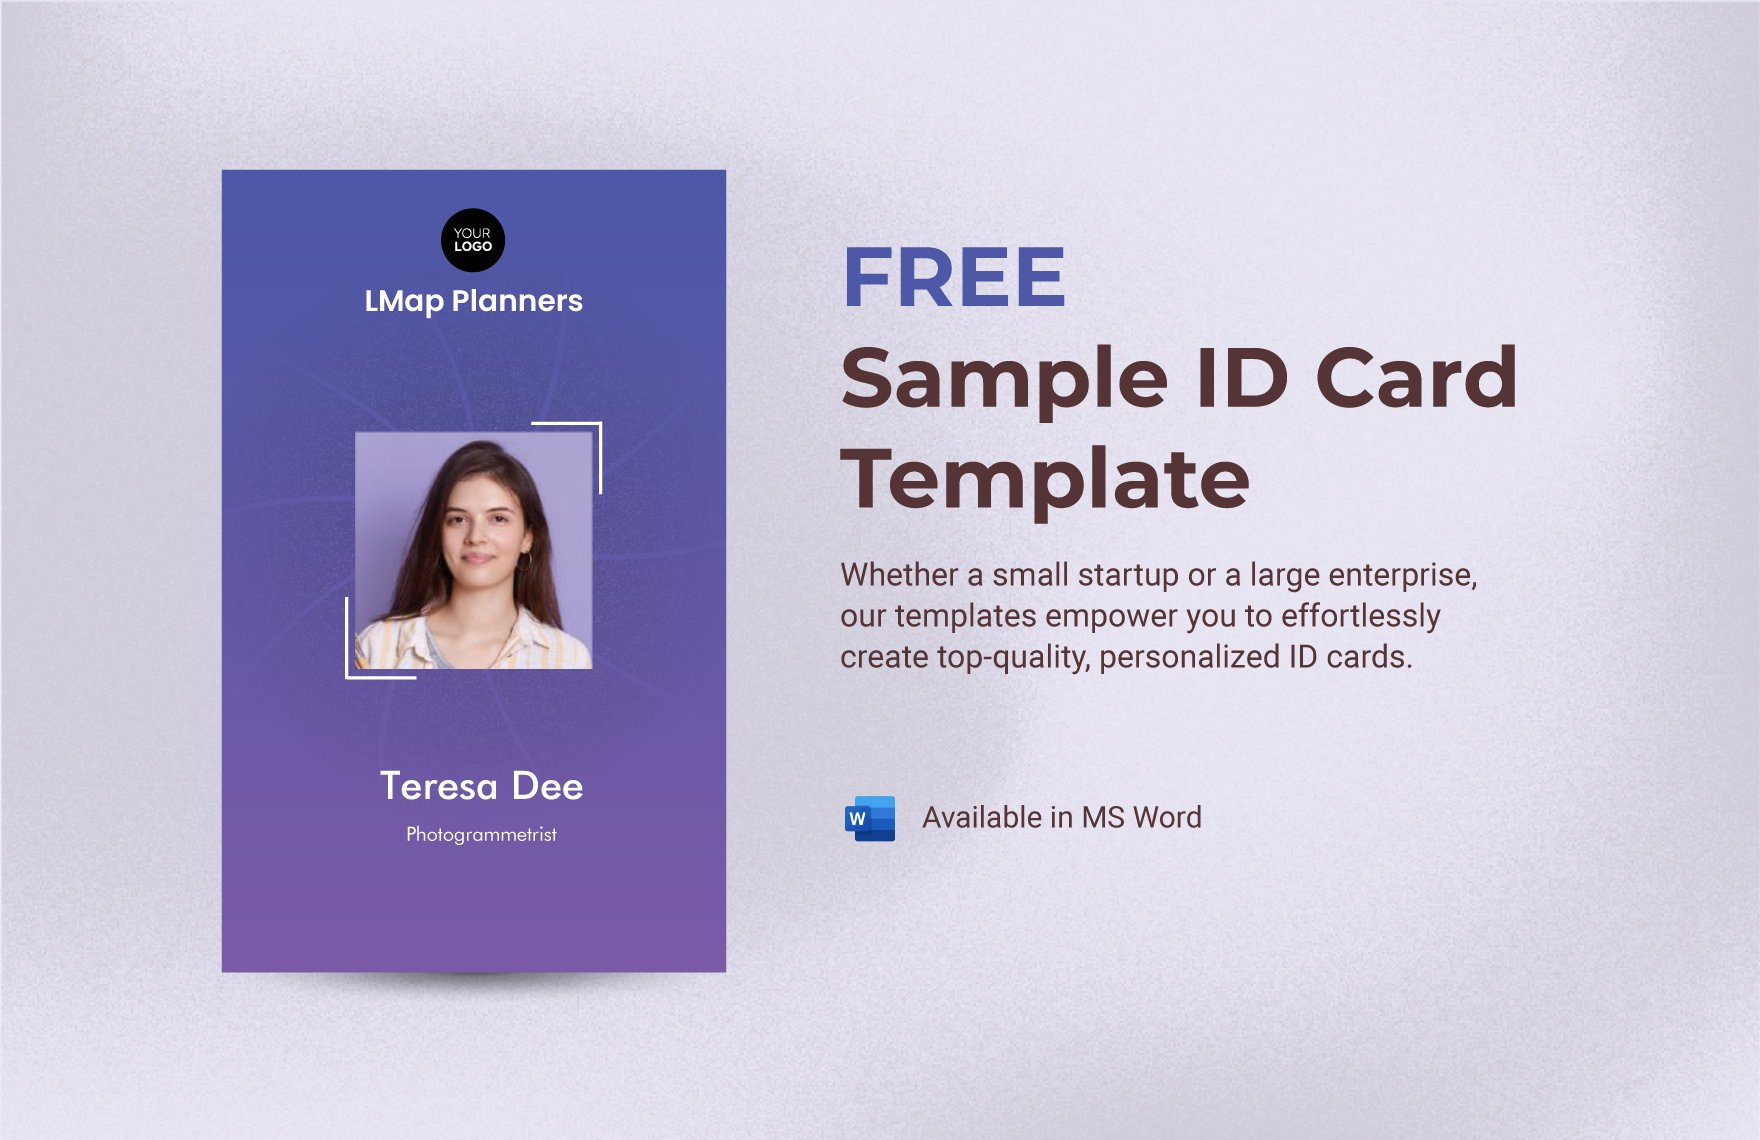
Ultimately, sample format templates are a solid starting point if you understand what they can and can't do for you. They give you the structure, the bleed margins, the zone markers, and the general layout logic. What they don't give you is an understanding of the production chain — how the design choices you make will actually behave when they hit the printer, the encoder, and the laminator. That knowledge comes from running into problems and fixing them. The guide I just laid out is basically a compilation of the problems I ran into and what I did about them. Use it as a reference, not a substitute for testing your own setup before committing to production.