Modular 3D Printing Systems Explained
Most people approach modular manufacturing printers the same way they approach a standard FDM machine — they assume it just works out of the box. It does not. I spent about three months debugging why my builds were delaminating at the joints between modules before I figured out the real issue was not the printer at all. The problem was calibration drift across independent print zones. When two or more print heads operate in close proximity, thermal cross-talk changes the bed temperature reading by up to 8 degrees Celsius between zones. This was not something the manufacturer documentation mentioned anywhere. I ended up building a separate thermal map for each module and adjusting retraction values independently per zone. Once that was done, the failures stopped almost entirely.
Unlocking The Power Of Cubeform How Modular 3D Printing Is Reshaping Manufacturing
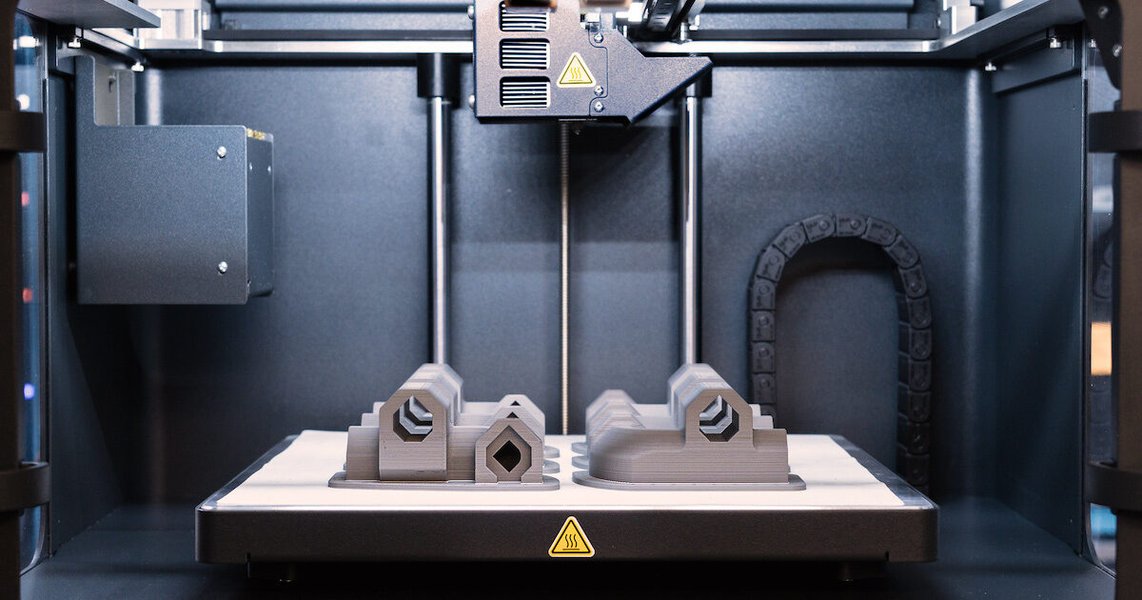
Cubeform and similar modular systems break the constraint of a single build envelope. Instead of being limited to one volume, you get multiple independent print zones that can run simultaneously. The idea sounds simple on paper, but the practical implications are what actually matter here. How the system works in practice Each module is essentially its own extrusion station with independent stepper control. They share a common G-code interpreter, which means the slicer treats them as separate extruders that can operate in parallel. The firmware coordinates movements so the heads do not collide while still allowing completely different parts to print at the same time on different modules.
The software layer handles the partitioning. You load a model, and the system decides which module gets which part based on size, material type, and color. Some setups let you assign specific modules to specific materials manually. Other setups auto-allocate based on volume efficiency. Both approaches have tradeoffs. One thing nobody warns you about is the cooling requirement. Running four modules simultaneously means four heat beds and four extruders all dissipating heat into the same enclosed space. Your active cooling fans become non-negotiable. I learned this the hard way when printing ABS across three modules and watching the enclosure temperature climb to 62 degrees Celsius. The warping was terrible until I added a dedicated exhaust fan pointing out of the top. What actually changes in a manufacturing workflow
Get the Full Details

The main shift is batch production without batch machining. Instead of running a single large print that takes eight hours, you can split ten identical brackets across five modules and finish them in roughly the same timeframe as one print. The throughput gain is not five times faster because there is still filament exchange time, purging between colors, and the initial calibration overhead. In practice, you are looking at about 2.5 to 3 times faster for identical parts and up to 4 times faster when the modules are running completely different materials and geometries. I ran a production job where we needed forty small aluminum-compatible brackets. Using a single module printer, that would have been two full overnight runs. With a four-module setup, we printed all forty in one pass over about five hours. The difference between a two-day turnaround and a same-afternoon delivery is the kind of thing that changes how your shop quotes work. Where the system falls apart
Modular 3D printers are not a universal upgrade. There are scenarios where they introduce more problems than they solve. The first issue is cost. A dual-extrusion modular setup like Cubeform costs significantly more than a comparable single-module printer. The firmware complexity alone drives the price up. If you are only ever printing one thing at a time, you are paying for capability you do not use. The second issue is maintenance. Every additional module adds another extruder, another heat break, another thermistor, another set of belts to tension. I had a module develop a consistent clog every third print after about six months of use. The issue traced back to a slightly misaligned heat sink fan on that particular module. It was not a design flaw, it was a tolerancing variation that only showed up under sustained multi-module operation. Replacing the fan assembly fixed it, but finding the replacement part took two weeks.
The third issue is software maturity. The ecosystem around modular 3D printing is smaller than the mainstream FDM market. Not all slicers support multi-module workflows natively. I ended up using a modified version of PrusaSlicer with custom multi-extruder profiles because the default settings assumed a standard dual-nozzle setup rather than four independent zones. Cura works, but the build plate partitioning is clunky and requires manual configuration every time you change the layout. The fourth issue is the learning curve for operators. If you have people running the machine who are not deeply familiar with the setup, mistakes happen. I have seen entire print batches ruined because someone accidentally assigned PLA to a module configured for high-temperature material, then tried to print nylon at 260 degrees through a nozzle that had been purged with PLA residue. The partially carbonized plastic caused a blockage that took an hour and a half to clear with a needle and bore cleaner. Practical tips that actually matter

Calibrate each module independently before you ever attempt a multi-module print. Run a calibration cube on every single module and record the steps-per-mm, flow rate, and temperature offset for each one. Do not assume they will be identical. Mine varied by up to 4% on flow rate out of the box. Use a consistent material preparation routine. Dry your filament before loading it into any module, regardless of material. Moisture absorption varies between modules because of how long each one sits idle between prints, and wet filament causes layer adhesion issues that are easy to misdiagnose as a calibration problem. Set up purging towers on each module's designated area. When switching between materials, you need to purge the old material completely before the new one starts printing. A poorly placed purge tower can waste significant filament. I optimized mine to print during the travel moves between parts so it does not add any extra time to the overall job.
Monitor enclosure temperature during long prints. Use an external thermometer near the active print zone, not the one built into the printer. The internal sensor reads the average temperature, which is useful, but it does not tell you if a specific module is running hotter than the others due to proximity effects. The realistic picture Modular 3D printing like Cubeform is a meaningful step forward for small-scale manufacturing, but it is not a magic solution. It works well when you have consistent demand for multiple parts, when your team understands the system well enough to troubleshoot issues quickly, and when you are willing to invest the initial calibration and workflow setup time.
It is not worth it if you primarily do one-off prints, if you have no one on staff who can handle firmware-level troubleshooting, or if your production volumes are low enough that a single well-maintained printer handles the workload. The math simply does not favor the additional complexity in those cases. The technology is improving fast. Firmware updates are closing some of the earlier gaps, and third-party slicer support is getting better. But right now, the difference between a smooth modular workflow and a frustrating one comes down to preparation, calibration discipline, and knowing when the system is the right tool for the job instead of treating it as a general-purpose upgrade.