
Modular Construction Doesn't Fix Bad Planning
I spent three years trying to convince myself that modular construction was going to solve project delays, budget overruns, and coordination headaches. It did not. What it actually does is shift where those problems show up. You trade on-site delays for factory scheduling conflicts. You trade labor shortages for supply chain fragility. But when it works, it works differently than conventional building ever does, and that difference matters. The reason most people approach modular incorrectly is they treat it like a product instead of a process. You cannot order modules like you order doors or HVAC units. The design has to be locked before any fabrication starts, and locking that design requires decisions most teams are not prepared to make early enough. I learned this the hard way on a mid-rise residential project where we had to redesign three module types mid-fabrication because the MEP risers did not align with the transportation envelope. That cost us four weeks and roughly $180,000 in rework and storage fees.
Unlocking The Potential Of UNT BLB Building Unleashing Creativity And Efficiency With Modular Construction
UNT BLB, or the University of North Texas Building Lab framework, approaches modular construction as a design and fabrication methodology rather than just a delivery method. The core idea is straightforward: standardize the connections, allow variability in the modules themselves, and let the factory do what it does best while the site crew handles only the final assembly. This is different from the typical panelized or volumetric modular approach because the BLB system prioritizes adaptable grid systems and interoperable connector details over fixed module dimensions. Here is how the process actually unfolds when you do it right. First you establish a structural grid and connection logic. UNT's framework typically uses a 4-foot by 8-foot base module that scales up through nesting. The connector details are designed to handle lateral loads, vertical loads, and utility passages through a single interface point. This means each module does not need its own separate structural framing at the connection edges, which reduces material usage and speeds up assembly significantly. I worked through the details on a campus project that used this system. We started with a 16-foot by 48-foot module that contained a full bathroom stack, a kitchenette, and structural framing for a second floor. The connecting interface used a steel plate with integrated conduit channels and bolted flange connections. What surprised me was how much design freedom we retained. The exterior cladding, interior finishes, and window placements varied between modules without requiring new connection details. The standardization was in the system, not in the module appearance.
Where This Actually Saves Time And Money
Factory fabrication typically runs 30 to 50 percent faster than equivalent on-site construction for repeatable units. That is not a theoretical number. On a project with 48 identical bathroom modules, we saw the factory complete them in six weeks while the same work would have taken fourteen weeks on-site with traditional methods. The labor distribution is fundamentally different. Factory workers stay in one place with fixed tooling. Site workers move from trade to trade as each building progresses through phases. But the time savings compound. While modules fabricate, site work continues simultaneously. Foundation, utilities, and slab work proceed in parallel with fabrication. For a typical four-story building, this parallel work can reduce the overall project schedule by eight to twelve weeks compared to conventional construction. That is significant when you are carrying construction loans and facing soft cost exposure. Quality control improves because factory conditions are controllable. Weather delays, material moisture issues, and subcontractor scheduling conflicts largely disappear from the module fabrication phase. I have seen concrete pours in a factory setting that would have been impossible on a congested urban site. Temperature-controlled environments mean curing compounds work properly, and inspection happens at every station rather than at scheduled milestones.
Get the Full Details
What Nobody Tells You About Transportation
Module transportation is the single most misunderstood aspect of modular construction. People assume you ship modules the way you ship containers. You cannot. The dimensions, weight, and road restrictions of your project location dictate what modules you can build and how many pieces you need to split them into. In Texas, where UNT operates, oversize load permits and escort vehicles are routine, but they add cost and schedule risk. A standard module wider than 16 feet requires special permits, route surveys, and sometimes utility line adjustments. I learned this when our initial module design at 18 feet wide kept getting delayed by TxDOT permit processing. We redesigned to 16 feet, accepted a seam in the ceiling plane, and cut our permit timeline from three weeks to five days. Storage at the site is another constraint most teams overlook. Modules arrive before the building is ready to receive them. You need a staging area that can handle loaded trailers, crane access, and temporary storage without damaging the modules. On a tight urban site, we rented a parking lot two blocks away and used a shuttle system to move modules to the crane zone as needed. This added about $40,000 to the project but prevented a scheduling catastrophe when the foundation work ran two weeks behind.
Design Decisions That Make Or Break Modular Projects
The most counter-intuitive thing about modular construction is that it requires more design development upfront, not less. Conventional construction allows you to sort things out as you go. Modular construction requires nearly 100 percent design completion before fabrication begins because every change order in the factory costs ten times what it would cost on site. Coordination between disciplines becomes critical during the design phase. Structural, mechanical, electrical, and plumbing teams must resolve every intersection before the module drawings go to fabrication. I used a BIM coordination process with weekly clash detection reviews. This caught approximately 200 conflicts before they became expensive field problems. The cost of that coordination was maybe $25,000 in additional design fees. The cost of resolving those same conflicts in the factory would have been closer to $200,000. Another thing people miss is that modular construction changes how you specify materials. Some finishes that work fine on-site do not survive transportation and handling. I learned this with a premium vinyl flooring installation. Three out of forty modules had edge damage severe enough to require complete floor replacement. After that, we switched to luxury vinyl plank with glued edges and added protective corner blocks to every module shipment. The material cost increase was maybe eight percent. The damage rate dropped to near zero.
When Modular Construction Is The Wrong Choice
Modular construction fails in several scenarios, and being honest about those failures matters more than any sales pitch you will hear. Projects with highly unique architectural forms struggle with modular approaches. If every module needs to be different, you lose the fabrication efficiency that makes modular attractive. The factory becomes a custom shop, and the cost advantage disappears. Remote sites present their own challenges. Transportation costs scale with distance, and at some point the factory-to-site haul becomes prohibitively expensive. I worked on a project in West Texas where the module transport cost exceeded the fabrication savings for certain unit types. We switched to panelized construction for those modules, which gave us about 60 percent of the schedule benefit at significantly lower transportation costs. Financing structures also matter. Modular construction requires different lending approaches than conventional construction. Some lenders understand the factory-to-site process. Many do not. I have seen projects delayed for months while lenders figured out how to release draws for off-site fabrication. This is not a modular problem. It is a financial institution adaptation problem, but it is a real problem that can kill a project if you are not prepared for it.

Practical Steps To Start A Modular Project
If you are considering modular construction, start with the site. Can you accommodate module delivery and crane operations? Is there adequate staging area? What are the road restrictions for your module sizes? Answer these questions before you answer anything about architecture or aesthetics. Next, identify the module types that will repeat. The more repetition you have, the better modular construction performs. A hotel with identical guest rooms is ideal. A museum with unique gallery spaces is not. Be honest about your project type and whether it fits the methodology. Then find a factory with capacity for your project timeline. I cannot stress this enough. Factory schedules fill up quickly, and many teams underbid factory lead times by six to twelve months. A factory that says they can start your modules in eight weeks probably means eight weeks from contract signing to first piece production, not from your project start date.
The UNT BLB framework provides specific design documentation standards and connector specifications that you can reference. Their published materials cover grid systems, connection details, and quality assurance procedures. Working within an established framework reduces the risk of developing your own system from scratch, which is where most first-time modular teams make costly mistakes.
Field Assembly Realities
Once modules arrive on site, the assembly process is faster than conventional construction but requires precise coordination. Crane operations, module placement, and connection sequence must follow a strict plan. Deviations in the field create structural complications that are expensive to correct. We used a module sequencing matrix that coordinated delivery order with crane positioning and connection sequence. Each module had a designated location, a scheduled arrival window, and a required connection sequence. This matrix prevented the chaos that occurs when modules arrive out of order and the crane is idle waiting for the next piece. Connections between modules require careful attention to weather sealing and utility integration. The interface between two modules is where most waterproofing failures occur. I have seen improperly sealed module joints leak after the first significant rain event. The solution is not complicated. It requires proper gasket installation,torqued bolt sequences, and inspector sign-off before the next module is set. But contractors often rush this process because the overall assembly feels fast enough.
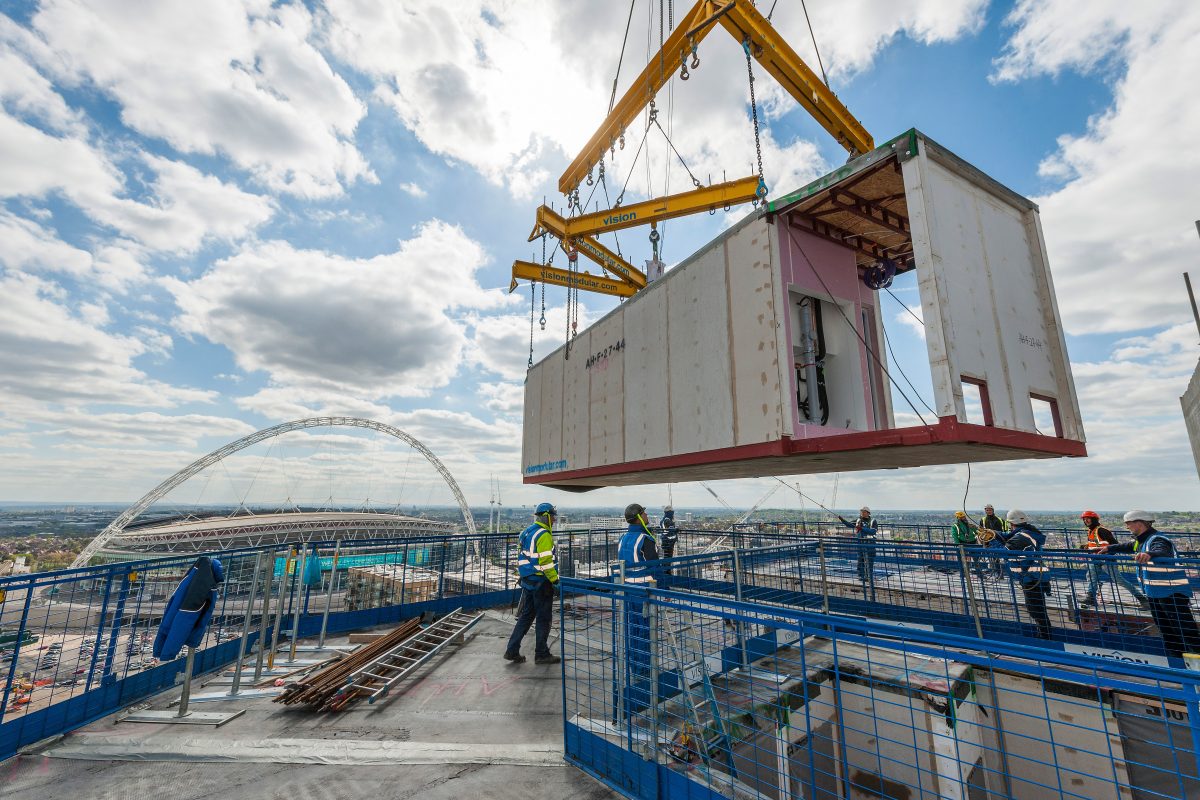
The utility connections between modules deserve particular attention. Electrical, plumbing, and HVAC interfaces between modules require pre-planned routing through the connector system. Field modifications to these systems are difficult and expensive. We ran every utility line through the pre-designed channels in the connector plates. When we had an unexpected field condition, we addressed it with a engineered field modification rather than a quick fix, which cost more upfront but avoided repair calls months later. Modular construction is not a magic solution for every project. It is a different set of trade-offs that favor repetition, planning, and factory discipline over flexibility and on-site adaptability. When your project aligns with those advantages, the results are genuinely impressive. When they do not, you are better off with conventional methods. The key is understanding which category your project falls into before you commit to either approach.


