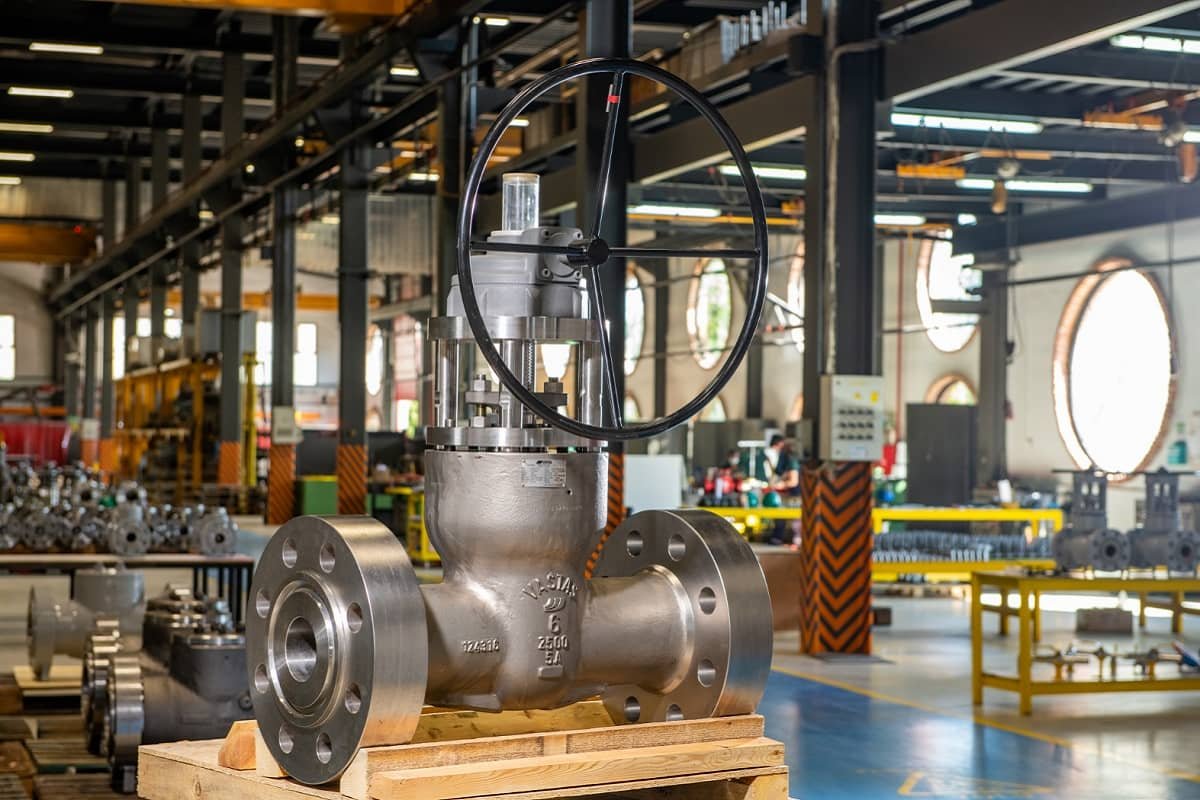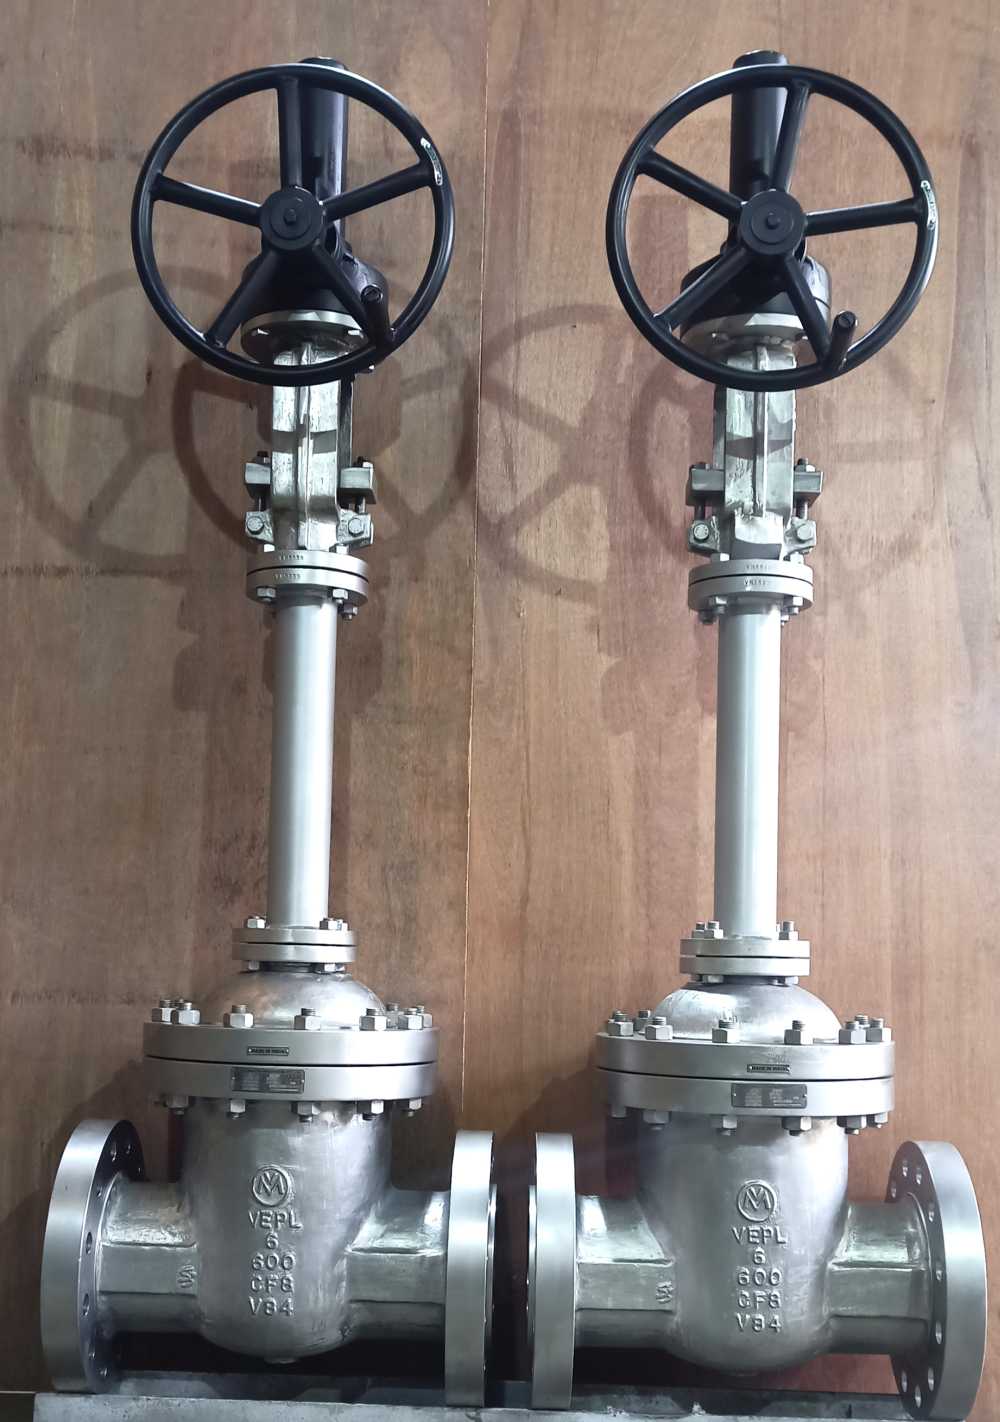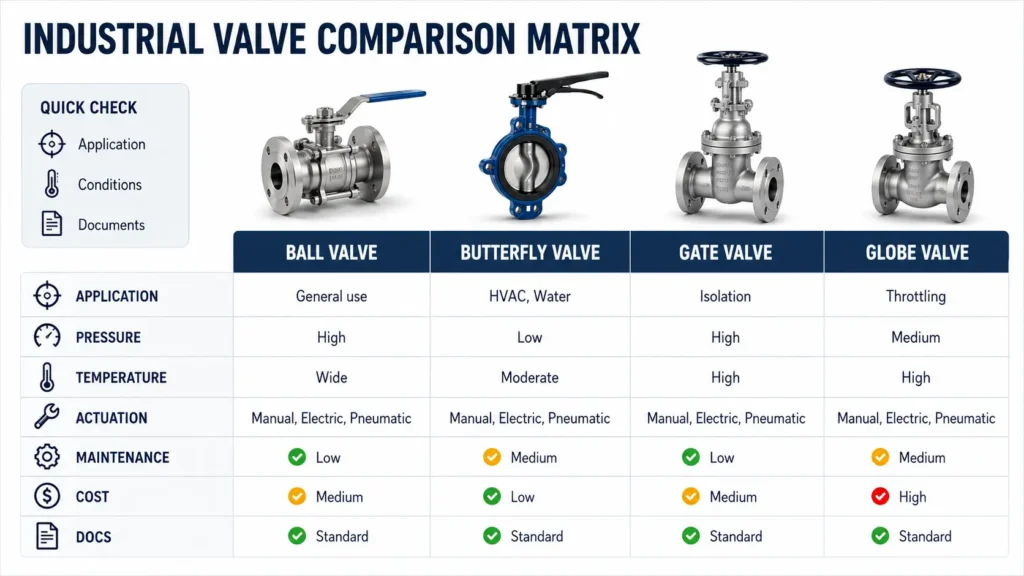
Gate Valves in Pune: What Actually Matters
Pune has grown into one of the larger industrial clusters for valve manufacturing in western India. If you are sourcing gate valves there, you will find anywhere from small family-run foundries to ISO-certified plants that export to the Middle East and Africa. The problem is not that the options are scarce. The problem is figuring out which ones are worth your time and which are just a glossy brochure with a GST number. I have spent more years than I would like to admit chasing down valve suppliers in the Ranjangaon MIDC and Peimpri areas. Here is what I actually look at, not what the catalogs say. Most legitimate gate valve manufacturers in Pune cluster around a few industrial zones. Ranjangaon MIDC on the Ahmednagar road has a concentration of foundries and machining shops. Peimpri near Talegaon has a mix of small and mid-size plants. Chakan and Talawade in the Pune-Nashik corridor have newer facilities, some of which are actually backed by capital investment rather than just a showroom in Katraj.
If someone tells you their factory is in Pune but the address is a residential society in Wakad or Baner, move on. That is a trading company dressed up as a manufacturer. The valves will still work, but you are paying a middleman margin and you have no traceability into who actually cast the body.
What to Check Before You Commit
I do not care about your minimum order quantity until I know you can back it up. The first thing I ask is for a current ISO 9001 certificate with the exact facility address, and I cross-check it on the QCI website. Some suppliers produce stale certificates that expired eighteen months ago. The audit report inside should mention pressure testing and material traceability. If it only says "quality management system," that is a red flag. Next is the material certification. For a standard cast steel gate valve, I want to see a mill test certificate that matches the actual heat numbers on the valves. I once rejected a batch of WCB gate valves because the MTC listed 450 pieces but the valves on the forklift had only 380 cast into them. The remaining seventy were from a different foundry. The supplier said it was "within tolerance." It was not. Material traceability is not a suggestion when you are dealing with steam lines.
Get the Full Details
Common Pitfalls Specific to Pune Suppliers
The casting quality varies a lot across small foundries in the region. Some operate single-pit sand casting lines with no spectrometer for incoming charge verification. That means two batches from the same vendor can have different carbon equivalents. If you are ordering SS316 or WC6 valves for high temperature service, ask for a chemical analysis report from an independent lab like TUV or SGS, not the vendor's own internal report. I learned this the hard way on a project in Satara where a WC6 gate valve cracked at the neck during hydrotest at 1.5 times design pressure. The material was borderline C15A with traces of phosphorus that should have been caught. Another issue is the face-to-face dimension tolerance. Some smaller manufacturers run their end connections loose, especially on sizes above eight inch. When you install them in a skid where the piping is already spooled, you end up field-trimming flanges. That costs you more than the valve itself. Always ask for a certified dimensional report before shipment, and specify the applicable standard, whether it is API 600, ISO 5752, or BS 5351.
Price vs. Performance
Pune valve prices are competitive, but the cheapest quote is rarely the cheapest option in the long run. A gate valve quoted at twenty percent below market rate often cuts corners on the stem, uses a lower grade packing, or skips the seat soft-seat test. I recommend budgeting for a mid-range supplier that can show you actual hydrotest records and a documented warranty clause. The difference in upfront cost usually pays back within the first two maintenance cycles. I always visit the shop floor if the order is above fifty units. What matters most is whether they actually have a hydrotest bay, a spectrometer, and a dedicated inspection log book. If the inspection area is just a corner of the dispatch floor with no controlled lighting, that is a sign of poor process discipline. I also check the paint quality. A properly prepared and painted valve will show uniform coating thickness with no runs. If the paint looks like it was sprayed by someone rushing to meet a dispatch deadline, the internal machining probably got the same treatment. After the visit, I ask for three references from the last two years. Call them. Ask about after-sales response time, not just whether the valve survived installation. Most vendors will not give you references for sensitive industries like power or refinery because the track record is mixed. That tells you something.
Who to Consider
I will not name individual companies here because the landscape changes frequently and reputation is not static. What I can say is that the reliable ones share a few traits: they publish their pressure ratings clearly, they do not fight on dimensions, they provide traceable material certs, and they answer the phone when you call with a complaint. If a vendor is aggressive on price but avoids talking about testing standards, that is a data point.

The Bottom Line
Sourcing gate valves from Pune is viable if you approach it with your eyes open. The city has real manufacturing capacity, but it also has a lot of trading companies and a few underqualified foundries. Do your due diligence on paper first, then on the shop floor. Check the certificates, verify the testing equipment, and ask for material traceability. If the supplier cannot produce a heat number matched MTC on request, you have your answer without ever seeing the casting.