Why Most People Get Sandblasting Grit Wrong
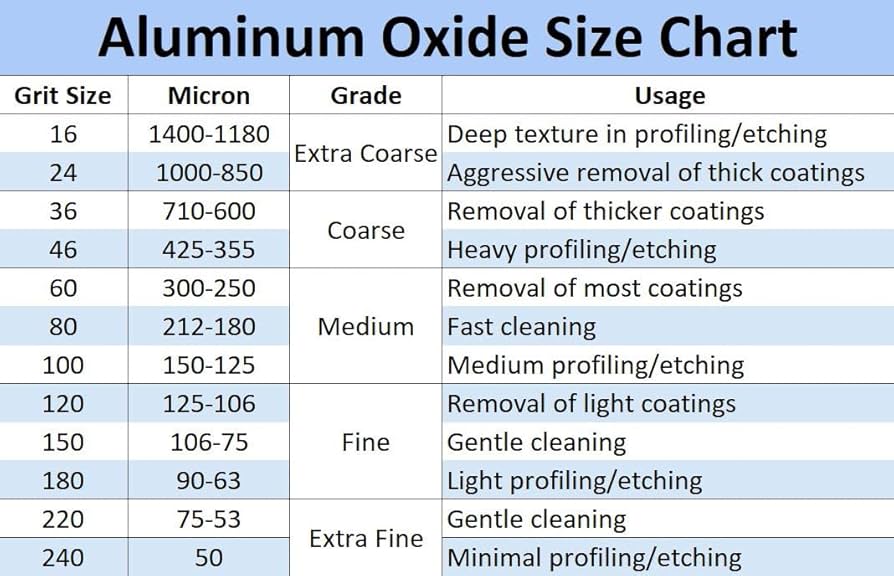
The grit size chart is the most important reference you'll keep near your blast cabinet, but it's also the most misunderstood document in surface preparation. I've watched enough people ruin good material by picking a number out of a chart without understanding what that number actually means in practice. Let me walk you through the chart properly. Grit size is measured in mesh, which is the number of openings per linear inch in a sieve screen. Higher mesh numbers mean smaller particles. That seems simple, but the relationship between mesh and actual particle diameter isn't linear and varies slightly between different abrasive manufacturers. Aluminum oxide, silica sand, crushed glass, and steel shot all have their own grit sizing standards, which is why a #80 aluminum oxide is not the same physical particle as a #80 silica sand. The standard grit sizes run from roughly #12 (coarse) up to #220 or higher (fine). Most sandblasting work sits in the #30 to #120 range. Here's what you need to know about the major ones:
#12 to #20 — These are huge. Used for stripping thick coatings, heavy rust, or concrete prep. They'll eat into bare metal fast. If you're blasting a thin sheet panel with these, you'll warp it. I learned that the hard way on a 16-gauge fender I was prepping for paint. Used #16 garnet thinking I was being efficient. By the time I had the rust off, the panel was wavy enough to rattle. Went with #60 and did it right. #30 to #50 — Workhorse range. Good for heavy mill scale removal, structural steel prep, and removing old paint from thick surfaces. This is what you want if you're doing a truck frame or a gate. The profile left behind is aggressive — about 2 to 4 mils — which is ideal for epoxy and primer adhesion on rough substrates. #60 to #80 — This is the sweet spot for most general metalworking. Stripping paint, cleaning welds, preparing surfaces for powder coating. It leaves a consistent profile around 1 to 2 mils. If you're only going to buy one abrasive, this is the range to pick from.
#100 to #120 — Fine enough for smoothing welds and preparing surfaces where a light profile is needed. Aluminum work lives here. Coarser grits will embed in soft aluminum and cause problems later. I've seen too many people use #80 on aluminum and then wonder why the finished paint developed flash rust spots six months later. Those weren't flash rust — they were grit particles working their way out of the substrate. #150 and finer — Mostly for delicate work, bluing removal on firearms, or preparing surfaces that will receive decorative finishes. Not for structural prep.
Get the Full Details
What The Grit Chart Doesn't Tell You
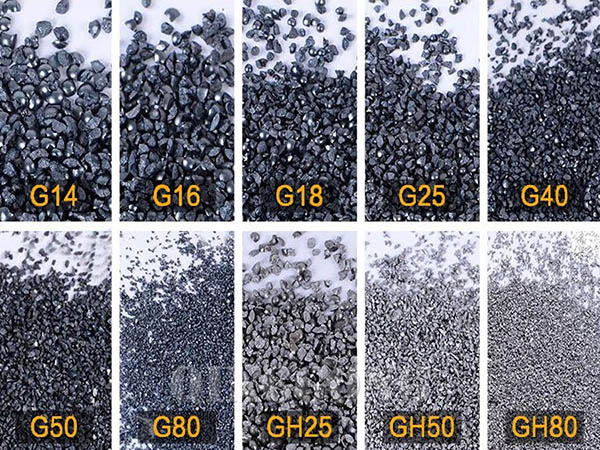
A grit size chart gives you particle diameter in microns and mils, but it says nothing about hardness, shape, or cutting speed. Two abrasives with the same mesh rating can perform completely differently. Garnet is angular and cuts fast but breaks down into fine dust. Crushed glass is sharper than garnet and lasts longer before fracturing. Steel shot is spherical — it peens the surface rather than cutting it, which means it won't remove tight-bonded coatings as effectively but will produce a smoother finish. The Mohs hardness scale matters more than most people realize. Quartz sand has a hardness of about 7. Steel substrate is roughly 4 to 5 on that scale. That's why silica sand works for cleaning steel — the abrasive is harder than the material you're trying to remove. But if you're working with softer metals like aluminum or brass, a hard angular abrasive like aluminum oxide will cut deeper and faster than you might expect. Soft abrasives like walnut shell won't damage the base metal, which is why they're used for cleaning without etching. Here's something the charts don't cover: moisture kills grit. Wet sand or damp abrasive clumps inside your blast pot and ruins your nozzle flow. I had a job once where the humidity hit 90 percent and my #80 silica just turned into sludge in the feed line. We ended up switching to a dry air setup with a moisture trap on the compressor and buying desiccant-grade storage containers for the media. Took me two days to figure out the moisture trap was the actual bottleneck — not the grit itself.
Choosing The Right Grit For Your Application
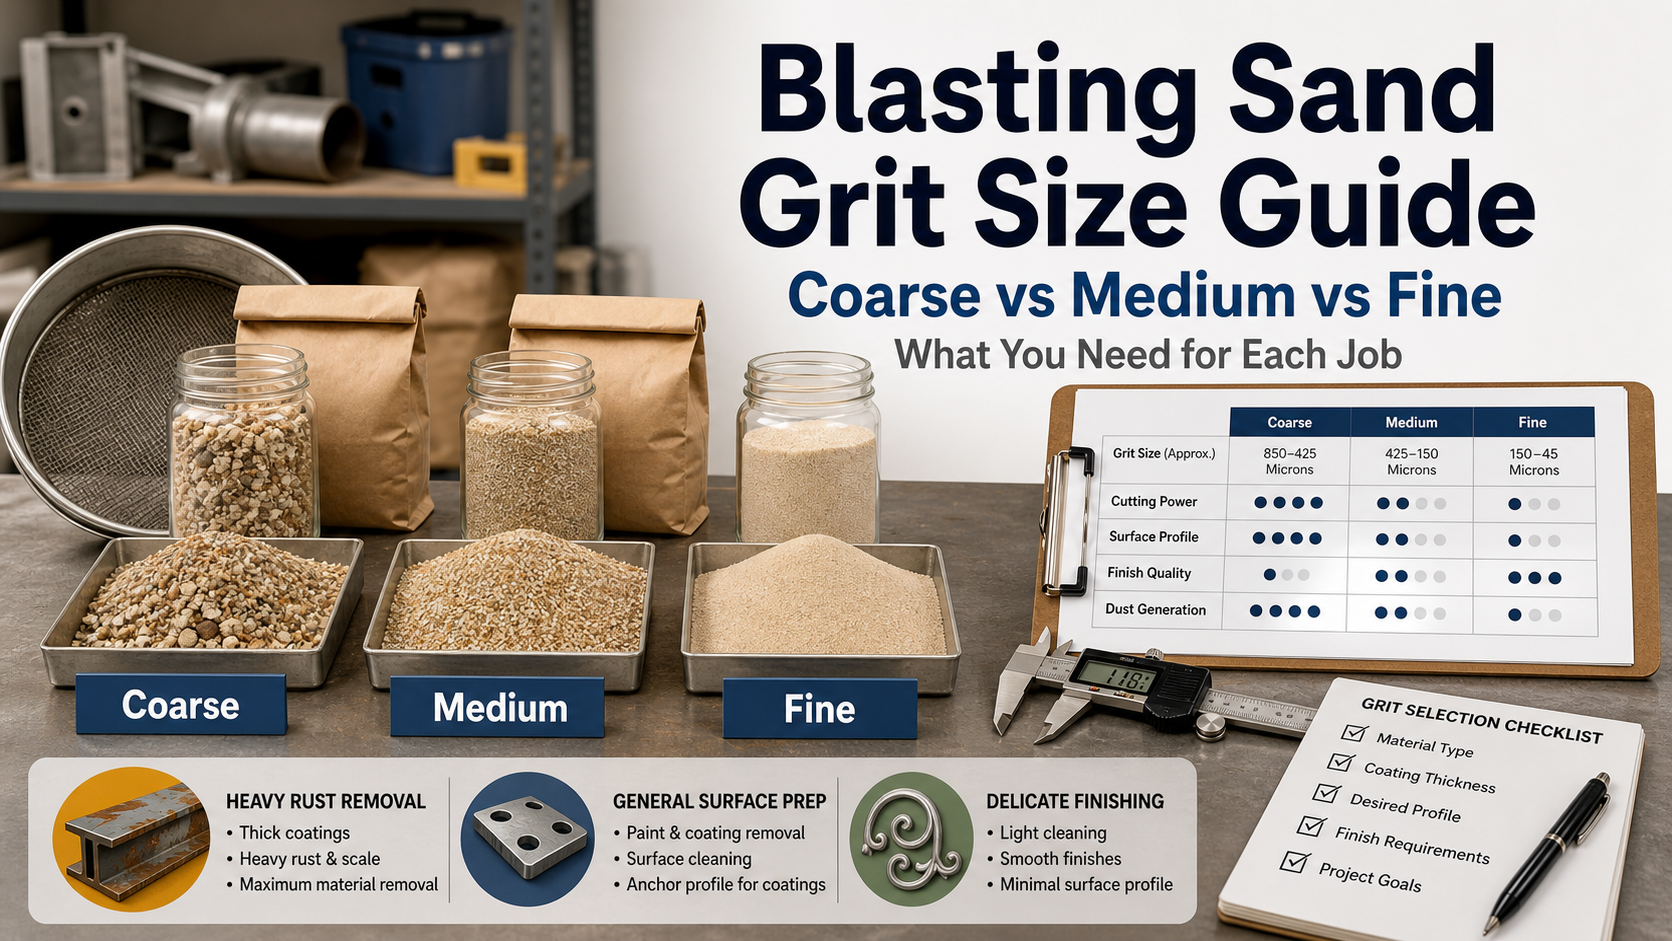
Strip thick paint or heavy rust from steel — #36 to #50 aluminum oxide or garnet. This will take about 3 to 5 minutes per square foot on a typical sandblaster setup at 90 to 100 PSI. A rotary bell cup at the same pressure does the same job in under a minute. Clean and prep for painting — #60 to #80. This is the default recommendation for a reason. It gives you a good anchor profile without over-cutting. Remove rust from delicate parts — #100 to #120 aluminum oxide or crushed glass. Softer on the base metal while still removing oxidation.
Prepare aluminum — #100 to #120. Never go coarser than #80 unless you're doing structural prep and don't care about surface smoothness. Embedding and galling are real problems with aluminum. Remove bluing from steel — #150 to #220 glass beads or plastic media. Whatever you do, don't use angular grit if you're just trying to remove a finish. You'll alter the dimensions of small parts.
Common Mistakes That Cost You Time And Money
Using the same grit for every job is the biggest waste I see. Some people load up their pot with whatever they have on hand and blast away. That might save you five minutes of setup but will cost you an hour in rework. If the profile is too deep for the primer you're applying, the primer won't bridge the valleys and you'll get premature failure. If the profile is too shallow, the coating doesn't have anything to mechanically bond to. Ignoring the equipment match matters too. A small 5-gallon pot blaster can't push #36 grit effectively — the media moves too slowly through the hose and the nozzle clogs. You need a larger pot or a pressure vessel with proper air volume for coarse media. Conversely, using #220 in a high-volume industrial setup just blows the media through without any cutting action. Fine grit needs lower pressure and a smaller orifice to be effective. Another thing nobody mentions: your media lasts longer if you recycle it properly. A good cyclone separator will recover 80 to 90 percent of your abrasive. The finer particles and dust get filtered out and the usable grit goes back into the pot. Without separation, you're burning through media at two to three times the rate and creating a dust hazard for no reason. Disposable blasting into a drop cloth is lazy and expensive over any kind of production run.
What The Chart Can't Solve
Grit size is only one variable. Your air pressure, nozzle distance, angle of attack, and nozzle wear all affect the outcome. A worn nozzle with an enlarged orifice will spray media faster but with less impact energy, which means you might need a finer grit than the chart suggests to get the same result. I measure my nozzle orifice every few weeks. Once it opens up past spec, I replace it. Going another month or two just wastes media and produces inconsistent results. If you need a perfectly smooth surface for a clear coat or liquid finish, sandblasting alone won't give it to you. You'll need to follow up with progressively finer abrasives or switch to polishing compounds. No single grit size bridges the gap from rough blast to mirror finish. Trying to do it in one step just creates an uneven surface with embedded media particles. Some materials simply cannot be sandblasted. Fiberglass will delaminate. Carbon fiber strands will be pulled loose. Plastics like polycarbonate and acrylic will craze or crack. Wood will splinter unevenly. For those substrates, you need alternative media — soda blasting for fiberglass, dry ice for delicate electronics enclosures, or chemical strippers where mechanical abrasion is out of the question.
The grit size chart is a starting point, not a rule book. Use it to make an educated guess, then test on a scrap piece first. One minute of testing saves you hours of fixing a mistake.