Why I Started Using Simulation Software Instead of Just Hitting Cycle Start
I spent years running programs directly off paper prints and hoping for the best. Then I crashed a $12,000 vise into a finished plate because the zero point shifted during a tool change. After that, I started simulating everything. A lot of people in this space still skip it. They shouldn't. OpenSCAM is an open-source 3D CNC simulation and CAD/CAM environment. It handles G-code preview, collision detection, and virtual machining so you can catch problems before they happen on real hardware. It is not the fastest tool on the market, but it does free simulation reasonably well, and it gives you visibility into what your program will actually do rather than what the CAM post-processor says it will do. The core workflow runs like this: import your G-code or CAD model, run the simulation, watch the toolpath in 3D, check for collisions, and save the output. That last part matters because simulation tools sometimes handle tool length offsets differently than your real controller. You need to verify that your simulation settings match your machine config before trusting it blindly.
Installation And Setup Basics
OpenSCAM runs on Windows, Linux, and macOS. I run it on Windows 11 primarily because some of the plugin integrations work smoother there. Download it from the official repository, install it, and launch it. The interface looks like a standard CAD viewport with a timeline and a code editor side by side. It is not pretty. It is functional. Before you load any program, go into Settings and configure your machine defaults. Set your work coordinate system, define your tool library with correct diameters and lengths, and set the travel limits for your machine. I have seen people skip this and wonder why the simulation shows the tool clipping through the table. It is because the simulation has no idea what your machine can actually reach without those limits defined. If you are using multiple workholding setups, create separate machine profiles and switch between them. I keep one profile for my 3-axis mill and one for my router. Mixing them up is an easy way to get false confidence in a simulation that was never calibrated for your actual hardware.
Loading And Verifying G-Code
Open your program file and let the parser read through it. OpenSCAM will highlight syntax issues, missing M-codes, or incompatible commands right away. If the parser flags something, do not ignore it. A flagged command might simulate fine in OpenSCAM but crash your machine because your controller interprets that M-code differently. I had a program that used G43 H1 for tool length offset. OpenSCAM accepted it without error. My lathe-style mill, however, required G10 L10 instead. The simulation looked clean. The real run would have collided on the first Z move. Always cross-reference the M-code and G-code list between what your CAM system outputs and what your machine actually supports before relying on simulation as the final check. Set the material block to match your stock dimensions. A simulation with the wrong stock size will hide collisions that would otherwise be obvious. I learned this the hard way when my simulation showed a clean finish pass that would have actually gouged the stock because the virtual block was smaller than my real clamp setup.
Get the Full Details
Running The Simulation
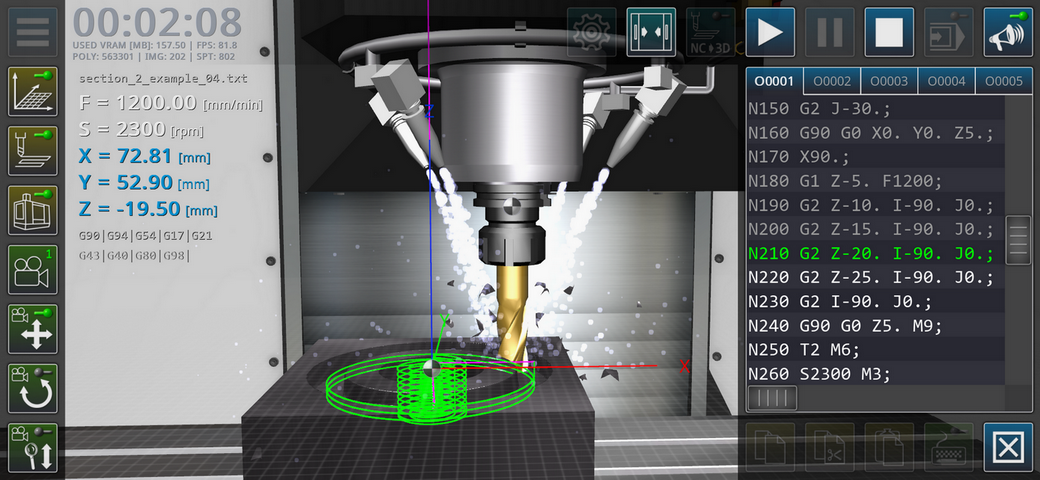
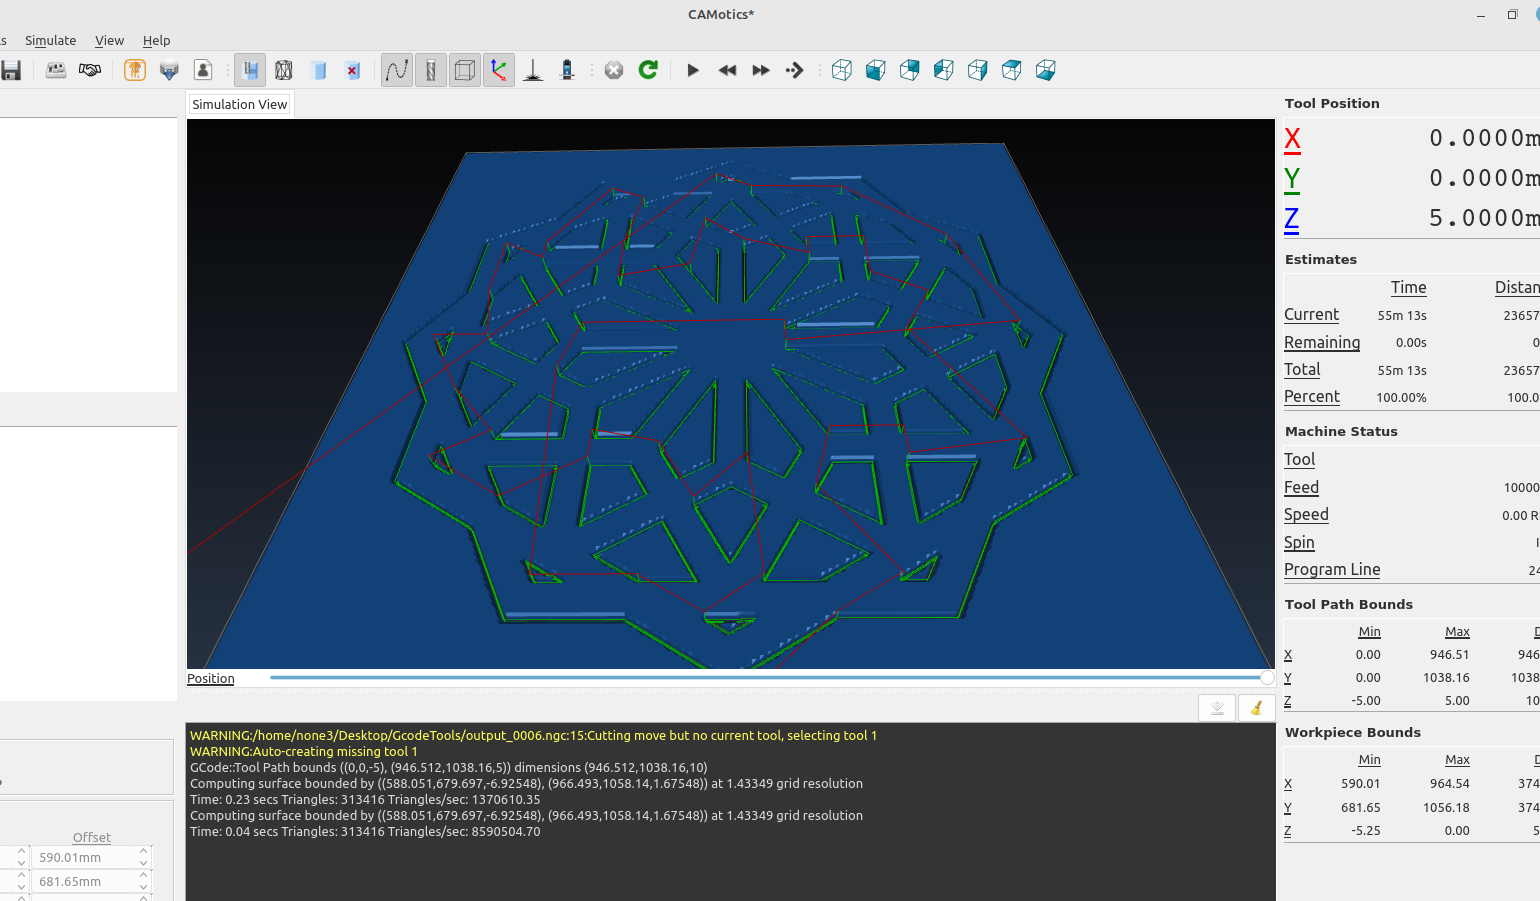
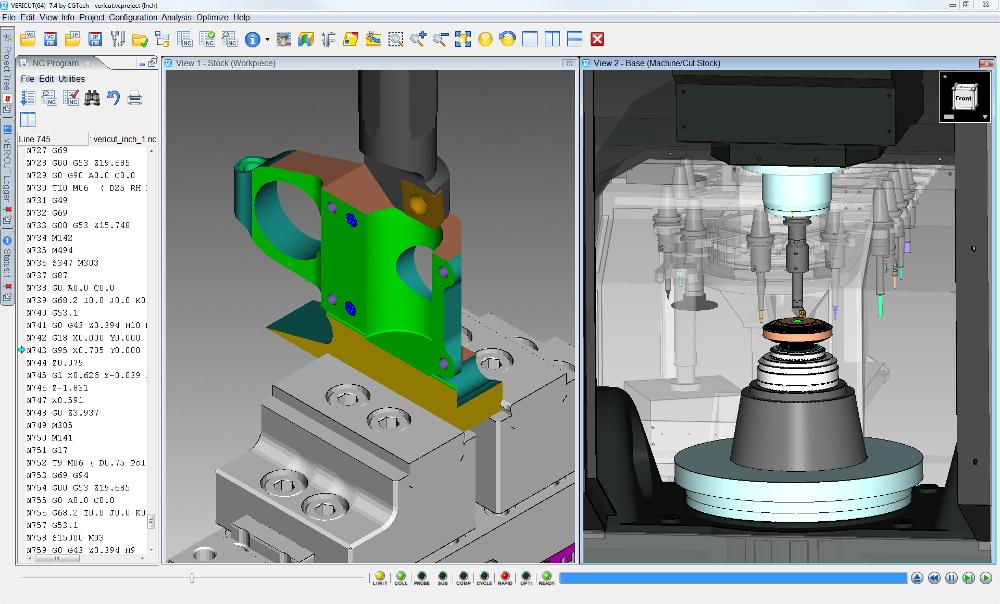
Hit play and watch the tool move through the program. Speed it up if needed, but slow it down during critical sections like deep pocket clearing or approach moves near workholding. The timeline at the bottom lets you jump to specific blocks and inspect the tool position at any point. Collision detection is where simulation earns its keep. Enable it and watch for red highlights or warning icons. Most collisions happen during rapid moves between features, not during cutting passes. Your eye tends to track the cutting motion and miss the fast traverse that slices through a clamp. I once caught a probe approach move that would have taken out a fixture bolt. The simulation showed the probe arm hitting the bolt three seconds before the program would have run on real hardware. That saved me a damaged probe and probably a ruined fixture. I slowed down that section and adjusted the approach vector so the probe came in perpendicular rather than at an angle that intersected the bolt pattern.
Common Pitfalls To Avoid
Simulation is only as good as the data you feed it. If your tool lengths are wrong, your offsets are wrong, or your work coordinate system is misaligned in the simulation settings, the results are garbage. Double-check every parameter before trusting the output. Another issue is post-processor mismatch. Some CAM systems output G-code that assumes a particular controller syntax. OpenSCAM parses it generically, which means it might accept code that your actual machine would reject. Run a dry cycle on the real machine after simulation, not before. Simulation catches geometric errors. Dry run catches control errors. Don't rely on simulation for everything. It cannot replicate machine dynamics like chatter, tool deflection, or thermal growth. If you are cutting deep pockets in aluminum at high feed rates, simulation will show a clean pass. Your tool will still deflect and leave a uneven surface. That is a process parameter problem, not a program problem.
When Simulation Fails You
OpenSCAM struggles with complex multi-axis programs and certain proprietary M-codes. If you are running a 5-axis machining center with swash-and-tilt tables, the simulation accuracy drops noticeably. I had a program that simulated fine for a 5-axis contoured surface cut, but the actual machine hit a kinematic limit that OpenSCAM did not flag because it does not model the full rotary table envelope for every machine type. In those cases, use the manufacturer's own simulation software if it is available. Haas, Mazak, and Fanuc all have their own solutions that understand their specific kinematics. OpenSCAM is best for standard 3-axis mills and routers where the geometry is straightforward and the code is clean G-code without proprietary extensions.
Practical Workflow Recommendation
Here is how I run things now. I generate the G-code in CAM, load it into OpenSCAM, set up the machine profile, run the simulation, note any collisions, edit the program to fix them, re-run until clean, then do a dry cycle on the actual machine before cutting material. This usually takes about 20 to 30 minutes for a standard part. Running it without simulation and discovering a collision mid-program costs far more in time and scrap. Save your simulation settings as a template so you do not have to reconfigure everything for each new program. I keep a default setup for my usual materials and tooling, which cuts the prep time down significantly. Simulation software like OpenSCAM will not replace the judgment of someone who knows their machine. But it will catch the mistakes that even experienced operators make under pressure. If you are not simulating your programs yet, start now. The first crash you avoid pays for the time you spend learning the tool.