Grinding Paste Is Still The Only Way To Get Mirror Finish Without Polishing Wheels
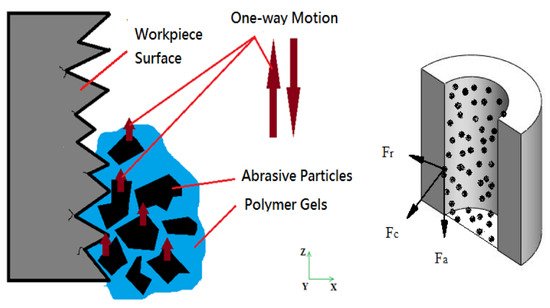
Most people walk into this thinking they need a buffing machine and three hours of arm work. They don't. A proper abrasive grinding paste gets the job done by hand in a fraction of the time, and the finish is more consistent because you control the pressure directly. I've spent years working with aluminum, stainless steel, brass, and even some composites, and the paste routine beats orbital polishing every single time when you want repeatable results. Abrasive grinding paste is simply micron-sized particles suspended in a carrier medium—usually a light oil, wax, or water-soluble base. The grit size runs from roughly 1 micrometer for fine finishing all the way up to 50 micrometers for heavy material removal. The carrier does the heavy lifting on heat dissipation and chip evacuation. Pick the wrong medium and you'll load up your work surface faster than you can wipe it off. Here's what actually happens during the process. The abrasive particles are pressed against the workpiece by hand pressure or a soft pad. Each particle cuts a microscopic groove. Repeat that across the entire surface and you get uniform material removal. The trick is working through progressively finer pastes until the deep scratches from the coarse grit disappear. Most beginners skip steps or rush the transitions, which is why they end up with a hazy finish instead of a clean shine.
I ran into a specific problem last year with a batch of 6061 aluminum panels that needed a mirror finish for an optical reflector application. The spec called for under 0.2 micrometers Ra. I was using a standard alumina-based paste at around 3 micrometers and getting decent results, but every panel had these faint orange-peel textures that refused to clear up no matter how many passes I did. What I eventually figured out was that the carrier in that particular paste was breaking down too quickly under the heat of continued rubbing, leaving behind resinous residue that filled the micro-valleys. The workaround was mixing in a small amount of isopropyl alcohol to slow the carrier evaporation and extend the working life of the paste on the surface. Switched to a diamond suspension in a glycol base for the final pass at 1 micrometer, and every panel came out clean. That change alone dropped my per-panel time from about forty minutes down to eighteen.
Choosing The Right Paste For Your Material
Not all pastes are interchangeable. Alumina trihydrate works well on softer metals like aluminum and copper but will gum up on hardened steels. Silicon carbide cuts faster on harder materials but tends to leave deeper scratches if you aren't careful. Diamond paste is the most expensive option but gives you the finest control and works on everything from tool steel to carbide to glass. If you're working with stainless steel, stick with diamond or a dedicated chromium oxide paste. Black iron oxide paste is traditional for steel and gives a blue-black patina that some people prefer over a bright mirror finish. The grit progression matters more than anyone admits. Going from 9 micrometers straight to 1 micrometer won't work. You'll spend twice as long fighting the fine paste and still end up with visible swirl marks. A typical progression for a heavily scratched surface is 25 micrometers, then 9, then 3, then 1. Each step removes the scratches left by the previous one. The rule of thumb is that each finer paste should take about thirty to forty percent less time than the one before it if you're doing it right.
Get the Full Details
Application Method That Actually Works
Apply the paste directly to the workpiece, not the pad. Use a clean lint-free cloth or your finger for small parts. Spread a thin, even layer across the entire surface you're working on. The layer should be barely visible—not a thick glob. Too much paste justs around and doesn't contact the surface effectively. You want maximum particle-to-surface interaction, not a slurry that dilutes itself. The motion pattern is where most people go wrong. Circular motions create visible swirl marks that are nearly impossible to remove later. Use overlapping straight strokes, preferably in one dominant direction for each grit stage. Switch direction when you move to the next finer paste so you can visually track whether the previous scratches are gone. When the cross-hatch pattern from the prior grit disappears completely, you're ready to move up. This usually takes between two and five minutes per square inch depending on the starting condition of the surface. Pressure is the variable nobody talks about enough. Light pressure produces a better finish because the particles are cutting shallowly and uniformly. Heavy pressure digs deep scratches and generates heat that breaks down the carrier. My hands cramp if I press hard for more than a minute anyway, so I learned to just let the abrasive do the work. The paste does the cutting, not your arm.
Common Mistakes That Waste Time
The biggest mistake is contamination between grit stages. Getting even a tiny amount of coarse paste residue mixed into your fine paste ruins the finer step instantly. Clean the surface thoroughly with a dedicated solvent between stages. Mineral spirits or a dedicated parts cleaner works. Wipe dry with a fresh cloth each time. Don't reuse rags. I've seen people save five minutes on cleaning and lose forty minutes redoing work because a speck of 9-micrometer grit survived into the 1-micrometer stage. Another mistake is assuming that more paste equals faster cutting. It doesn't. A thin film is more effective than a thick one because the particles can reach the surface. Excess paste just acts as a cushion and reduces cutting efficiency. Use enough to keep the surface lubricated and visible, not enough to look wet and sloppy. There are also situations where grinding paste simply won't work. Deep pitting from corrosion, machining tool marks deeper than 10 micrometers, or surface irregularities that require material removal beyond what abrasives can handle—these need stone finishing, tumbling, or mechanical preparation first. Paste is for refining, not for fixing catastrophic surface damage. If your part has visible defects that a fingernail catches, stop and reconsider your approach before wasting a tube of expensive diamond paste.
Storage And Shelf Life
Most grinding pastes last between one and three years unopened if stored between fifty and eighty degrees Fahrenheit. Once opened, keep the cap tight and avoid contaminating the nozzle. Water-soluble pastes can separate if stored too cold or too hot, which ruins their effectiveness. If a paste looks grainy or has liquid pooling on top after stirring, it's degraded. Don't use it for precision work. It'll score your surface instead of polishing it. Diamond paste in particular degrades faster than alumina if exposed to repeated temperature swings. The diamond particles can settle out of the carrier over time. Give it a thorough mix before each use, even if it looks fine. A quick shake isn't enough. The particles settle to the bottom and the top layer becomes carrier-only with zero cutting ability.
When To Move Beyond Hand Application
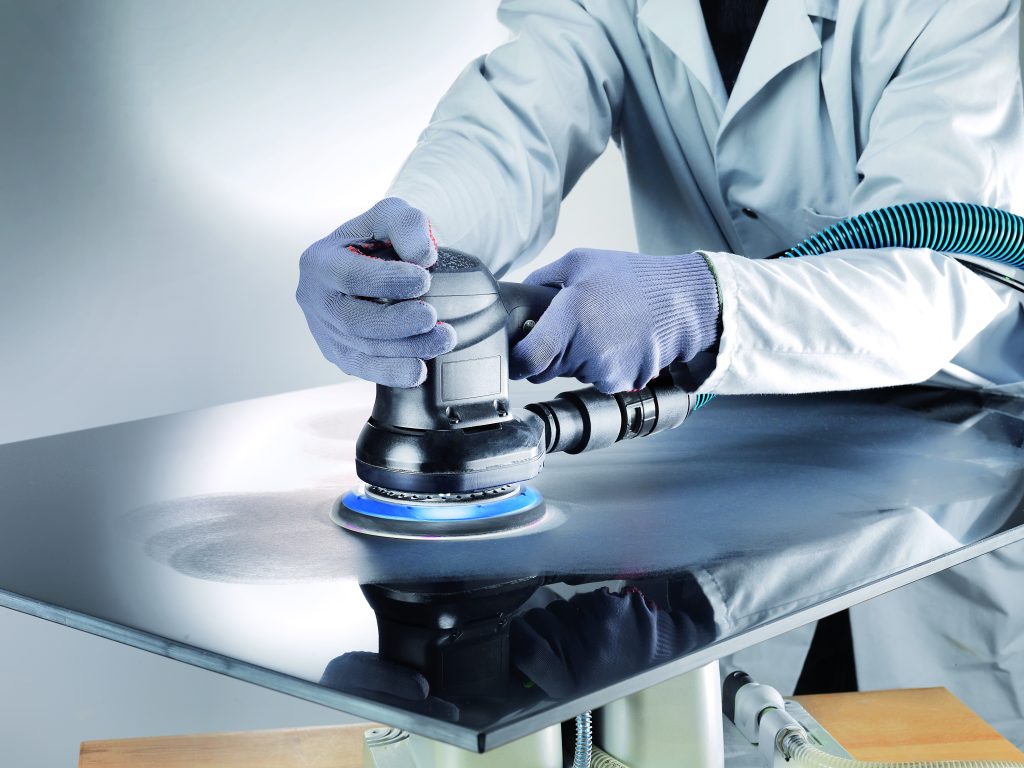
For small parts under four inches, hand application is usually sufficient and gives you the most control. For larger surfaces like sheet metal or wide panels, consider a soft foam pad attached to a low-RPM drill or rotary tool. Keep the speed below eight hundred RPM. Higher speeds generate too much heat and throw the paste off the surface before it can cut effectively. A felt wheel works better than foam for aggressive material removal, but it leaves a different scratch pattern that requires additional stages to clean up. Vibratory finishing with grinding paste is an option for high-volume small parts, but the results are less consistent than hand work and you lose the ability to target specific areas. If you need a mirror finish on a complex geometry with tight tolerances, stick with hand application. The time investment pays off in reduced rework.