What Actually Changes When You Swap to a 0.3mm Nozzle on the A1
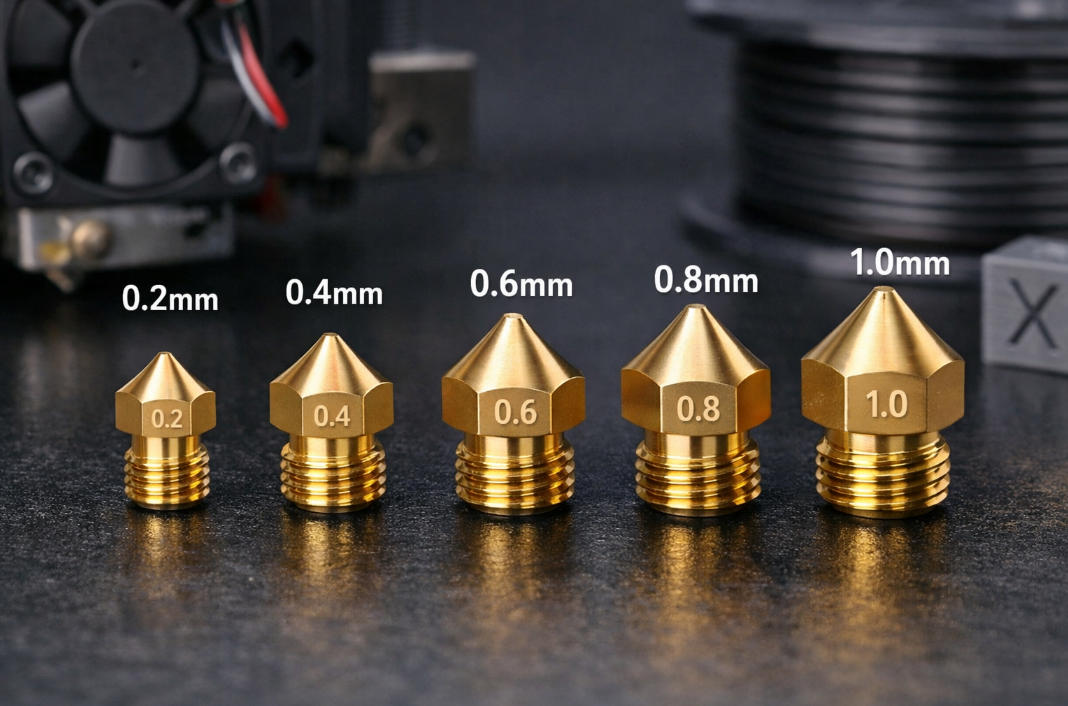
The Creality A1 comes stock with a 0.4mm nozzle, and most people never think about changing it. That changes once you hit the point where you need sharper details on small figures, thinner walls on precision mechanical parts, or cleaner text on test prints. A 0.3mm nozzle is not a magic upgrade. It does one thing: it reduces your minimum line width and lets you print finer layers more reliably. Everything else gets harder. I installed a 0.3mm E3D Volcano-style micro nozzle on my A1 and printed about forty hours across PLA, PETG, and a few TPU runs before writing this down. The short version is that it works well for detail work but punishes bad calibration. If your flow rate is even slightly off, you will see blobs and overextrusion on every layer change. If your nozzle is not seated properly during install, you get partial clogs that look random. I spent three hours on one print figuring out why it was clogging every twenty minutes before realizing I had not tightened the nozzle enough on reassembly. The heat dissipation path goes through that fitting. Looser fitting means less heat transfer into the heatsink, which means heat creep up the bore.
Unlock 3D Printing Precision The Definitive Guide To 03mm Nozzle For A1
This is not a download. It is a tuning workflow. There is no software patch or config file that unlocks the potential of a smaller nozzle. What you get here is the actual procedure I use, the numbers that work on my machine, and the places where things go wrong. You need a 0.3mm nozzle that fits the A1 hotend. The A1 uses a standard CR-10-style threaded hotend assembly, so most aftermarket 0.3mm nozzles will thread right in. I use the E3D V6-style versions from Micro Swiss or the generic clones from Onyx or Enriler. The real differentiator is not the brand. It is whether the nozzle has a long copper barrel or a short brass one. Long copper barrels move heat better and resist heat creep, which matters a lot more at 0.3mm than at 0.4mm because you are pushing less material through a tighter space. You also need a proper nozzle cleaning needle set and a pair of nozzle pliers. The A1 hotend bolts are small and strip easily if you use the wrong tool. I use a 7mm hex key for the heatsink top bolt and 13mm wrench for the nozzle itself. Do not use adjustable wrenches. They round the fittings and then you are replacing the whole hotend assembly.
Installation Procedure
Remove the print head cover. Loosen the two screws on the heatsink clamp just enough to free the hotend block. Unscrew the old nozzle using the 13mm wrench while holding the heater block with the other tool. Clean the inside of the heater block with a nozzle cleaning needle and compressed air. Apply a thin layer of graphite or copper anti-seize paste to the threads of the new 0.3mm nozzle. This is optional but it prevents the nozzle from welding itself to the block on your next removal, which happens more often than you would expect with repeated thermal cycling. Thread the new nozzle in by hand first to avoid cross-threading, then tighten it to about 35 to 40 inch-pounds of torque. That is roughly where the factory spec sits. Do not overtighten. The seal is made by the nozzle shoulder seating against the block, not by crushing the threads. Once the nozzle is seated, reassemble the heatsink and make sure the thermistor and heater cartridge wires are not pinched. Route them away from the moving print head arms so they do not snap during high-acceleration moves.
Get the Full Details
Slicer Settings That Actually Matter
The biggest mistake people make with a 0.3mm nozzle is leaving their flow rate at the default 100%. With a smaller opening, the relationship between extrusion width and filament diameter becomes more unforgiving. I start at 90% flow and adjust from there. Your mileage will vary based on filament diameter tolerance, but 90% is a safer starting point than 100% because it is easier to add flow than to remove it without getting underextrusion. Layer height should stay at or below 0.16mm on a 0.3mm nozzle. That gives you a good ratio without starving the extruder. Anything above 0.18mm and you start losing detail because the nozzle is squeezing the material too much and the layers do not bond cleanly. I typically run 0.10 to 0.14mm layer height for detail work and 0.16mm for everything else. Printing speed drops significantly. Where the A1 with a 0.4mm nozzle can comfortably do 200mm/s outer walls, a 0.3mm nozzle at the same flow rate will struggle above 100mm/s. I run 60 to 80mm/s on perimeters and 100 to 120mm/s on infill. The A1's core XY kinematics handle the acceleration fine. The bottleneck is the extruder gear grabbing the filament and pushing it through a smaller orifice. At high speeds the gear skips, which causes underextrusion that looks like a clog but is actually a feeding problem.
Temperature Adjustments
PLA at 200 to 210 degrees Celsius works well. PETG needs 230 to 240 degrees. The smaller nozzle restricts airflow through the melt zone, so the filament spends slightly more time melting and you can sometimes run a bit cooler than you would with a 0.4mm. I found that dropping PLA from 210 to 200 on the 0.3mm actually improved surface quality because there is less oozing during travel moves. If you are printing with a direct drive extruder like the A1 has, this effect is more pronounced than on Bowden setups because the melt zone is closer to the feed point. Print a flow calibration cube at 90% flow first. Measure the wall thickness with calipers. The target is usually 0.30mm for a single wall on a 0.3mm nozzle, or 0.60mm for two walls. If your measured thickness is higher than target, decrease flow in 2% increments. If lower, increase. This process takes about twenty minutes end to end once you know what to look for. After flow is dialed in, run a tuning tower that steps through layer heights from 0.08 to 0.16mm. The best layer height for your filament and printer is the one where the surface looks smooth without visible ridging or layer separation. I found 0.12mm to be the sweet spot for PLA on my A1 with the 0.3mm nozzle. Finer than that and the print time doubles for negligible visual gain. Coarser and you lose the benefit of switching to a smaller nozzle in the first place.
Common Failure Modes
Clogging is the most obvious one. It usually happens because your printing temperature is too low for the filament, your flow is set too high, or you are using a filament with a loose diameter tolerance. I had a spool of PLA that ranged from 1.68 to 1.74mm and it clogged the 0.3mm nozzle four times in a single weekend. Switching to a tighter tolerance spool solved it immediately. Filament diameter consistency matters more than anyone admits when you drop below 0.4mm. Another issue is poor layer adhesion on the first few layers. The 0.3mm nozzle lays down less material per millimeter of travel, and if your Z offset is even slightly off, the first layer gets squished too thin or not enough. I always calibrate Z offset specifically for the 0.3mm nozzle after installation rather than assuming the A1's auto-level will carry over accurately. The bed leveling on the A1 is good but the nozzle swap changes the effective tip height by about 0.2mm depending on how the old and new nozzles seat, and that is enough to throw off the first layer if you do not recheck. Heat creep is rare but real. If you are printing PETG or ABS at sustained high temperatures and your part cooling fans are not directing airflow properly across the heatsink fins, you can get plastic solidifying in the throat area above the nozzle. I solved this on my setup by adding a small 30mm fan duct that blows directly across the heatsink fins rather than relying on the stock configuration. The A1 has decent cooling by default but the stock fan placement is optimized for the 0.4mm nozzle, not a high-flow scenario through a restricted orifice.
When Not to Use a 0.3mm Nozzle
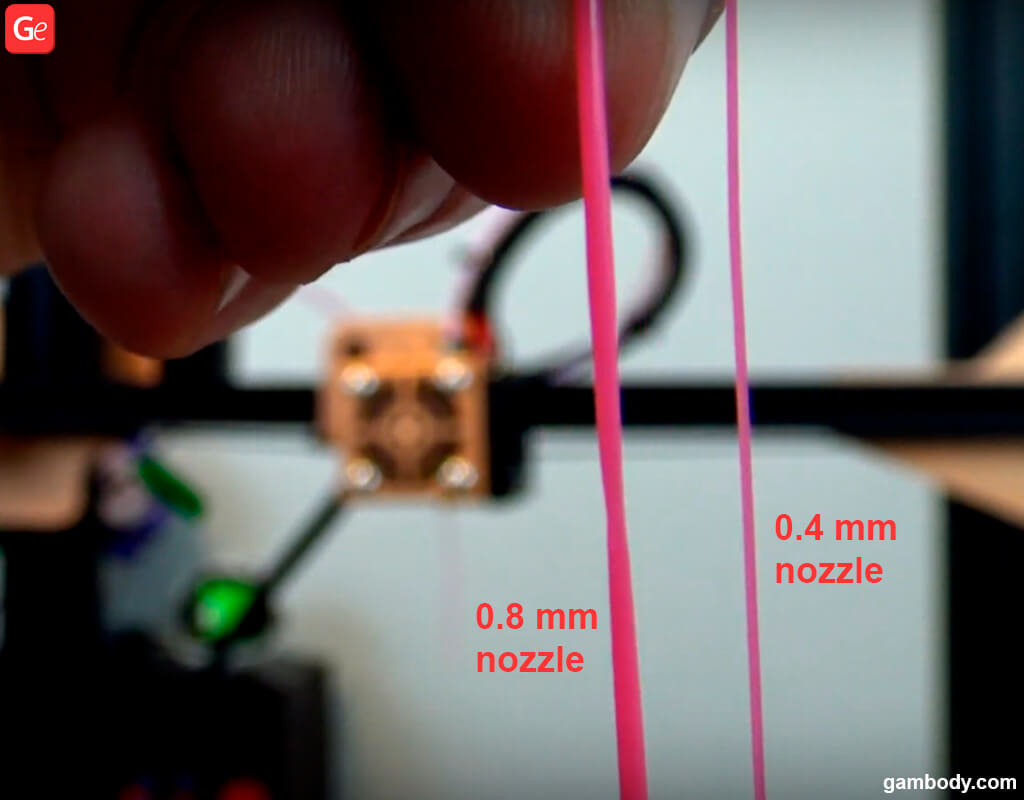
Do not use a 0.3mm nozzle for large prints, functional parts that need high infill density, or anything where print time is a factor. The A1 is fast, and the 0.3mm nozzle makes it slower in a way that is immediately noticeable. A bench desk organizer that takes twelve hours with a 0.4mm nozzle will take roughly eighteen to twenty hours with a 0.3mm. That is not a small difference. If you need fine detail only on specific sections of a model, consider printing the whole thing with a 0.4mm and doing a detail pass with a 0.3mm in a separate build. That is more work but it saves time overall when you are printing at scale. Also, if your filament storage is poor and you print with moist filament, the 0.3mm nozzle will clog far more often than a 0.4mm would. Moisture turns to steam inside the melt zone and expands, blocking the narrow passage. Dry your filament first. It is cheaper than replacing clogged nozzles.
Summary of Practical Settings
Flow rate: 88 to 94%, calibrated per spool. Layer height: 0.08 to 0.16mm, with 0.12mm as the recommended target. Perimeter speed: 60 to 80mm/s. Infill speed: 100 to 120mm/s. PLA temperature: 200 to 210C. PETG temperature: 230 to 240C. Nozzle torque: 35 to 40 inch-pounds. Z offset: recalibrate after every nozzle change. These numbers are starting points. Your filament, ambient temperature, and individual printer will shift them slightly, but they are close enough that you should not need more than two or three calibration prints to get stable results.