Friction Is Usually Treated As A Problem
The standard engineering instinct is to minimize it. Lubricate bearings. Polish mating surfaces. Use ball screws instead of linear slides. This approach works fine for most general-purpose machinery, but it breaks down quickly when you need controlled slip, positive gripping, or energy dissipation. The people who understand friction at a material level tend to get the results they want faster because they stop fighting the physics and start working with it. I want to walk through how friction actually behaves across a few practical domains, what goes wrong when you ignore the details, and a few methods that will save you a lot of trial and error. We will cover the science briefly so the rest makes sense, then move into applications and the specific workarounds that matter in a shop environment.
Unleashing The Power Of Friction A Deep Dive Into The Science And Applications
The Physics You Actually Need To Know
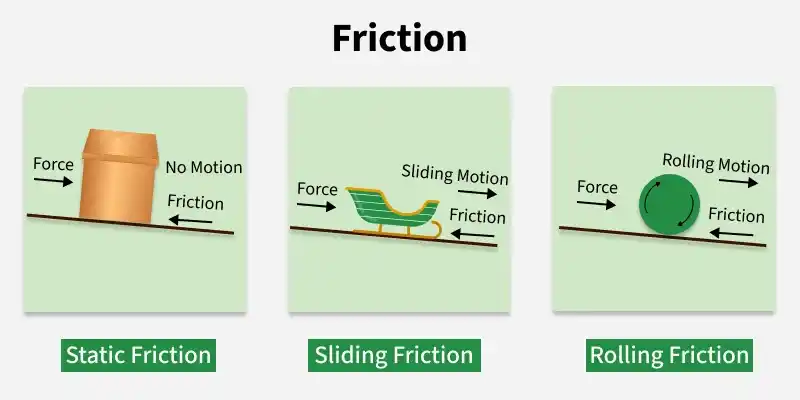
Friction force equals the coefficient of friction multiplied by the normal force. That is the entire equation most people need. The coefficient is not a fundamental property of a material. It is a property of a pair of materials under specific conditions. A steel plate on aluminum at 0.2 might become 0.05 or 0.4 depending on surface finish, temperature, and contamination. That variation alone explains why half the friction-related failures in production are never caught on paper. Static friction is higher than kinetic friction. This is why a part starts moving in a sudden jump rather than smoothly. In assembly work this causes micro-slip and positioning errors that are hard to diagnose because they appear intermittently. I spent three days troubleshooting a robotic pick-and-place station where components were landing two millimeters off target only when the ambient humidity crossed a threshold. The adhesive tape on the gripper pads was absorbing moisture, which changed the static coefficient and caused the parts to slide during the acceleration phase. The fix was switching to a silicone-coated polymer pad rated for controlled humidity and recalibrating the acceleration ramp. Two hours of work after three days of guessing.
Where Friction Becomes A Tool
Brake systems are the most obvious application, but they are also the most misunderstood. The friction material in a brake pad is not selected for a single coefficient number. It is selected for a coefficient that remains stable across a temperature range from ambient to over 400 degrees Celsius. Many budget formulations start strong when cold and then fade aggressively as heat builds. This is called brake fade and it is directly caused by the coefficient dropping under thermal load. The workaround for anyone designing or specifying brakes is to request the friction-temperature curve from the manufacturer, not just the nominal coefficient. Belts and pulleys operate on the same principle in reverse. You want friction to transmit torque without slip until a specific threshold. The capstan equation describes this relationship and it shows that friction engagement increases exponentially with wrap angle. A belt wrapped once around a pulley transmits far less torque than the same belt wrapped twice, even with identical tension. This is why V-belts exist. The wedge action increases the normal force component without requiring higher tension, which reduces bearing loads and extends component life.
Get the Full Details

Surface Preparation That Actually Matters
People obsess over the friction coefficient and ignore surface preparation. That is the most common mistake I see. A surface with a target Ra value of 0.8 micrometers can behave completely differently if the lay direction is parallel to the motion versus crossed. Cross-hatching increases the effective friction by creating mechanical interlock points between asperities. I ran into this when specifying a linear guide system for a precision milling table. The supplier guaranteed a coefficient based on a unidirectional ground finish. When we installed the table with the guideways running parallel to the grind marks, the actual friction was 40 percent higher than specified and caused positional error in the feed axis. We switched to a lapped finish with a crossed lay pattern and the numbers matched the spec sheet immediately. Another detail that gets missed is the difference between running-in and breaking-in. Running a new friction interface at low load for a controlled period allows the asperities to conform and creates a stable transfer layer. Skipping this step on a new clutch plate or brake rotor often leads to uneven wear patterns and premature failure. I typically recommend a break-in cycle of thirty minutes at moderate load, then a gradual increase to full operational parameters over the next few hours. This process alone extends component life by roughly two to three times compared to immediate full-load operation.
When Friction Fails Completely
There are scenarios where friction simply cannot be relied upon and no amount of surface treatment will help. Vacuum environments are the primary example. In space-grade mechanisms, standard lubricants outgas and leave residues that attract particulates while simultaneously reducing friction unpredictably. Some designs in this environment use magnetic coupling or positive mechanical engagement instead of friction-based transmission. Adhesive friction between ultra-smooth metals in vacuum, known as cold welding, is another failure mode that nobody predicts until it happens. I saw a deployment mechanism jam permanently because two polished titanium surfaces in a low-pressure enclosure had bonded together. The fix was applying a thin coating of solid lubricant like molybdisum disulfide during assembly, which prevented metal-to-metal contact without the outgassing problems of liquid lubricants. Ceramic components present a different set of challenges. Silicon nitride bearings have very low friction against steel but only when properly lubricated. Running them dry causes rapid surface degradation because the ceramic is harder than the steel and plucks material from the mating surface. The friction coefficient jumps from around 0.1 to above 0.5 within hours of dry operation, and the resulting wear debris accelerates the damage in a feedback loop. Specifying the correct lubricant grade for the operating temperature range is non-negotiable with these materials.
A Practical Workflow For Specifying Friction Interfaces
Start by defining the operating conditions before looking at any materials. Temperature range, velocity, load, contamination exposure, and required lifetime all matter. A clutch surface operating at 200 degrees Celsius with oil mist present needs an entirely different friction material than a dry conveyor guide running at room temperature. Write these parameters down explicitly. Most friction failures trace back to a mismatch between the design assumption and the actual operating environment. Next, request test data from suppliers that matches your conditions, not generic data from a catalog. A coefficient measured at 25 degrees with clean dry surfaces tells you almost nothing about performance at 80 degrees with light oil contamination. Ask for the Stribeck curve if the application involves mixed lubrication regimes. This curve shows the transition from boundary friction through mixed friction to hydrodynamic friction and reveals the velocity and load points where the system will behave unpredictably. Finally, build a verification test before committing to production. A simple test rig with a load cell and a rotation or sliding stage costs very little compared to the rework involved when a friction interface fails after assembly. I usually design a test that runs for at least ten hours under worst-case conditions and monitors the coefficient over time. If the coefficient drifts more than five percent during that test, the interface needs redesign before it goes into production. This has saved my team multiple costly field failures over the years.

The Bottom Line
Friction is not a fixed number you look up in a table. It is a dynamic interaction between materials, surfaces, and environment. The engineers who get results are the ones who test their assumptions against actual conditions rather than relying on nominal values. Surface preparation, break-in procedures, and environment-specific material selection matter more than the coefficient number itself. When friction works for you, the systems are simpler and more reliable. When you fight it without understanding the underlying mechanisms, you pay for it in downtime and rework.