What Bioreactors Actually Are Now
The bioreactor industry has shifted quietly over the past decade. What used to be a handful of expensive, floor-standing stainless steel tanks has become a landscape of single-use disposables, continuous processing modes, and software-driven automation that most people still don't fully understand. I have spent years working with these systems across multiple facilities, and the reality is less glamorous than the brochures suggest. Most problems come down to contamination control, mixing efficiency, and trying to get cells to behave consistently when they absolutely refuse to. Let me start with something that surprised me when I first encountered it at scale. Bioreactors are not fundamentally about growing cells. They are about controlling the environment those cells live in, and that environment is incredibly small. A five-liter vessel might look simple, but the dissolved oxygen, pH, temperature, and metabolite concentrations all interact in ways that matter exponentially more than any single parameter. You adjust one thing and two other things break. That is the daily reality.
Unleashing The Power Of Bioreactors A Comprehensive Guide To The Latest Technology
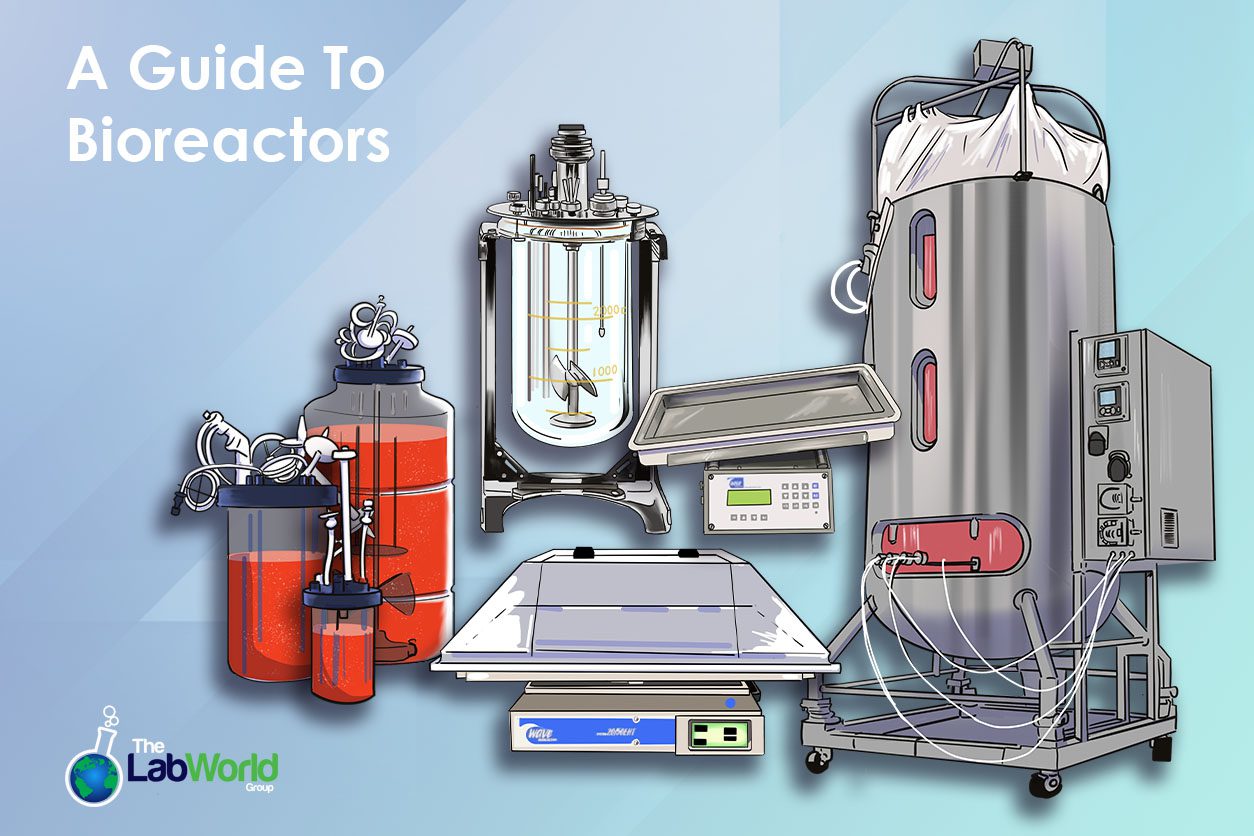
The latest technology centers on three overlapping developments. First, single-use bioreactors have matured from a niche solution for early-stage development into a production-grade option. Second, continuous perfusion systems are replacing traditional batch processes for certain cell lines. Third, real-time analytics and soft sensors are replacing offline measurements for critical quality attributes. I will walk through how these work in practice, not just what the marketing says.
Single-Use Bioreactors: The Real Picture
Single-use bioreactors use flexible polymer bags instead of stainless steel vessels. The bags are pre-sterilized and come with integrated sensors, impeller shafts, and spargers already installed. You load them into a support frame, connect the utilities, and run your process. Afterward, you discard the bag and replace it with a new one. The obvious advantage is reduced cleaning and validation time. No CIP systems, no sterilization cycles, no swab testing. A typical changeover between batches drops from eight hours down to roughly forty-five minutes on a well-designed line. That is substantial when you are running high-mix, low-volume production. The less obvious problem is that single-use bags are fragile. I once ran a 2,000-liter process where a micro-tear developed in the bag during the feeding phase. It was nearly impossible to detect because the leak was slow and the bioprocess seemed normal. By the time we noticed the volume discrepancy, we had lost an entire batch worth of product. The root cause was a sharp edge on the bag support frame that had worn through the polymer over six hours of agitation. We solved it by adding a silicone gasket along the contact point. It is a detail you will not find in any vendor documentation.
Get the Full Details

Another issue is extractables and leachables. Single-use plastics introduce a different contaminant profile than stainless steel. The industry now standardizes on USP Class VI certified materials, but that does not eliminate the risk entirely. You need to validate your specific process for compatibility, especially if you are working with low-protein formulations or products that will not undergo rigorous downstream purification.
Continuous Perfusion: When It Works and When It Does Not
Continuous perfusion bioreactors keep cells inside the vessel while continuously removing product-containing media. The cell retention device can be a hollow fiber filter, a tangential flow filtration unit, or a spinning disk separator. The concept is simple. The execution is where things get difficult. Perfusion shines with cell lines that produce slow-secreting proteins or when you need to maintain very high cell densities for extended periods. I have seen perfusion runs sustain viable cell densities above 50 million cells per milliliter for over forty days. In a traditional batch process, the same cell line would typically crash out after ten to fourteen days as metabolites accumulate and nutrients deplete. But perfusion is not universally better. It requires tighter process control, more complex equipment, and significantly more startup time. If your product is a fast-secreting antibody and your target titer is moderate, a well-optimized batch or fed-batch process will often outperform perfusion on a cost-per-gram basis. The overhead of perfusion equipment, consumables, and control systems eats into the yield advantage before you even account for the increased risk of contamination over longer runs.
A common mistake I see is assuming perfusion automatically means higher productivity. It does not. The real metric is volumetric productivity adjusted for operational complexity and risk. For many platforms, a two-week fed-batch process remains the most economical choice. Perfusion pays off when you need prolonged high-density culture, which usually means difficult-to-express cell lines or products that require extended glycosylation optimization.
Real-Time Analytics and Soft Sensors
The biggest shift in recent years is the move from offline laboratory measurements to real-time monitoring. Invasive sampling used to be the standard. You pulled samples, sent them to QC, and got results hours or days later. Now, inline sensors track dissolved oxygen, pH, conductivity, and biomass density continuously. Raman spectroscopy and FTIR probes can measure glucose, lactate, glutamine, and product concentration in real time without touching the culture. Soft sensors combine these real-time measurements with kinetic models to predict critical quality attributes that cannot be measured directly. For example, a soft sensor can estimate the percentage of correctly folded protein based on the correlation between metabolic rates and product quality, then alert you when the process is drifting toward an unacceptable range. I set up a system like this for a monoclonal antibody process a few years ago. The Raman probe was installed in a 500-liter single-use bioreactor. The model predicted glycosylation shifts three days before they would have been caught by offline HPLC. We adjusted the feed strategy based on the prediction and avoided what would have been a batch rejection. The system required about two weeks of model training before it was reliable, and it needs recalibration whenever you switch cell lines or media formulations. Do not expect plug-and-play performance.
Process Control: What Actually Matters
Mixing is the parameter that gets overlooked the most. Everyone watches dissolved oxygen and pH. Very few people pay attention to power input per unit volume or tip speed of the impeller. These numbers determine whether your cells experience shear stress or nutrient gradients, and both kill cultures quietly. In a 10,000-liter stirred tank bioreactor, the impeller design matters enormously. A standard Rushton turbine creates high shear zones that damage sensitive mammalian cells. An axial-flow hydrofoil impeller provides gentler mixing with better bulk fluid movement. The trade-off is that hydrofoils are less efficient at gas dispersion, so you may need a secondary disc turbine near the gas sparger to maintain adequate oxygen transfer. Gas transfer itself, the kLa value, is where most scale-up failures happen. A kLa that works in a 5-liter lab vessel does not scale linearly to a 2,000-liter production vessel. The impeller tip speed, gas flow rate, and sparger geometry all change during scale-up, and the oxygen transfer coefficient responds in unpredictable ways. I have seen processes that looked perfect at 5 liters fail at 200 liters because the agitation power density dropped below the threshold needed to keep cells adequately oxygenated. The cells did not die immediately. They slowed down, metabolites shifted, and the product quality drifted over several days until someone noticed.
The workaround is to test your process across multiple scales before committing to a production vessel. Run parallel experiments at 50 liters and 200 liters and compare the specific oxygen uptake rates. If the smaller scale shows a significant difference in metabolic behavior, your 2,000-liter design needs adjustment before you go full production.

Contamination: The Unavoidable Risk
Contamination ruins more bioprocesses than any technical limitation. Bacteria, fungi, mycoplasma, and cross-contamination between cell lines are the main threats. Single-use bioreactors reduce cleaning-related contamination but introduce new risks from the bag material itself and from the sterile connectors used in assembly. I recommend a layered approach. Sterile barrier systems on all inlet and outlet ports, atmospheric containment through HEPA-filtered isolators or controlled-grade rooms, and routine environmental monitoring at multiple points around the bioreactor setup. The isolator approach is more expensive upfront but has cut our contamination rate from roughly one in every forty batches down to one in every two hundred. Mycoplasma is the quiet killer. It does not always show obvious signs. Cultures grow slowly, yields drop gradually, and the product quality degrades without dramatic warning. I have seen entire production campaigns delayed by weeks because mycoplasma was detected late in a run. PCR-based testing is the gold standard now, but it is expensive to run on every batch. A practical compromise is to test incoming cell banks and media components, then monitor periodically during long runs rather than testing everything continuously.
Downstream Processing: Where Bioreactors End and Reality Begins
A well-run bioreactor is pointless if downstream processing cannot handle the output. The harvest step, where you separate cells from the product-containing media, often determines whether you preserve product quality or lose it. Centrifugation and depth filtration are the standard methods, and each has trade-offs. Disc-stack centrifuges are fast but can generate shear forces that damage sensitive products. Depth filtration is gentler but creates filter cake that requires careful optimization to avoid clogging. I once spent three days troubleshooting a depth filter that kept blinding on a particular culture, only to discover that the cell debris from a specific feeding strategy was creating an unexpected particulate profile. Changing the feed timing and reducing the feeding frequency resolved the issue entirely. This is the kind of detail that never appears in process documentation but determines whether a run succeeds or fails. Protein A chromatography remains the workhorse for monoclonal antibody purification, but resin lifetime and cleaning validation are constant concerns. I have seen resin beds degrade prematurely because the bioreactor harvest was not properly clarified, allowing particulates to enter the column and compact the resin bed unevenly. Always check your harvest clarity before it reaches the chromatography step.
Scale-Up: The Hardest Part
Scaling from bench to pilot to production is where most projects fail. The mathematical relationships are well established, but the practical outcomes are rarely linear. Geometric similarity alone does not guarantee consistent performance. Impeller type, sparger design, baffle configuration, and vessel height-to-diameter ratios all influence mixing and oxygen transfer in ways that complicate simple scaling rules. A commonly used approach is constant power per unit volume, but this fails for shear-sensitive mammalian cell processes. Those processes often require constant impeller tip speed instead, which means the larger vessel runs at lower agitation rates relative to its size, accepting lower oxygen transfer efficiency in exchange for reduced cell damage. You then compensate with higher gas flow rates or pure oxygen enrichment. I worked on a scale-up from 200 liters to 2,000 liters where the constant power density approach caused a significant drop in viable cell density. The cells were surviving but growing slower than expected, and the product titer fell well below the target. Switching to constant tip speed and adding pure oxygen to the sparge gas restored performance. The lesson is straightforward but easy to miss: there is no universal scaling criterion. You need to identify which parameter matters most for your specific cell line and process, then build your scale-up around that constraint.
Automation and Data Management
Modern bioreactors generate enormous amounts of data. Every sensor, every actuator, every offline measurement creates records that need to be stored, analyzed, and reported. Batch record compliance, audit trails, and data integrity requirements under FDA and EMA regulations mean you cannot ignore this infrastructure. Most facilities now use distributed control systems with Historian databases and electronic batch records. The initial setup is tedious, but the long-term benefit is real. When you can query a complete process history for any given batch in seconds, troubleshooting becomes significantly faster. I recently traced a batch quality deviation back to a temperature probe calibration drift that had occurred three weeks earlier. The electronic batch record showed the anomaly in the raw data, and the trend analysis made it obvious within an hour. Without that system, it would have taken days of manual review. The downside is that these systems require skilled operators and regular maintenance. A calibration drift in one sensor can cascade into incorrect automated decisions if the control logic depends on that input. Always maintain manual override capability and regular instrument calibration schedules.
Cost Reality
Bioreactor operations are expensive. Capital costs for a 2,000-liter stainless steel system with the required supporting infrastructure run into the millions. Single-use systems reduce capital expenditure but increase per-batch consumable costs. The break-even point depends entirely on your production volume and product value. Operational costs include utilities, media, single-use consumables, labor, quality control, and facility maintenance. A typical 2,000-liter batch process for a monoclonal antibody can cost between fifty thousand and two hundred thousand dollars to run, depending on the scale of the operation and the complexity of the downstream purification. High-throughput screening and process development add additional costs on top of that. If you are considering entering this space, the economics favor either high-value products or high-volume manufacturing. Low-value biologics with thin margins are extremely difficult to produce profitably in traditional bioreactor facilities. Continuous processing and single-use systems improve the economics somewhat, but they do not fundamentally change the cost structure.
Where the Field Is Heading
Several trends are shaping the next generation of bioreactor technology. Modular continuous manufacturing is moving from concept to implementation for several product platforms. AI-driven process optimization is becoming more common, though the models are only as good as the data they are trained on. Additive manufacturing is being explored for custom bioreactor components and mixing elements. And the push toward personalized medicine is driving demand for smaller, more flexible bioprocessing systems that can handle low-volume, high-complexity products. The fundamental challenge remains the same. Biological systems are inherently variable. No amount of technology eliminates that variability, but it does give you better tools for understanding and managing it. The engineers who understand both the biology and the engineering tend to get the best results. Specialists in either domain alone usually hit walls that the other domain could have resolved.

