Aluminum Welding Actually Works When You Stop Fighting It
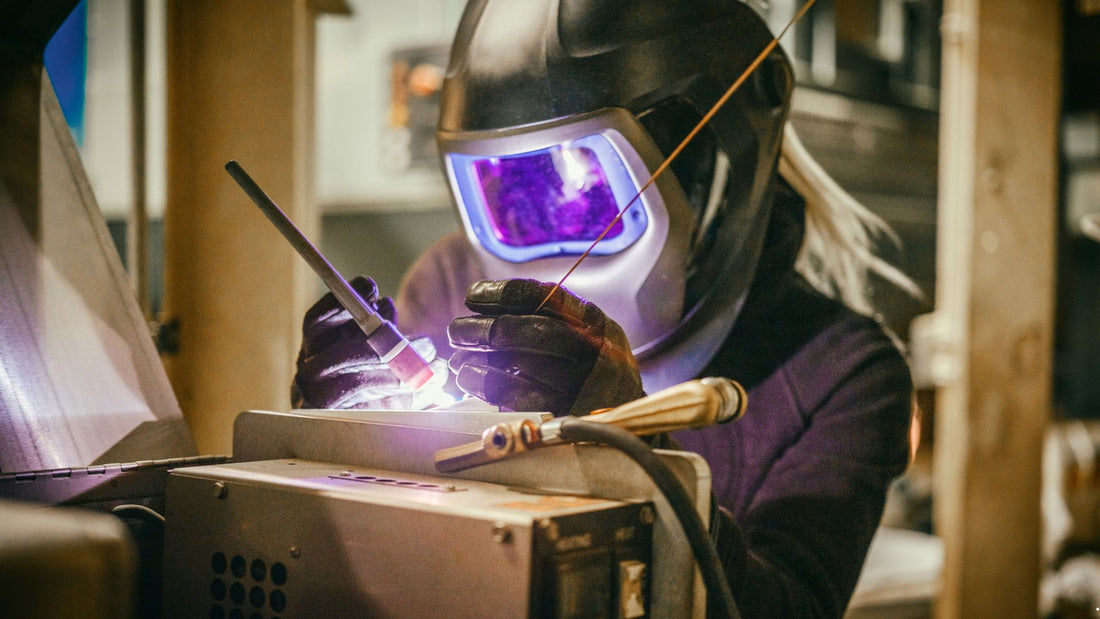
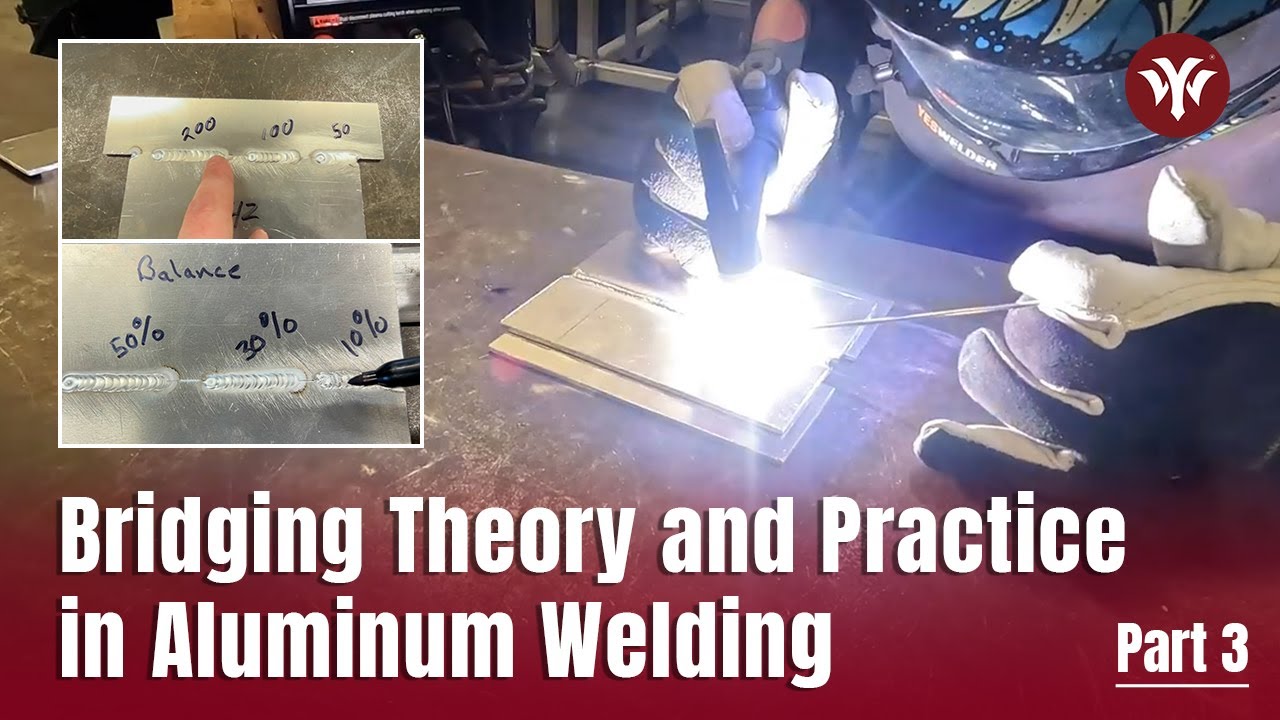
I spent years fighting aluminum like it was personal. The first thing you need to understand is that aluminum does not behave like steel, period. It has no color change before it melts, it conducts heat away from the arc roughly twenty times faster than mild steel, and the oxide layer on the surface sits at about 3,600°F while the base metal underneath gives up around 1,225°F. You are essentially burning through a ceramic skin that refuses to melt at the same time your material is turning to liquid. The machine settings matter, but they matter less than your prep work. I have seen people dial in perfect parameters on a Miller or Lincoln and still produceporous, unreliable beads because they skipped the cleaning step. Aluminum oxide absorbs moisture. That moisture breaks down during welding and releases hydrogen into the weld pool. Hydrogen in a cooling weld is what causes porosity. So before anything else, use a dedicated stainless steel wire brush, never one that has touched steel, and clean the material from one direction only, not back and forth. Then weld within a few hours of cleaning. Leaving it sitting overnight is asking for trouble. For TIG welding aluminum, you need AC balance and frequency controls on your machine, not just a basic on-off switch. The pure AC wave is the starting point, but it eats tungsten and usually produces a wide, messy puddle. Bump the high-frequency clean action up to around 60 percent and drop the balance toward 70-75 percent electrode positive. This gives you deeper penetration while keeping the cleaning action strong enough to break through that oxide layer. I run a 3/32 inch 2 percent thoriated tungsten, pointed to about a 30-degree angle, with the tip sticking out maybe half an inch from the cup. A ceriated tungsten works too, but thoriated holds its point better under the heat aluminum demands.
The gas setup is not optional. Use 100 percent argon, not argon-helium mixes unless you are welding thick plate over half an inch. Helium increases heat input and travel speed, but it also makes the arc less stable and more difficult to control, especially for someone who is not already comfortable with aluminum. At 40 CFH through a 12-inch cup, you are in the right neighborhood. Larger joints might push that to 50 CFH. Shielding is everything. Here is the problem I ran into that almost made me quit aluminum altogether. I was welding 3/16 inch 6061-T6 bracket plates together for a custom fabrication job. My travel speed was decent, my shielding looked fine, but when I broke out the dye penetrant after grinding, the entire joint was full of pinpoint porosity. I had cleaned the material. I had the machine dialed in. I checked everything. Turns out the argon cylinder had been sitting outside in the cold garage for two weeks, and the pressure was low enough that atmospheric moisture was pulling back into the regulator when the flow dropped between welds. Cheap trick to fix it: wrap a heat tape around the bottom third of the cylinder and set the tank indoors at least a day before you plan to use it. After that, my porosity dropped to nearly zero on the same setup. It was not a technique problem at all. When you are actually laying down a bead, let the puddle do the work. Aluminum does not give you the slow, viscous pool you get with steel. It stays fluid and aggressive. If you hesitate, the puddle drops through and you burn a hole. Walk the cup. Keep the torch at about a 15-degree drag angle and move at a pace that keeps the leading edge of the puddle molten while the trailing edge just barely starts to freeze. You should be able to see the bright, mirror-like surface of the puddle reflecting light as it forms. If it goes dull gray or black, you are either overheating or your gas coverage is insufficient.
Backstepping is a legitimate technique for aluminum, especially on thin material or when you are dealing with a root pass that needs extra time to fuse. You set up the puddle, let it start to solidify, then push the arc back a quarter inch or so to re-melt the leading edge and allow gases to escape before moving forward again. This is particularly useful on 6061 when you are seeing micro-cracking in the HAZ, which happens more often than people expect on that alloy if you do not control heat input properly. Filler metal selection deserves more attention than it gets. 4043 is the standard for general purpose aluminum welding. It has lower silicon content than 5356, flows better into tight joints, and is less prone to cracking on constrained assemblies. But 4043 has a slightly lower melting point and produces a darker weld bead that does not match the base metal as nicely. If color matching matters, like on show panels or architectural work, go with 5356. It welds a little differently, requires a cleaner surface, and it will crack if you get too much heat into a thin section. Neither filler is universal. Picking wrong just creates problems you can weld around but should have avoided entirely. Clamping and fixturing is where most people lose time on aluminum. Unlike steel, aluminum expands significantly more during heating and contracts aggressively on cooling. If you tack a rigid aluminum assembly and then run a long continuous bead, something is going to warp or crack. I use copper backing bars under every groove weld on material over 1/4 inch. Copper pulls heat away fast and gives you a controlled backing profile without the filler drooling through. I also tack weld at three or four points around a joint before running any continuous pass, and I leave about two inches between tacks so the joint can shift slightly as it heats without building up dangerous stress.
Get the Full Details
Post-weld heat treatment is another area where people make assumptions. 6061-T6 can be post-weld heat treated to restore some of the lost strength, but that requires a furnace cycle at roughly 800°F for an hour followed by water quenching, and then aging at 325°F for about eight hours. Most shop setups cannot do this accurately, and attempting it on a large or complex assembly usually warps it worse than the weld did. For production work where full strength matters, you either design the joint to avoid putting load directly on the weld, use 5083 or 5356 filler which retains more strength in the welded condition, or accept that the HAZ will be weaker and design accordingly. There is no shortcut around metallurgy. MIG welding aluminum follows similar principles but introduces a new variable: the spool gun or push-pull feed system. Standard pressure-fed MIG guns struggle with soft aluminum wire because it buckles inside the liner, especially past about four feet of cable run. A spool gun solves this by placing the wire source directly at the torch. It is heavier and less convenient to maneuver, but it feeds reliably. Push-pull systems are more expensive upfront and require maintenance, but they give you the range of a standard MIG setup with the feeding reliability of a spool gun. If you are welding aluminum regularly, one of these is not a luxury, it is a necessity. Parameters for MIG on 3/16 inch 6061 typically land somewhere around 18 to 22 volts and 150 to 180 amps with .035 inch 4043 wire. Gas flow stays in the 35 to 45 CFH range. Preheat is rarely needed on material this thin, but on thicker sections above half an inch, a gentle preheat to about 200-250°F reduces thermal shock and gives you more working time on the puddle. You will know it is hot enough if you can hold your bare finger on the surface for two seconds without burning, which is not great advice to follow literally but it is a practical gauge.
The biggest mistake I see beginners make with aluminum is treating it like a harder, slower version of steel. It is not. The puddle dynamics are fundamentally different. The lack of color change means you are welding by feel and observation rather than by visual cues the way you would with MIG on steel. Spend time practicing on scrap pieces of the same thickness and alloy you intend to weld. Watch the puddle. Learn what it looks like when it is correct. The skill is in recognizing that state, not in memorizing parameter tables. Porosity remains the most common defect even for experienced welders, and it is almost always preventable. Check your gas lines for leaks with soapy water before every session. Make sure your contact tip is the correct size and not worn out. A worn tip increases electrical resistance, heats up, and can cause the wire to melt prematurely inside the tip, creating intermittent feed issues that look nothing like porosity but produce similar results. Replace tips regularly. They are cheap. Downtime is expensive. If you are running into persistent issues despite checking all the obvious causes, look at your work clamp connection. Aluminum oxidizes rapidly, and that oxide is non-conductive. A work clamp attached to a painted or oxidized surface will create an unstable arc that manifests as inconsistent penetration and sporadic porosity. Grind a bare spot on the workpiece where the clamp makes contact. The connection should be metal-to-metal, bright and tight. This single step resolved a recurring issue for a fabricator I worked with who was tearing his hair out over seemingly random defects.
Welding aluminum is straightforward if you respect what the material actually requires. Clean surface, proper shielding, appropriate filler, correct heat input, and acceptance that the process will not forgive sloppy technique the way some other metals do. It rewards preparation and punishes assumptions. The results are consistent when you give the process what it needs.