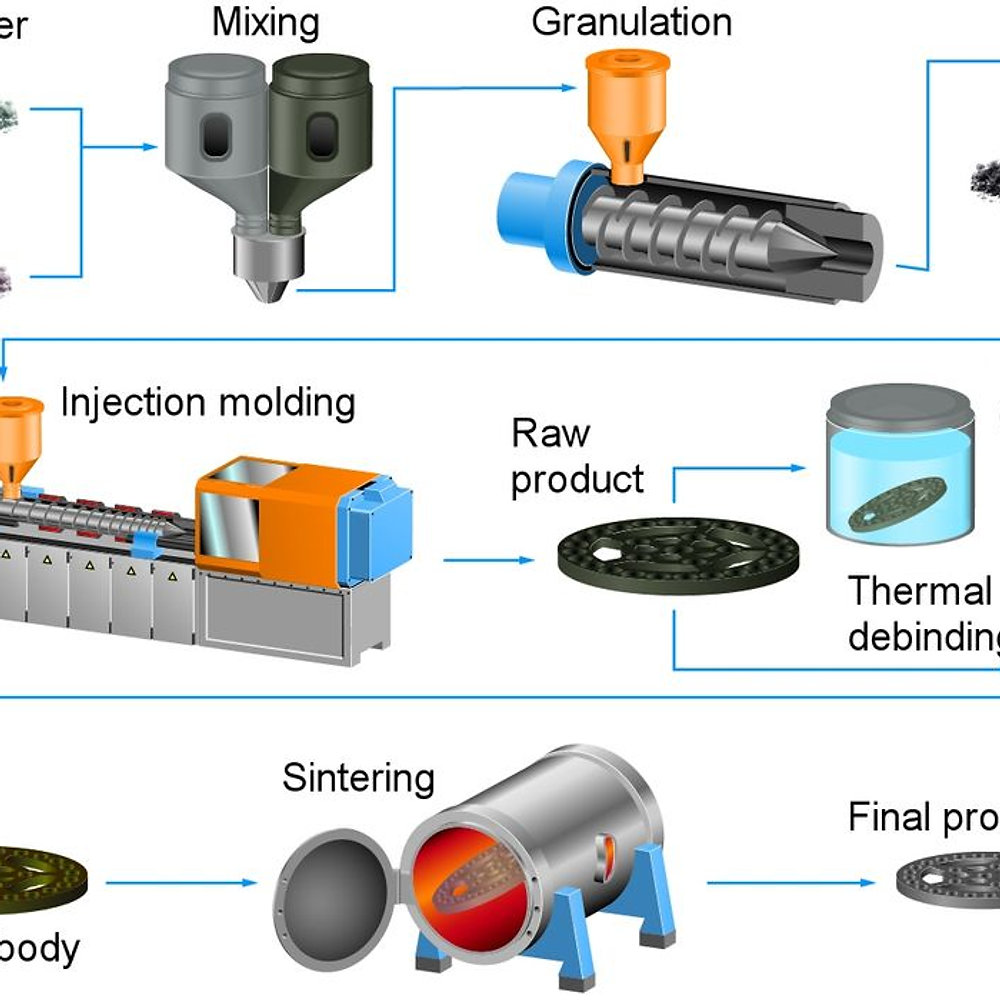
Getting Past the Bottlenecks in Injection Molding
Most people treat injection molding like it is a straightforward process. You melt plastic, inject it into a mold, wait for it to cool, and eject the part. That oversimplification is exactly why production lines stall out and why cycle times never improve. The reality is messier. I spent roughly nine years running production floors before moving into process consulting, and the difference between a mediocre line and an efficient one usually comes down to a handful of variables nobody talks about in training manuals. Cooling time is the single biggest factor in cycle time, and it is also the most misunderstood. The rule of thumb says cooling time scales with the square of the thickest section. So doubling wall thickness quadruples cooling time. That sounds simple enough, but the practical implication is that a part that looks trivially thin can still dictate your entire cycle if one rib or boss is thicker than the rest. I once had a client running small connector housings where the cosmetic walls were 1.5 millimeters, but an internal rib at 2.8 millimeters was controlling the cooling. We redesigned the rib with a 1.5-millimeter core instead of a solid one and cut the cycle time by nearly forty percent without changing anything else. The parts came out structurally identical and the sink marks disappeared too.
Unleashing Efficiency A Comprehensive Guide To Injection Molding Accelerate Your Manufacturing Process
There is no single downloadable PDF that will transform your output. What actually works is a systematic audit of the entire cycle, broken down into measurable phases. Shot time, fill time, packing time, cooling time, and mold open-close time each have their own constraints, and improving one phase often creates a problem in another. The trick is understanding the tradeoffs rather than blindly optimizing a single variable. Start by pulling the machine data logs. Most modern clamping units record pressure, temperature, position, and time for every shot. The data usually tells you exactly where time is being wasted. You might find that the packing phase is holding pressure far longer than the part actually needs it, which wastes seconds per cycle and also increases residual stress inside the part. Or you might discover that the mold is spending more time waiting for the next shot than it should because the robot placement is inefficient. These are the kinds of problems that only show up when you stop guessing and start measuring. Mold temperature control is another area where people routinely leave performance on the table. Standard single-zone controllers sitting on the mold surface are adequate for basic runs but they cannot maintain consistent temperature across the entire cavity face. If you are running high-volume production, retrofitting the mold with an inline chiller that circulates temperature-controlled oil through properly sized lines is a significant upgrade. Oil heating and cooling is faster than water and maintains temperature within plus or minus one degree Celsius across the full cycle. The upfront cost is real. A decent multi-zone modular controller with heat transfer oil and upgraded chillers can run anywhere from three to eight thousand dollars depending on the mold size, but on a high-volume part it pays for itself within the first six to twelve months through cycle time reduction and scrap reduction alone.
Material selection matters more than most shops admit. Switching from a standard polypropylene grade to a fast-cycling formulation can shave a second or two off cooling time per shot, and on a part running thousands of cycles per shift, that adds up fast. I worked with a medical device shop that switched from a generic PP to a specialized homopolymer grade designed for thin-wall applications. The change dropped their cycle time from twenty-eight seconds to nineteen seconds on a small cap component. They also reduced warpage issues by about half because the new material crystallized more uniformly during cooling. The material cost per kilogram was higher, but the total cost per part went down because the machine was producing significantly more output per hour.
Get the Full Details

The Hidden Cost of Overpacking
Packing pressure is where a lot of well-intentioned adjustments do more harm than good. Operators see a slight sink mark on a cosmetic surface and respond by cranking up the packing pressure. Sometimes that fixes the sink mark temporarily, but it also increases clamp force requirements, raises internal stress, and can make part ejection much more difficult. The right move is almost always to address the root cause rather than mask it with more pressure. If the sink mark is coming from a thick section, the solution is to modify the geometry, not the machine settings. Reducing wall thickness, adding a spiral rib instead of a solid rib, or changing the gate location so the thick section fills last and remains accessible for packing are the actual fixes. This is counterintuitive for people who are used to thinking of injection molding as a black box where you turn knobs until the part looks acceptable. It is not a black box. The geometry drives the physics, and the machine settings simply follow the physics. Gating strategy deserves its own attention. A poorly placed gate forces the melt front to travel long distances before filling the cavity, which creates higher shear rates, more orientation, and uneven cooling. Multiple gates can balance the fill pattern, but they also create weld lines that weaken the part structurally. I once evaluated a housing component that was running with a single edge gate. The fill pattern was causing a visible weld line across the center of the part, and the cycle time was excessive because the melt had to travel too far. We switched to a dual fan gate configuration placed symmetrically on opposite sides. The weld line moved to a non-cosmetic area, the fill time dropped by roughly thirty percent, and the part showed significantly less warpage because the cooling pattern became more uniform. The mold modification cost about four thousand dollars, but the annual savings from reduced scrap and faster cycles covered it within a year.
Ventilation and the Unsung Problem
Trapped air in the mold cavity is one of those issues that nobody notices until it becomes a disaster. Air gets compressed rapidly as the molten plastic advances, and if it cannot escape through proper venting, it creates burn marks, short shots, and surface defects. The fix is not complicated but it is often overlooked during mold design. Vents should be placed at the end of the fill path, typically around 0.02 to 0.05 millimeters deep depending on the material. For polypropylene you can go slightly deeper. For engineering plastics like polycarbonate or PEEK, the vents need to be shallower to prevent flashing. I ran into a situation a few years ago where a batch of nylon parts kept showing occasional burn marks near the end of the cavity. We ruled out material degradation and machine issues first. The problem turned out to be vent blockage. Natural oils from the operator's hands during manual inspection had seeped into the vent grooves and carbonized over time. Cleaning the vents with a fine copper brush and running a mold cleaner through a few cycle shots fixed it completely. We switched to a preventive maintenance schedule after that, cleaning and inspecting the vents weekly instead of waiting for defects to appear. The burn marks stopped showing up again.
Resin Drying and Moisture Sensitivity
Some materials require drying before processing, and skipping or inadequately drying the material is one of the fastest ways to destroy part quality. Nylon absorbs moisture from the air readily, and even a small amount of residual water can cause hydrolysis during the injection process. The resulting parts will have reduced mechanical properties, surface blisters, and streaking. Most material suppliers specify drying conditions in their datasheets, and those specifications are not suggestions. If the datasheet says dry at eighty-five degrees Celsius for four hours, you dry at eighty-five degrees for four hours. The drying system itself matters too. A simple hopper dryer with a basic thermostat is often insufficient for high-volume runs. Desiccant dryers that push air below the dew point into the hopper maintain consistent moisture levels throughout the entire production run. I have seen shops switch from atmospheric dryers to desiccant dryers and reduce moisture-related scrap from nearly eight percent down to under one percent on a single changeover. The energy cost of a desiccant dryer is higher, but the scrap reduction alone justifies it on engineering resins.

Robot Integration and Cycle Consistency
Automated part removal is not optional at volume. Hand-loading and hand-unloading introduces variability that machine settings cannot compensate for. Different operators remove parts at different speeds, place them in different positions, and sometimes touch the part in ways that affect cooling or dimensional stability. A properly programmed robot with the right end effector removes this variability entirely. The initial investment is significant, typically ranging from five to fifteen thousand dollars for a standard three-axis pick-and-place system with a gripper tailored to the part, but the consistency gain is immediate. One thing that is not obvious is the communication protocol between the robot and the molding machine. Not all robots integrate seamlessly with all machines. If you are working with an older machine, you may need an external interface box to translate the signal handshake. I encountered this on a line where we introduced a new robot to an aging hydraulic press. The robot kept receiving false cycle-complete signals because the machine's output relay was degrading. We replaced the relay module and reprogrammed the synchronization logic, which resolved the issue. Without that fix, the robot would occasionally attempt to extract the part while the mold was still closing, which resulted in damaged parts and an occasional damaged mold.
When Injection Molding Is Not the Right Call
There are scenarios where injection molding simply makes no economic sense, and it is worth acknowledging that upfront. Low-volume production, prototype runs under five hundred pieces, or parts made from materials that degrade at processing temperatures are all cases where alternative methods are more practical. For low volumes, CNC-machined aluminum molds or soft tooling in aluminum can produce functional parts at a fraction of the cost of a hardened steel injection mold. A steel injection mold for a medium-complexity part typically costs between fifteen thousand and fifty thousand dollars depending on cavity count and complexity. That tooling cost only becomes justifiable when you are amortizing it across thousands or tens of thousands of parts. Similarly, if your part has extreme geometrical complexity with deep undercuts that would require multiple slider mechanisms, the mold cost and maintenance burden can become prohibitive. In those cases, checking whether a simpler two-part design with draft angles and relocated undercuts could achieve the same function at a lower tooling cost is usually worth the engineering time. I have seen designers insist on retaining complex geometries that were unnecessary, driven by CAD models that did not account for manufacturability constraints. A brief conversation with a mold designer early in the development phase can save tens of thousands of dollars in tooling costs.
Measuring What Actually Matters
Process monitoring and statistical process control are not buzzwords. They are the difference between reacting to problems and preventing them. Installing sensors to track cavity pressure, not just hydraulic pressure, gives you a direct read on what is happening inside the mold during each cycle. Cavity pressure sensors cost anywhere from two to six thousand dollars per cavity, but they provide data that hydraulic sensors cannot. You can detect variations in fill consistency, packing efficiency, and cooling uniformity in real time. If the cavity pressure curve shifts even slightly between cycles, you know something is changing before it shows up as a defective part. Data logging and trend analysis turn those sensor readings into actionable intelligence. Modern systems can flag a drift in cavity pressure and alert the operator before the parts go out of specification. Some shops integrate this with automated machine adjustment, where the system compensates for minor variations by tweaking injection speed or packing pressure automatically. This level of automation is not cheap, but for a high-volume production environment running twenty-four hours a day, it eliminates the variability that comes from human monitoring alone. The practical steps are straightforward even if the investment is not trivial. Audit your current cycle times against the machine logs. Identify which phase is consuming the most time and where the largest improvements are possible. Review the mold design for gating and venting issues. Upgrade temperature control if you are running high-volume production with tight tolerances. Introduce automated part removal to eliminate human variability. Implement cavity pressure monitoring if the volume justifies it. Each of these steps addresses a specific source of inefficiency, and together they form a coherent approach to accelerating the manufacturing process without cutting corners on quality.