Lean Manufacturing at Toyota: What Actually Happens on the Floor
Most people hear "lean" and think it means cutting staff or squeezing budgets. That's not what it is. Lean manufacturing is about removing friction from a process so work flows without stopping. Toyota built their reputation on this, and it isn't magic. It's just disciplined observation of where time and material actually go versus where management thinks they go. I worked on a line conversion project a few years back where we tried to apply Toyota's principles to a small-batch electronics assembly operation. The real problem wasn't the layout. It was that nobody on the floor would admit when a station was falling behind. There was a cultural gap between the written process and the actual process. We found out by just standing at a point for three hours and recording every stop, delay, and workaround the workers used. The documented cycle time was 4.2 minutes per unit. The real cycle time was 6.8 minutes. That's the kind of blind spot lean exposes.
Toyota Lean Manufacturing Prinsip Manfaatnya Yang Membuat Perusahaan Lebih Efektif
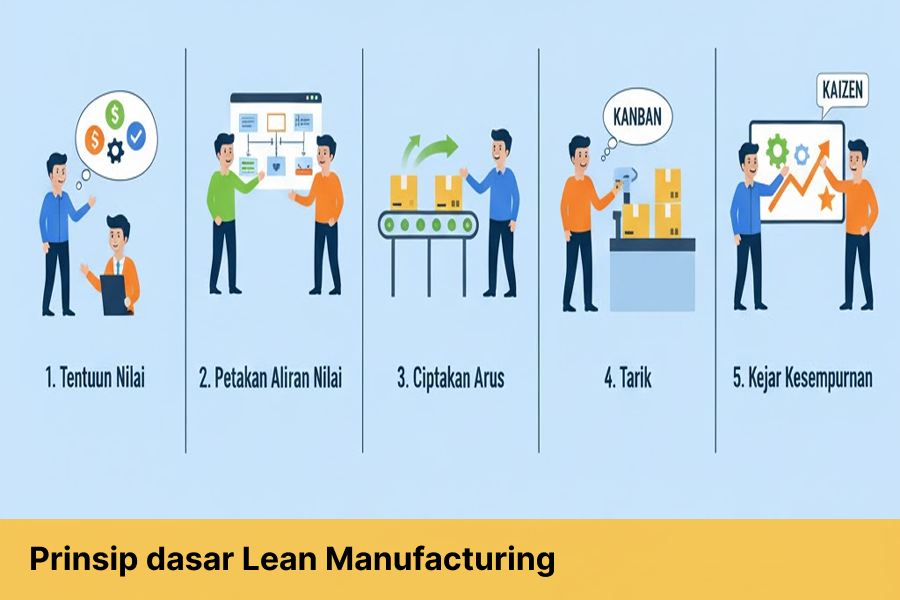
The principles are straightforward on paper. Define value from the customer's perspective. Map the value stream to see every step. Make value flow without interruption. Let the customer pull production through the system. Chase perfection through continuous improvement. The Indonesian phrase you referenced basically translates to the principles and benefits that make companies more effective. It's the same framework, just localized terminology. Where beginners go wrong is treating these as a checklist. They're not. The first principle, defining value, is the hardest one and the one most people skip because it requires actual conversations with customers instead of assumptions from a sales report. A value definition exercise I ran once took four days of interviews before we realized our "premium" product feature was something zero customers asked for and another core feature they cited constantly was deprioritized in engineering. That single insight reoriented the entire product roadmap.
How the Principles Work in Practice
Value stream mapping is the backbone. You draw every step a product takes from raw material to delivery, including wait times, storage, quality checks, and transport. The map usually looks nothing like what anyone expected. In one case, a component sat in a staging area for 18 hours between two operations that each took six minutes. The bottleneck wasn't production speed. It was material handling. Pull systems replace forecast-driven pushing. Instead of building to a schedule and hoping demand catches up, you produce only when downstream demand signals it. Kanban cards or digital equivalents trigger each movement. This sounds simple but requires stable demand patterns and reliable suppliers. I've seen pull systems fail in environments where lead times are unpredictable and suppliers can't respond within a single shift. In those cases, a hybrid approach with strategic buffer stock at certain nodes works better than a pure pull model. Jidoka, or automation with a human touch, means machines or processes stop automatically when an abnormality occurs. This isn't about expensive robotics. It's about building quality into the process so defects don't cascade. The Andon cord system at Toyota is the famous example, but you can implement the same logic with simple visual indicators. A red light, a flagged bin, a digital alert. The point is immediate visibility, not elaborate technology.
Get the Full Details

Heijunka, or production leveling, smooths out the mix and volume of production over time. Instead of running a batch of 200 identical units then switching to a different product, you alternate between variants in smaller increments. This reduces inventory swings and makes the flow more predictable. The tradeoff is slightly more changeover time, which is why Toyota invested heavily in SMED, or single-minute exchange of dies, to keep changeovers under three minutes. If your changeovers take 45 minutes, heijunka will hurt your throughput rather than help it.
The Benefits Are Real but Not Universal
Companies that implement lean correctly typically see inventory reduction of 30 to 60 percent, lead time improvements in the same range, and defect rate reductions that often exceed 50 percent. These aren't theoretical. They're documented across industries. But the results depend entirely on implementation fidelity. The biggest pitfall is treating lean as a cost-cutting exercise rather than a flow optimization exercise. When you cut staff without fixing the underlying flow problems, you just create more work for the remaining people. The system becomes leaner in name only and more brittle in practice. I watched a facility apply lean tools during a downturn and end up with higher error rates because the remaining team was too overwhelmed to maintain the new standards. Cost went down temporarily. Effectiveness went down permanently. Another common mistake is investing in lean training for managers without empowering floor workers to stop the line or suggest changes. Toyota's system relies heavily on worker authority. If the people doing the work can't flag problems or propose fixes, you lose the continuous improvement engine. Kaizen events are useful for quick wins, but they don't substitute for daily improvement habits embedded in the work routine.
Lean also struggles in low-volume, high-variety environments where standardization is inherently limited. If every job is fundamentally different, the concept of a repetitive value stream breaks down. Some firms in those environments adapt by creating modular value streams around common sub-processes rather than finished products. It works, but it requires a different mapping approach than the textbook examples show.

What to Do First if You're Starting Out
Pick one product family and map its current state value stream yourself. Don't delegate this. Sit with the data, walk the floor, and record actual times, not textbook times. You'll find discrepancies that tell you more than any software dashboard ever will. Identify the constraint. Not the busiest station. The constraint. The constraint is the step that determines the output rate of the entire system. Fixing anything else is optimization theater. Theory of Constraints and lean are compatible, and applying both together prevents the common mistake of improving non-constraint steps while the bottleneck still dictates throughput. Implement a small pull system in one area before scaling it. Start with a two-bin kanban between two adjacent processes. Measure the results for two weeks. Then decide whether to expand or adjust. Most organizations skip this and try to pull the entire factory simultaneously, which creates chaos.
Accept that lean is never finished. Toyota has been refining this system for decades and they still run kaizen events weekly. If your leadership treats lean as a program with an end date, it will fail. It's a operating model, not a project. The Toyota lean manufacturing principles and benefits that make companies more effective aren't about perfection. They're about making problems visible so they can be solved. The companies that succeed are the ones that don't fear seeing the mess, but use the mess as the starting point.