What TiN Coating Actually Does
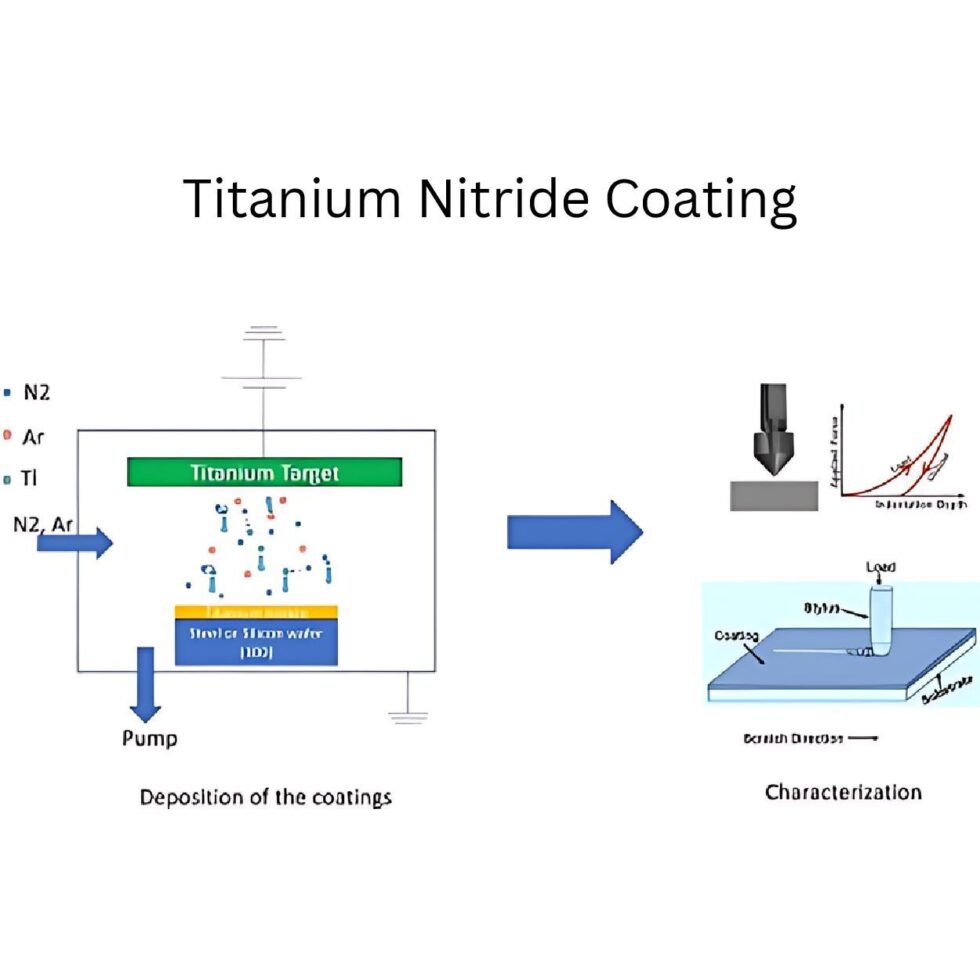
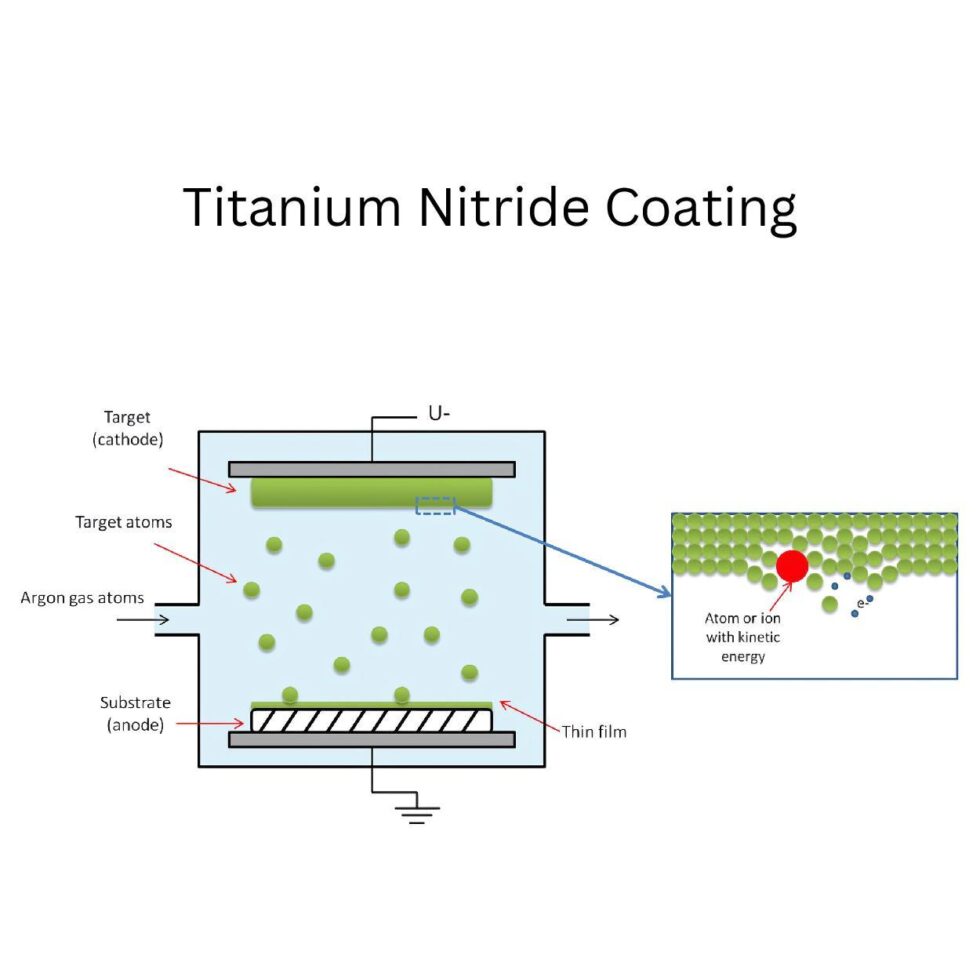
Titanium nitride is a PVD coating most people see on drill bits, end mills, and CNC inserts because it looks gold and wears better than bare steel. That isn't really the whole story. The coating is hard, roughly 2200 to 2600 HV depending on deposition conditions, and it reduces friction against workpiece material. It also acts as a diffusion barrier at moderate temperatures, which matters more than the hardness does in most machining operations. This guide assumes you're either getting parts coated by a job shop or running your own PVD setup. The fundamentals stay the same regardless. Start with a clean, properly prepared substrate. Any oil, coolant residue, or micro-scale oxide layer will wreck adhesion, and you won't catch it by looking. Parts go through ultrasonic cleaning in acetone, then isopropanol, then dry under nitrogen. After that they enter the vacuum chamber for an ion etch step. This is where argon plasma bombards the surface and removes native oxides without any chemical additives. Typical parameters sit around 400 to 800 volts on the substrate bias, 10 to 20 millitorr argon pressure, and 15 to 30 minutes of etching time before any titanium or nitrogen gas enters the system.
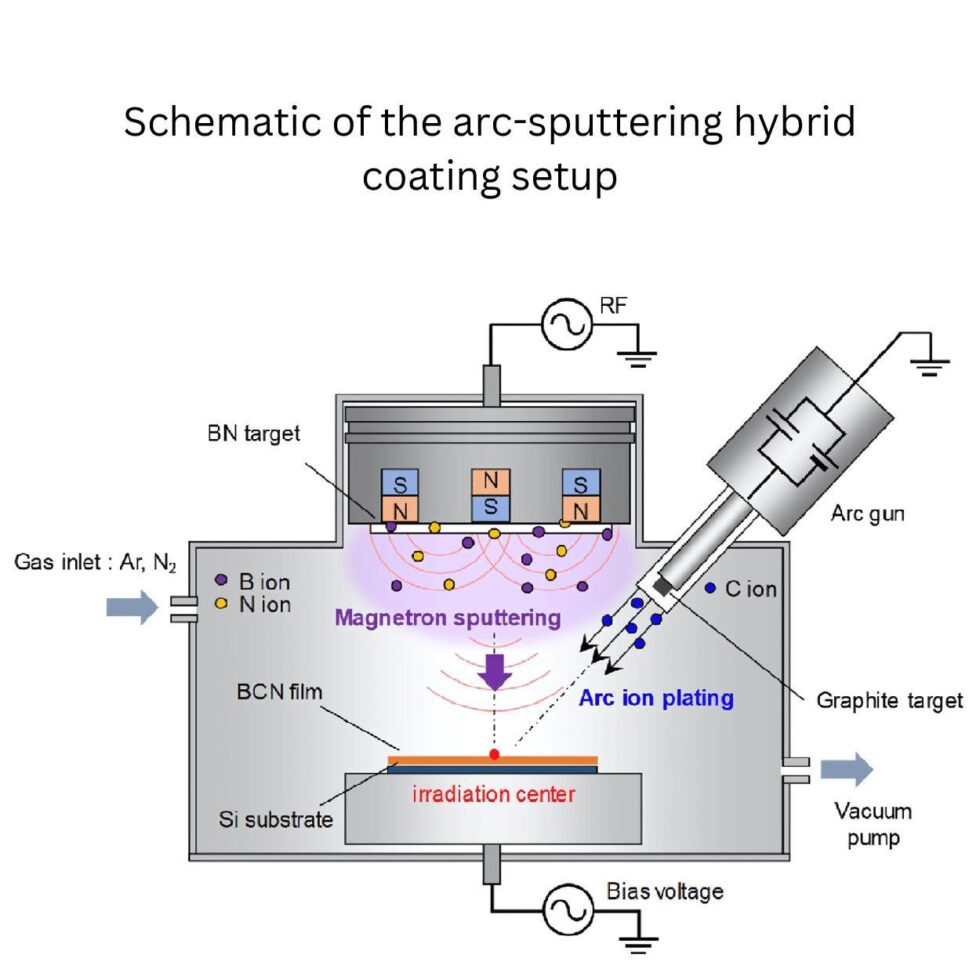
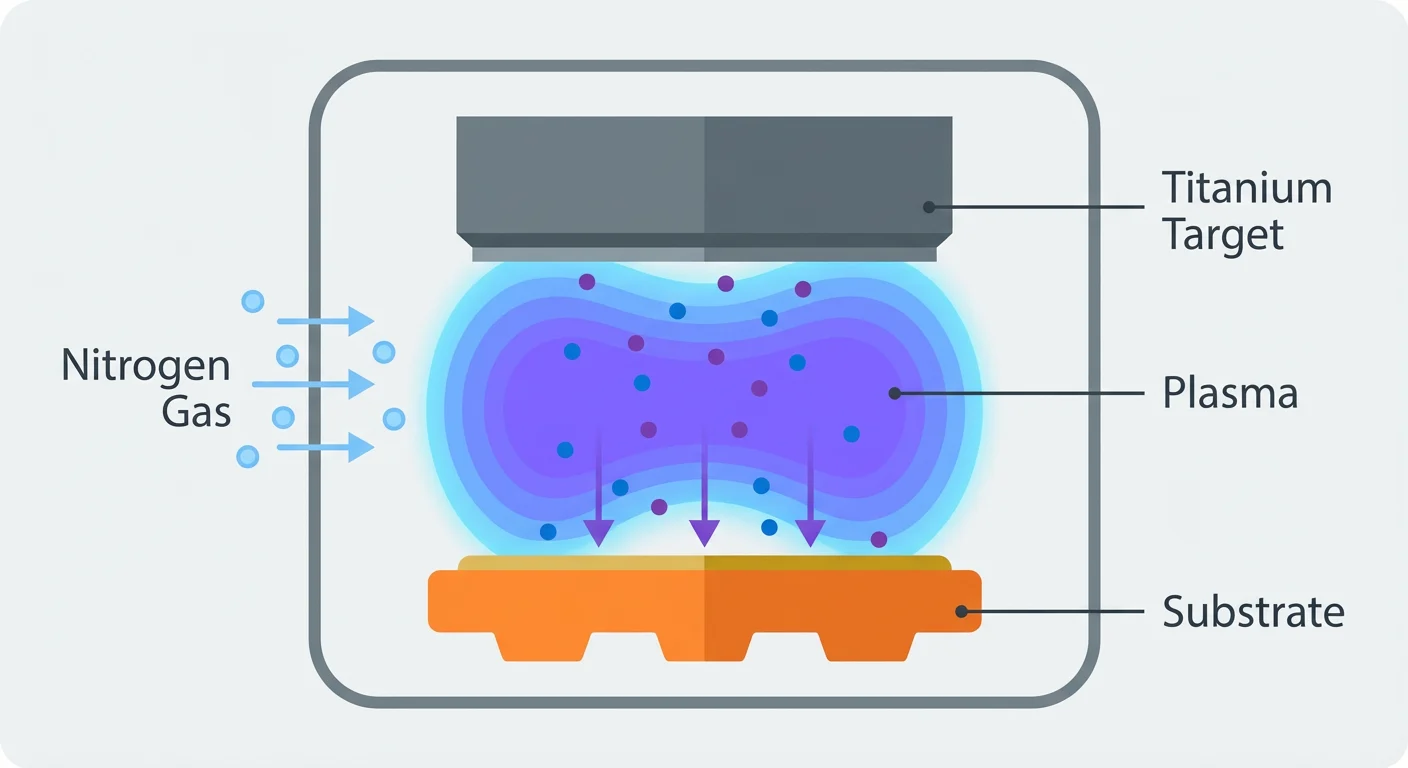
Once the substrate is etched, you introduce titanium into the chamber. Cathodic arc evaporation is the most common method for tool coatings. An electric arc hits a titanium cathode target, vaporizing tiny droplets of molten titanium that ionize and travel toward the parts. Nitrogen gas is bled into the chamber at a controlled ratio, usually between 10 and 30 percent of the total gas flow, and the titanium reacts with it as it deposits. The result is TiN on the surface. If you're using magnetron sputtering instead, the process is slower but produces fewer particles and a smoother film, which matters for precision components that can't tolerate micropitting. Deposition temperature typically runs between 350 and 550 degrees Celsius for tool steel substrates. Going above 550 risks tempering your hardened tool and softening the base material. That's why some shops pre-hardened parts to HRC 65 or higher, then coat them, accepting that the coating temperature will slightly reduce surface hardness near the interface. For HSS tools that haven't been through a final hardening step, the temperature window is much tighter, around 300 to 400 degrees, because the tool will lose its temper if you push it higher.
What Goes Wrong in Practice
Coating delamination is the most common failure, and it almost always traces back to one of three things: inadequate ion etching, contamination introduced during transfer between steps, or a coating thickness that exceeded the adhesion limits of the substrate. A typical cutting insert might need 2 to 4 microns of TiN. Going thicker doesn't help. At 6 microns and above, internal stress in the film becomes significant, and the coating starts cracking under thermal cycling during cutting. The user sees spalling after a few passes and assumes the coating is low quality, when really they just asked for too much material. Another issue that beginners miss is the shadowing effect. If you're coating complex geometries like threaded inserts or deep hole drills, areas that the plasma can't reach directly will stay uncoated or be very thin. Job shops handle this by using rotating fixtures and multiple arc sources positioned at angles, but even then, certain valleys inside a thread profile might only get 30 to 50 percent of the nominal thickness. If your application depends on coating inside a threaded feature, tell the coater upfront or plan to machine a post-coat fit. I once had a batch of carbide end mills come back from a coater with a beautiful gold finish and a hardness reading that checked out. The first machining run destroyed them. The problem turned out to be trapped hydrocarbon contamination from the cleaning solvent. The ultrasonic cleaner had been running on a schedule that hadn't been updated in six months, and the acetone was saturated with previous batch residues. The parts looked clean but carried a monolayer of organics that prevented proper ion etching adhesion. I switched to fresh solvent, shortened the cleaning cycle to two cycles of 10 minutes each, and ran a peel test on sample coupons before committing the full batch. The second run lasted three times longer. I still don't know exactly which contaminant was responsible, but the correlation between fresh solvent and the improvement was clear enough that I never skipped the peel test again.
Get the Full Details
Substrate Choices Matter
TiN adheres differently depending on what it's coating. Carbide tools are the standard application and work well with standard parameters. High-speed steel requires lower deposition temperatures and often a thicker intermediate layer to accommodate the different thermal expansion coefficient. Stainless steel substrates for wear applications need a careful balance because the chromium oxide layer that naturally forms on the surface is stubborn. Some coaters use a titanium interlayer of 0.2 to 0.5 microns before depositing the TiN, which improves grip on reactive metal surfaces. Aluminum and brass substrates are problematic. TiN bonds poorly to soft metals at typical deposition temperatures, and the hardness difference between the coating and the base material causes rapid wear on the substrate underneath. If you need a gold-colored hard coating on aluminum, consider chromic anodizing instead, which grows the coating from the substrate material itself rather than depositing it on top.
Post-Coating Handling
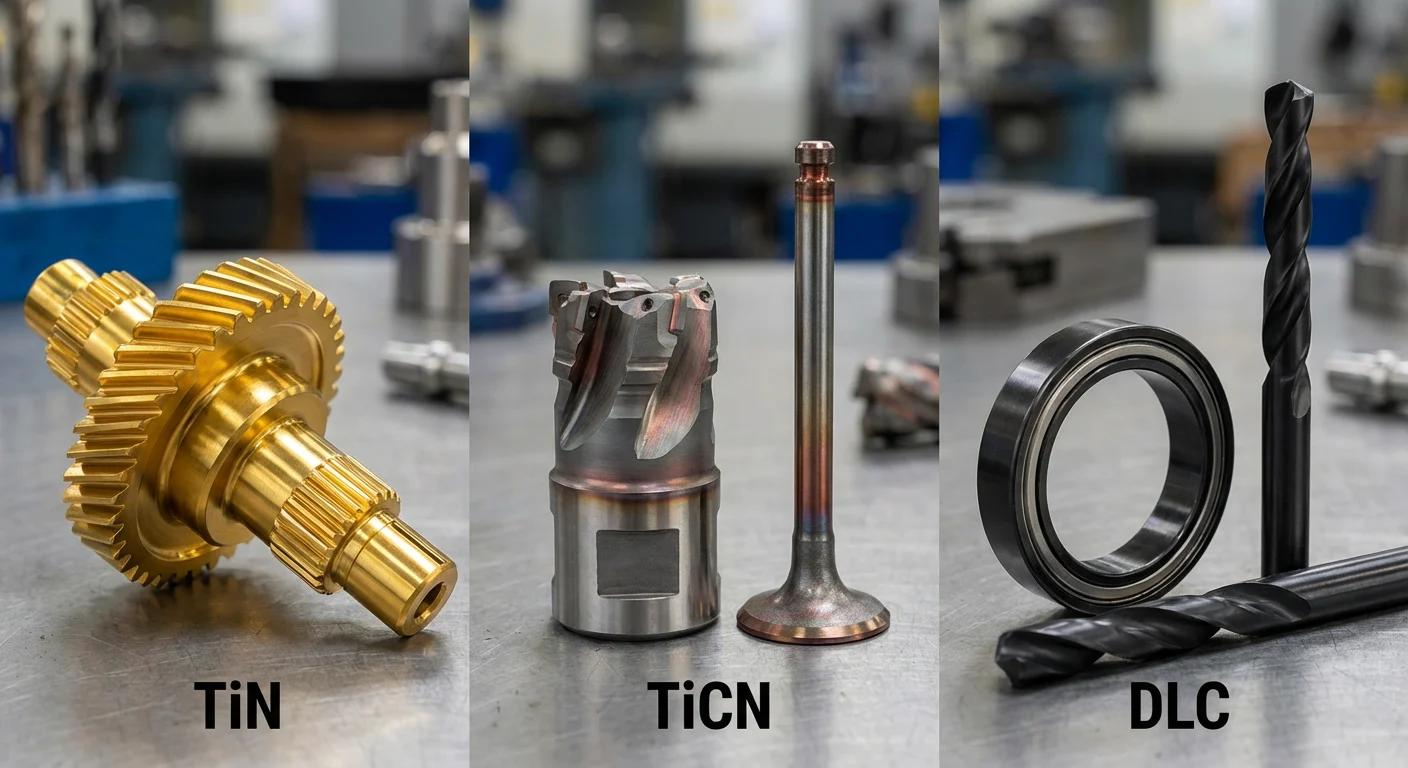
Once the coating comes out of the chamber, handle the parts with clean gloves. Fingerprints contain salts and acids that attack the coating surface over time, especially in humid environments. Don't sand or grind the coated surface unless you're intentionally removing the coating for touch-ups. TiN is hard enough to scratch standard abrasive papers, and trying to polish it with conventional compounds just embeds abrasive particles into the film. If you need to restore a worn coating edge on a tool, the only reliable approach is to strip it completely using a reverse ion etch in the PVD chamber or a chemical dip, then recoat from scratch. TiN has real limitations. It reacts with ferrous materials at elevated temperatures, which is why it's generally avoided for high-speed steel machining of steel at cutting speeds above 100 surface feet per minute. The nitrogen in the coating can diffuse into the workpiece and cause built-up edge formation. In those situations, titanium carbonitride (TiCN) or aluminum titanium nitride (AlTiN) perform better because the carbon or aluminum content raises the thermal stability and reduces chemical affinity for iron-based materials. For non-ferrous machining like aluminum or copper, TiN can actually promote galling because the coating has a high affinity for those soft metals. DLC, or diamond-like carbon, is the standard alternative there. It's slippery, not hard in the traditional sense, and it stays clean on sticky materials. The tradeoff is that DLC is softer and wears faster on abrasive materials like cast iron or composite carbon fiber.
Quality Verification
A simple visual check gets you so far. Consistent gold color without bluing or discoloration indicates even deposition. Use a coating thickness gauge, preferably an eddy current or X-ray fluorescence unit calibrated for TiN on your specific substrate material. Spot readings across the part should vary no more than 15 to 20 percent from the target thickness. Adhesion testing can be done with a cross-hatch tape test for production acceptance, though that method is qualitative at best. For more reliable data, a scratch adhesion tester with a Rockwell-indenter tip loaded at increasing force until coating delamination occurs will give you a critical load value. TiN on carbide typically clears 40 to 60 newtons of critical load with a good deposition. Below 30 newtons, the coating is marginal for any serious cutting application. Hardness verification with a microhardness indenter at 100-gram load is standard. Expect 2200 to 2600 HV for a properly deposited TiN layer. If your readings are consistently below 2000 HV, the nitrogen flow ratio was likely too low during deposition, or the substrate bias voltage was insufficient to densify the film.
Cost and Turnaround Realities
Job shop coating for a small batch of cutting tools usually runs between 80 and 250 dollars depending on part size, quantity, and whether you need a specific thickness range. A full production run of 500 inserts might drop the per-part cost to under a dollar in coating fees alone, but fixture setup and chamber loading time add a flat minimum charge. Lead times of 5 to 10 business days are normal. Rush service at double the price is available from most shops but rarely saves more than 2 days because the coating cycle itself is the bottleneck, not the paperwork. If you're considering in-house coating, a basic cathodic arc PVD system capable of tool-grade TiN runs in the 75 to 150 thousand dollar range for a production-capable unit. Smaller research-grade systems exist for under 40 thousand but will not match the throughput or consistency of a dedicated tool coater. The real cost isn't the equipment, it's the skilled operator. Getting stable coatings consistently requires someone who understands vacuum physics, plasma behavior, and thermal management. That person costs money, and training them takes time that most shops don't have to spare.
Summary Parameters for a Standard TiN Coat on Carbide Inserts
Substrate prep: ultrasonic clean in fresh acetone and IPA, dry with filtered nitrogen. Ion etch: 600V bias, 15 mTorr argon, 20 minutes. Deposition: cathodic arc titanium, nitrogen partial pressure at 20 percent of total, substrate bias at 30V during growth, temperature held at 450C. Target thickness: 3 microns. Post-coat cool under vacuum to below 100C before chamber venting to prevent oxidation of the hot coating surface. Handle with gloves, inspect with thickness gauge and scratch adhesion test before shipping. Those numbers are a starting point, not a guarantee. Every machine, every batch of inserts, and every lot of titanium target material behaves slightly differently. Run a qualification batch first, measure everything, and adjust from there. The coating industry runs on incremental refinement, not on following a recipe exactly.