Why Your Measurements Keep Confusing You
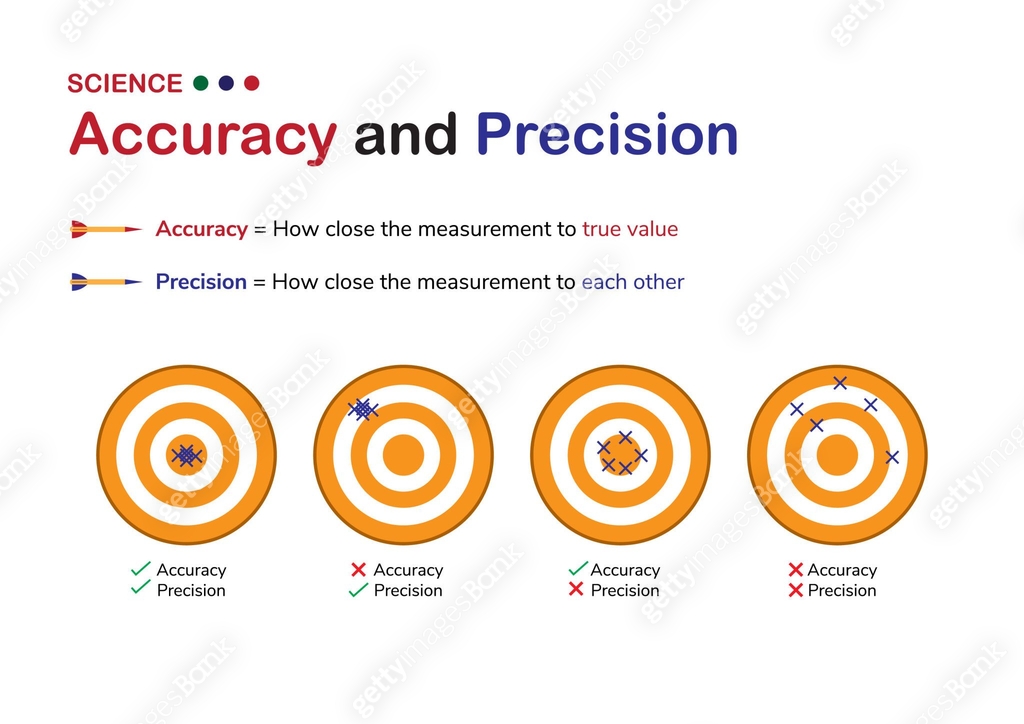
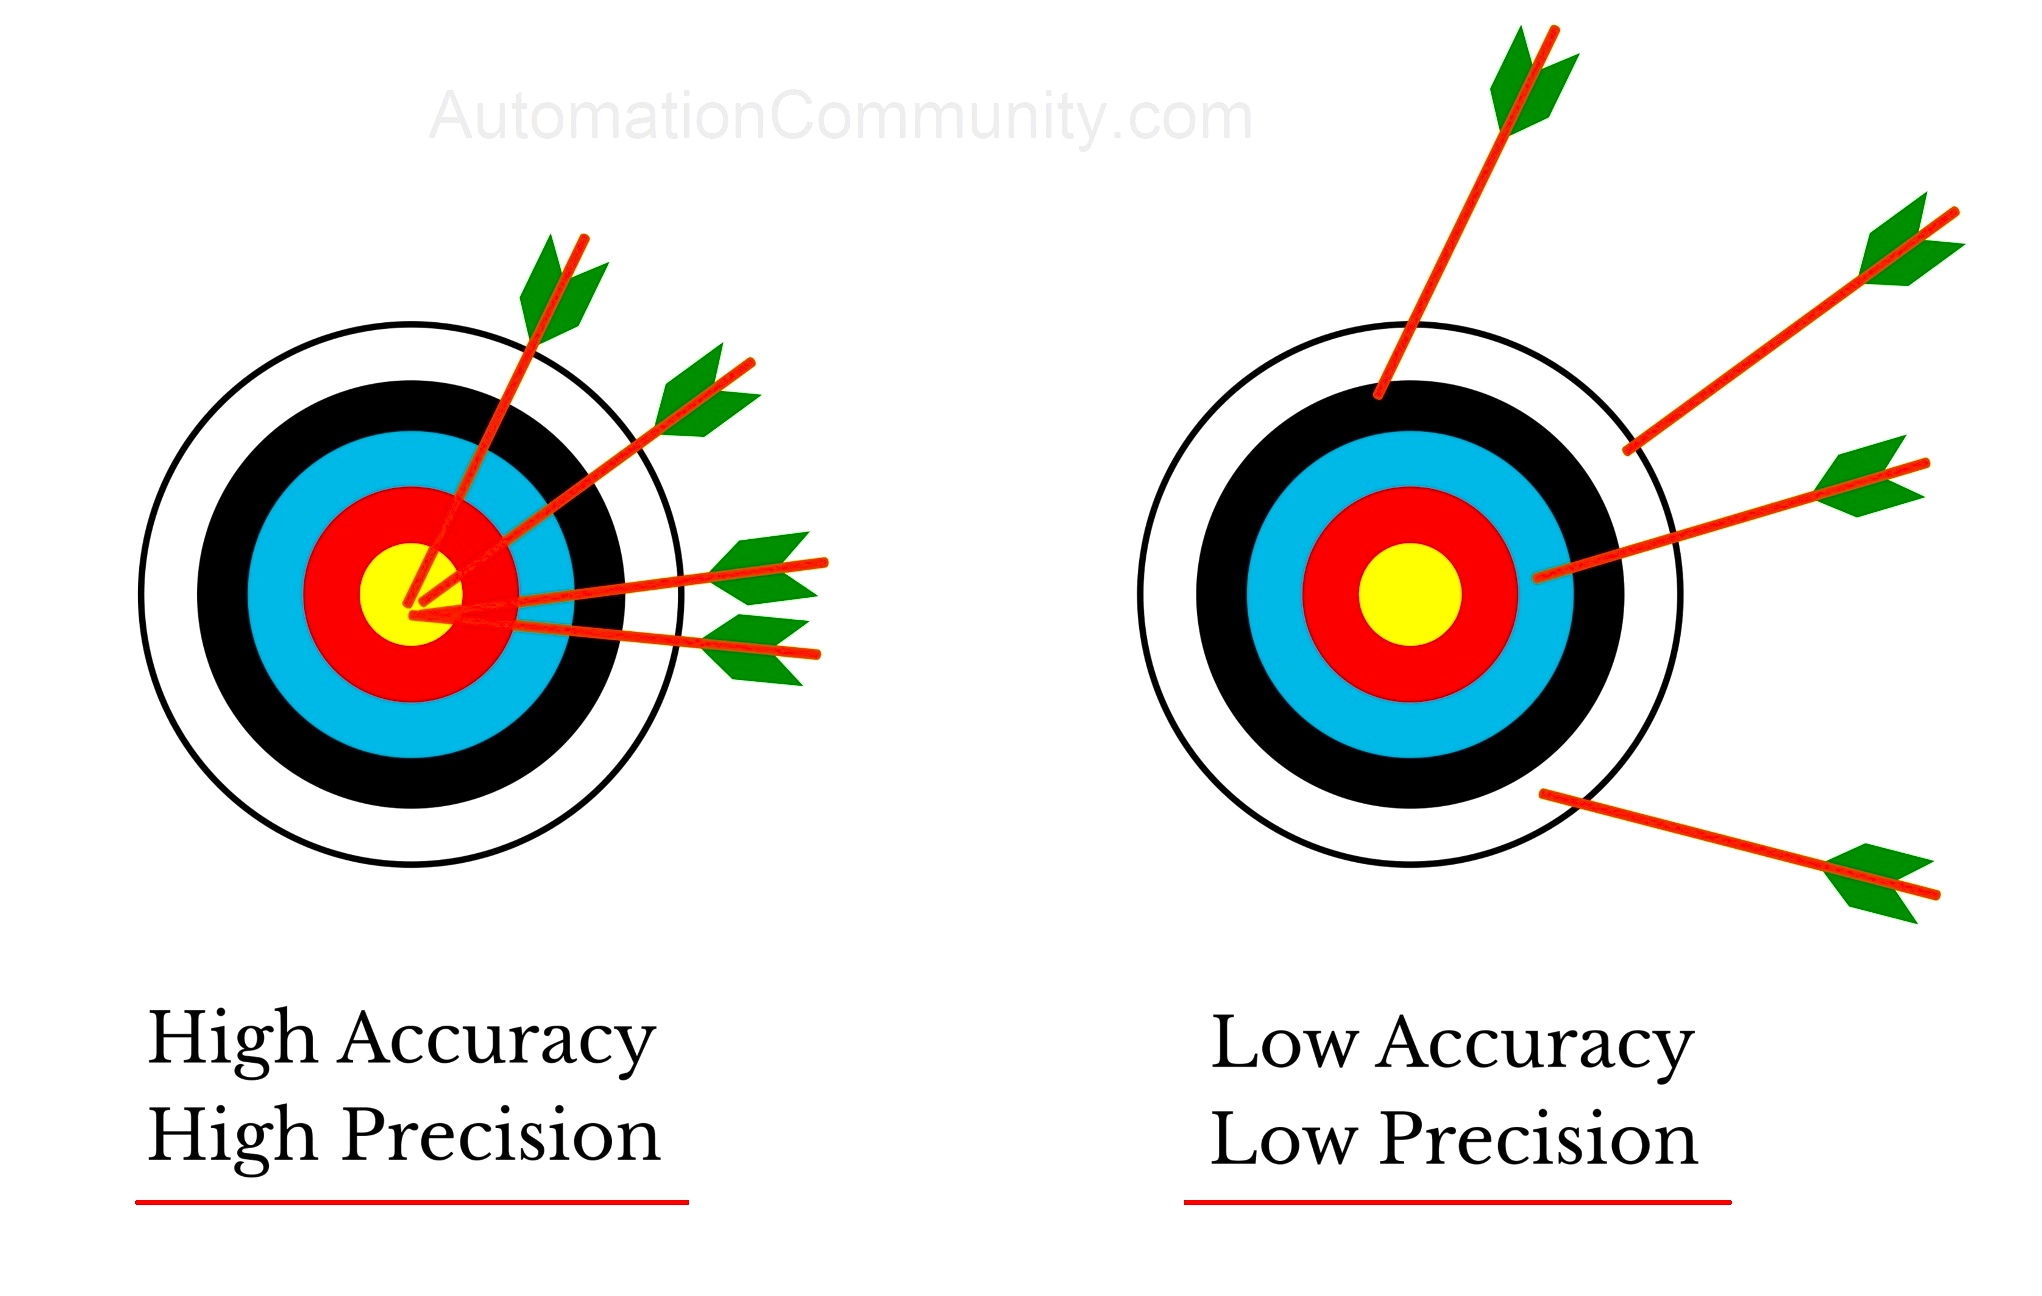
I spent three weeks trying to figure out why a calibration lab kept rejecting our part dimensions before I realized I was thinking about precision and accuracy as the same problem. They aren't. The distinction isn't philosophical — it's the difference between a tool that works and one that destroys your batch yield. Here is how to stop mixing them up and actually use each one. Precision describes repeatability. If you measure the same thing ten times and get nearly identical numbers every time, your process is precise. Accuracy describes correctness. If those identical numbers are consistently wrong by two millimeters, your process is precise but inaccurate. You can have both, neither, or any combination. The combinations matter more than the definitions because they determine what fix to apply.
The War Between Precision And Accuracy Separating The Two Essential Concepts
In my work, the most common failure mode is treating a precision problem as an accuracy problem. Let me walk through the method first because that is where most people get tripped up. Step one: take twenty repeated measurements under identical conditions. Do not adjust anything between readings. Record everything. If the standard deviation is large relative to your tolerance, you have a precision problem. If the standard deviation is small but the mean is offset from the target, you have an accuracy problem. If both are bad, fix precision first because calibrating an imprecise instrument gives you false confidence. I once had a CMM (coordinate measuring machine) that was producing parts that measured perfectly within tolerance on our floor but failed incoming inspection at the customer site. The CMM was precise — readings repeated to within 0.001mm — but it was reading 0.004mm high across all axes due to a thermal drift I had missed. The fix was not recalibration. It was installing a temperature stabilization protocol and adding a daily artifact check before production runs. That cut our rework rate from about eighteen percent down to under two percent within a month. The customer's CMM happened to be calibrated correctly, which meant our "good" parts were actually slightly oversized. We were precisely wrong.
There are two things beginners consistently miss about this distinction, and both cost people real money. First, precision is scale-dependent in ways that confuse people. A measurement system might show a standard deviation of 0.05mm, which looks terrible for a 100mm part but is completely acceptable for a 10mm feature. The gauge capability ratio (Cg/Cgk) accounts for this by expressing precision relative to the tolerance band rather than as an absolute number. You should always use this metric instead of raw standard deviation when evaluating whether your measurement system is adequate. Second, accuracy and precision trade off against each other in ways that are rarely discussed. When you increase measurement speed to boost throughput, precision usually degrades because the sensor integrates over a shorter window. This means your production line might become more accurate on average (less drift over time) but less precise (higher per-part variance). The right choice depends entirely on whether your downstream process is sensitive to the mean or the spread. In machining, spread usually kills you first. In assembly, mean offset usually does.
Get the Full Details

The Gage R&R study is the standard framework for separating these effects properly. It breaks measurement variation into three components: repeatability (same operator, same part, same setup), reproducibility (different operators or setups), and part-to-part variation. Most people skip the reproducibility portion because it takes more time, but that is where hidden accuracy problems live. I learned this the hard way when a new technician on my team started getting consistently different readings on the same fixture. Her technique was slightly different — she was seating the probe at a three-degree angle instead of perpendicular. That introduced a systematic accuracy error that only showed up under reproducibility testing. The precision numbers looked fine in isolation. Here is the blunt truth about when this framework fails: it assumes your measurement process is linear and your errors are normally distributed. Neither assumption holds in real manufacturing. Thermal expansion in aluminum parts creates non-linear dimensional shifts that change throughout the day. Runout in a spindle creates periodic error patterns, not random noise. If your error distribution is not normal, standard deviation becomes a misleading metric and you need to look at percentiles or use a non-parametric capability analysis instead. I had a situation where the Cpk looked healthy at 1.67 but the actual defect rate was much higher because the distribution had a heavy tail caused by tool wear. The tail was invisible in the standard report. For situations where traditional Gage R&R does not apply — like optical measurements, subjective visual inspections, or processes with very long cycle times — you need a different approach. Attribute agreement analysis works better there, though it is less sensitive to small systematic biases. If your process involves human judgment, precision and accuracy split even further apart because human observers introduce their own consistency and correctness variances independently of the measurement device.
A practical shortcut for the field: run a known reference standard through your measurement system at the start and end of every shift. Track the mean shift and the range separately. The mean shift tells you about accuracy drift. The range tells you about precision degradation. Plotting both on separate control charts lets you catch problems before they reach production. This alone caught a failing spindle bearing on my line before it produced a single bad part. The precision range started widening gradually over six hours, and the accuracy mean hadn't moved at all. The bearing was about to fail, and the early warning came from the precision signal, not the accuracy signal. If you are dealing with a process where both precision and accuracy matter equally and your tolerance band is tight relative to your measurement variation, you need a measurement system that accounts for both simultaneously. The Cgk index does this by incorporating both the precision spread and the accuracy offset into a single number. A Cgk below 1.0 means your measurement system is not capable of verifying conformance regardless of what the parts actually are. That is the most important threshold to remember. Everything else is optimization.