Bed Leveling on the Ender V2
The Ender V2 is one of the more common entry-level 3D printers out there. It prints fine when the bed is leveled. It prints poorly when it isn't. That's basically the whole story. Here's how I actually do it. Forget the manual. The manual describes a perfect machine that doesn't exist. Start with the printer cold. Not warm, not at operating temperature. Cold. Let it sit for at least an hour if it's been running. Thermal expansion matters more than people admit. I learned this the hard way when I was getting consistent first-layer failures on large PLA prints — the bed would be perfect at room temperature, then lift at the corners once it hit 60°C. Moving the leveling screws while hot threw everything off.
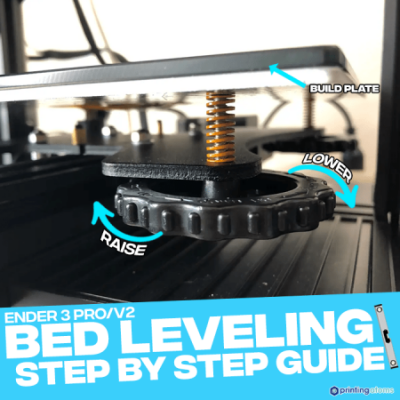
The paper method is standard. Slide a sheet of regular printer paper between the nozzle and the bed. Adjust the spring tension on each corner until you feel slight drag on the paper. Not zero resistance. Not a lot of resistance. A barely-there drag. If the paper slides through completely free, you're too high. If you can't move it at all, you're too low. There are four adjustment points on the Ender V2: two front, two back. But here's the thing nobody tells you — the springs interact with each other. When you tighten one corner, the opposite corner often loosens slightly. Go in circles. Corner one, then the diagonal opposite, then the remaining two. Do it three times. That's usually enough. I use a piece of paper about 80gsm. Thinner paper gives you less feedback. Thicker cardstock binds too much. Regular copy paper hits the sweet spot.
After the manual leveling, run the auto-level routine if your firmware supports it. The Ender V2 with the stock board and an upgraded LCD does. This runs a mesh bed leveling pattern across the surface. It won't fix a wildly unlevel bed, but it compensates for minor imperfections in the build surface. The mesh data gets stored in EEPROM and applies a correction factor to each point during printing. Here's where most people mess up: they skip the calibration cube test. After leveling, print a 20mm calibration cube. If the walls look good but the top layers are thin or gaps show, your Z-offset is wrong. The bed leveling gets the surface flat relative to the nozzle travel path. The Z-offset sets where the first layer actually touches. These are two different adjustments. I had a printer that printed perfectly on the mesh but had a hairy bottom surface every time. Turned out the Z-offset was off by 0.04mm. Fixed that and the bottom layers snapped into place. For the actual first layer, I print a single-line calibration object. A 100mm line with a 0.2mm layer height and 20mm/s print speed. Look at how it squishes. You want it to look like a slightly flattened ribbon, not a round wire and not a scattered dusting of filament. Adjust the Z-offset in small increments — 0.02mm at a time — until the line looks right.
Get the Full Details
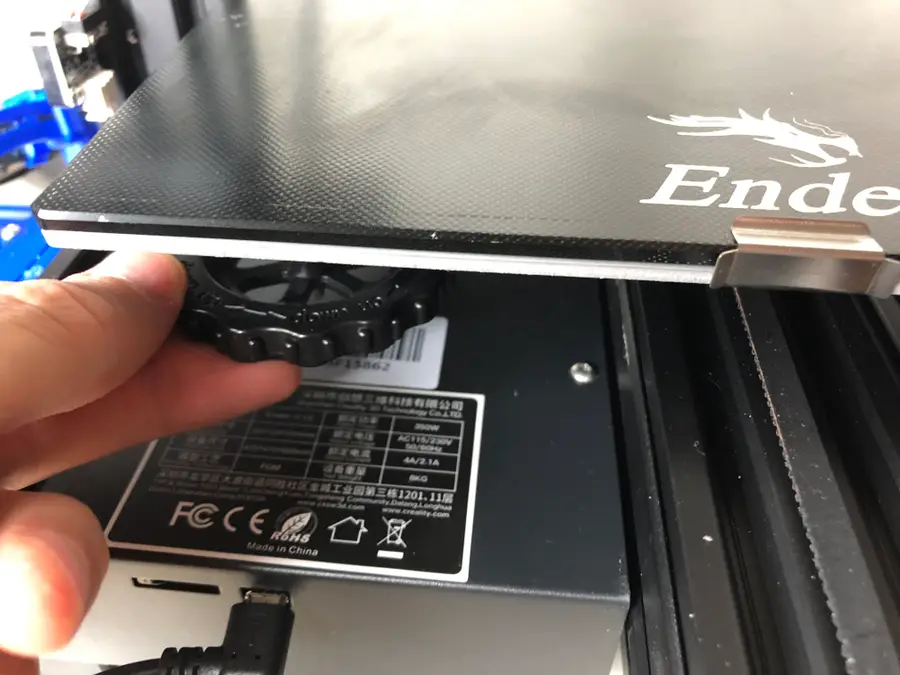
Spring tension is another overlooked area. The Ender V2 uses tension springs on each corner. Over time they lose their rebound. If you find yourself constantly readjusting the screws, the springs might be fatigued. I replaced mine with stronger 3D-printed spacers and new springs from a parts pack. Cost about three dollars. Made a noticeable difference in how long the leveling held. There's a limit to what software can fix. If your bed is warped more than 0.1mm across the surface, mesh leveling will only get you so far. You'll see inconsistencies at the edges. In that case, a magnetic build plate with a thinner, more uniform surface helps more than any firmware feature. I switched to a cold-rolled steel sheet on a magnetic bed and stopped worrying about leveling as much. The surface stayed consistent for months. Common pitfall: people level at the center and call it done. Check all four corners and the center. Five points minimum. The Ender V2's bed is 250x250mm. That's big enough that a small error in one corner becomes a visible problem across the whole print.
Another one: forgetting to check the belt tension after adjusting the bed height. When you turn those leveling screws, you change the Z-height of the hotend relative to the frame. If your Z-axis belts were already borderline, this can introduce wobble. Tighten them so there's about 5mm of deflection when you press the belt midway between pulleys. If you're getting adhesion issues on the first layer that leveling doesn't fix, check the nozzle height at multiple points during a print. Sometimes the issue isn't the static bed level but Z-hop or backlash in the Z-axis. Run a diagnostic print and watch the first layer with a flashlight at an angle. You'll see inconsistencies immediately. Download the official Creality firmware updates occasionally. They patch bed leveling routines and sometimes improve mesh resolution. The stock firmware has some rough edges around the auto-level function that get smoothed out in newer versions. Not a game-changer but worth doing.
The bottom line is that bed leveling on the Ender V2 is a process, not a one-time task. Print a few test objects, check the first layer, adjust, repeat. Once you know how your specific machine behaves at temperature, you'll develop a quick routine that takes maybe ten minutes. Before that, expect to spend more time figuring out what's actually wrong than fixing it.