Why This Conversion Keeps Coming Up
Millimeters and inches live in different worlds on most shop floors. I once had a supplier quote a bracket in inches while our assembly drawings were all in metric. The mounting holes were listed as 0.591 inches instead of 15mm. That's a 0.004-inch gap per hole. Fine for a loose fit, terrible if you're pressing a bearing in. We had to re-cut the part rather than force it. That kind of mismatch costs time, not just money. The exact conversion factor is one inch equals exactly 25.4 millimeters. That definition has been locked in since 1959. It is not an approximation. When you divide 15 by 25.4, you get 0.5905511811 inches. Most people round that to 0.5906 or 0.591 depending on what tolerance band they are working in. Set up a simple ratio or just type 15 ÷ 25.4 into any calculator. The result is 0.5905511811023622 inches. Do not trust a phone app that rounds aggressively. I saw one tool return 0.6 inches for 15mm during a quick check. That error is over 15 thousandths of an inch, which will throw off a stack-up calculation faster than you can blink.
If you need more precision, keep at least four decimal places in your intermediate work and round only at the end. A good rule of thumb is to carry one extra digit beyond your target tolerance. Working in a spreadsheet is fine, but lock the cell format so it does not silently round your numbers when someone else opens the file.
When 0.5906 Inches Is Enough And When It Isn't
For general fabrication, a tolerance of plus or minus 0.005 inches covers most situations. That means 0.5906 inches is perfectly adequate. Your CNC mill or lathe will hold that without breaking a sweat. Even hand filing a slot to that dimension is straightforward with a decent. Precision assemblies demand more care. In my experience with optical mounts and bearing housings, a 0.001-inch mistake can mean a press fit that either jams or slips. If you are designing something where 15mm is a critical stack dimension, specify the decimal as 0.5906 inches with a tolerance of plus or minus 0.0005 or tighter. That way the machinist knows exactly how far they can drift before the part becomes scrap.
Get the Full Details
Common Mistakes That Waste Hours
The first mistake is assuming that rounding to three decimal places is always safe. Two decimal places gives you 0.59 inches, which is off by nearly four thousandths. That is the difference between a sliding fit and a rattling fit in a mechanism. The second mistake is mixing up conversion direction. Dividing by 25.4 goes from millimeters to inches. Multiplying by 25.4 goes the other way. I have seen junior designers multiply a millimeter value by 25.4 and then call it inches. That produces a number wildly too large. A quick sanity check helps here: one inch is roughly 2.5 centimeters, so 15mm should land around 0.6 inches, not 6 inches.
A Practical Workaround I Use All The Time
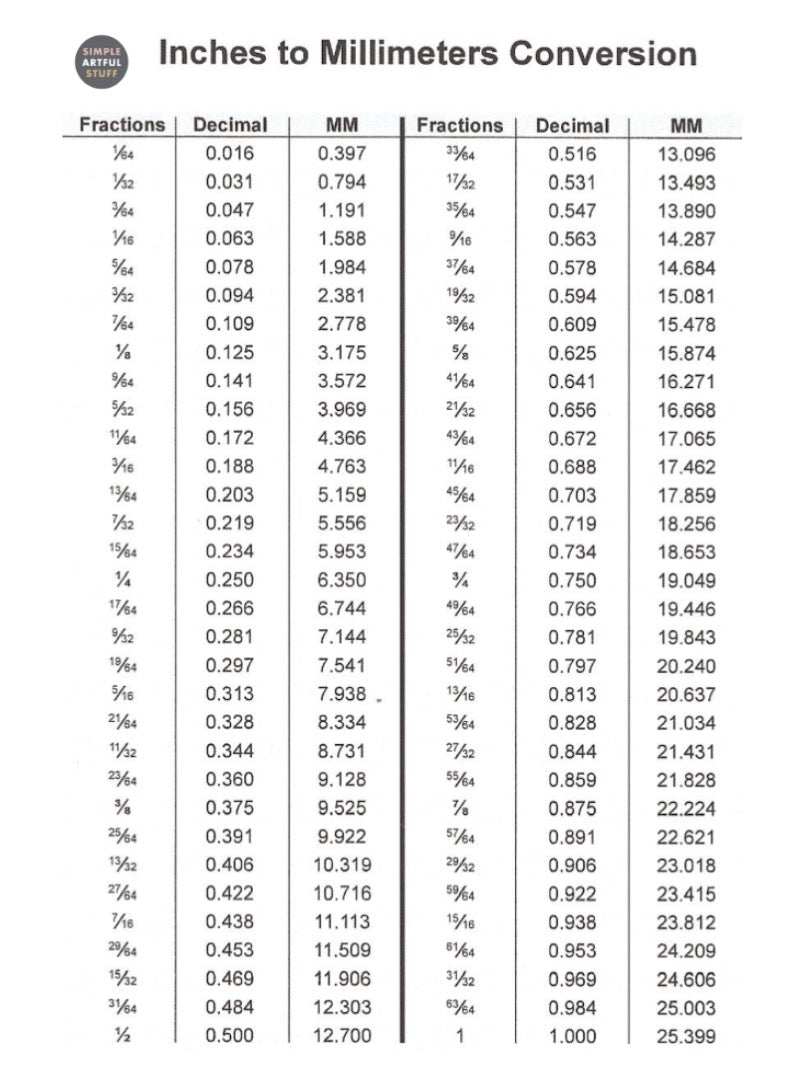
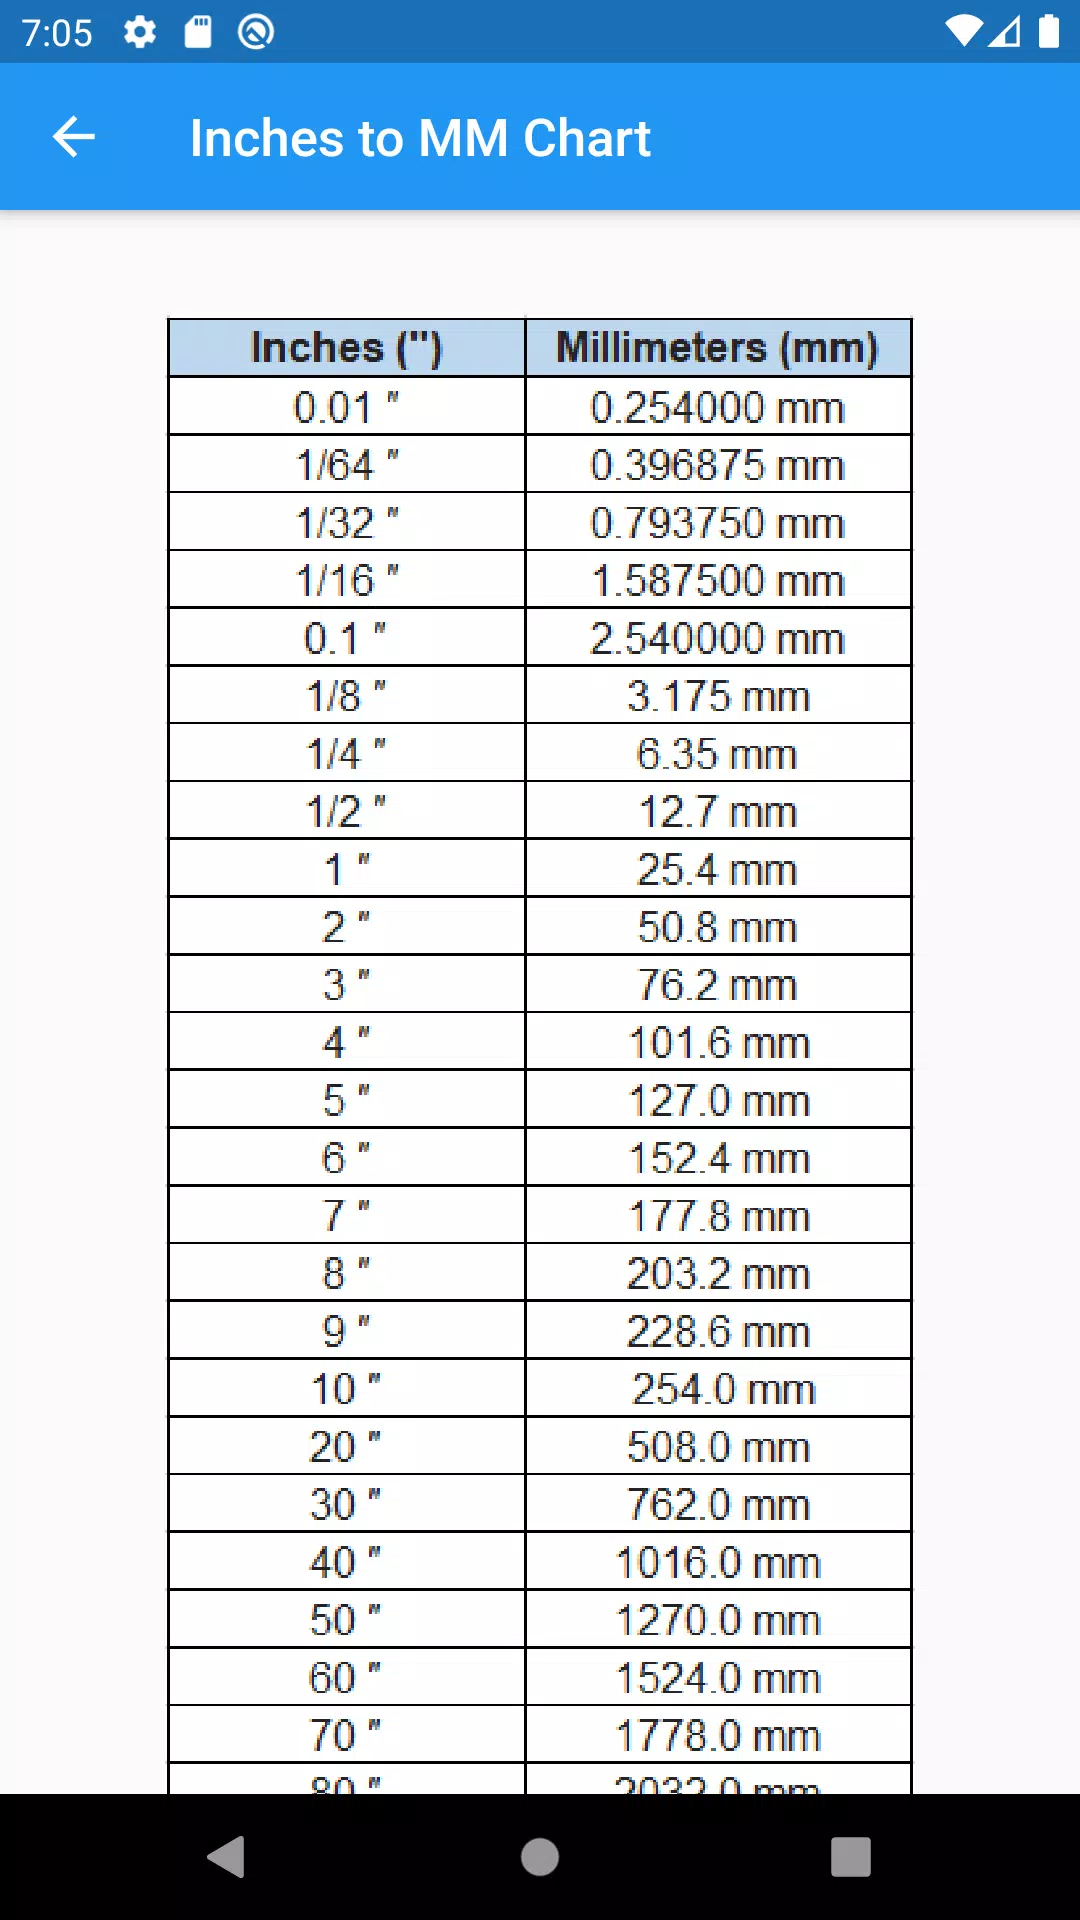
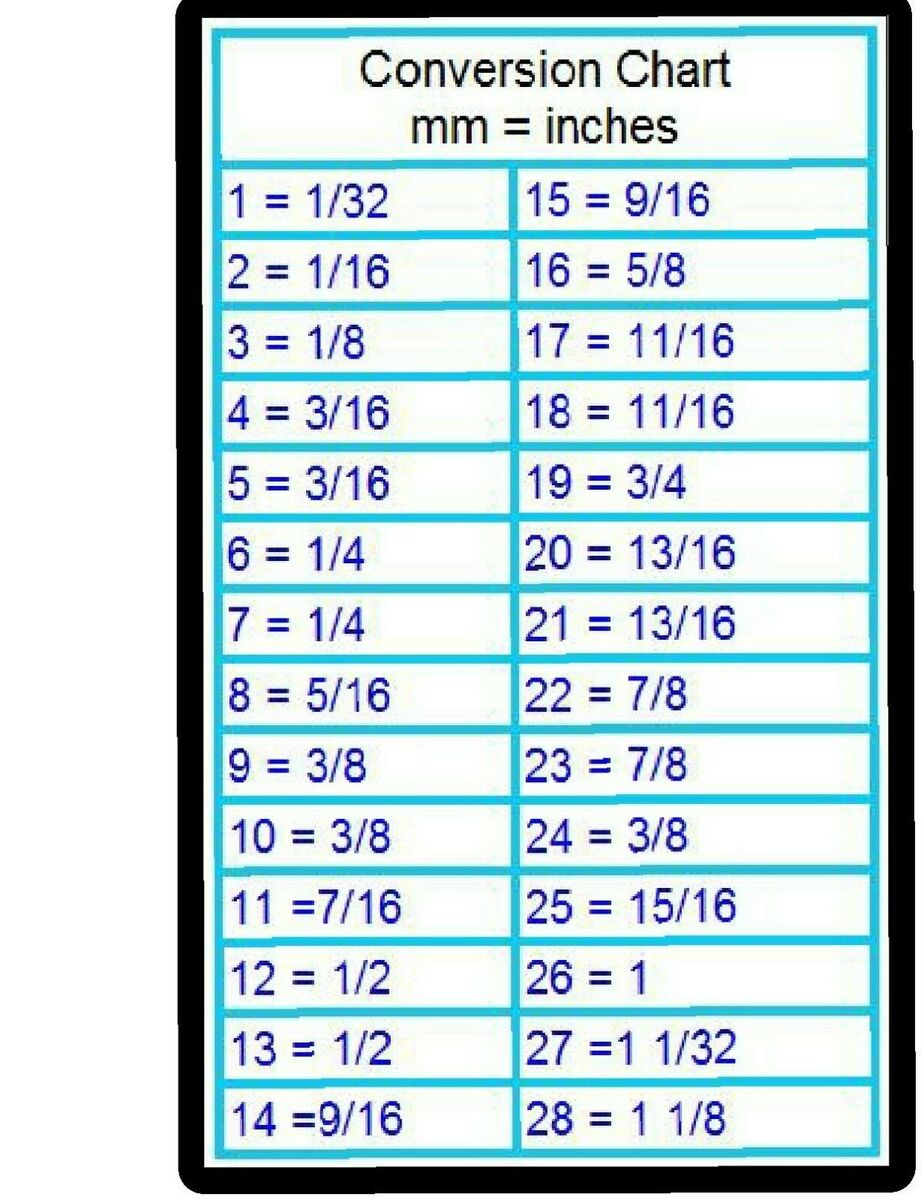
When I need to convert repeatedly, I set up a small reference table inside my CAD environment. A quick script or even a lookup table with millimeter values from 10mm to 20mm in 0.1mm increments saves me from recalculating every time. The values are fixed because the conversion factor is fixed. I store the table as a csv file and reference it whenever a drawing calls for both metric and imperial dimensions on the same part. For single conversions, a physical conversion chart pinned near the workbench is still useful. It sounds old-fashioned, but I have found that flipping to a printed table is faster than opening an app when your hands are greasy and your gloves are on. The chart does not crash, it does not need Wi-Fi, and you do not have to squint at a screen while measuring a part with calipers.
Limitations You Should Accept
No conversion chart will solve a bad datum choice. If your drawing base point is unclear, an exact 0.5906-inch number does not matter because everyone will measure from a different edge. Always establish datums before writing tolerances on a print. Another blunt truth: decimal inch notation is not ideal for thread calls. If your design involves a metric thread like M15, do not convert the thread diameter to inches and expect a clean fit. Standard thread forms differ between metric and imperial systems, and a converted dimension will not produce a matching thread. Use the correct standard designation instead of converting the diameter.

What To Do When Tolerance Stacks Up
If you are building a stack of multiple 15mm features, the individual tolerances add together. Four holes spaced at 15mm centers with a tolerance of plus or minus 0.005 inches each can create a total stack variation of plus or minus 0.020 inches. That is enough to misalign a plate with four mounting points. In those cases, use statistical tolerance analysis or tighten the individual tolerances based on how the parts actually assemble. I once caught this issue on a custom bracket that had five equally spaced 15mm holes. The drawing called for plus or minus 0.005 on each hole. When we assembled it, the last hole was out by almost 0.018 inches. We had to re-machine the plate rather than force the bolts. After that, I started checking stack-ups before sending drawings to the shop. It usually takes ten minutes and prevents a full day of rework.
Quick Reference Values Around 15mm
14mm converts to 0.5512 inches. 15mm is 0.5906 inches. 16mm is 0.6299 inches. If you are eyeballing these on a rule that only reads in inches, the gap between marks gets small fast. A vernier caliper or digital caliper rated to 0.0005 inches is worth the investment if you regularly switch between systems. For makers working in a home workshop, a simple conversion card with the key values from 10mm to 20mm taped to the bench is cheaper than a fancy tool and just as effective for most hobby projects. The card will not fail, and it does not require batteries.