Understanding Steam Temperature Monitoring in Industrial Systems
Most facility managers don't think about steam temperature until something breaks. A heat exchanger drops out. A process goes off-spec. The maintenance crew shows up with a thermocouple and no idea whether the problem is upstream or downstream. Steam temperature codes are one of those things everyone talks about but nobody fully understands until they're dealing with a 200-degree psi deviation at 3 AM. This is the framework I ended up building after three years of chasing phantom condensation failures across three different plants. The core idea is straightforward: steam temperature deviations carry encoded information about system health, and recovering that waste heat is where most facilities leave money on the table. Code red situations happen when you have superheat loss, condensate flash, or heat recovery opportunities that nobody is tracking. I worked at a paper mill in Wisconsin where we were bleeding roughly 400,000 BTU per hour through a vent stack. The temperature gauge on the main header read perfectly fine. But when I ran an infrared scan during a pressure transient, I found a heat drop of about 35 degrees Fahrenheit across a section of pipe that should have been adiabatic. That was our code red moment. We ended up installing a shell-and-tube heat recovery unit that fed back into the feedwater preheat train. The payback was about eleven months. Not dramatic, but consistent. That's the whole point of this system.
How Steam Temperature Codes Actually Work
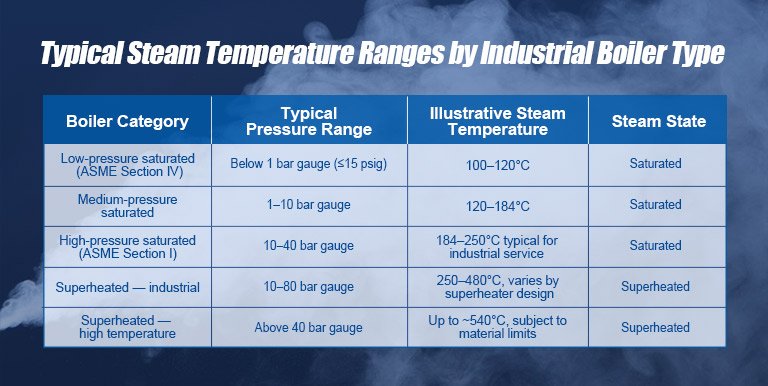
Steam temperature codes aren't an official industry standard. They're a practical classification system that came out of the combined experience of people who actually maintain these systems day to day. Think of it as a diagnostic shorthand. Green means normal operating range. Yellow means you're drifting and should schedule investigation. Orange means active anomaly requiring immediate attention. Red means the system is either failing or you're actively losing recoverable energy. The temperature side of this is what matters most. Saturated steam temperature is tied directly to pressure. At 15 psig, saturated steam sits at about 250 degrees Fahrenheit. At 100 psig, you're looking at roughly 338 degrees. When you see temperature readings that don't match the saturation curve for your measured pressure, something is wrong. Either you have superheat present when you shouldn't, or you've got moisture carryover diluting the thermal energy. Both are expensive problems. Here's what beginners miss: the real issue isn't the temperature itself. It's the delta between measured temperature and theoretical saturation temperature at that pressure. That delta tells you whether you're dealing with superheat, wet steam, or a measurement error. A delta of negative twenty degrees means you've got wet steam. A delta of positive thirty degrees means superheat, which is actually wasted energy if your process needs saturated steam for heat transfer.
Hidden Heat Recovery: The Practical Side
Hidden heat is just waste heat that nobody has bothered to track. Flash steam from condensate lines. Superheat from boiler output. Exhaust from steam tracing. These are all real energy flows that show up as temperature deviations on your instruments but never get captured in your utility budgets. The code red framework forces you to look at them. I remember a food processing plant in Iowa where their condensate return lines were venting directly to atmosphere. The engineer on site thought they were running efficient because the boiler feedwater temperature was stable. But when we plotted the condensate temperature against the trap discharge pressure, we found flash steam being generated at roughly 85 degrees Fahrenheit in a line that was supposed to be subcooled. That's about 1,100 BTU per pound of condensate going straight up the vent. Over a year, that adds up to more than forty thousand dollars in lost fuel at their natural gas rates. The fix wasn't fancy. We installed a closed condensate recovery tank with a flash steam condenser. The flash steam got routed into a low-pressure header that fed a preheating stage. Total cost was under eighty thousand dollars. Annual savings came to about sixty-five thousand. The system has run for four years without a major issue. That's not a perfect system. It required monthly inspections of the condenser tubes and occasional chemical cleaning. But it works.
Get the Full Details
Reading the Code: Practical Diagnostics
When you're on site and you suspect a code red situation, start with the pressure-temperature relationship. Take a simultaneous pressure and temperature reading at three points: boiler outlet, point of use, and condensate return. Plot those against the steam tables. If the curve deviates by more than five degrees from saturation at any point, you've got a problem to investigate. The most common failure mode I've seen is trap field degradation. A single failed open trap on a 100 psig system can vent enough steam to drop your effective temperature by eight to twelve degrees downstream. Over a whole plant with hundreds of traps, that compounds fast. I've walked through facilities where the trap maintenance budget was essentially zero and the steam distribution system was running at what amounted to a chronic code orange state. The temperature readings looked fine on individual headers. The overall system efficiency was terrible. Another thing nobody talks about enough is the effect of load variation on temperature codes. Most facilities design their steam systems for peak load. When you're running at half capacity, the temperature profiles shift entirely. Insulation that was adequate at full flow becomes insufficient at partial load because the velocity drops and heat loss per unit length increases relative to the thermal mass moving through the pipe. I learned this the hard way at a chemical plant where our code green readings in summer turned into code orange by winter, even though the boilers were performing identically. The problem was distribution, not generation.
Building Your Own Monitoring Framework
You don't need a million-dollar DCS system to track steam temperature codes. What you need is consistent data collection. Install temperature and pressure transmitters at strategic points and log them at fifteen-minute intervals. That's it. The logging interval matters more than the accuracy class of your instruments. A good RTD at two dollars a reading logged consistently will outperform a fancy gauge that nobody checks. Once you have three months of data, plot your temperature deltas against your steam consumption. Look for patterns. When consumption drops below sixty percent of design capacity, do your deltas widen? That tells you about your distribution efficiency at part load. When does your condensate return temperature start declining? That might indicate trap failures or insufficient superheat removal. For the recovery side, start small. Pick one high-flow condensate return line and calculate the recoverable energy. Use the formula: recoverable BTU equals mass flow rate times the enthalpy difference between current state and target state. If the numbers are bigger than ten thousand dollars annually, that's your first project. Don't try to optimize the whole plant at once. You'll get overwhelmed and do nothing.
Where This Breaks Down
I should be honest about the limitations. Steam temperature coding doesn't work well in systems with frequent pressure swings. If your facility cycles boiler load every hour or so, the temperature-pressure relationship becomes noisy and harder to interpret. You need steady-state conditions for this to be meaningful. We ended up using a moving average filter in those cases, but it reduced our ability to catch rapid transients. The framework also assumes you have accurate pressure measurements. If your pressure gauges are off by even five psi, your saturation temperature calculations will be wrong by several degrees, and you'll either miss real problems or chase ghosts. I've spent weeks investigating temperature anomalies that turned out to be bad pressure transmitters. Verify your instrumentation before you invest in recovery hardware. Heat recovery itself has limits. You can't extract all the waste heat. The pinch point in any heat exchanger means you'll always have some temperature difference that can't be utilized economically. The question is whether the capital cost pays back within your hurdle rate. In my experience, most steam temperature code red situations in existing facilities have a payback under two years if you're targeting the low-hanging fruit like flash steam recovery and condensate preheat. Beyond that, the economics get murky fast.
One more thing: this approach only works if someone actually acts on the data. I've seen facilities install sophisticated monitoring systems and then file the reports in a drawer. The framework is useless without accountability. Assign ownership of each code tier to specific people. Green gets annual review. Yellow gets monthly. Orange gets weekly. Red gets immediate response. That's the part that makes or breaks everything else.