Getting NMOS Transistors Made Right
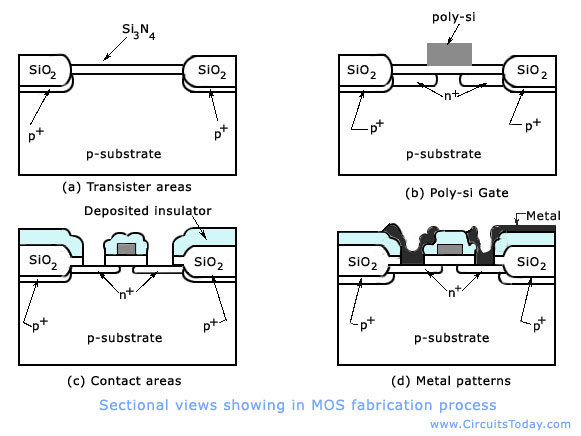
The fabrication process for NMOS transistors is far more complicated than most people think, and honestly, most introductory texts gloss over the parts that actually matter in production. I worked in a cleanroom environment for a decade before moving into process engineering, and even after all that time, every new fab node throws something at you that you never dealt with before. The basic sequence is well known — oxide growth, photolithography, implantation, annealing, metallization — but getting each step right depends on variables that textbooks rarely mention. I still remember running into a problem back in 2014 where our thin gate oxides kept developing pinhole defects after the rapid thermal anneal step. We were using a standard 8 nanometer oxide thickness and everything looked fine under optical inspection, but the leakage currents were all over the place. What we eventually figured out was that the ramp rate on the anneal was too aggressive for the specific quartz tube furnace we were using. We cut the heating ramp from 100 degrees per second down to about 30 degrees per second and the defect rate dropped by roughly 80 percent. That kind of detail doesn't show up in any datasheet. Gate oxidation is the foundational step. You start with a silicon wafer that has been through a chemical mechanical polish to get a surface roughness below 0.5 nanometers RMS. Then it goes into a dry oxidation furnace. The choice between dry and wet oxidation matters significantly. Dry oxidation produces a denser, higher quality oxide but grows much slower. For the gate oxide specifically, you always want dry oxidation. A 10 nanometer gate oxide at 900 degrees Celsius in pure oxygen will grow at roughly 25 nanometers per hour. You can calculate the rest from there.
After oxidation comes the photolithography step, and this is where most people underestimate the difficulty. You're patterning features that are approaching the diffraction limit of the light source you're using. If you're working in a older facility with g-line scanners, your minimum feature size is probably around 180 nanometers. Transitioning to i-line pushes that down to about 130 nanometers. Each resolution node requires tighter control over focus, exposure dose, and photoresist chemistry. I've seen entire lots scraped because the exposure dose varied by just 4 percent between the center and edge of the wafer due to a lamp aging issue that the monitoring system didn't flag. The photoresist coating itself is another minefield. Spin coating speed, solvent composition, and post-application soft bake all affect how well the resist adheres and how sharply it develops. A typical process runs about 30 seconds spin at 3000 RPM for a 1-micron thick layer, followed by a 90-second soft bake at 90 degrees Celsius on a hot plate. Change any of those parameters and you're chasing issues through subsequent steps that don't actually originate there. The resistance to etching changes, the linewidth control drifts, and suddenly your channel lengths are inconsistent across the wafer. Source and drain implantation follows lithography. This is where you dope the silicon regions that will become the source and drain contacts. The implant energy and dose determine the junction depth and sheet resistance. For a typical bulk CMOS process, you might run arsenic or phosphorus implants at energies between 10 and 50 keV with doses around 10^15 to 10^16 ions per square centimeter. Lower energies give you shallower junctions but require more precise alignment because the ion beam can cause channeling effects in crystalline silicon if the wafer isn't tilted at least 7 degrees off axis during implant.
I encountered a particularly annoying issue once where our implant dose calibration was drifting by about 6 percent over a three month period because the Faraday cup used for beam current measurement had accumulated carbon contamination on its surface. The process recipe called for a quarterly recalibration, but we caught the drift mid-lot through electrical testing of test structures. This is exactly why statistical process control charts matter more than anyone wants to admit. The implant system was technically within specification the whole time, but the specification window was too wide to catch that kind of systematic error. After implantation, you need a high temperature anneal to repair crystal damage from the ion bombardment and activate the dopants. Rapid thermal processing is standard here because prolonged high temperature exposure causes the dopants to diffuse too far, blurring the junction profiles you worked hard to define. An RTP cycle at around 1000 to 1050 degrees Celsius for 5 to 10 seconds achieves dopant activation while limiting diffusion to roughly 0.1 micrometers. Conventional furnace anneals at the same temperature would need 30 to 60 minutes to achieve similar activation, and the junctions would spread out 0.5 micrometers or more, which destroys the performance of short channel devices. The spacer formation step is critical for modern NMOS devices and it's often the step that limits how small you can scale the transistor. You deposit a thin layer of silicon nitride or silicon oxide on the sidewalls of the gate structure and then anisotropically etch it back. This serves multiple purposes: it defines the effective channel length by acting as a mask for the source drain extensions, and it reduces the parasitic capacitance between the source and drain. The thickness of the spacer directly affects the junction depth and the overlap capacitance, which in turn affects switching speed and power consumption. Getting the etch rate right is essential because over-etching removes material from under the gate and changes the effective channel length, while under-etching leaves residues that cause short circuits between adjacent devices.
Get the Full Details

Metallization is the final major step. You deposit a metal layer, typically aluminum or copper in modern processes, and pattern it to form the interconnects. Contact holes need to be etched through the dielectric layers to reach the doped source and drain regions, and these contacts must have low resistance. A poor contact can add several ohms of resistance per via, which is catastrophic for high frequency operation. Silicide formation at the contact interfaces, usually titanium silicide or cobalt silicide, reduces the specific contact resistance from around 10^-4 ohm-centimeters down to roughly 10^-6 ohm-centimeters. Skipping the silicide step to save process time is one of those decisions that seems smart until you measure the actual device performance and realize you've degraded the drive current by 20 to 30 percent. One thing that catches almost everyone off guard is the impact of process contamination at virtually every stage. A single particle of dust measuring 0.5 micrometers landing on the wafer during photolithography can kill every transistor underneath it. In a high-volume fab, particle counts are monitored constantly, but the real killer is usually not the count itself but the random large particles that slip through. I once traced a yield loss on a particular product to a small piece of degraded O-ring material that had flaked off a vacuum line on the lithography scanner. It took six weeks and two process engineers to find because the failure pattern was inconsistent enough that statistical analysis couldn't isolate it quickly. Testing is where you find out whether any of this actually worked. Key metrics include threshold voltage, subthreshold swing, on-current, off-current, and gate leakage. Threshold voltage should be consistent across the wafer within about 5 percent of the target value, and subthreshold swing should be below 90 millivolts per decade at room temperature for a well-fabricated device. If you're seeing subthreshold swings above 120 millivolts per decade, you typically have interface trap density that's too high, which points back to problems in the gate oxide growth or the anneal process.
Gate leakage current is becoming an increasing problem as oxide thicknesses shrink below 3 nanometers. At that point, direct tunneling through the oxide contributes significantly to static power dissipation, and no amount of process optimization can fix it. This is why the industry moved to high-k dielectrics like hafnium oxide, which provide equivalent capacitance with a physically thicker layer, reducing tunneling current. But introducing high-k materials adds new complications including Fermi level pinning at the interface, thickness uniformity challenges, and compatibility issues with the existing process flow. There is no free lunch in semiconductor fabrication. If you're looking to fabricate NMOS transistors yourself in a academic or startup setting without access to a full fab, your options are limited but not useless. Some universities offer multi-project wafer services through foundries like TSMC or GlobalFoundries where you can submit a layout and get fabricated devices back. The design rules will be generous compared to cutting edge nodes, but you can still learn a great deal about the process by working within those constraints. The minimum feature sizes available through university programs are typically in the 130 to 180 nanometer range, which is perfectly adequate for learning the fundamentals without the equipment investment. Another approach that some groups have used successfully is electron beam lithography on specially prepared wafers. You can pattern features down to around 20 nanometers this way, but the throughput is terrible, something like 10 to 20 wafers per day for a single tool, and the cost per wafer is extremely high. For research purposes this can work, but it's not scalable to anything resembling production volumes. The tradeoff between resolution and throughput is fundamental to lithography and there's no way around it.
Process simulation tools like Sentaurus TCAD or Silvaco Atlas can help you understand the physics before you commit to a fabrication run. These tools model doping profiles, electrical characteristics, and process variations based on first principles. They're not perfect, and the accuracy depends heavily on how well you calibrate the models against real data, but they're invaluable for predicting how changes in one step affect downstream results. Running a simulation takes a few hours on a decent workstation, while a full fabrication run in a university cleanroom can take two to three weeks from start to finish. Getting the simulation right saves you from learning things the hard way, though it won't save you from the things the simulation couldn't predict. The reality is that NMOS transistor fabrication sits at the intersection of physics, chemistry, materials science, and a substantial amount of trial and error. The theoretical foundation is well understood, but the practical execution requires patience, meticulous record keeping, and the willingness to spend a lot of time debugging problems that have no obvious cause. Every parameter matters, and changing one thing will ripple through multiple other processes in ways that are often not immediately apparent. That's why process engineers in fabs tend to be cautious about making changes, even small ones, without extensive characterization afterward. A new batch of silicon wafers from a different supplier once caused a 15 percent drop in yield on a mature product line, and the root cause traced back to a slightly different oxygen content in the starting silicon that affected the defect density in the oxide grown on top of it.