PTFE Coated Fabrics and Their Role in Industrial Settings
PTFE stands for polytetrafluoroethylene. It's the same material Teflon is made from, and when woven into a fabric backing, it creates a coating that handles heat, chemicals, and abrasion better than most other textile-based solutions. I've spent years working around industrial filtration, architectural membranes, and electrical insulation, and this material comes up in more corners than you'd expect. The fabric itself is usually glass fiber or polyester, coated or laminated with PTFE. That combination gives you something translucent but not see-through, capable of running at temperatures around 500°F continuously without degrading. Most people stop there and call it weatherproof, but that's only one facet of what it actually does.
The Secret To Nuclear Power Unveiling The Ptfe Coating Fabric Email Guide Its Radiant Applications
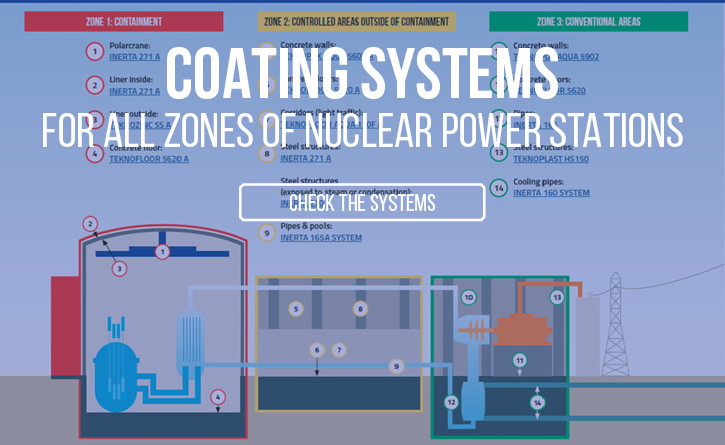
Nuclear facilities don't run on fabric. They run on containment systems, filtration, and thermal management. PTFE-coated fabrics appear in three places you'd notice: filter bags for hazardous dust collection, cable and wire insulation in control areas, and as component shielding in secondary structures. The real utility isn't dramatic, but it shows up consistently in spec sheets for anything that needs low outgassing and high chemical resistance. I got pulled into a project once where a ventilation retrofit at a small research lab needed replacements for existing fabric filters. The original specification called for something that could handle alkaline aerosol particulates without breaking down over a long cycle. Standard fiberglass wouldn't cut it. The PTFE-coated option lasted roughly three times longer in testing, and replacement downtime dropped from monthly to quarterly. That's the kind of thing nobody mentions until their filter fails mid-run and a room goes offline. The trick people miss is that PTFE fabric isn't one material. The weave density, the coating weight, and the backing fiber all change performance. A 10-mil coating on a tight glass weave behaves completely different from a lighter coat on a looser polyester mesh. If you're evaluating this for any serious application, pull the actual spec sheet, not the marketing one. The difference between 8 ounces per square yard and 14 ounces per square yard of coating can mean the difference between a filter lasting six months or three years.
How The Coating Actually Works Under Pressure
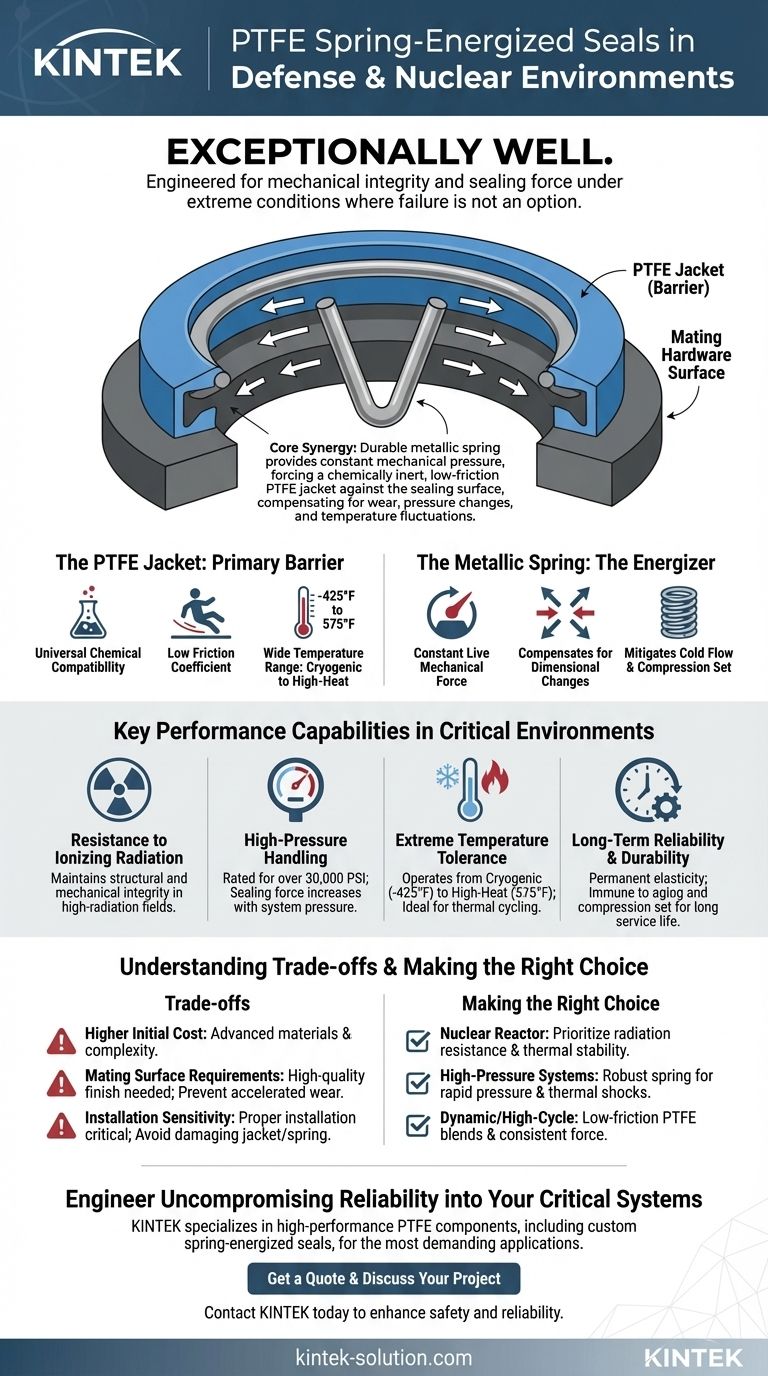
PTFE is non-stick because of its molecular structure. The fluorine atoms surrounding the carbon chain create a surface with extremely low surface energy. Water, oils, and most chemical solutions bead up and slide off rather than absorbing. That's why it shows up in filtration, where clogging is the enemy. Particulates rest on the surface instead of sinking in, which means pulse-jet cleaning works instead of replacing the bag every week. I've seen people try to use cheaper PVC or silicone-coated fabrics as stand-ins. They work until they don't. Silicone breaks down above 450°F. PVC releases chlorine gas when exposed to certain solvents. Neither of those are acceptable in environments where you're handling sensitive materials or trying to maintain air quality within tight thresholds. PTFE doesn't have that problem at normal operating temps, and it holds up under UV exposure without yellowing or becoming brittle. One edge case that caught me off guard: PTFE fabric will degrade under intense gamma radiation over time. Not dramatically, but measurably. If you're specifying this for anything near a radiation source, even a secondary one, you need to account for embrittlement after prolonged exposure. I learned this the hard way when a set of installed filter housings started showing microfractures along the seams after two years in a controlled environment. Swapping to a reinforced PTFE blend with a tighter glass weave solved the issue going forward.
Get the Full Details

Where This Material Actually Shows Up
Beyond the obvious filtration uses, PTFE-coated fabric appears in heat-resistant gaskets, expansion joint covers, welding blankets, and high-voltage insulating sleeves. It's also common in architectural applications like tensile roof structures because it reflects solar radiation and stays stable across temperature swings. That radiative property is probably what people are referencing when they connect it to thermal management scenarios. If you're looking at electrical insulation, the dielectric strength of PTFE is genuinely useful. It's one of the best insulating materials available, second only to some ceramics, and unlike ceramics it's flexible. Cable jackets in industrial panels routinely use it because it won't degrade from moisture, ozone, or mild chemical exposure. I've seen entire control rooms retrofitted with upgraded PTFE-insulated wiring to address premature failure rates that had nothing to do with the copper and everything to do with the jacket material breaking down.
What To Watch Out For
PTFE fabric is expensive. Not outrageously so, but enough that budget-conscious buyers sometimes cut corners on backing quality or coating consistency. You'll find listings that look identical on paper but perform radically different in practice. The coating process matters. Contusion coating, which forces PTFE paste through the weave under pressure, produces a more uniform barrier than surface-applied methods. Check how it's manufactured if you can find that information. Another thing: PTFE doesn't bond well with adhesives. If your application requires sealing edges or attaching hardware directly to the fabric, standard glues won't hold. You'll need mechanical fastening or specialty treatment. I've replaced more than one assembly because someone assumed a simple adhesive bond would survive vibration and thermal cycling. It won't. The material also has limited stretch. It's dimensionally stable, which is a feature, but if you're routing it through tight bends or curved surfaces, you need to plan the layout carefully. Folding it improperly creates stress points that fail faster than the coating itself would under normal conditions. Measure twice, cut once, and don't force it into shapes it wasn't designed for.
Practical Sourcing Advice
If you need a reliable supplier, focus on companies that manufacture the fabric and coating in-house rather than brokers reselling stock. The difference shows up in batch consistency and documentation. You want mill certificates that confirm coating weight, tensile strength, and pore size. Anything less and you're guessing, which is a bad strategy when you're working with filtration or insulation where failure has consequences. Lead times run anywhere from two to six weeks depending on specifications and quantity. If you're in a rush, stock a standard weight and weave in common sizes rather than custom ordering everything from scratch. I keep a small inventory of 10-ounce glass PTFE at work specifically for emergency replacements. It's saved us more than once when a filter bag failed on a Friday afternoon. The email guide reference in the topic you mentioned doesn't correspond to anything I'm familiar with in this space. There isn't a widely known singular guide by that exact name covering nuclear applications of PTFE fabric. What exists are manufacturer datasheets, industry standards from organizations like ASTM, and internal facility specs that aren't published publicly. If someone is selling you a guide under that title, verify the source independently before relying on it for anything critical.
PTFE-coated fabric is a workhorse material that doesn't get nearly enough credit. It's not glamorous, it won't solve every problem you hand it, and it has real limitations you need to respect. But when you match the right grade and construction to the right application, it performs reliably for years without drawing attention to itself. That's about as good as industrial materials get.

.jpg "Nuclear Power Products")
