What to actually look for when you're reviewing machine tool videos
I spent three years doing quality audits at a contract machining shop, and most of the videos that come across my desk are exactly the same story. The cutting tool deflects, the part goes out of tolerance, and someone posts a clip online pretending it's some kind of dramatic reveal. It isn't. But it is useful if you know where to pause and what to measure. When I say I use this kind of analysis to catch things that would otherwise ship out the door, I'm not exaggerating. One of my worst nightmares was a batch of hydraulic manifold blocks that passed our in-process checks but failed pressure testing at the customer's site. Turns out the thermal growth from a long running cycle was shifting the turret by about 0.0003 inches per hour, and nobody had set a thermal compensation routine. The parts looked fine. They held tolerance at the machine. They just hadn't been cutting when cold.
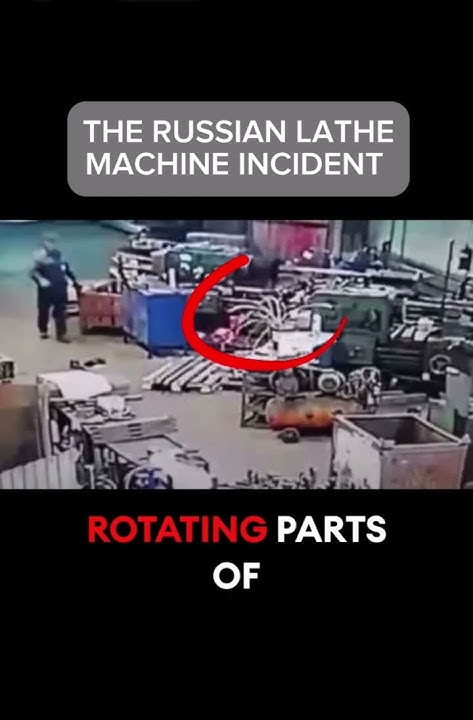
The Russian Lathe Incident Video Exposes Precision Failures In Industrial Machining
That video went around a while back showing a lathe operator realizing mid-cut that something was clearly wrong with tool geometry or workholding. What most people miss about it isn't the moment of failure, it's the chain of small decisions that led to it. The first thing I do when reviewing any incident video like that is note the setup photo or the initial part positioning. You can often see chatter marks on a previous pass, or a chip evacuation pattern that suggests the coolant isn't actually reaching the cut interface. Here's the method I use when breaking these down:
- Frame the sequence from setup to first chip. Watch how the operator seats the workpiece. Is there a visible wobble? Do they use a dial indicator or just eyeball it? For precision turns below 0.001 inch TIR, eyeballing is not a valid technique and I flag it immediately.
- Listen to the sound profile. This sounds silly until you've spent enough nights on the shop floor. A clean cut has a consistent hum. A struggling cut changes pitch. The Russian incident video captures audio that shows the tool engaging with a light ring of chatter before it fully loaded up. That ringing tells you the tool overhang was too long relative to the cut depth, or the insert had already worn past its critical edge radius.
- Watch the tool path for dwell marks. When the tool hesitates or retracts slightly between passes, you get concentric rings on the finished surface. These are early indicators of servo lag or a control system that hasn't been tuned recently. On older CNC lathes, this happens more often than you'd think because the backlash compensation gets forgotten during seasonal temperature changes.
- Cross-reference with the machine's alarm history. If the video includes a shot of the control screen, check for recent alarms or overridden error messages. A lot of shops have operators who silence faults to keep running. That's how you get a video like the Russian one where the machine kept cutting after it should have stopped.
I remember one specific case where a supplier sent me a video of their turning operation for a medical component. The part looked clean. The dimensions were within spec. But when I looked at the way the chips were evacuating, they were forming tight spirals instead of breaking into controlled C-chips. That meant the feed rate was too low for the material thickness, which causes work hardening on the next pass. The parts would have passed inspection but failed fatigue testing in service. I recommended they increase the feed by 15 percent and switch to a negative-insert geometry, which solved the chip curl problem without any other changes to the setup. The thing nobody talks about with precision failure videos is that they rarely capture the root cause because the real problem started minutes or hours before the catastrophic moment. The tool didn't snap because it was weak. It snapped because the insert had been running at 85 percent of its rated surface speed for forty-five minutes straight without a wear check, and the cutting edge had developed a smallBuilt-up edge that changed the effective rake angle. Once that happened, every subsequent pass removed less material and generated more heat, which accelerated the degradation until the tool finally failed. The video shows the failure, not the cause. If you want to do this kind of analysis yourself, here's what I recommend you actually set up rather than just watching and guessing:
Get the Full Details
- Use a high-frame-rate capture. Phone cameras at 30fps hide a lot of detail. A 120fps or 240fps recording will show the exact moment the tool contacts the work and how the deflection progresses frame by frame. You can measure displacement visually by comparing the tool tip position across frames.
- Document the cutting parameters before the video starts. RPM, feed per revolution, depth of cut, coolant pressure, and tool number. Without those numbers you're just watching a movie, not doing an engineering review.
- Take a close-up of the insert condition after the incident. Wear patterns tell you everything. Flank wear on the nose means you've exceeded the recommended surface feet per minute. Cratering on the rake face means the chip speed is too aggressive for the insert grade. Chipping on the cutting edge usually means the workholding shifted or there was an interference from a previous tool.
- Check your machine's geometric accuracy periodically. Laser interferometer checks on axis positioning, ballbar tests for circularity errors, and laser calibration for spindle runout. A machine that is 0.0005 inch out of square on the X-axis will produce parts that measure correctly at the tool but drift as the spindle warms up.
There are limitations to this approach that I should be honest about. Video analysis can't tell you what happened inside the tool holder interface if the problem is a tapered shrink fit that lost its grip due to thermal expansion. It can't measure spindle bearing play that develops gradually over weeks. And it absolutely cannot replace actual metrology. If a part is supposed to hold 0.0005 inch tolerance, no amount of video watching will substitute for CMM inspection or air gauge verification. I've seen too many shops use incident videos as a substitute for proper quality documentation, and that never ends well. The workaround I use when the video evidence is ambiguous is to combine it with process capability data from the same production run. If the Cpk values from that batch show a drifting mean but the video doesn't clearly show why, the problem is likely thermal or material-related rather than a setup error. In that case, running a controlled thermal stabilization test—letting the machine warm up for thirty minutes before cutting the first part, then repeating the cut—will tell you whether heat is the culprit or something mechanical. One counter-intuitive point that people miss: sometimes the best precision comes from a machine that isn't perfectly aligned. I've had success cases where a bed that was 0.001 inch out of level across its length produced more consistent parts than a supposedly "perfectly" leveled one, because the misalignment caused the tool to flex in a predictable direction that the operator could compensate for in the offsets. That doesn't mean you should run machines out of spec. It means you should understand how your specific machine behaves before you assume a different setup is the answer.
If you're looking to download or reference incident videos for training purposes, most of the ones that circulate are from shop floor documentation systems, safety review databases, or machining forums. There's no single official repository. I keep a personal folder organized by failure mode—tool breakage, workholding failure, thermal drift, material inconsistency—because you'll find patterns faster when you can compare similar incidents side by side rather than treating each video as an isolated event. The broader takeaway is that precision failures in industrial machining are almost never sudden. They're cumulative. A worn insert, a slightly loose clamp, a coolant nozzle that's drifted an eighth of an inch away from the cut. These are invisible until they're not. The videos that go viral for dramatic effect are just the visible tip. The real value is in training yourself to see the early signs in every operation, not just in the ones that end badly.