How The Ford Motor Company Built The First Real Mass Market Automotive Operation
The Rise Of The Mass Market The Ford Motor Companys Journey From 1908 To 1927
The Ford Motor Company fundamentally changed how machines get built between 1908 and 1927. That nineteen-year window is where you see the entire arc from a working assembly process to a fully realized mass production system, and then the beginning of its decay as the market shifted. Most people only know the Model T. They do not know why it worked, how it actually worked on the factory floor, or what broke when it stopped working. I spent years studying old manufacturing case studies and talking to engineers who had inherited lines that were direct descendants of Ford's original system. The practical reality is a lot more complicated than the textbook version. The moving assembly line did not appear fully formed. It was a series of failures, redesigns, and desperate pivots that happened under enormous financial pressure. Ford was nearly bankrupt in 1915. The system that saved them was ugly and exhausting to operate.
The Foundation: Why The Model T Actually Sold
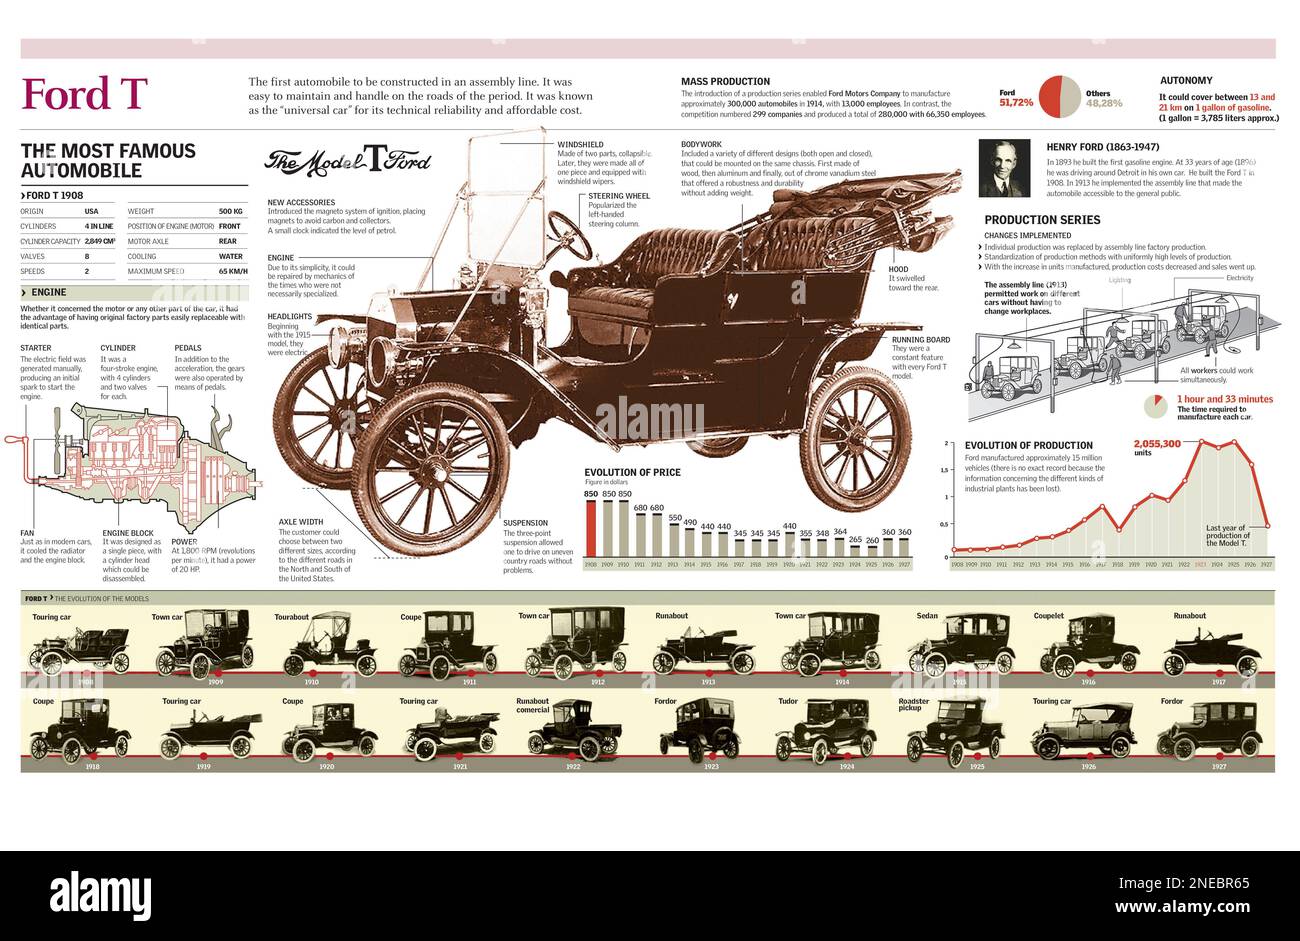
The Model T launched in 1908 at $850. By 1924 the price had dropped to about $290. That is not just good business. That is industrial redesign happening at a pace the rest of the world could barely track. The core insight was that cost reduction could come from standardization, not just from cheap labor or cheap materials. Every part had to be interchangeable to any tolerance that mattered. A Model T engine block from 1912 fit a 1918 frame without any hand fitting. The high-ground-clearance design was not a marketing choice. It was a response to the fact that most American roads were unpaved and often impassable after rain. In 1911, a customer in rural Indiana filed a complaint that his Model T could not clear a mud-covered stone bridge. Ford's engineering team responded by raising the clearance from eight inches to nine and a half inches across the entire line. That single change required retooling the axle housings and the suspension geometry. It also added about seven pounds per vehicle. Most competitors ignored this entirely because their markets had better roads. The real breakthrough happened in 1913 at the Highland Park plant. Moving the chassis along an overhead trolley system cut assembly time from twelve hours down to about ninety-three minutes. This was not a theoretical improvement. The plant managers at the time were dealing with workers who simply refused to keep up with the pace. One shift supervisor reported that after three weeks, nearly forty percent of the line workers had quit on the spot. The turnover rate was catastrophic for any operation that relied on skilled fitters. Ford solved this by raising the daily wage to five dollars in January 1918. That was more than double the going rate. It stabilized the workforce immediately and let the line run at full speed without constant retraining.
The Vertical Integration Problem
Ford did not just build cars. He built the infrastructure around building cars. By 1920, the company controlled steel mills, glass factories, rubber plantations in Brazil, and a railroad that ran between his plants. The idea was to eliminate every middleman between raw material and finished vehicle. In practice, this created enormous rigidity. When Ford needed a different grade of steel for a new stamping, he could not just order it from a supplier. He had to reroute production through his own facilities, which were already running at maximum capacity for other products. I have seen this exact problem repeat in modern manufacturing. A company I consulted for in 2019 had the same vertical integration mindset applied to cloud infrastructure. They owned their own data centers instead of using managed services. The result was that when demand spiked, they could not scale quickly because provisioning new hardware took six to eight weeks. Ford's problem in the 1920s was identical, just at a larger scale. The Rouge Plant, completed in 1928, was the physical manifestation of this thinking. It received raw materials at one end and shipped finished cars out the other. Nothing entered or left the site without passing through Ford's control. It was impressive. It was also incredibly expensive to maintain and inflexible when consumer preferences began shifting away from the Model T.
Get the Full Details

What Happened When The Market Changed
By 1925, General Motors had introduced color options, different body styles, and annual model year updates. Ford refused to do any of this. The company believed that offering choices would complicate the production line and raise costs. Henry Ford publicly stated that customers could have any color they wanted as long as it was black. This was not a marketing catchphrase. It was a genuine operational constraint. Black enamel dried the fastest, which meant higher throughput on the painting line. Every other color required longer drying times and slower conveyor movement. The sales numbers tell the story clearly. In 1921, Ford held roughly sixty percent of the American car market. By 1927, that had dropped to under twenty percent. The company was still selling well, just not dominating like it used to. Production of the Model T ended on May 26, 1927. By that point, Ford had built over fifteen million of them. That number is still impressive by any standard, but the reason it matters is the pace at which it was achieved. No other manufacturer came close to those volumes until the late 1930s. The shutdown of the Model T line required laying off tens of thousands of workers and idling massive capital equipment. Ford spent fourteen months retooling the Rouge Plant for the Model A, which launched in late 1927. During that gap, Chevrolet captured the market segment that had been drifting away. Many of those buyers never returned to Ford. They stayed with GM because the newer cars felt more modern and were available in multiple colors and body types.
The Practical Takeaway
If you are studying this period for operational reasons rather than historical interest, the key insight is that mass production is a system, not a trick. You cannot adopt the assembly line without also adopting the supply chain discipline, the quality control standards, and the labor management strategies that make it work. Ford learned this the hard way. The early years were filled with failed experiments, including a brief attempt at assembling engines on a horizontal conveyor that jammed constantly and caused significant downtime. The overhead trolley solution was not obvious. It emerged after watching how slaughterhouses moved carcasses in Chicago. The danger here is assuming that copying one element of Ford's system will reproduce the results. It will not. The wage policy, the vertical integration, the standardization philosophy, and the relentless cost reduction all had to work together. Remove any one of them and the system breaks. A modern operation that adopts moving assembly without the supplier relationships and quality systems will find itself with fast-moving lines producing defective products at high volume. That is worse than slow-moving lines producing decent products because the waste is multiplied. The Model T era ended because the market stopped being a single monolith. Once consumers started wanting choice, Ford's system became a liability instead of an advantage. The company that adapted fastest to that reality was the one that won the next decade. Ford survived, but it never regained the same level of market dominance. That is the practical lesson from 1908 to 1927. Mass production works brilliantly until it does not. The companies that last are the ones that recognize the shift before the numbers force them to react.