Industrial Abrasive Media: A Practical Overview
I spent last month dealing with a batch of Rom White that was clogging faster than expected on some stainless welds. The shop floor was not happy. I have been running abrasive media since the late nineties, when white alumina was about the only thing most shops stocked beyond the cheap brown aluminum oxide stuff you find in any hardware store. It took me a while to learn that Rom White and similar white fused alumina products are not universal solutions, even though suppliers will tell you otherwise. Rom White is essentially a white fused alumina abrasive produced in specialized furnaces where iron content is kept extremely low. The resulting grain is lighter in color because it lacks the iron oxide staining you see in cheaper abrasives. More importantly, the purity gives you a different fracture pattern under load. Standard aluminum oxide tends to blunt and then shed. White fused alumina fractures in a way that continuously exposes fresh cutting edges, which is why it stays aggressive longer on hard materials like stainless steel, titanium, and high-chromium alloys. The rise of products like Rom White in mainstream industrial use has largely been driven by surface preparation specifications tightening up. Aesthetic finish standards in food processing equipment, pharmaceutical-grade metal work, and architectural metal cladding require that you do not introduce iron contamination into the substrate. That is the primary reason people pay the premium over standard abrasives. If you are grinding carbon steel and do not care about surface cleanliness, white fused alumina is usually overkill. You will spend more money and get marginally better results.
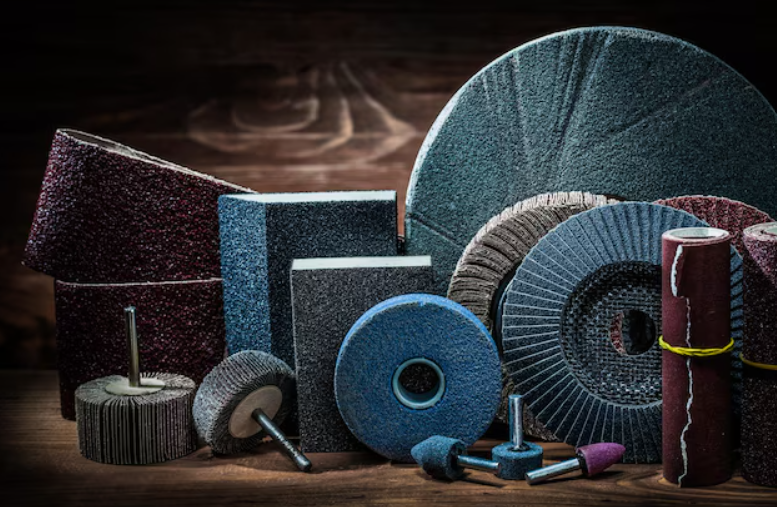
I run Rom White in both bonded wheels and coated abrasives. For flap discs on a standard angle grinder, I typically use an 80-grit zirconia-alumina blend for stock removal and then switch to a 120-grit white fused alumina flap disc for the final pass on stainless. The zirconia handles the heavy work without loading up, and then the white alumina brings the surface to a consistent finish that is ready for passivation. Trying to do everything in one grit with white fused alumina tends to waste material and time. It is too aggressive in a different way and breaks down unevenly when you push it hard. One thing people get wrong is how much pressure to apply. White fused alumina does not benefit from heavy downward force. You want light contact, maybe four to five pounds of pressure on a flap disc, and let the abrasive do the cutting. Push harder and you just glaze over the surface and warm up the material faster. On stainless that can mean introducing heat tint within seconds. I have seen operators slow their pace by half and actually double their wheel life by just reducing pressure and using a traversing motion instead of a stationary grind. If you are considering switching your shop over to white fused alumina media, start with a controlled test. Take a batch of your most common material and run a side-by-side with what you are currently using. Document surface finish, material removal rates, and media consumption over a full shift. The numbers will tell you whether the upgrade is worth it for your specific applications. Supplier samples are usually free. Requesting a few bags and doing actual shop floor testing costs almost nothing compared to committing a full order based on a data sheet.
The other reality is storage. White fused alumina absorbs moisture more readily than some other abrasives if you leave bags open. I keep mine in a sealed container or at least folded and taped closed after each use. Moisture degrades the bond on coated abrasives and reduces cutting performance on bonded wheels. This is a small thing that nobody mentions in marketing material but shows up immediately when your media has been sitting out in a humid shop overnight.
Get the Full Details