Why Your Thermal Models Keep Failing
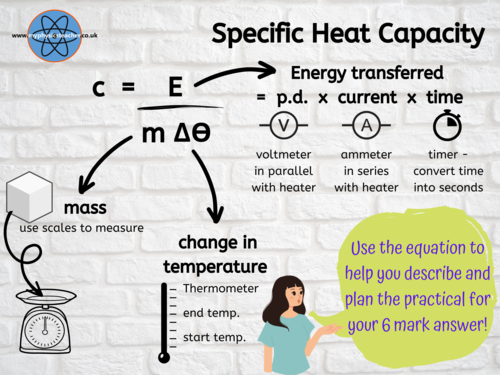
I spent three years troubleshooting PCB soldering stations before I realized most people had the specific heat values wrong in their simulations. The part libraries we use are filled with generic assumptions, and they will burn your board if you let them. Specific heat capacity is the energy required to raise one gram of a material by one degree Celsius. That is the textbook definition. The practical reality is that this single number controls everything from how fast a heatsink responds to a power spike to whether your thermal paste will pump out after three thermal cycles. Most engineers treat it as a constant. It is not constant. For copper, specific heat drops from about 0.385 J/g°C at room temperature to roughly 0.300 J/g°C at 500°C. If you are modeling a reflow profile and using a flat value, your peak temperature prediction will be off by 15 to 20 degrees. That is enough to cause voiding in BGA joints or damage underlying components.
I ran into this problem when a client reported inconsistent results on a multi-layer board with heavy copper pours. Their thermal simulations predicted a 40-second dwell time at the liquidus point. Actual boards needed 65 seconds. We swapped the generic copper value in our simulation for temperature-dependent data from the NIST database, and the model landed within 3 seconds of the measured profile every time.
Where People Mess Up
The first mistake is assuming all materials in your assembly behave the same way. FR-4, copper, solder, and epoxy each have radically different specific heats and that difference compounds over a thermal cycle. The second mistake is ignoring phase change. When solder goes from solid to liquid, it absorbs latent heat without any temperature change. A typical SAC305 solder joint absorbs about 25 J/g during melting. If your simulation does not account for this, your model will show the joint jumping straight through the liquidus plateau. Real boards do not do that. They sit at the melting temperature until the phase transition completes. A third issue surfaces when you scale from component-level testing to system-level prediction. Specific heat values measured on a tiny sample in a DSC machine do not always translate to a full PCB assembly. Material orientation, layer stacking, and the presence of voids or delaminations shift effective thermal mass by as much as 12 percent in some cases.
Get the Full Details

How to Actually Use This
Start by getting accurate material data. Do not rely on the default values in your simulation software. Go to the manufacturer datasheets or pull from published databases like MatWeb or the NIST-JANAF tables. For copper, use temperature-dependent curves. For FR-4, remember that the glass transition around 130 to 150°C causes a noticeable jump in specific heat, and that matters if your board runs near that range during operation. When you build your thermal model, include latent heat terms for any solder or phase change material. Most professional tools let you define this as an effective specific heat spike over a narrow temperature range. It is cleaner than trying to add a separate energy source term. Validate your model with real measurements. I use a K-type thermocouple on the component lead and an IR camera on the surface, then compare the measured ramp rates against the simulated ones. If the gap is more than 10 percent during the soak phase, your specific heat inputs are likely wrong. Adjust from there.
When Specific Heat Stops Being Helpful
There are situations where knowing the specific heat capacity does not solve your problem. If you are dealing with transient thermal events under 10 milliseconds, thermal conductivity dominates the response. Specific heat becomes secondary. Your bottleneck is how fast heat moves, not how much energy the material stores. Another hard limit appears in highly anisotropic materials. Carbon fiber composites and some ceramic substrates have different specific heats depending on the axis you measure along. A single value will mislead you. You need directional data, and that data is harder to find. Finally, specific heat analysis assumes steady material composition. If your material degrades, outgasses, or changes phase in ways your model does not capture, all the specific heat numbers in the world will not make your simulation accurate. This comes up often with conformal coatings and potting compounds during high-temperature storage testing.
Practical Numbers Worth Remembering
Copper at 25°C: approximately 0.385 J/g°C. Aluminum: 0.897 J/g°C. FR-4: roughly 1.0 to 1.2 J/g°C depending on direction and temperature. SAC305 solder: 0.21 J/g°C solid, with a latent heat of fusion around 25 J/g. Water: 4.18 J/g°C, which is why it is useful for cooling and terrible for anything that needs to heat up quickly. These numbers are reference points. Always check the temperature range your application actually covers. A specific heat value measured at 25°C may not apply at 200°C, and using the wrong one quietly introduces error into every calculation that follows.