Calcium oxide is one of the most underrated industrial chemicals. People call it quicklime when they mean it's dead simple, then act like it's some breakthrough.
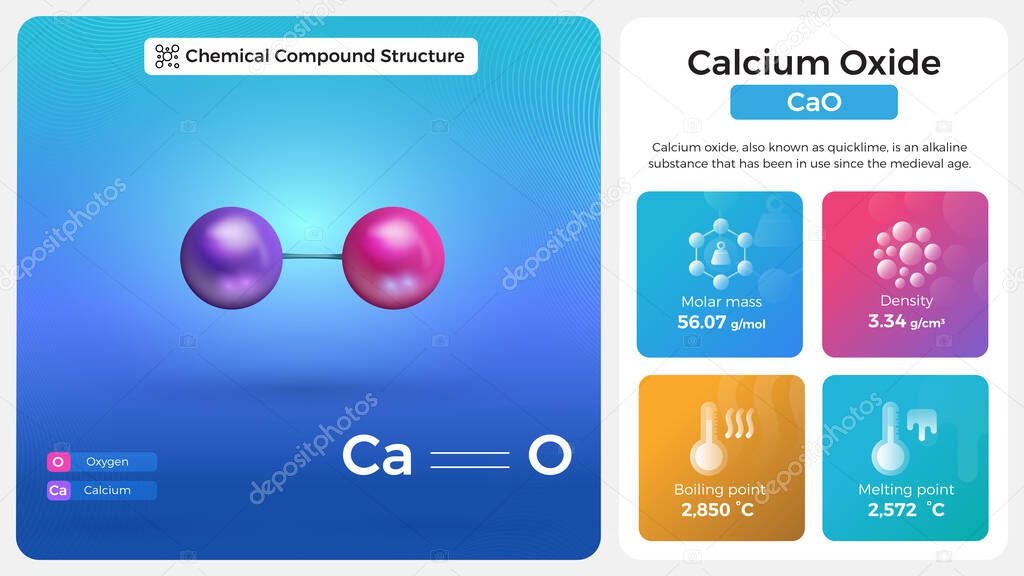
It's been around for millennia. The Romans used it. We just figured out new ways to weaponize it since. The compound itself is CaO, made by heating limestone (CaCO3) to roughly 900°C. That's the whole reaction. It's exothermic as hell when it rehydrates, which is why you don't want it in your eyes or lungs. Here's where the practical side gets interesting. Most people know calcium oxide from construction. Flue gas desulfurization is the thing that actually matters. You spray a slurry of CaO and water through exhaust stacks from power plants and waste incinerators. The SO2 reacts with it to form calcium sulfite, then sulfate. It's cheap, it's effective, and it's been the backbone of regulatory compliance in the US and EU for twenty years. Without it, we'd be looking at sulfur limits that nobody could afford to meet. I worked on a scrubber retrofit back in 2014 where the original spec called for high-purity lime. The plant was running off biomass and the sulfur content in the flue gas was nowhere near what the design assumed. We switched to a hybrid approach using a mix of CaO and NaOH in the slurry. The CaO handled the bulk SO2 absorption while the sodium hydroxide kept the pH up enough to drive the reaction forward. Cut our lime consumption by about forty percent and stopped dealing with the plugging issues we were having in the recycle lines. The original engineer on that project thought I was crazy. He also left when the next maintenance cycle came around.
Steel production is another area where this stuff does heavy lifting. The basic oxygen furnace process uses lime as a flux to form slag. The slag captures phosphorus and sulfur from the molten iron. Without adequate basicity in the slag, you're just making dirty steel. The trick isn't just adding lime, it's getting the CaO/SiO2 ratio right. Too much silica in the charge and you need more lime to compensate, which drives up slag volume and energy costs. Most mill operators learn this the hard way after a heat goes to spec and wastes three tons of refractory lining in the process. Water treatment is where most hobbyists and small operators encounter calcium oxide. You add it to raise pH and precipitate heavy metals. The common mistake is adding it dry to concentrated water without pre-slaking. You get hot spots, incomplete dissolution, and your pH readings go all over the place. Slurry it first at about a 10-15% solids concentration, let it hydrate completely, then feed it into the main stream. Takes maybe ten extra minutes but saves you from chasing pH for an hour. There's a growing application in carbonation curing for concrete. Instead of traditional steam curing, you expose fresh concrete to CO2 under pressure. The CO2 reacts with CaO to reform CaCO3. This actually sequesters a meaningful amount of carbon per cubic meter and speeds up early strength gain significantly. Several companies are commercializing this now, mostly in Europe. It's not a silver bullet, but it does reduce the clinker content needed, which is the real emissions problem in cement anyway.
The downside nobody talks about is storage. Quicklime is hygroscopic. If your silo or bag house has any moisture ingress, you're waking up to a brick of calcium hydroxide that won't flow. I've seen entire batches ruined because a vent filter got wet during a rain event. Desiccant breathers on storage silos aren't optional. They're mandatory if you want consistent feed rates. Particle size distribution matters more than most people realize. Fine lime (sub-75 micron) hydrates faster but creates dust hazards and can blow through filtration systems. Coarse lime (retained on a 45-micron sieve) hydrates slower and may not fully react before it exits the process. The sweet spot for most wet scrubbing applications is around 80-90% passing through a 75-micron screen. Anything outside that range and you're either paying for material that doesn't react or breathing dust that will eat your lungs. Check the mill specs on every delivery. Don't trust the certificate of analysis without verifying particle size distribution yourself. Another counter-intuitive point: higher purity isn't always better. For desulfurization, trace impurities like magnesia and alumina can actually improve slurry rheology and reduce scaling in heat exchangers. Industrial grade lime (around 85-90% CaO) often outperforms food or pharma grade in scrubber service because it contains just enough impurities to keep things moving. The ultra-pure stuff tends to form harder scale deposits and requires more frequent cleaning cycles.
Get the Full Details
Soil stabilization is another application worth noting. Agricultural lime and road stabilization both use calcium oxide, but they're fundamentally different processes. Agricultural applications rely on slow neutralization. Road base applications rely on the pozzolanic reaction where CaO reacts with silica and alumina in the soil to form cementitious compounds over time. The road stuff needs to be properly compacted within hours of mixing. If it dries out before compaction, you've wasted the material. I've seen crews pour lime on a road bed, get delayed by traffic, and come back the next morning to a slab that was harder than concrete because the hydration reaction had already started setting up. The cost structure is straightforward. Limestone is cheap and everywhere. Calcination is the energy cost driver. A ton of CaO requires roughly 3.1 tons of CO2-equivalent emissions just from the calcination reaction alone, not counting the fuel burned. That's why carbonation curing and direct air capture integration with lime are getting attention. The chemistry is on your side if you can capture that CO2 rather than vent it. Handling safety is non-negotiable. Calcium oxide reacts with moisture in your respiratory tract. Even brief exposure to dust causes irritation that can escalate to chemical burns in the mucous membranes. Respirator isn't optional for dry handling. Closed transfer systems and wet conversion before any human contact is the standard. I once watched a new contractor ignore the splash zone warnings on a slurry preparation unit and get second-degree burns on his forearm from a line rupture. That lime was already partially hydrated, which means it was hot. Fresh calcined material hitting skin moisture is worse.
If you're evaluating calcium oxide for a new application, start with the impurity profile of your source material. Different limestone deposits have wildly different trace element content. A deposit in the Midwest US will behave differently than one in the UK or Australia, not just because of purity but because of the mineralogy. Run a small-scale test with your actual feedstock before committing to a full design. The lab results and the pilot plant results will diverge. They always do.