Getting the Most Out of Your Bambu Lab A1 Mini Print Bed
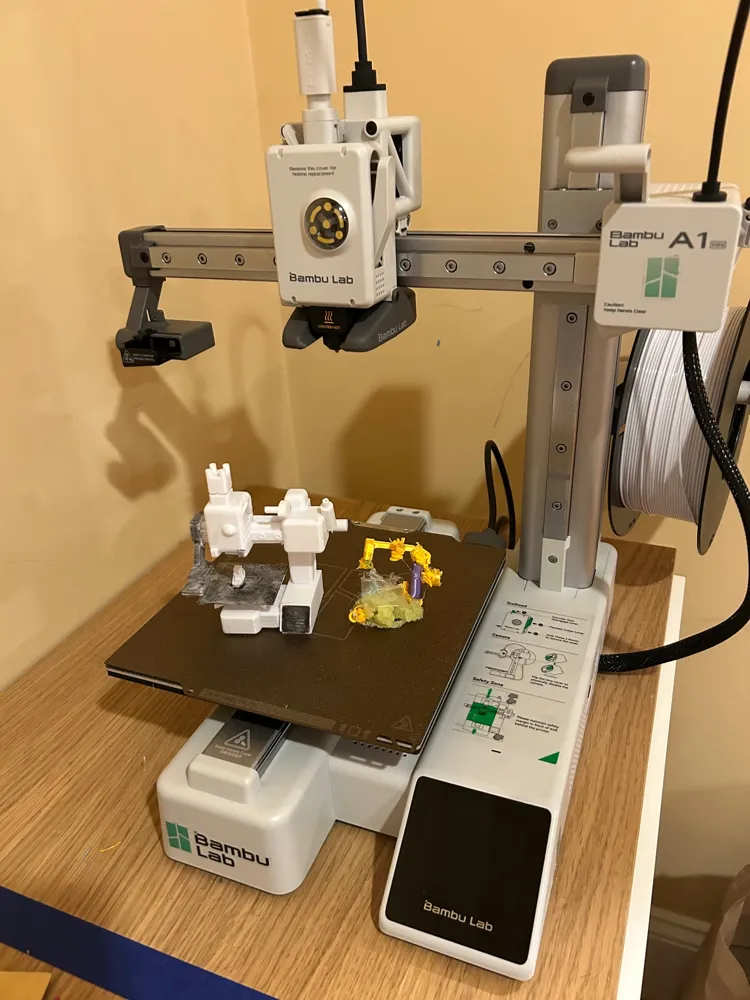
The A1 Mini comes with a 180 x 180 x 180mm build volume. That's the usable area you're working with, not including any overhangs or supports that might drift past those edges. The stock build surface is a textured spring steel PEI sheet, and it ships pre-mounted on a magnetic replacement plate. I've run probably two hundred prints on mine over the last eight months, and there are a few things nobody really tells you about this setup until you've burned through a couple of failed prints. Let me be precise about what those dimensions actually mean in practice. The 180 x 180mm is the flat X-Y work area. Your first layer needs to land somewhere within that rectangle, and your entire model has to fit inside it when sliced. If you're running a 175mm tall cylinder, you're already at the limit on Z and you need to double-check that Bambu Studio isn't silently shifting your model upward during slicing. It happens. I've caught it twice now. The bed itself is heated, reaches about 100C, and uses automatic first-layer calibration through the touchscreen menu. You don't adjust the Z-offset manually the way you would on an older Ender-style machine. The probe does it for you by measuring the gap between the nozzle and the bed at multiple points and calculating the offset. This is good, but it has a known blind spot: the four corners. The probe samples near the edges but doesn't always account for the slight spring steel flex that happens under the nozzle's weight at the absolute perimeter. If you're printing something that spans the full 180mm width and the corners are lifting, that's why. I solved it by running a full bed calibration with a thin squish setting and then manually adding 0.02mm to the Z-offset for that specific print. Small tweak, fixed the corner adhesion problem entirely.
Here's the thing about the textured PEI surface that I wish someone had mentioned upfront: it's excellent for most filaments but brutal on certain materials. PLA releases fine, PETG sticks a bit too well and can tear if you try to flex the sheet aggressively, and ASA will bond so strongly that you'll likely damage the texture trying to pop it off. For ASA, I lay down a thin coat of standard blue painter's tape, smooth it out, and print on that. The tape gives you a consistent surface and the print comes off cleanly afterward. That adds maybe 3-4 minutes of prep time and saves you from replacing the PEI sheet every few months. Bed preparation matters more than most people realize. The factory sheet arrives with a protective film and whatever handling oils got on it during assembly. I wipe mine down with isopropyl alcohol before the first print and after every few large prints. Not a huge deal for small PLA figures, but if you're printing functional parts that need reliable first layers, a clean bed makes the difference between a successful adhesion test and a print that walks across the surface like a crab. I've lost two complete PETG prints to a bed that looked clean but had a thin film of finger oil on it. You won't see it. The first layer just won't stick properly in patches. When it comes to slicing settings, the default Bambu Lab profiles work reasonably well out of the box. For PLA, I run the standard profile at 60C bed temperature. For PETG, bump it to 80C and add a brim of at least 5mm around the entire model. The A1 Mini's bed is small enough that PETG warping is a real risk without that extra margin. I used to skip the brim on medium-sized PETG prints and end up spending an hour rescuing a curled edge with a spatula. Not worth it.
One more practical detail: the magnetic plate system is genuinely well designed. Plates snap on and off quickly, and you can buy replacements separately when one gets scratched up or degraded. I have a spare blank plate and a sheet of glue stick. For ABS and ASA on this printer, a thin layer of standard white school glue stick applied to the bare PEI gives better adhesion than tape and is easier to clean off than many alternatives. The glue dissolves with a little warm water when the print is done. Takes about 30 seconds to apply and 30 seconds to clean. Worth the minor time investment if you're working with engineering materials regularly. The A1 Mini doesn't have a closed enclosure, which directly affects what materials you can use successfully on this bed size. PLA and PETG are fine. ABS is risky because drafts and temperature fluctuations will warp even small prints. Nylon is basically out of the question unless you've built some kind of DIY chamber around it. The bed heating helps, but 180mm of heated surface can't fight a cold room on its own. I keep my printer in a climate-controlled office, and even then I stick to PLA and PETG unless I'm using the glue stick method for ASA in a pinch. If you need more build volume than 180 x 180 x 180mm, the A1 Mini simply won't accommodate it. There's no upgrade path for the frame. The A1 standard model offers the same height but a wider X-Y area depending on the exact revision, and the X1 series moves into enclosed territory with significantly larger beds. But if your use case fits the Mini's footprint, this is a competent setup that just needs the right surface prep and realistic expectations about what materials it can handle.
Get the Full Details