Identifying What Actually Stops You
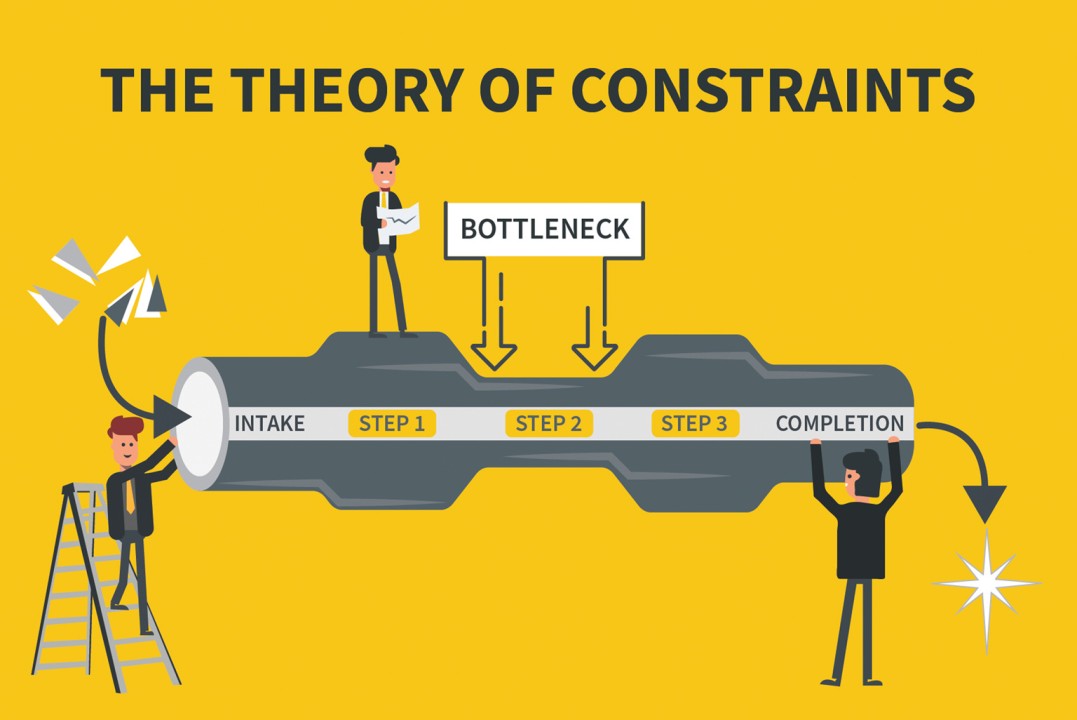
Most growth problems aren't what they look like on the surface. I spent three years running a small manufacturing operation where we couldn't figure out why increasing sales volume never translated to more revenue. We threw marketing spend at it. Hired more reps. Nothing moved the needle for months. The actual problem had nothing to do with demand or selling. It was our assembly line could only process seventeen units per day because one particular station required a manual calibration step that took twenty-two minutes and only our lead technician could perform it correctly. That single bottleneck controlled everything. Until we fixed that one station, every other improvement was wasted money. Limiting factors are straightforward in theory. A system can only grow as fast as its slowest constraint allows. The problem is identifying which constraint is actually limiting you, because it shifts over time and it's rarely the obvious one. In my experience, most teams fix the wrong thing because the visible problem feels urgent while the actual constraint sits quietly somewhere downstream. You might have a sales team begging for product, but if production can't keep up, those conversations are just theater. Or you might have production capacity while orders dry up. The constraint has moved, and you're still solving yesterday's problem. The practical approach is to map your full value chain and then go measure each stage under real operating conditions, not theoretical maximums. I found that the quickest way to identify the bottleneck is to look at where inventory piles up right before a station. Whatever queue is growing the fastest is your current constraint. Work there first. Everything else is optimization theater until that queue shrinks. The method itself is simple to explain but brutal to execute because the bottleneck often isn't a process problem. It's usually a person, a policy, or a piece of equipment that leadership doesn't want to replace. In my case it was the calibration station requiring a specialist who took two weeks of vacation per year and sick days on top of that. The workaround was documenting the calibration procedure into a checklist and cross-training two other technicians. Took about six weeks of deliberate practice. Cut downtime by eighty percent and let us run the line at twenty-eight units per day instead of seventeen.
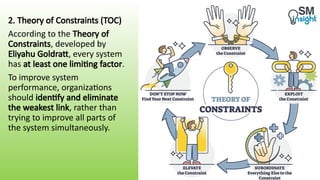
Here's the counter-intuitive part most people miss. Strengthening a non-bottleneck step actually makes things worse. If you speed up a stage that isn't the constraint, you just push more work into the bottleneck faster. Inventory builds up there even more. Cycle times get longer. Confusion increases. You've invented a new kind of waste. I learned this the hard way when we upgraded our packaging line thinking it would help throughput. It didn't. Packaging had never been the problem. We just accelerated starvation at the calibration station because parts arrived faster than they could be processed. Took another two months to realize what happened and revert the change. The lesson is that you need to measure the effect of every improvement on the actual constraint before calling it progress. Another nuance that matters is that constraints have different types and they require different interventions. There are physical constraints like machine capacity or floor space. Then there are policy constraints like quality standards that are stricter than necessary, approval workflows that add waiting time, or pricing models that discourage the most profitable customers. Policy constraints are harder to spot because they feel normal. Everyone follows them. I once spent four weeks arguing with a vendor about delivery schedules before realizing the constraint wasn't their timeliness. It was our own policy requiring three separate purchase orders for the same recurring material. Consolidating that into one weekly order eliminated half the administrative delay without changing a single piece of equipment. The fix was bureaucratic, not technical. Most teams don't know how to solve that kind of problem because they're trained to think in hardware and headcount. The approach that actually works is something called Theory of Constraints, developed by Eliyahu Goldratt. It's a five-step process that boils down to: identify the constraint, exploit it fully without new investment, subordinate everything else to the constraint, elevate the constraint if you still can't meet demand, and then repeat because the constraint will move. The repetition is where people fail. They solve one bottleneck and declare victory. The constraint just shifted to another part of the system. In manufacturing it often moves to supply chain or quality. In software it moves to deployment pipelines or documentation. In services it moves to scheduling or response time. You have to keep going until you hit a constraint that genuinely can't be moved without major capital or strategic change.
I should be honest about where this framework breaks down. It assumes you have a relatively stable system with a identifiable flow. If your business is inherently unpredictable, like a creative agency taking on one-off projects with different requirements each time, the concept of a single constraint becomes almost meaningless. You'll have different bottlenecks for different projects simultaneously. The framework also doesn't handle multi-product environments well. When you're running ten different product lines through shared resources, the bottleneck isn't one station. It's a mix, and simple queue observation doesn't tell you which product to prioritize. In those cases you need mathematical optimization or at least decent simulation modeling before you make decisions. I've seen teams try to apply Theory of Constraints to complex product portfolios and end up optimizing for the wrong product mix because they were focusing on throughput without accounting for contribution margin per constrained unit. That mistake cost us about fourteen thousand dollars in a single quarter before someone caught it. There's also the question of whether constraints are external. If your bottleneck is market demand rather than internal capacity, the whole framework flips. You shouldn't be trying to increase production speed. You should be investing in sales, distribution, or product-market fit. I've watched companies pour money into operational efficiency when their real problem was nobody wanted what they were building. That happened to us in 2019. We spent six months streamlining our fulfillment process, reducing order cycle time from forty-eight hours to thirty-one. Two months later we realized demand had dropped twelve percent because a competitor launched a similar product at a lower price point. All that operational work was irrelevant. The constraint was outside the system entirely. Recognizing when a constraint is external takes honesty most organizations don't have because fixing internal problems feels like progress while admitting external failure feels like defeat. If you're working with a constrained system, start by measuring current state for at least two full production or service cycles before you change anything. My rule is minimum four weeks of data in a stable environment. Take daily measurements at every stage. Track queue sizes, cycle times, and idle time. Write it down. Don't rely on memory or rough estimates. Then find where the biggest queue is forming and focus all your energy there. Don't touch anything else until that queue drops below your normal operating level. When it does, the constraint has moved. Find the new one. Repeat. This process usually takes between eight and sixteen weeks to complete a full cycle depending on system complexity. Simple systems might close in three weeks. Complex multi-stage operations can take six months. The timeframe doesn't matter as much as the discipline of only working on the actual constraint at any given moment.
Get the Full Details

The real reason this matters for strategy and survival is that organizations that ignore limiting factors tend to overinvest in the wrong places. They buy equipment for stations that already have excess capacity. They hire people for roles that aren't blocking anything. They implement software that automates processes that don't need automation. Meanwhile the actual constraint sits there getting worse because nobody has the bandwidth to address it. The financial impact compounds quickly. In my experience, the gap between a company that understands its constraints and one that doesn't usually shows up as a twenty to forty percent difference in effective capacity over a two-year period, assuming similar resources and market conditions. That gap is the difference between sustainable growth and chronic stress. It's also why limiting factor analysis isn't optional. It's the difference between working on the right problem and working efficiently on the wrong one.