Understanding the Ford Louisville Assembly Plant and What Actually Matters
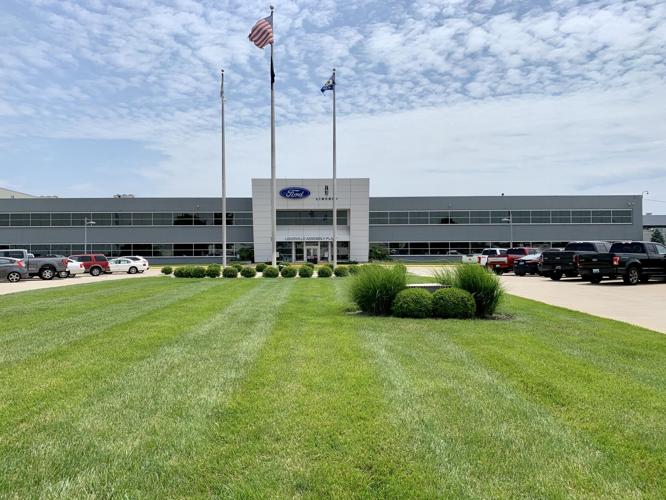
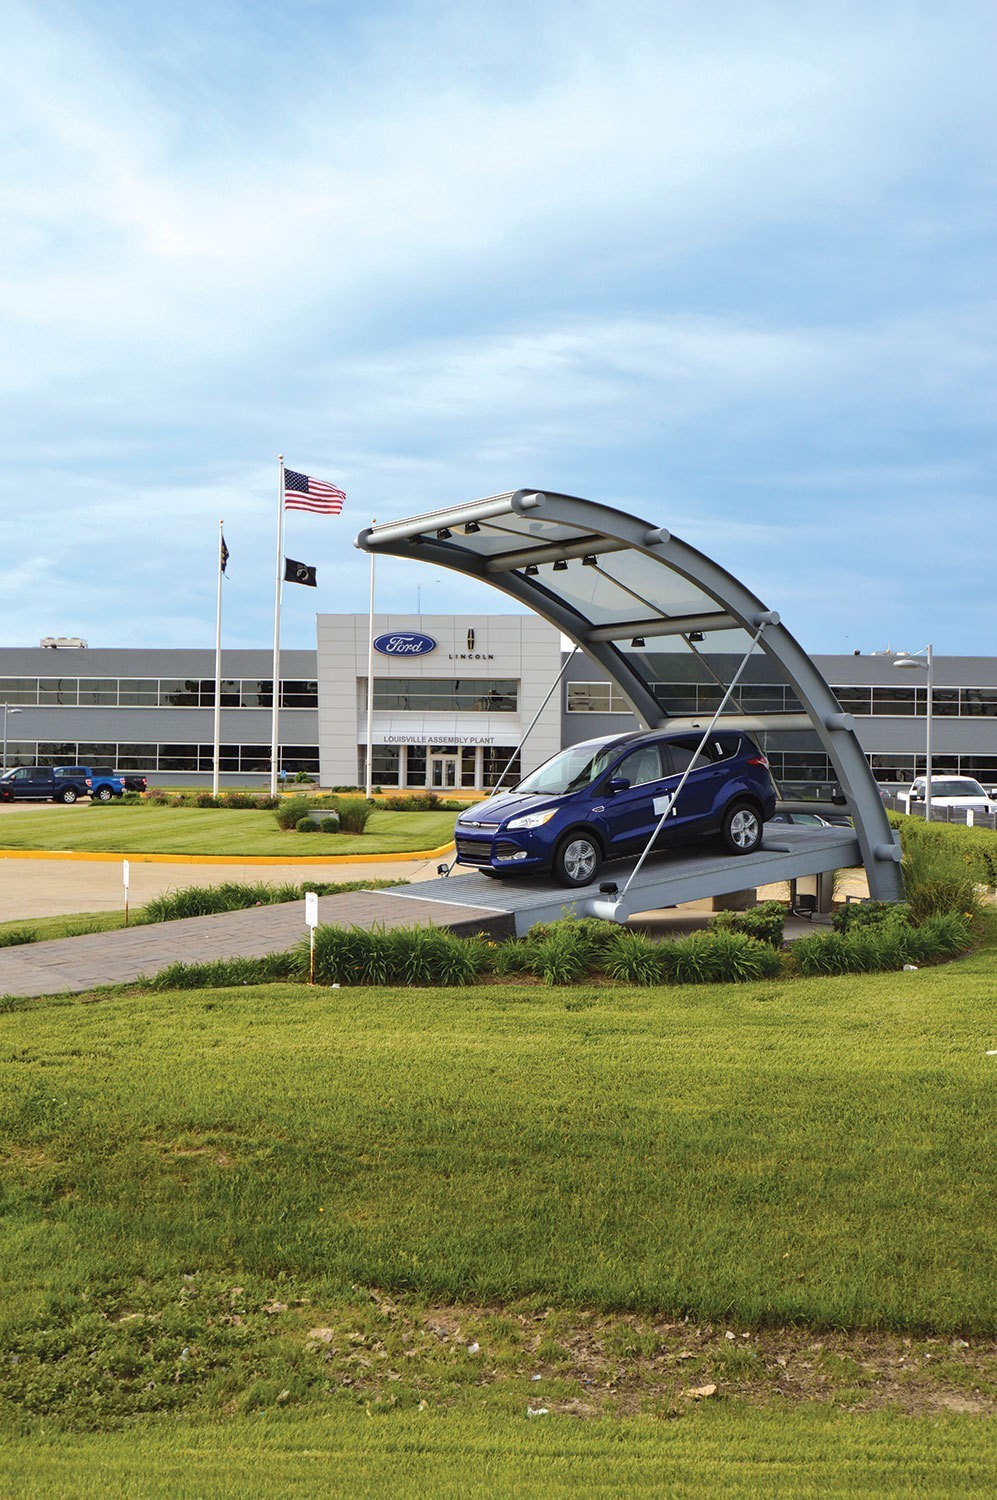
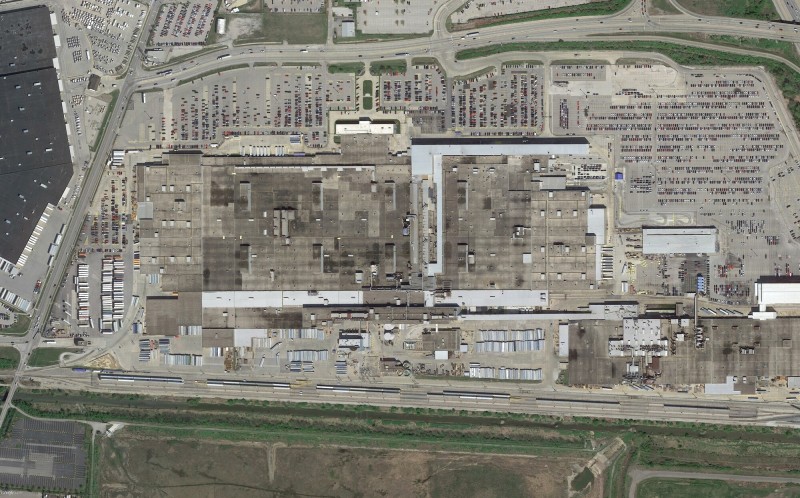
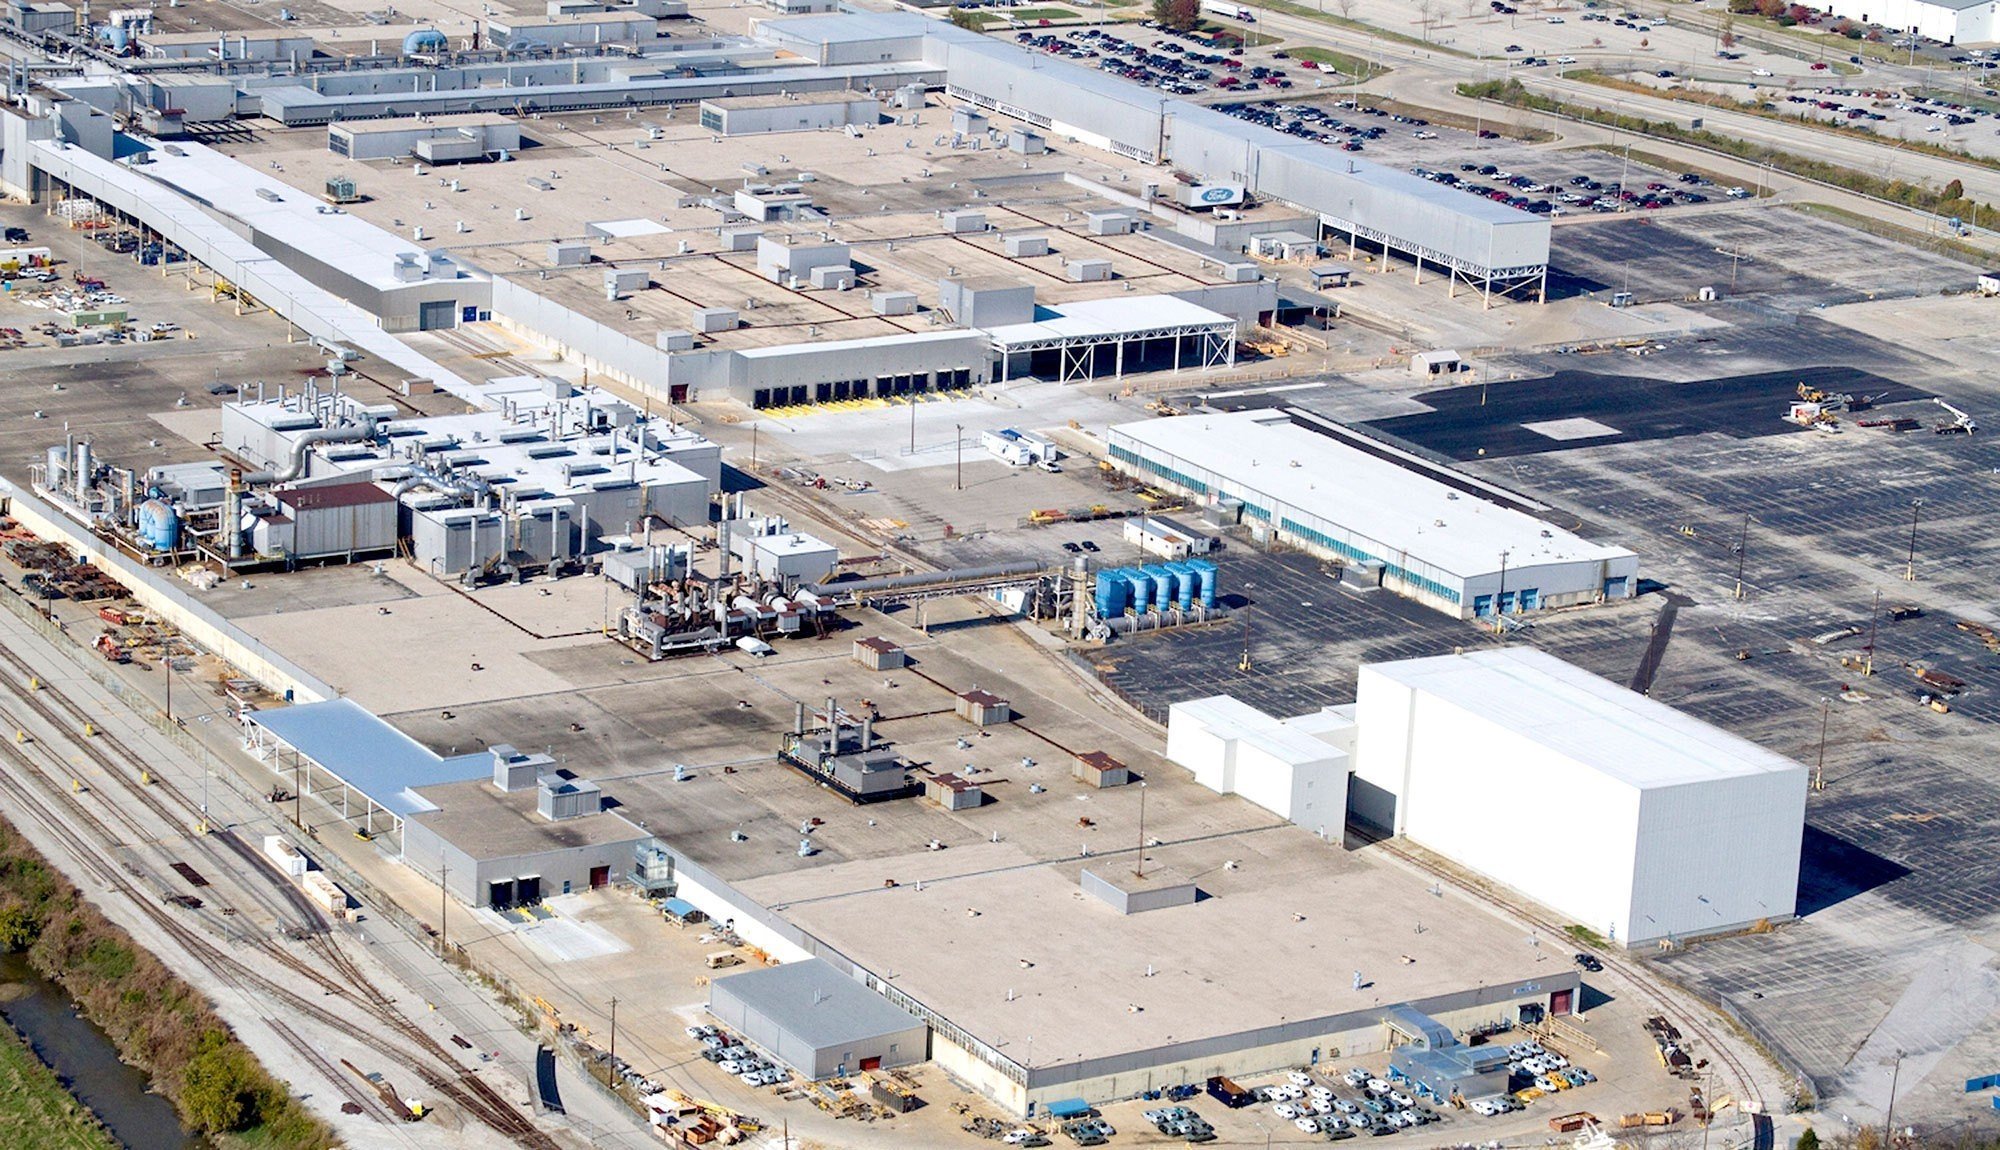
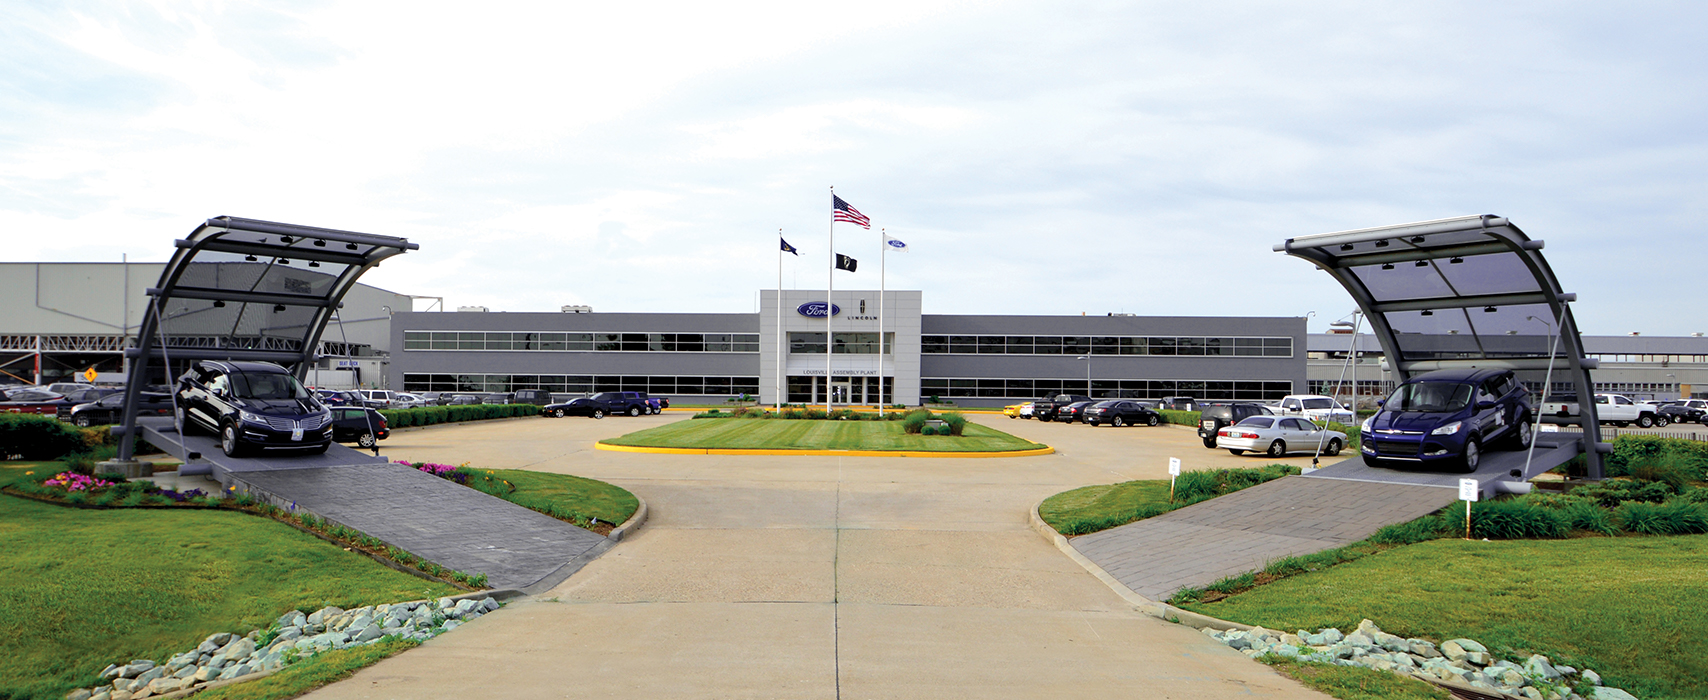
The Ford Louisville Assembly Plant sits off I-65 in Clark County, Kentucky, about twenty minutes south of downtown Louisville. It opened in 1956 as a truck plant and has gone through several identity changes since then. Right now it builds the F-150, the Maverick, and has assembled the Lincoln Aviator at various points. The facility covers roughly 2.3 million square feet of floor space and runs on three shifts around the clock. It is one of the larger Ford operations in North America by output volume. That phrase shows up in marketing materials and tourism stuff, but in practice the plant is just a big factory doing what every modern assembly plant does: receiving stamped metal, welding bodies, painting them, and putting mechanical components into those bodies on a moving line. The stamping plant adjacent to the main facility produces body panels that feed directly into the welding shop. Body-in-white moves to the paint shop, which runs electrocoat, primer, basecoat, and clearcoat in sealed environments. From there, the final assembly line pulls it all together with engines, transmissions, interiors, and underbody packages. It is a continuous flow operation with takt time measured in minutes, not hours. What most people miss about plants like this is how much the line balance depends on supplier sequencing. If a tier-one supplier is late on a dashboard module or a wheel end assembly, the line does not just slow down locally — it can cascade across the entire shift. I learned this the hard way during a supply chain disruption in 2022 when a single bracket supplier in Indiana had a power outage. The plant had about forty minutes of buffer before the line stopped cold. The workaround was rerouting through a secondary supplier in Ohio who had not been on the approved parts list for that specific trim level, but the quality team fast-tracked the audit and we got temporary approval within six hours. The line never stopped. It was messy but it worked.
Another thing beginners overlook is that the plant does not run a single product type through the whole line. The F-150 and the Maverick share the same final assembly line, which means the system has to handle radically different vehicle architectures on the same conveyor. The F-150 is a body-on-frame truck with a longer wheelbase. The Maverick is a unibody compact. The line uses a mix of fixed stations and flexible robotic cells to accommodate both. This flexibility costs money in tooling and programming, but it is necessary because demand for light trucks fluctuates independently of compact SUV demand. You cannot run one plant profitably on a single model year after model year. The paint shop is where the biggest capital investment sits. Modern automotive paint lines use e-coat baths, multi-stage robotic application, and infrared curing ovens. The Louisville plant runs waterborne paints now, which means lower volatile organic compound emissions but stricter temperature and humidity controls. If the humidity in the paint booth drifts outside the specified range, you get orange peel or fisheyes on the finish, and the reject rate climbs fast. I have seen operators shut down sections of the line for half a day just waiting on HVAC systems to stabilize after a weather front moved through. There is no bypass for that. Quality control at this scale relies heavily on automated vision systems. Cameras scan weld spots, panel gaps, and paint surfaces at every stage. The system flags defects in real time and routes affected vehicles to rework stations. Human inspectors still do spot checks, but the data comes from machines. The downside is that these systems generate massive volumes of data — terabytes per shift — and sifting through it to find patterns takes dedicated engineering staff. A lot of smaller plants struggle with exactly this: they have the sensors but not the analytics team to make sense of what the sensors are telling them. Defects repeat because nobody connects the dots between a weld variance in station twelve and a paint adhesion issue two hours later on the line.
If you are visiting the plant for a tour or an audit, plan for security. There are checkpoints, badge verification, and restricted zones. Some areas of the final assembly line are visible from walkways, but the robotics cells and paint shop interior are not open to general observation. The plant runs safety briefings for all visitors — PPE is mandatory in certain zones. Do not expect to wander near active equipment. The last person I knew who tried that got escorted out and their company was blacklisted from future tours. It is not personal, it is just how these places operate. The workforce at Louisville is largely union, represented by the UAW. Labor agreements cover wage scales, shift differentials, overtime rules, and seniority provisions. Disputes over staffing levels or work rules can ripple through production schedules. I have seen line speed increases negotiated as part of contract renewals, which sounds straightforward but actually changes the pace for every station on the line. Workers adapt, but adaptation takes time and there is usually a temporary dip in first-pass yield while people recalibrate. Management tracks this closely and plans maintenance windows around known transition periods. One counter-intuitive fact about modern assembly plants: having more robots does not necessarily mean higher quality. The Louisville plant uses robots for welding, painting, and some material handling, but critical joinery and fitment checks are still done by trained technicians. Robots are consistent within their programmed parameters, but they cannot judge whether a door closes with the right feel or whether a trim piece has the right gap variation across different lighting conditions. Humans handle that. The best plants blend automation and skilled labor rather than replacing one with the other. Pure automation sounds efficient on paper but breaks down in practice when you encounter a defect the system was not programmed to recognize.
Get the Full Details
The plant's environmental footprint has decreased significantly over the years. Stormwater recycling, LED lighting retrofits, and compressed air leak reduction programs are standard upgrades. The stamping shop recycles cutting oil and metal scrap internally. Paint overspray is captured through filtration systems. None of this is free — the capital expenditure for environmental compliance at a facility this size runs into the tens of millions over a decade — but regulatory pressure and corporate sustainability targets make it non-negotiable. Plants that delay these upgrades face fines and reputational damage that cost more in the long run. If you are looking to source parts from or supply components to a facility like this, the vendor qualification process is rigorous. You will go through audits covering quality management systems, delivery performance, capacity planning, and financial stability. The timeline from initial contact to approved vendor status typically runs six to eighteen months depending on your category. Expect multiple site visits, sample submissions, and pilot production runs before you get full release. Some suppliers get turned away after the first audit because their documentation does not meet Ford's Global Quality System requirements. It is not arbitrary — the standards exist because a single bad batch of brake calipers can take down an entire production run. The Louisville plant also handles some experimentation with alternative powertrains. Ford has used certain assembly lines for prototype runs of hybrid and electric variants, though the main Louisville line is currently focused on internal combustion and mild-hybrid powertrains. Battery-electric vehicle production at Ford is concentrated in other facilities right now. That may change as demand shifts, but retooling an existing line for BEV production is a multi-year project involving structural changes to the floor plan, new heavy-power electrical systems, and different safety protocols for handling high-voltage components. It is not a swap you can do over a weekend.
There is no single download or tool that captures how this plant operates. The closest thing to a hands-on guide would be Ford's supplier portal documentation, which is available through the Ford Motor Company vendor registration system. You need a Dun & Bradstreet number, a completed tax form, and a quality system certificate before you can access anything substantive. The public-facing information is limited to press releases and facility brochures. If you need technical specifications for a particular component or process, you go through the proper procurement channel. There is no shortcut around that. The reality of a facility like this is that it runs on coordination, not drama. Hundreds of suppliers, thousands of workers, dozens of subsystems all need to move in sync every single day. When it works, you get a vehicle rolling off the line every ninety seconds or so. When it does not, the problems are usually mundane — a missed shipment, a calibration drift, a scheduling conflict between two departments. The big failures are rare. The small ones are constant. The people who keep it running are the ones who know how to resolve the small ones before they become big ones.