Cutting parts on a Gerber system is mostly about setup, not magic.
You load the material, align the markers, set the cutting parameters, and fire the software. The machine does the rest. That's the surface version. Underneath, there's a chain of decisions that determine whether you get clean edges and consistent cycle times or scrap, tool breakage, and debugging sessions that eat half the shift. I've run Gerber accumark and AutoCut environments for years across fabric, leather, and composite laminates. The workflow is similar in principle but diverges sharply in practice depending on material behavior, blade type, and how tightly you control repeatability. If you treat it like a black box, you'll lose money on rework. If you understand where the system pushes back, you'll get reliable output without chasing symptoms.
What people mean by The Gerber Revolution Precision Engineering Meets Modern Manufacturing
The phrase usually points to how modern Gerber cutting and nesting ecosystems combine precise motion control, calibrated tools, and software-driven layout optimization. It's not a single gadget. It's the integration of vector-based pattern libraries, material-specific profiles, camera registration when needed, and automated feed management. The precision comes from calibrated kinematics and repeatable tool paths. The manufacturing part comes from batching orders, nesting efficiently, and tying cut data to ERP or PLM systems so you can trace yield and cycle time per SKU. In practice, that means you spend more time on profile validation and marker optimization than on pressing start. The machine itself is capable of submillimeter consistency when the environment and consumables are stable. Instability usually shows up as edge drag, inconsistent kerf, or marker collapse due to poor nesting constraints.
How the workflow actually runs on the floor
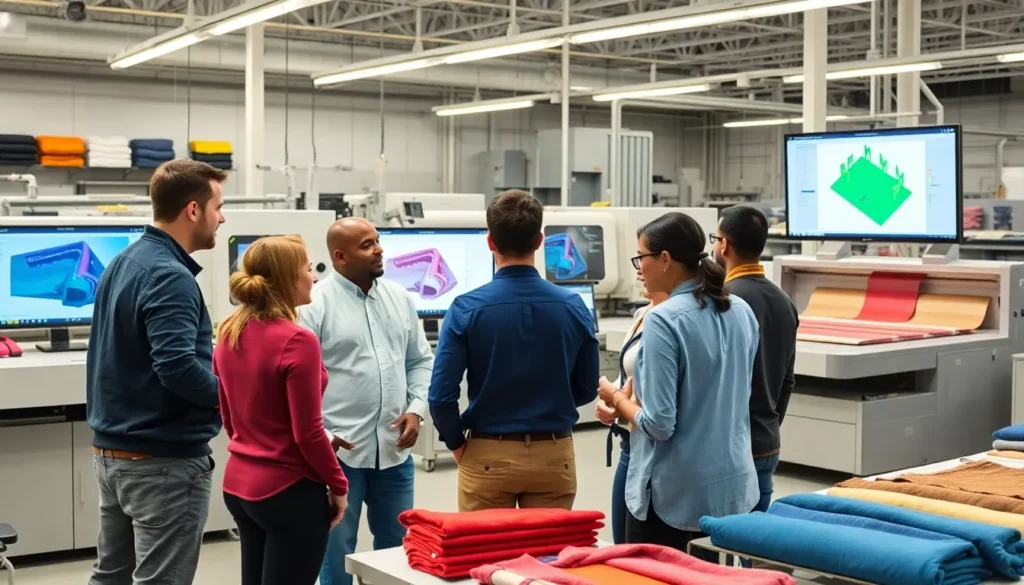
Start with a clean, well-managed pattern library. I keep patterns in a structured folder hierarchy by material type, grain direction rules, and finish requirements. Each pattern carries attributes for nap, one-way print, and seam allowance where applicable. That upfront organization saves hours later when you're building markers under pressure. Next, validate your cutting profiles. A profile is the combination of speed, force, lift height, compensation, and blade geometry for a specific material thickness and condition. I test profiles on scrap samples before committing to production runs. You want data for at least three thickness increments and for materials that have rested in the shop for twenty-four hours after unboxing. Moisture content and temperature shift cut dynamics more than most operators account for. When you build markers, use constraint-aware nesting. Tell the software which pieces must maintain grain alignment, which can rotate, and which have directional print or shade lots. Auto-nest aggressively, then manually adjust clusters that look stable but violate hidden constraints like bias stretch or layer count limits. I usually run an automatic nest, inspect the tight spots, then apply local manual tweaks rather than forcing the auto engine to handle everything. It's faster in the long run and less prone to weird artifacts near complex curves.
Get the Full Details
Register the material when tolerances demand it. Camera-based registration is useful for pre-printed fabrics or when layup shifts during handling. Calibration matters more than the camera itself. I recalibrate whenever I change camera mounts, lenses, or lighting conditions, and I verify with a test grid before cutting high-value stock. Without proper calibration, registration adds overhead without improving accuracy. Monitor tool wear with measurable checkpoints. I track cuts per blade and inspect edge quality at regular intervals. Dull blades cause fraying in synthetics and ragged edges in leather. I keep a simple log: blade type, material, thickness, count, and observed edge defect type. When the defect rate crosses a threshold, I replace the blade and update the profile compensation if kerf has shifted. This prevents cumulative errors that show up only after a full batch.
My actual workflow for a typical multi-material order
Import patterns and assign material attributes. Generate an initial nest with grain and shade constraints. Export layer sequence and tool assignment. Load material, align markers, and run a test strip to verify profile behavior. Adjust speed or force based on test results. Cut the full marker, inspect sample pieces for edge quality and dimensional accuracy, and record yield. If the job includes delicate trims or intricate notches, I switch to a smaller blade and reduce speed rather than pushing the same profile across all features. This approach usually reduces first-article failures to under five percent on stable materials. Delicate laminates and coated leathers can still spike failure rates until you dial in the right lift height and adhesion settings for the backing film.
Common mistakes that look harmless but wreck throughput
Skipping profile validation is the biggest one. Operators often reuse a profile from last month without checking current blade condition or ambient humidity. That's how you get sudden edge melting in polyester blends or excessive friction burn in dense neoprene. Over-relying on auto-nest without enforcing constraints produces markers that look efficient but violate production rules. You'll discover issues during cutting when pieces shift or grain direction errors become obvious after sewing. Always run a manual review pass focused on constraint violations, not just density. Neglecting maintenance on guidance systems and belts leads to drift that manifests as dimensional inconsistency across large markers. I schedule weekly checks of rail lubrication, belt tension, and spindle runout measurements. Small deviations compound over long cuts and are harder to trace back if you don't log them.
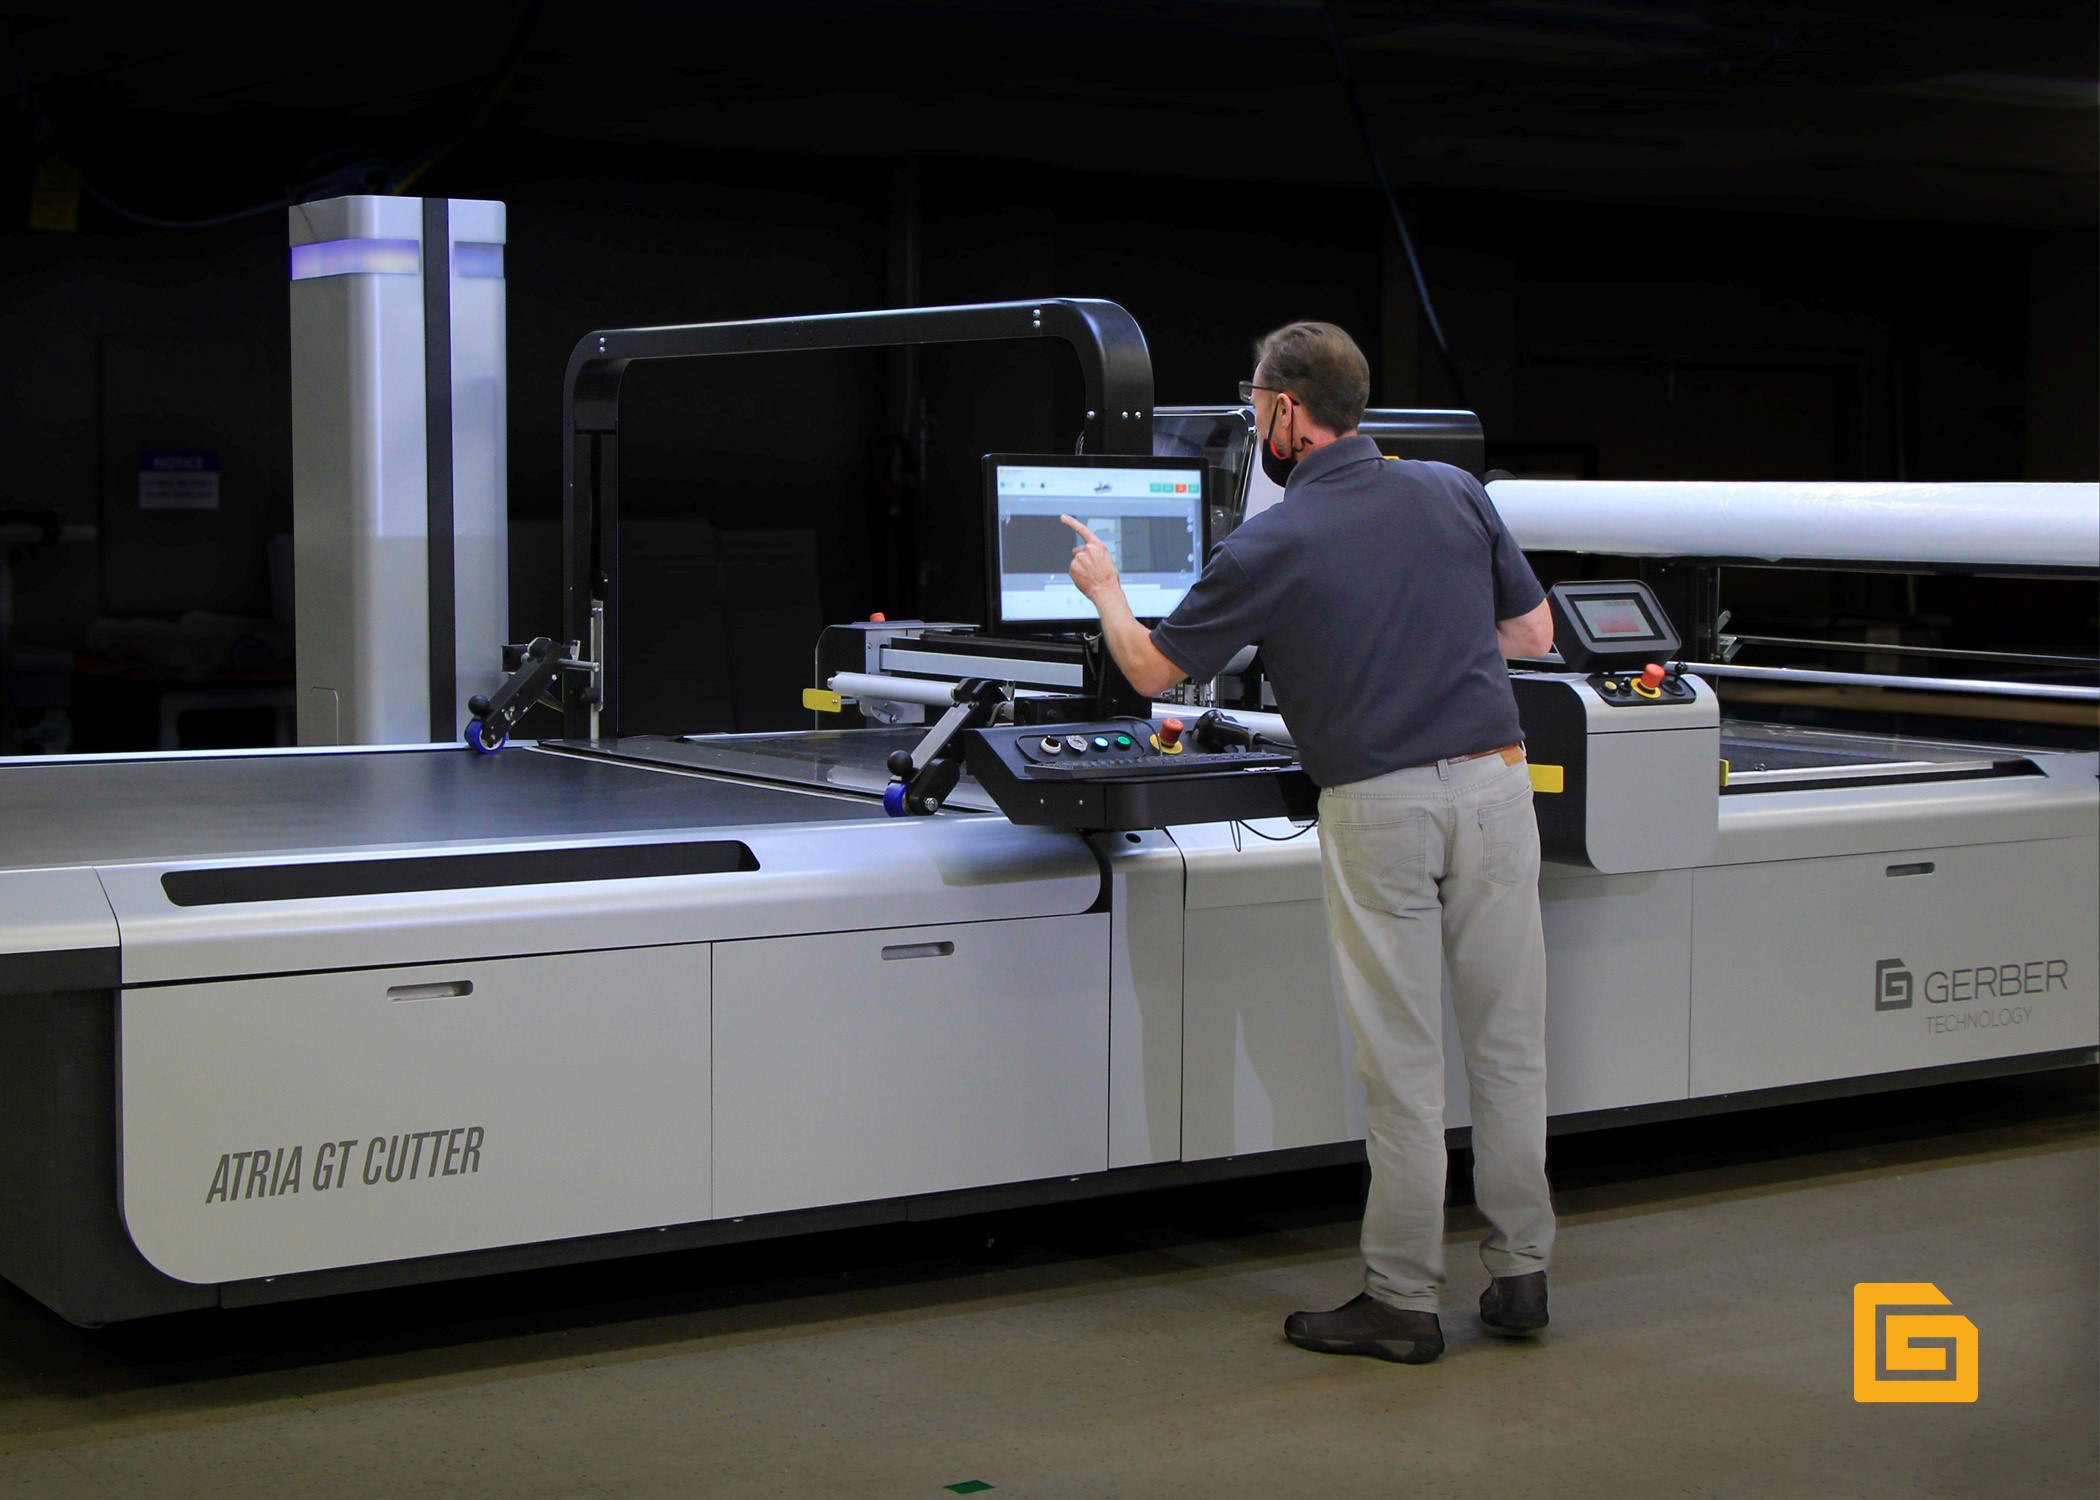
Another frequent error is ignoring layer count limits for thick or sticky materials. Stacks above the recommended height cause compression errors and uneven cutting through the bottom layers. The software may allow it, but the physical material won't behave consistently. I cap stacks based on empirical tests for each material type and adjust when supplier batches change.
A specific problem I ran into and how I fixed it
I was cutting multi-layer carbon fiber prepreg sheets for an automotive interior project. The edges showed micro-fraying and resin smear despite using a fresh diamond-coated blade and optimized speed. The nesting software reported excellent utilization, but yield dropped because downstream trimming was required on most panels. The root cause was vibration resonance at certain spindle speeds combined with slight deflection in the cutting head mount. I resolved it by reducing the spindle speed by fifteen percent, adding a damping pad under the head carriage, and switching to a slower feed rate for the outer contour passes while keeping a faster rate for internal cutouts. I also adjusted the blade compensation value after measuring actual kerf with a caliper on test coupons. Edge quality improved enough to eliminate secondary trimming on eighty percent of parts, which saved roughly twenty minutes per large marker in post-processing. This workaround isn't a universal fix. It's specific to stiff, brittle laminates with adhesive backs that amplify tool vibration. For woven fabrics or foams, the same changes would reduce throughput without benefit.
When Gerber-style precision systems fall short
They struggle with highly variable handmade materials like hand-dyed textiles or irregular hides where thickness and density fluctuate across the roll. Automated profiling can adapt within limits, but extreme variance still requires manual intervention or offline sorting. If your supply chain lacks consistency, expect higher labor costs per unit regardless of software quality. High-speed cutting of very thin films often leads to migration and static issues that no amount of calibration fully eliminates. You'll need anti-static measures, slower speeds, and sometimes vacuum stabilization to maintain registration. In those cases, the system's precision is capped by material behavior, not machine capability. Another limitation is software licensing and ecosystem lock-in. Moving pattern libraries or historical data to another platform can be tedious due to proprietary formats and custom profile structures. Plan migrations early and maintain exported neutral formats like DXF or AI alongside native files if you anticipate future vendor changes.

If your production volume is low and product mix changes weekly, the setup time may outweigh the automation benefits. Manual cutting or smaller plotters can be more economical until you reach a threshold where marker optimization and repeatable profiles pay for themselves.
Practical tips that actually move the needle
Keep a calibrated reference sample set for each material family. Use it monthly to verify profile consistency and detect subtle machine drift before it affects production. This takes about ten minutes and prevents batch-level surprises. Document every profile change with date, blade type, material lot, and environmental conditions. You'll thank yourself when a quality issue surfaces weeks later and you need to trace back parameters. Train operators on constraint-aware nesting rather than purely density-driven nesting. A slightly less dense marker that respects grain, shade, and layer limits will produce fewer rejects and require less manual rework.
Schedule preventive maintenance based on usage hours, not calendar dates. Spindle bearings, guide rails, and belt systems wear proportionally to cycles and load. Hour-based scheduling aligns maintenance with actual stress.
Alternatives worth considering
For very small batches and frequent design changes, manual waterjet or hand-guided CNC routing might offer more flexibility despite lower throughput. For high-volume apparel with simple geometries, ultrasonic cutters can outperform blade systems on certain synthetics due to sealed edges that prevent fraying. If your primary challenge is material variability rather than geometric complexity, investing in upstream material sorting and grading may deliver better ROI than upgrading cutting hardware alone. Precision engineering cannot fully compensate for inconsistent input stock. Some shops blend Gerber systems with robotic material handling for continuous feed operations. That integration adds capital cost and programming complexity but can significantly improve labor utilization on long runs with standardized layups.
Final notes on adoption
The Gerber Revolution Precision Engineering Meets Modern Manufacturing when you treat it as a disciplined workflow rather than a one-click solution. The hardware is reliable. The software is powerful. The variable is human process control. Establish clear standards for pattern management, profile validation, constraint-aware nesting, and maintenance logging. Measure outcomes with yield, cycle time, and rework rate, not just machine uptime. I recommend starting with a pilot line on your most stable material family. Quantify baseline metrics, implement the workflow steps outlined here, and track improvements over thirty days. Once you have calibrated data, extend the process to more challenging materials incrementally. This reduces risk and gives you concrete evidence of where adjustments are needed. There is no universal profile, no perfect nest, and no system that eliminates operator judgment. The goal is predictable performance through documented practices and continuous measurement. That's where the real precision lives.