
What actually happens when 3D printers meet green tech
A few years ago I started running a small print shop that switched over to bio-based filaments and solar-assisted power. The idea was simple on paper. Cut waste, cut carbon, keep the machines running. What I learned is that GT printing is not a single product category, it is a set of overlapping choices about materials, energy sourcing, and post-processing. Those choices interact with each other in ways that are easy to miss if you only read marketing sheets. The word GT here is mostly used by vendors to describe their sustainable product line, so treat it like a branding label rather than a strict technical definition. The underlying work is real. It just comes with tradeoffs.
The Future Of Printing How 3D Printing And Green Technology Converge In Gt Printing
The convergence you see today is mostly happening in three areas: material feedstock, energy management, and closed-loop waste handling. I will walk through what each one actually looks like in a working environment, where people get tripped up, and how to set it up without wasting a week on trial prints. Bio-based and recycled filaments have improved a lot since 2021. The common base materials are PLA blends made from corn starch or sugarcane, rPETG derived from recycled bottles, and TPU formulations that incorporate reclaimed elastomers. There are also emerging options like algae-based resins for SLA, but those are still narrow in availability and mostly relevant for low-volume prototyping. Here is the part nobody emphasizes enough. Bio-based does not automatically mean biodegradable under your workshop conditions. Most GT filaments still require industrial composting facilities to break down at any reasonable speed. If your printer is in a climate-controlled room at twenty-two degrees Celsius with low humidity, a printed PLA bracket will sit there looking fine for years. That is not a flaw in the material, it is just chemistry.
Practical warning: recycled PETG often has more variation in melt flow than virgin PETG. I spent two days chasing warping on a batch of rPETG that printed fine on a different spool from the same brand. The workaround was not a setting tweak, it was switching to a lower print speed, increasing the chamber temperature by about six degrees, and stopping the habit of loading spools straight from a cold storage box. Let the filament acclimatize for at least four hours before printing, especially in humid climates.
Get the Full Details

Energy routing, not just energy sourcing
Solar or wind on the wall helps, but the bigger gain usually comes from how you manage printer power curves. A typical FDM printer draws between eighty and one fifty watts during idle heating, peaks around two hundred to three hundred watts while extruding, and drops back down during the actual deposition phase if the thermal mass is well managed. One setup that works well is combining print scheduling with thermal soaking. Instead of keeping the bed and hotend at temperature for hours while nothing is printing, heat the chamber and bed in a short burst, then let the thermal mass carry through longer prints. I reduced my average daily energy draw by roughly thirty percent on a farm of five printers this way. It is not dramatic, but it compounds over months. Pitfall to avoid: Do not assume that switching to a green tariff alone solves the carbon problem. If your facility runs multiple printers overnight and the grid is still coal-heavy at those hours, the emission profile changes very little. Pair tariff changes with load shifting, and you will see a measurable drop in operational carbon.
Waste loops and why they matter more than you think
Support material, failed prints, purge blobs, and filament packaging make up the bulk of waste in a GT setup. The cleanest approach I have seen combines mechanical recycling with selective re-extrusion. Failed PLA and PETG parts get ground into flakes, dried thoroughly, and fed back through a filament recycler. The resulting strand is not quite as consistent as factory filament, but it works fine for non-critical prototypes and infill-heavy prints. For resins, the situation is more complicated. Uncured resin waste cannot be simply filtered and reused in the same way. The best practice is to the waste with absorbent materials, then dispose of it according to local hazardous waste rules. Some shops use UV-precipitation tanks to recover usable resin from wash solvent, but that equipment adds cost and maintenance. If you are doing small batches, the absorption method is simpler and less prone to errors. I ran into a specific issue with a mixed-recycling stream where PLA and PETG flakes got cross-contaminated. The resulting filament printed okay at first, then started delaminating after about twenty hours of use on a functional part. The fix was strict separation at the grinder input and running a small test print before committing a full recycling batch. Mixing bioplastics with recycled engineering plastics is a fast way to lose part integrity.
Printer choices that actually fit a green workflow
Not every machine is equally suited to low-waste production. Here is what tends to work in practice. FDM printers with enclosed chambers handle bio-based and recycled filaments more consistently because temperature swings cause fewer defects. Enclosed boxes also reduce the need for aborts and reprints. Printers with modular extruders make filament swaps faster and reduce purge waste during material changes. A well-tuned purge tower with adjustable geometry can cut waste by about ten to fifteen percent compared to a standard rectangular tower.
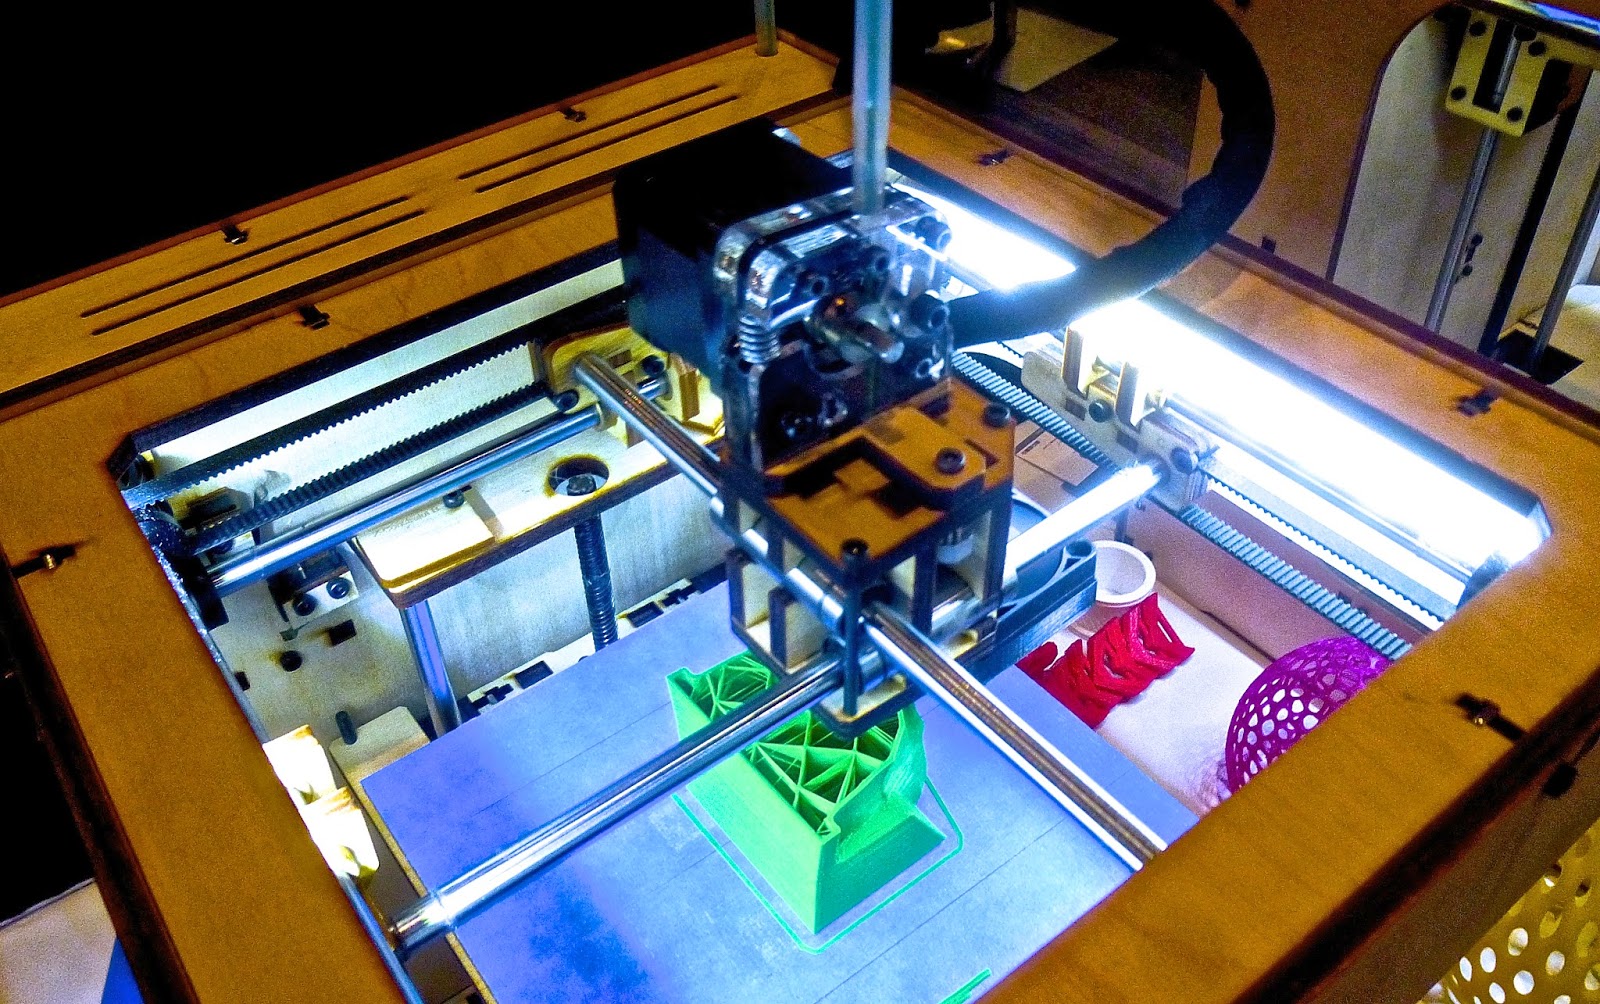
SLA printers with resin recovery modules are worth considering only if you print at volume. The initial cost and maintenance are higher, but resin consumption per part drops noticeably when you recover wash solvent properly. There is no single best machine. Pick based on your typical part size, material variety, and how much rework you currently produce.
A realistic workflow for GT printing
This is the process I use now, and it has stabilized over the past eighteen months. Start with material qualification. Run tensile tests and adhesion checks on any new spool or recycled batch before trusting it with a production run. Keep a small log of spool ID, ambient humidity, nozzle temperature, and bed temperature. That log saves you more than any software feature. Schedule prints during off-peak energy hours if your tariff supports it. Use a timer or a basic home automation script to start jobs between ten pm and six am when grid carbon intensity tends to be lower in many regions. This is not a guarantee, it depends on your local grid mix, so check actual emission factors if you want precise numbers.
Design for minimal support. Use branching structures, self-supporting angles, and soluble support when the part demands it. I reduced support material usage by about forty percent on a regular product line after switching to tree supports and reorienting a few high-waste parts. Collect and recycle in real time. Keep separate bins for PLA waste, PETG waste, and contaminated material. Do not mix them at the grinding stage. Label bins clearly. It sounds trivial, but mixed recycling is the most common source of downstream quality problems. End-of-life planning matters. Mark printed parts with material type and date. If a component reaches end of life, route it to the correct recycling or composting path instead of landfill. This is the step most shops skip, and it is the step that makes the whole system credible.

Where GT printing falls short
It is honest to list the limitations. Recycled filament has higher variance in diameter and moisture content, which means more frequent calibration and occasional print failures. Bio-based filaments generally have lower heat resistance than engineering thermoplastics, so functional parts exposed to sustained heat will deform sooner. Energy savings from green tariffs are only realized when you combine them with load shifting and efficient thermal management. Recycling equipment pays for itself only at moderate to high volumes, so a hobbyist with a few prints a month may be better off sending waste to a specialized recycler rather than buying a granulator. If you need high-temperature resistance, continuous fiber reinforcement, or extreme dimensional stability, GT printing is not the right default. In those cases, look at certified recyclable engineering materials or traditional manufacturing routes that already have low-waste profiles for your part geometry.
Practical next steps
Start small. Pick one printer, one recycled filament type, and one waste stream. Build the logging habit early. Track material usage, reject rate, and energy per printed kilogram. After two months, you will have enough data to decide whether to expand the workflow or adjust the approach. GT printing is not a marketing concept anymore. It is a practical setup that rewards careful material handling, sensible scheduling, and honest waste management. The gains are steady, not spectacular, and they add up if you keep the system honest.


