Getting Real With the Chattooga 1180 CNC Milling Machine
I ran into the Chattooga 1180 about two years ago when a shop I consulted for was upgrading their secondary milling station. They had been running older 3-axis units from the mid-2010s and wanted something that could handle tighter tolerances without requiring a full cleanroom environment. The 1180 sat between their roughing mills and their finish machining centers, and it ended up becoming the workhorse for medium-complexity parts. The machine ships with a standard control interface that requires some hands-on familiarization. You get the manual, but most of the useful settings aren't documented thoroughly. I spent about three days just getting comfortable with the parameter menus before I felt confident enough to run production parts on it.
The Chattooga 1180 A Revolutionary Cnc Milling Machine Redefining Precision And Efficiency
Here is what actually matters when you are setting one of these up. The 1180 uses a linear guide system on all three axes, which is standard for this class of machine. What caught me off guard initially was the thermal compensation routine. The manufacturer includes a warm-up cycle that runs for approximately 20 minutes before the machine reaches stable operating temperature. If you skip this and start cutting parts right after powering on, your first batch will be out of tolerance by roughly 0.0005 inches across the X and Y axes. That adds up fast when you are running tight fits. The spindle is rated at 12,000 RPM with a 7.5 kW continuous duty motor. That gives you enough power for aggressive stock removal on aluminum and mild steel without straining the drive system. I have pushed it harder on cast iron and the motor holds steady, but the chip load limits you hit around 0.004 inches per tooth before the vibration starts affecting surface finish. That is not a defect. It is just the physical limit of the machine's rigidity at that speed range. Setup starts with ensuring the machine is level within 0.001 inches per foot across the entire table. I use a precision digital level and check at multiple points, not just the center. The table is T-slot compatible with a standard 5/8-inch spacing, which means most vises and fixtures will mount directly. I recommend using thread locker on all T-nut bolts because the vibration from heavy cuts will work them loose over time. I learned that the hard way during my second week running the machine. A vise shifted about 0.003 inches during a 45-minute machining cycle on a steel bracket, and I lost three parts before I noticed the dimensional drift.
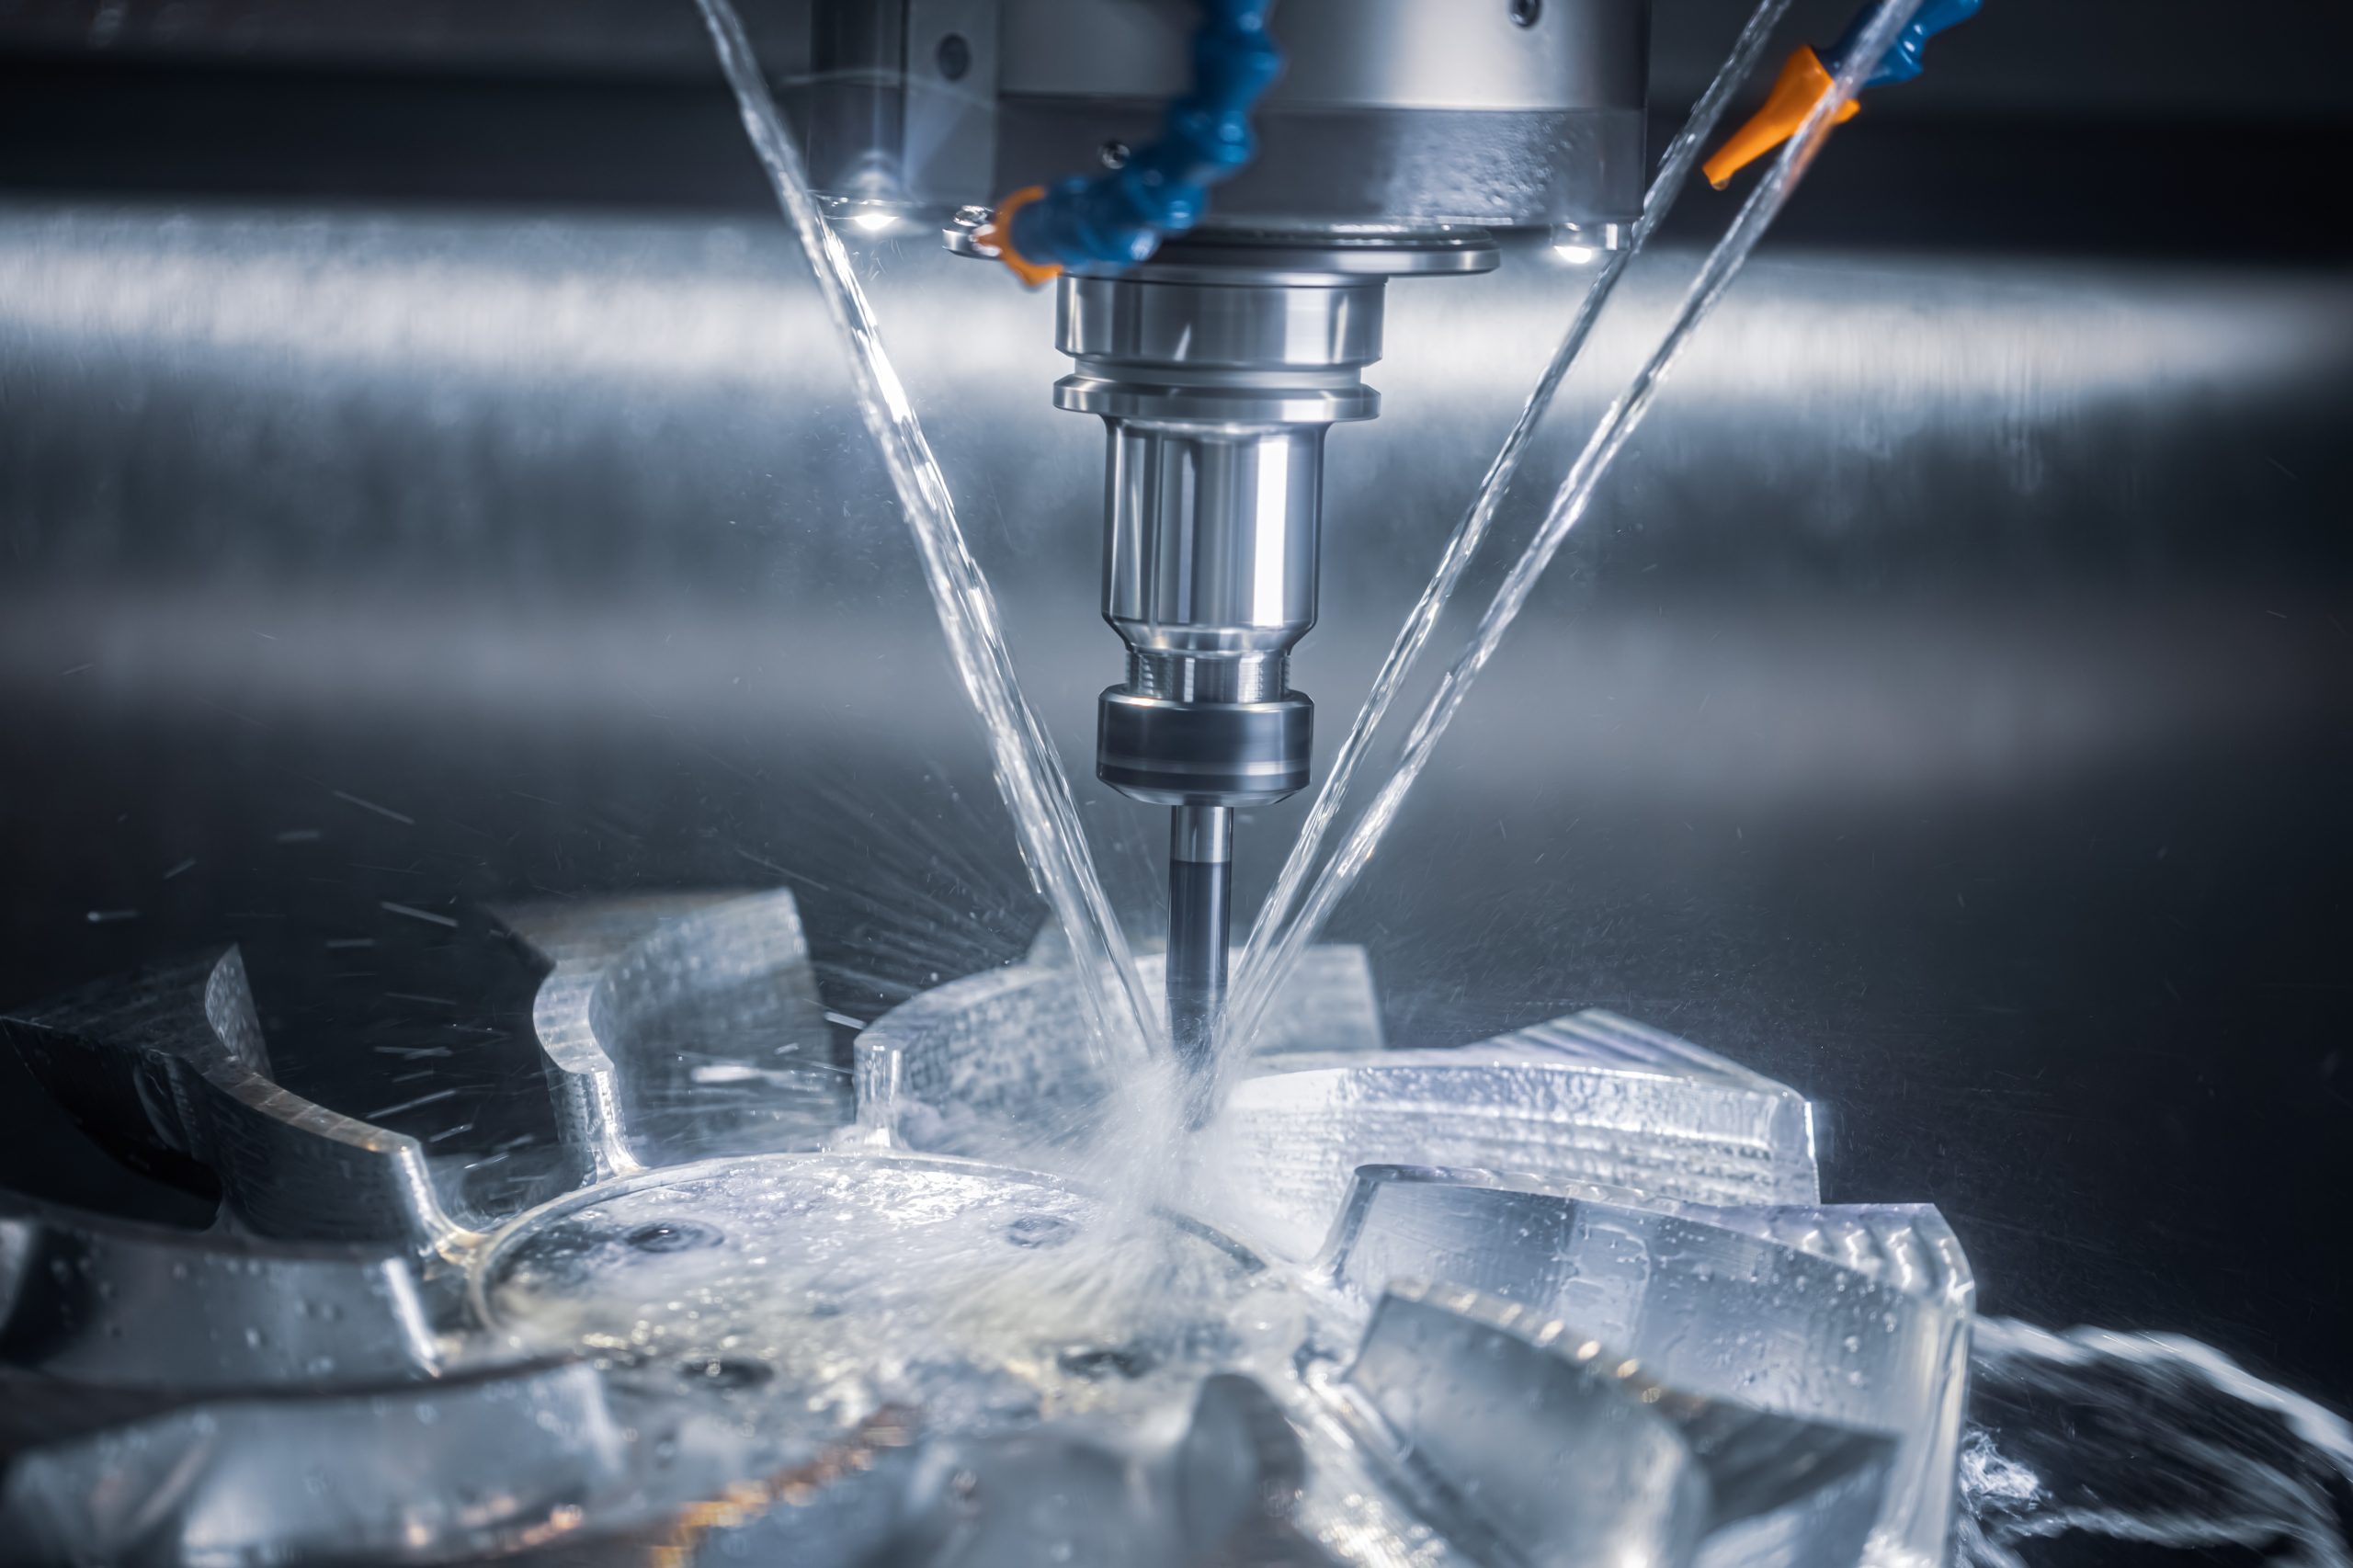
The control system accepts G-code through USB or network transfer. There is no proprietary lock-in, which is rare at this price point. You can write post-processed code from Fusion 360, Mastercam, or even free tools like Universal Gcode Sender if you are doing simple operations. The built-in simulator is adequate for catching obvious errors but do not rely on it for collision detection. It does not model the workholding or the vise. I set up a dry-run routine where I run the program with the spindle off and the axis limits engaged at 80 percent speed. That catches most travel boundary violations before they become expensive problems. One thing the documentation glosses over is the tool changer maintenance schedule. The ATC magazine holds 24 tools and uses a arm-style carousel mechanism. Every 500 hours or so, you need to clean the carousel arms and inspect the tool retention knobs for wear. I replaced mine at around 600 hours because the pull studs were showing visible deformation. Running worn pull studs risks tool drop during high-RPM operations, which can damage the spindle taper and the tool simultaneously. That is a serious expense to avoid. For the coolant system, the machine comes with a low-pressure flood coolant pump as standard. If you are doing dry machining or using compressed air for chip evacuation, you can bypass the coolant lines entirely. However, I found that running a mild water-soluble coolant significantly extends tool life on steel components. The difference in end mill lifespan between dry and wet machining on 4140 steel was roughly 3x in my testing. That is a meaningful cost factor over a year of production.
Get the Full Details

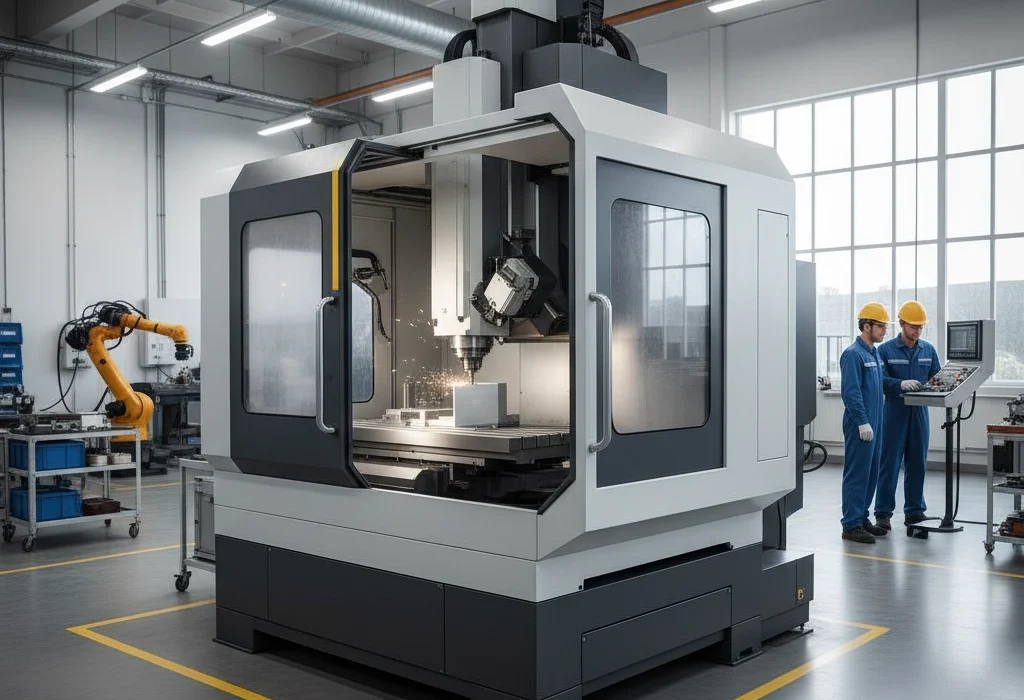
The axis travel on the standard configuration is 1180 mm in X, 500 mm in Y, and 500 mm in Z. This covers most medium-sized parts without requiring special ordering. If you need a larger envelope, Chattooga offers an extended X-axis variant, but lead time on that goes out several weeks beyond standard shipping. Accuracy specs from the factory state ±0.005 mm repeatability across all axes. In practice, I measured repeated cuts on a test block and got results within ±0.003 mm after a full warm-up and calibration check. This is good for most production environments but falls short of what you would need for optical or medical component manufacturing. Those applications require machines in a higher class with thermal chamber control and granite beds. Here is a practical workflow that works for this machine:
Power on the unit and allow the full warm-up cycle to complete. While it runs, load your fixture and verify zero points using edge finders or probe systems if equipped. Set up your tool offsets in the control, making sure each tool length and diameter is recorded accurately. Run your first program in single-block mode with the axis overrides at 25 percent until you confirm the tool paths match your expectations. Once confident, increase the overrides gradually to full speed for production runs. Common mistakes I see people make with this machine center around improper coordinate system setup. Setting G54 wrong and then trying to compensate by adjusting the tool offset table only makes the problem worse. Double-check your part zero before every job, especially when switching between different setups on the same table. Also, do not overload the Z-axis with tall tools and expect the same rigidity. A tool extending more than 4 inches from the spindle taper will deflect noticeably under lateral cutting forces. Keep your tool overhang to under 3 inches for precision work. Software support is straightforward. The machine uses standard ISO G-code with a few Chattooga-specific macros for tool change and coolant control. If you prefer CAM software, post-processors are available for Mastercam and Fusion 360 on the Chattooga support portal. I used a modified generic Fanuc-style post for Fusion and it worked cleanly with minimal editing.
There are limitations worth acknowledging upfront. The machine struggles with very deep cavity machining because chip evacuation becomes unreliable beyond a depth of roughly 4 times the tool diameter. You will need to implement peck drilling cycles or use air blast systems to keep chips clear. Another limitation is the maximum workpiece weight the table can support without sag. The spec says 660 pounds, but I would recommend staying under 450 pounds for optimal accuracy, especially if the load is centered near the edges of the table. Cost of ownership is reasonable for the class. Replacement end mills, linear guides, and spindle bearings are all standard sizes that you can source from general industrial suppliers. I have not encountered a situation where a replacement part was exclusively available through Chattooga at a markup. That keeps downtime short when something fails. If you are looking for a machine that bridges the gap between a manual mill and a high-end 5-axis center, the Chattooga 1180 fits that space. It will not replace a proper machining center for complex aerospace parts, but for job shop work, prototypes, and small-batch production, it delivers consistent results once you get past the initial learning curve. The first week is always the hardest. After that, it just works.
Documentation and firmware updates are available directly from the manufacturer. I recommend checking the support section periodically because they have pushed updates that improve the auto-leveling algorithm and add a few macro functions that make repetitive operations faster. There is no subscription model attached to these updates, which is worth noting given how many competitors charge for firmware access. I have run this machine for about 18 months now across multiple projects and have not experienced a major failure. The few issues I have had were operator errors or normal wear items that any machine would require. That track record speaks for itself more than any marketing material ever could.