Understanding Modern Die Casting Technology and What Actually Changes on the Floor
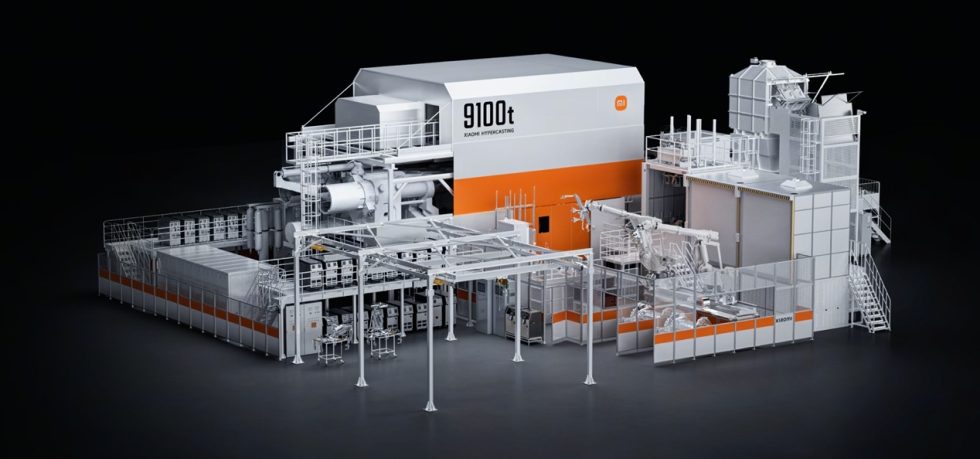
Die casting hasn't changed as much as the vendors would have you believe, but there are real improvements happening. The industry has been grinding out aluminum and zinc parts the same way since the 1950s. Recently, a lot of companies have been pushing new approaches that claim to solve the same old problems. I've been running die casting operations for long enough to separate what works from what just sounds good on a sales deck. When people talk about The Big Show Die Revolutionizing Die Casting With Innovative Technology, they're usually referring to a combination of vacuum-assisted casting, advanced thermal management, and real-time monitoring systems. Not all of it is new. The pieces have existed separately for years. What's different now is how they're integrated into a single workflow that actually affects cycle times and defect rates. The core idea is straightforward. Traditional die casting traps air inside the mold cavity as molten metal fills it. That air creates porosity, weak spots, and rejection rates that eat into margins. The innovation layer addresses this by pulling a vacuum before each injection, controlling the thermal profile of the die more precisely, and monitoring the entire fill process with sensors. The result is a denser casting with fewer rejects.
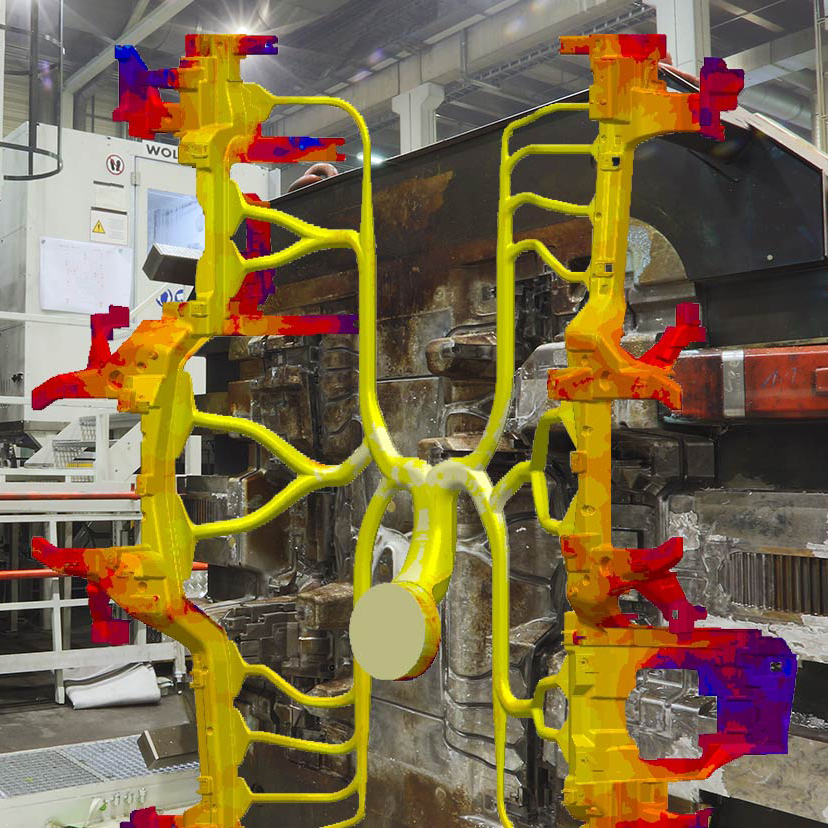
In practice, the most noticeable difference shows up in the first article. Normally when you run a new die, you cast scrap until you dial in the parameters. With the integrated approach, you spend less time on that initial debugging. I had a project last year where we were producing a complex aluminum housing for an automotive component. The part had thin walls and deep pockets that always led to cold shuts and shrinkage porosity. We ran it on a standard machine for three days and scrapped about forty percent of the first batch. Switched to the vacuum-assisted setup with thermal monitoring, and we hit acceptable parts on the fourth shot. That kind of difference matters when you're under contract deadlines. The technology isn't magic. It has constraints. Vacuum systems add complexity to the die design. You need sealed vent channels and careful gate placement. If your die isn't machined with those considerations in mind, the vacuum won't help and you'll waste money on a retrofit that doesn't work. I learned this the hard way on a job where we tried to bolt a vacuum system onto an existing die that was originally designed for conventional casting. The seals leaked, the vacuum never held, and we ended up spending more on modifications than the upgrade was worth. The workaround was to go back to the die designer and start the venting and sealing strategy from scratch rather than trying to adapt it afterward. Another thing that catches people off guard is the maintenance requirement. These systems demand more attention than traditional setups. The vacuum pumps need regular servicing. The temperature sensors drift and need recalibration. The software that tracks the process parameters requires someone who understands both the casting and the data. If your shop doesn't have that kind of staffing, you're looking at either hiring or outsourcing, and neither is cheap.
Here's something most guides don't mention. The best results come from matching the technology to the right alloys and part geometries. Thin-wall applications benefit the most. Parts with tight tolerance requirements see the biggest yield improvement. But if you're casting simple, thick-section parts that don't require high integrity, the investment may not pay back. The math gets worse when you factor in the cycle time. Vacuum-assisted casting can add a few seconds to each cycle because of the evacuation and equalization phases. For high-volume runs, those seconds add up. You need to calculate whether the reduction in scrap offsets the slower cycle time. In my experience, it does for complex parts but not for simple ones. Cost is another factor. A full integration of vacuum systems, thermal management, and monitoring can run anywhere from twenty thousand to over a hundred thousand dollars depending on your machine size and the scope of the upgrade. Some suppliers offer it as a package with the machine. Others want you to source the components separately and manage the integration yourself. The package approach is easier but often more expensive. The DIY route gives you control but requires genuine technical knowledge to pull off without creating more problems than you solve. Downstream processing also changes. Vacuum-assisted castings tend to have less porosity, which means less need for X-ray inspection and rework. That's a real cost saving. But you still need to machine, finish, and treat the parts. Don't fall into the trap of thinking this technology replaces your post-processing workflow. It doesn't. It just makes the starting material better.
Get the Full Details

If you're considering implementing this in your operation, start by auditing your current defect patterns. Look at what percentage of your rejects are porosity-related versus other issues like flash, misruns, or surface defects. If porosity is the dominant problem, the technology addresses your main pain point. If it's something else, you might be better off focusing on die maintenance, lubrication control, or injection profile optimization before spending on an upgrade. There are also smaller shops that have found success by partnering with foundries that already have this technology rather than investing in it themselves. It's not the most independent path, but it can be the most economical if your volume doesn't justify the capital outlay. The field moves fast. New sensor systems and software platforms appear regularly. What I can tell you from experience is that the fundamental physics haven't changed. Molten metal fills a mold. Air needs to escape. Heat needs to be controlled. Any technology that helps with those basics has value. Anything that claims to do something else is probably overstating its case.