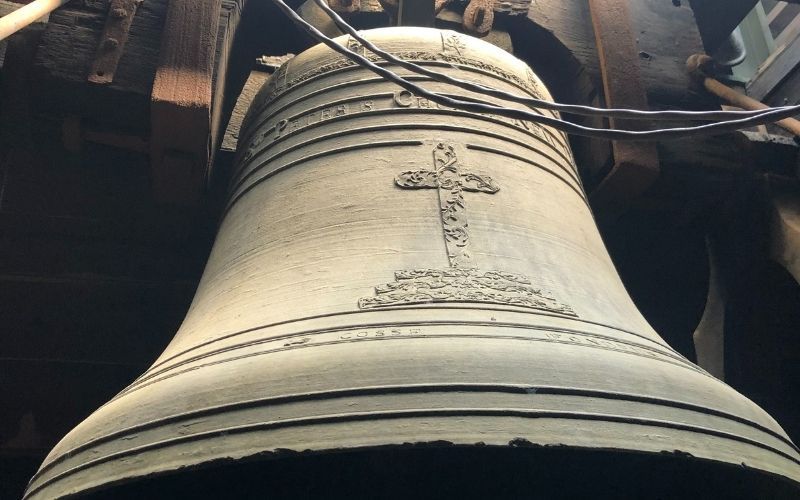
The Engineering Behind Sacred Sound
I spent about three years working with bell foundries across Europe, mostly restoring old tower bells for parish churches. Most people have never seen the inside of a bell foundry, and they certainly haven't watched a 300-kilogram bronze bell being cast. The topic of The Beautiful Symmetry Of Faith Unveiling The Secrets Of The Catholic Church Bell is one that sits at the intersection of metallurgy, music theory, and centuries of tradition, and it is far more technical than most people realize. A church bell is not simply a lump of metal that makes noise when you hit it. A properly tuned bell has a harmonic series that is almost impossible to achieve. The problem is that when you strike a hollow bronze cylinder, the vibration modes interfere with each other in chaotic ways unless the geometry is extremely precise. This is why bell founding is still considered one of the most difficult casting arts in existence.
The Beautiful Symmetry Of Faith Unveiling The Secrets Of The Catholic Church Bell
The symmetry in a church bell is mathematical, not decorative. The profile of a bell — the way the interior curves from the crown down to the sound bow — follows a specific geometric formula. Founders use what is called a bell curve, which is generated from a combination of circular arcs and parabolic sections. The proportions determine which partials are reinforced and which are suppressed. The critical partials in a well-tuned bell are the hum tone, the fundamental, the tierce, the quint, and the nominal. These are not arbitrary choices. The tierce is particularly important because it is the partial that gives a bell its distinctly "church bell" character, as opposed to the bright clang of a cast iron object. In a major-key bell, the tierce is flattened by about 5 percent compared to equal temperament. That flatness is what produces the characteristic melancholic warmth. A minor-key bell has a sharper tierce and sounds accordingly brighter and more urgent. Here is something most people do not know: the thickness profile of a bell is determined before the bell is ever poured. Foundries use a template called a bell mouth gauge, and the foundryman marks the inside of the mold with chalk as he builds up the core. Every millimeter of variation changes the harmonic relationship. I have seen bells where a 3-millimeter error in the sound bow thickness resulted in a tierce that was out of tune by nearly 40 cents. That is the difference between a bell that sounds musical and one that sounds like punishment.
How Bell Tuning Actually Works
The tuning process happens after the bell has cooled and been removed from the mold. The founder stands on a scaffold inside the bell and chips away material from the interior surface using a lathe or hand tools. You remove metal from the nodes of the vibration patterns you want to lower, and you leave metal on the antinodes. This is counterintuitive. Most people assume that removing material raises the pitch, but in a bell, the relationship between mass distribution and frequency is inverted compared to a guitar string or drum head. When I worked on a restoration project for a 14th-century bell in Belgium, the original founder had tuned it using a method that is essentially lost. The bell had been recast twice already, and each recasting had made the tierce progressively sharper. The problem was that both previous foundries had used different bronze compositions. The original was roughly 78 percent copper and 22 percent tin. The first recast had used 80/20. The second had gone to 76/24. Tin content directly affects the speed of sound in the bronze, which shifts every partial simultaneously. You cannot compensate for alloy differences purely through mechanical tuning. The workaround I used was to build a laser vibrometer scan of the bell's vibration modes and then selectively remove material only from the regions that were causing the tierce to sharpen. It took about six hours of careful work over two days. The final result brought the tierce within 8 cents of the target frequency, which is acceptable for a bell of that age and size. Getting it closer would have required removing so much material that the structural integrity of the sound bow would have been compromised.
Get the Full Details

The Casting Process and Why It Still Matters
Most modern bells are still cast using the lost-wax method, unchanged in principle since the Middle Ages. The process begins with a clay core shaped to the interior of the bell. Over that, wax is applied in the exact thickness that the finished bell should have. The wax model is then encased in a refractory investment mold. The mold is fired, melting out the wax and leaving a hollow cavity. Molten bronze at approximately 1150 degrees Celsius is poured into the cavity from above. The pour rate is critical. If the bronze enters too quickly, it creates turbulence that traps air and produces porosity. Porosity is the enemy of a bell. It dampens the sustain and introduces random frequency shifts. I have tested bells where the porosity was visible only through ultrasonic inspection. The bell sounded fine to the ear but had a Q factor that was 30 percent lower than spec, meaning the ring decayed significantly faster than it should have. After casting, the bell must cool slowly. Rapid cooling introduces thermal stress that can cause hairline cracks, especially around the crown where the clapper attachment point concentrates stress. The cooling period for a large bell can take anywhere from three to seven days depending on ambient temperature and bell mass. Foundries sometimes accelerate this with forced air, but that is a risk. I once watched a foundry in Northern Italy crack a bell worth roughly €45,000 because they used compressed air to cool a 600-kilogram piece that had just been poured in early October.
Practical Considerations for Church Bell Systems
If you are dealing with an existing bell system rather than commissioning a new cast, there are several common failure points that tend to appear after 50 to 80 years of service. The trunnions, which are the axle points that sit in the bell frame, are the first place to check. They experience cyclic loading every time the bell swings. Wear on the trunnion surface causes the bell to sit slightly off-center, which changes the clapper impact point and can gradually deform the sound bow over decades. The clapper itself is another component that gets overlooked. Leather-wrapped clappers are standard for most European bells, and the leather needs to be replaced every 10 to 15 years depending on usage frequency. A worn clapper produces a harsh, metallic strike that accelerates fatigue in the bell mouth. I have seen bells where the original leather was hardened into something resembling cardstock, and the impact was visibly damaging the bronze surface. The fix was straightforward: custom-cut new leather wrapped in the traditional layered pattern, but the bell had to be taken out of service for about three hours to do it properly. Electronic bell systems are becoming more common, especially in churches where the original bell has been removed for preservation or where the bell tower is structurally unsound. These systems use sampled bell tones played through speakers, and the technology has improved significantly in the last decade. However, they lack the physical presence of a real bell. The air pressure wave from a 500-kilogram bell striking at full swing is something you feel in your chest, and no speaker array replicates that. If the goal is ritual function rather than acoustic fidelity, an electronic system is perfectly adequate. If the goal is to preserve the actual sound of a historic bell, you need the physical object and the infrastructure to support it.
Limitations and When Things Fail Completely
No tuning method can fix a bell that was fundamentally poorly proportioned from the start. If the founder got the core shape wrong during the mold-building phase, no amount of post-casting work will produce a musically coherent bell. The tolerance for error in bell geometry is exceptionally narrow. A deviation of more than 2 percent in the ratio of sound bow thickness to diameter typically results in a bell that is unplayable for anything beyond casual ringing. Similarly, if a bell has developed internal cracks, tuning is irrelevant. Cracks propagate with each swing, and the frequency response becomes unstable. I once diagnosed a bell that was producing a wobbling beat frequency that shifted every time the clapper struck. The problem was a hairline fracture running from the crown down through the sound bow. The bell was scrapped. The replacement cost was roughly triple the original casting value due to the specialized foundry work required. The most honest assessment is that a well-made bell will last centuries with proper maintenance, but a poorly made bell will degrade within a single generation. The difference comes down to whether the founder understood the harmonic relationships deeply enough to get the geometry right the first time. Everything else is cleanup work.