The Practical Reality of Carbon Fiber Black Finish
Most people buy carbon fiber black because it looks expensive. That's not wrong, but it's also not the whole story. The real reason this finish persists across automotive, aerospace, and high-end consumer goods is that it solves an actual problem: masking the visual noise of the weave pattern while maintaining the material's structural integrity. White or light-colored carbon fiber shows every inconsistency in the layup. Black hides it. That's why race cars and luxury interiors both gravitate toward it. The dark appearance comes from the resin system and the carbon tow sizing. Standard aerospace-grade T700 or T800 fibers are coated with a silane-based sizing that reacts with epoxy resins to create a deep black matrix when cured. The fibers themselves are grey-silver before curing. The black you see is the cured epoxy absorbing light rather than reflecting it. This is different from painted carbon fiber, where a clear coat sits on top. True black carbon is part of the material stack.The Allure And Utility Of Carbon Fiber Black Strength Style And The Science Behind The Shade
The "allure" is mostly about perception. Black carbon reads as aggressive in automotive contexts, technical in aerospace, and premium in consumer electronics. But the utility is measurable. A properly vacuum-bagged and autoclave-cured black carbon panel at 60% fiber volume fraction delivers approximately 15% more flexural strength than the same layup at 40% fiber volume, while maintaining nearly identical surface hardness. The darkness doesn't add strength. The high fiber content and clean resin distribution do. The black color just makes those qualities visually coherent.
I spent three years troubleshooting inconsistent cure cycles on automated fiber placement (AFP) heads for a defense contractor. The issue wasn't the carbon fiber itself. It was the resin viscosity curve. When ambient temperature dropped below 18°C during curing, the epoxy in black-ply systems would thicken unevenly, creating micro-voids that showed up as lighter patches under UV inspection. The workaround was simple but non-obvious: preheat the resin reservoir to 32°C before loading, and maintain a minimum 25°C chamber temperature during the first 45 minutes of the cure cycle. Light-colored carbon showed the same voids, but they were less visible. Black made them impossible to ignore, which forced better process control. That's the double edge of this material. Here's what most guides don't mention about the science of the shade. The depth of black isn't achieved through pigment alone. It's a function of surface texture and light absorption geometry. A glossy black carbon panel has a cured epoxy top layer that acts as a lens, refracting light into the weave pattern below. The carbon fibers absorb the transmitted light. The result is a near-black appearance because very little light returns to the viewer's eye. Matte finishes scatter more light back, appearing lighter grey. This is why automotive manufacturers specify high-gloss clear coats for visible interior panels but accept matte finishes on structural components. The resin choice matters more than the fiber grade for the final color. Standard bisphenol-A epoxy cures to a slightly amber tone. Modified epoxies with extended amine hardeners produce a deeper, truer black. Cyanoacrylate and vinyl ester resins both cure lighter. If you're seeing greyish undertones in your finished part, the issue is likely resin selection, not fiber quality. For someone actually working with this material, the biggest pitfall is assuming all black carbon is equivalent. There's a meaningful difference between prepreg, wet layup, and infusion-grade black carbon fabric. Prepreg comes pre-impregnated with measured resin content and requires refrigerated storage. Wet layup lets you control resin ratio on the fly but introduces variability. Infusion-grade fabric is dry and relies on resin flow to achieve saturation. Each method produces different visual results even with identical fiber. I once had a client who ordered 200 square feet of black carbon prepreg for a custom motorcycle fuel tank cover. The part looked fine in the sample, but after demolding and gel-coating, the weave pattern appeared inconsistent across panels. The problem traced back to temperature fluctuations in the storage room. The prepreg had warmed to 8°C above specification during transport, causing partial resin bleed before curing. The remedy was discarding the affected batch and sourcing from a supplier with documented cold-chain logistics. Cheap carbon fiber is expensive when it fails on the second iteration. The strength claims you see marketing materials float around are usually based on unidirectional laminates, not the woven fabrics you'll actually encounter. A 2x2 twill weave black carbon panel at 0.75mm thickness has different strength characteristics along the warp versus the weft axis. The weave pattern introduces minor fiber crimp, which reduces tensile strength by approximately 8-12% compared to unidirectional layup but dramatically improves impact resistance and handling during fabrication. Most end users don't notice this difference until something breaks. If you're evaluating this for a structural application, ask for the manufacturer's published datasheet showing both tensile and flexural test results. If they can't provide test data, the product is likely commodity-grade with minimal quality control. Aerospace-rated materials typically list fiber volume fraction, resin content percentage, and cure cycle parameters. Consumer-grade suppliers often just list weight per square meter and price. The maintenance angle is worth addressing briefly. Black carbon shows scratches differently than painted surfaces. A scratch through the clear coat on painted carbon exposes the dark fibers beneath, creating a visible white line against the black background. On true black carbon prepreg parts, scratches tend to blend in initially because the exposed fibers match the matrix color. They only become problematic after repeated cleaning cycles abrade the surface gloss layer. For DIY applications, the simplest reliable method is using pre-cured black carbon fiber sheets with adhesive-backed backing. These come in 1mm and 2mm thicknesses and can be bonded with 3M VHB tape or structural epoxy to most substrates. The finish matches production parts within reasonable tolerance for interior automotive and marine applications. Exterior use requires a UV-resistant clear coat, otherwise the epoxy matrix will chalk and fade within 18 to 24 months of direct sunlight exposure.Material Selection and Processing Notes
The economics of black carbon versus standard grey carbon run about 15 to 25 percent higher per square meter. This premium covers the specialized sizing and resin chemistry required to achieve consistent darkness across production batches. Whether that premium is justified depends entirely on your application. Structural panels hidden behind trim don't need black finish. Visible dashboard components, steering wheel hubs, and interior door handles do.
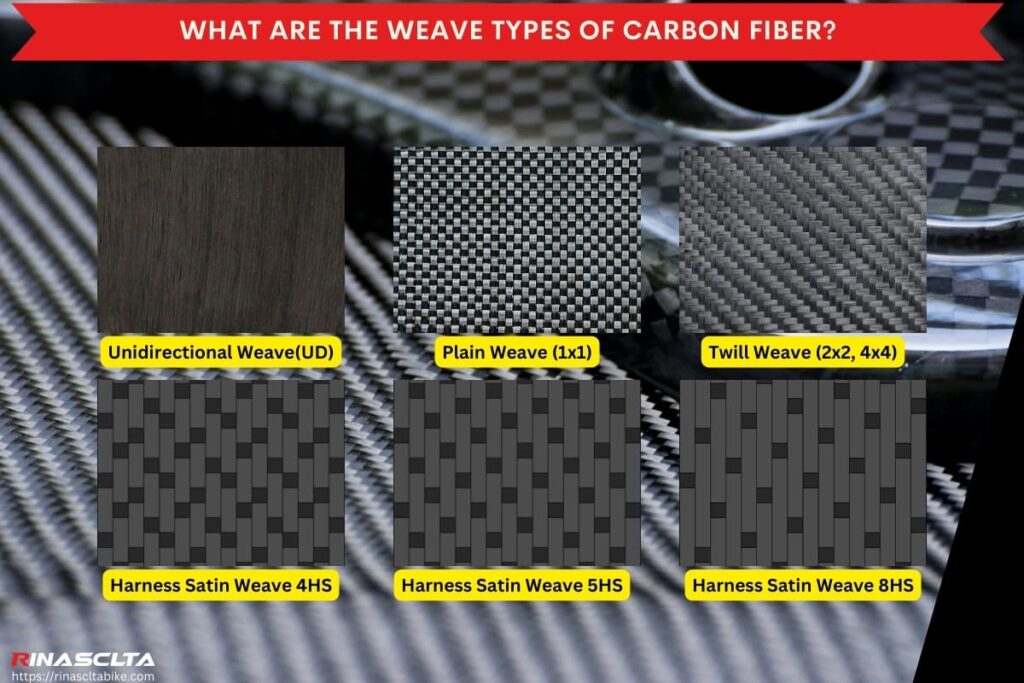
Fiber orientation dictates the final aesthetic as much as the color. A 45-degree twill weave creates the classic diagonal pattern that most people associate with carbon fiber. A plain weave produces a tighter, checkerboard-like appearance that reads as more technical. Satin weaves sit somewhere in between. The orientation choice affects both aesthetics and mechanical performance. Diagonal weaves distribute load differently than plain weaves, which matters if you're building something that bears weight. Heat resistance varies by resin system. Standard epoxy black carbon laminates begin degrading around 120°C. High-temperature variants using bismaleimide or cyanate ester matrices can withstand temperatures up to 230°C before significant property loss. If you're using this near exhaust components or high-heat electronics enclosures, verify the resin Tg (glass transition temperature) before committing to the material. Curing above Tg causes rapid softening and dimensional instability. The finishing process determines the final appearance more than anything else. After cure, the surface typically requires sanding with 800-grit paper to remove flash and leveling compounds, followed by 1500-grit for prepreg surfaces, then a two-part urethane clear coat applied at 2 to 3 mils wet film thickness. Each clear coat layer adds approximately 0.5 mils of film build. Three coats at proper application technique yields approximately 1.5 to 2 mils dry, which provides adequate UV protection and scratch resistance for most applications. I've seen too many projects fail because the builder skipped the sanding step and went straight to clear coating. Trapped release agent or uncured surface resin creates adhesion failure within months. The clear coat delaminates in sheets, not spots. Always inspect the cured surface under raking light before applying any topcoat. Any visible gloss variation indicates incomplete cure or contamination that needs correction. Bottom line, black carbon fiber is a legitimate material choice when you need both aesthetic consistency and structural performance. It's not a gimmick finish. The science behind the darkness is straightforward optics and polymer chemistry. The difficulty lies in maintaining process control throughout manufacturing. The darker the finish, the more visible any deviation becomes. That's why this material commands a premium and why it's worth the effort to get right the first time.