
Working with Right Isosceles Triangles in Practice
Most people learn about the 90-45-45 triangle in high school geometry and then never think about it again until they actually need one for something real. I ran into this repeatedly in structural framing and CAD layout work. The theory is simple. Applying it without mistakes is where things get interesting.The 90 90 45 Triangle Unlocking The Hidden Geometry In Your Right Isosceles World
A right isosceles triangle has two equal legs and a hypotenuse that is exactly leg times the square root of two. That 2 ratio shows up everywhere once you start paying attention. Roof pitches, tile layouts, diagonal bracing, even certain CNC toolpaths. The angle is always 45 degrees on the acute sides, which makes it predictable in a way most other triangles aren't. Here's what nobody tells you: the 2 relationship means you can never lay out an exact 45-degree diagonal using only rational measurements. Every time you need a precise 45-degree line, you're dealing with an irrational number. In the shop or on a job site, you work around this. I usually snap a chalk line using the 3-4-5 method adapted for 45 degrees, or I just use a speed square and trust the tool. For CAD work, you set the angle directly and let the software handle the irrationality. I worked on a custom stair case project where the stringer needed a perfect 45-degree run. The spec called for a rise and run that were mathematically identical. I measured twice, cut once, and still ended up with a gap at the top landing because the floor wasn't perfectly level. The triangle was right. The world wasn't. I added a shim plate to compensate. Always check your reference surfaces before you commit to the cut.
When the Basic Formula Falls Apart
The hypotenuse equals leg multiplied by approximately 1.41421356. That's clean enough for most rough work. But in precision fabrication, that irrational decimal becomes a problem. I've seen people round too early and end up with pieces that don't match up. If you're cutting metal or woodworking joinery where tolerance matters, keep at least four decimal places through your calculations and only round at the final measurement stage. Another thing that trips people up: assuming all right triangles with a 45-degree angle are the same size. They're similar, yes, but similarity doesn't help you cut a specific piece. You need the actual leg length to determine the hypotenuse. I once had someone bring me a drawing labeled "45-degree triangle" with no dimensions. I asked for the leg length three times before they realized they'd omitted it. Don't skip the dimension callout.
Practical Layout Methods
For on-site work, the diagonal method is the fastest. Measure equal distances along both legs from the right angle corner, then connect those points. That line is your hypotenuse. If your legs are each 24 inches, the hypotenuse is 24 times 2, which comes to about 33.94 inches. Mark that distance across and you're set. In CAD, the approach is different. You draw the two legs perpendicular to each other with equal length, then connect the endpoints. Most drafting software has a direct angle input option where you can specify 45 degrees and let the geometry resolve itself. I prefer constraining the two legs to be equal length using the software's dimension constraints rather than typing angles. It's faster and less prone to rounding errors.
Get the Full Details

Common Mistakes I See Repeatedly
The biggest one is confusing the 90-90-45 triangle with the 30-60-90 triangle. They look somewhat similar on paper if you're not paying close attention, but the ratios are completely different. A 30-60-90 has side ratios of 1 to 3 to 2. Mix those up and your structural calculations will be off by a significant margin. I've seen this happen in load-bearing bracket designs where someone grabbed the wrong triangle formula from memory. A second mistake is using a standard protractor for 45-degree layout when a speed square or calibrated triangle is available. Protractors have parallax error and hinge play. A good speed square is rigid and accurate to within a fraction of a degree. The difference matters when you're laying out multiple consecutive 45-degree cuts. There's also the issue of material thickness. When you're cutting a 45-degree bevel on a piece of stock, the measured length changes depending on which edge you're measuring from. The face width at the top of the bevel is shorter than at the bottom. I usually measure along the flat surface before the cut and verify with a test piece if the joint is critical. This is especially relevant in mitered frame work where two 45-degree cuts meet at a corner.
Where This Geometry Actually Matters
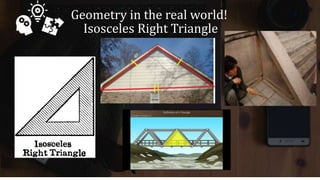
Roof framing is probably the most common real-world application. A standard gable roof with a 45-degree pitch means the rafters form right isosceles triangles in cross-section. The horizontal run equals the vertical rise. This simplifies layout because you don't need complex pitch tables. Measure the span, divide by two for the run, and that's also your rise. Tiling is another area where this comes up constantly. Diagonal tile layouts follow 45-degree lines relative to the room walls. If your room isn't perfectly square, those 45-degree lines won't align with the edges the way you expect. I always snap reference lines from the center of the room rather than from the walls. It takes two extra minutes and saves you from figuring out a mistake after you've already set six tiles. CNC and laser cutting benefit from this geometry too. Toolpath optimization for 45-degree features is straightforward because the feed rate can remain constant along the diagonal. Unlike arbitrary angles where you need to recalculate vector components, a 45-degree cut has equal X and Y movement. The machine controller handles it efficiently.
Limitations to Keep in Mind
The 90-90-45 triangle works perfectly in theory and in most practical applications, but it has clear boundaries. It only applies when you need equal legs at a right angle. If your application requires a different proportion, forcing a 45-degree solution will give you the wrong geometry. Don't use it just because it's familiar. Material constraints can also make a pure 45-degree layout impossible. Thin or flexible materials like sheet metal or thin plywood may spring or deflect during cutting, causing the angle to drift. I've dealt with this on sheet metal work where the laser kerf and material tension shifted the cut path by nearly a degree. In those cases, I do a test cut on scrap first and measure the actual result before committing to the production piece. There's also the tolerance stack-up problem in assemblies. A single 45-degree joint might be within spec, but chain multiple joints together and the error compounds. I once assembled a framework with eight consecutive 45-degree miter joints and the final closure panel was off by nearly three-eighths of an inch. The individual joints were all fine. The accumulated error was the problem. Breaking the assembly into smaller sub-assemblies and checking each one helped contain the drift.
If you need higher precision than a 45-degree layout can reliably provide, consider switching to a different geometric approach or using CNC machining instead of manual layout. Manual methods are fast and usually sufficient, but they have a ceiling on accuracy that you'll hit eventually.


